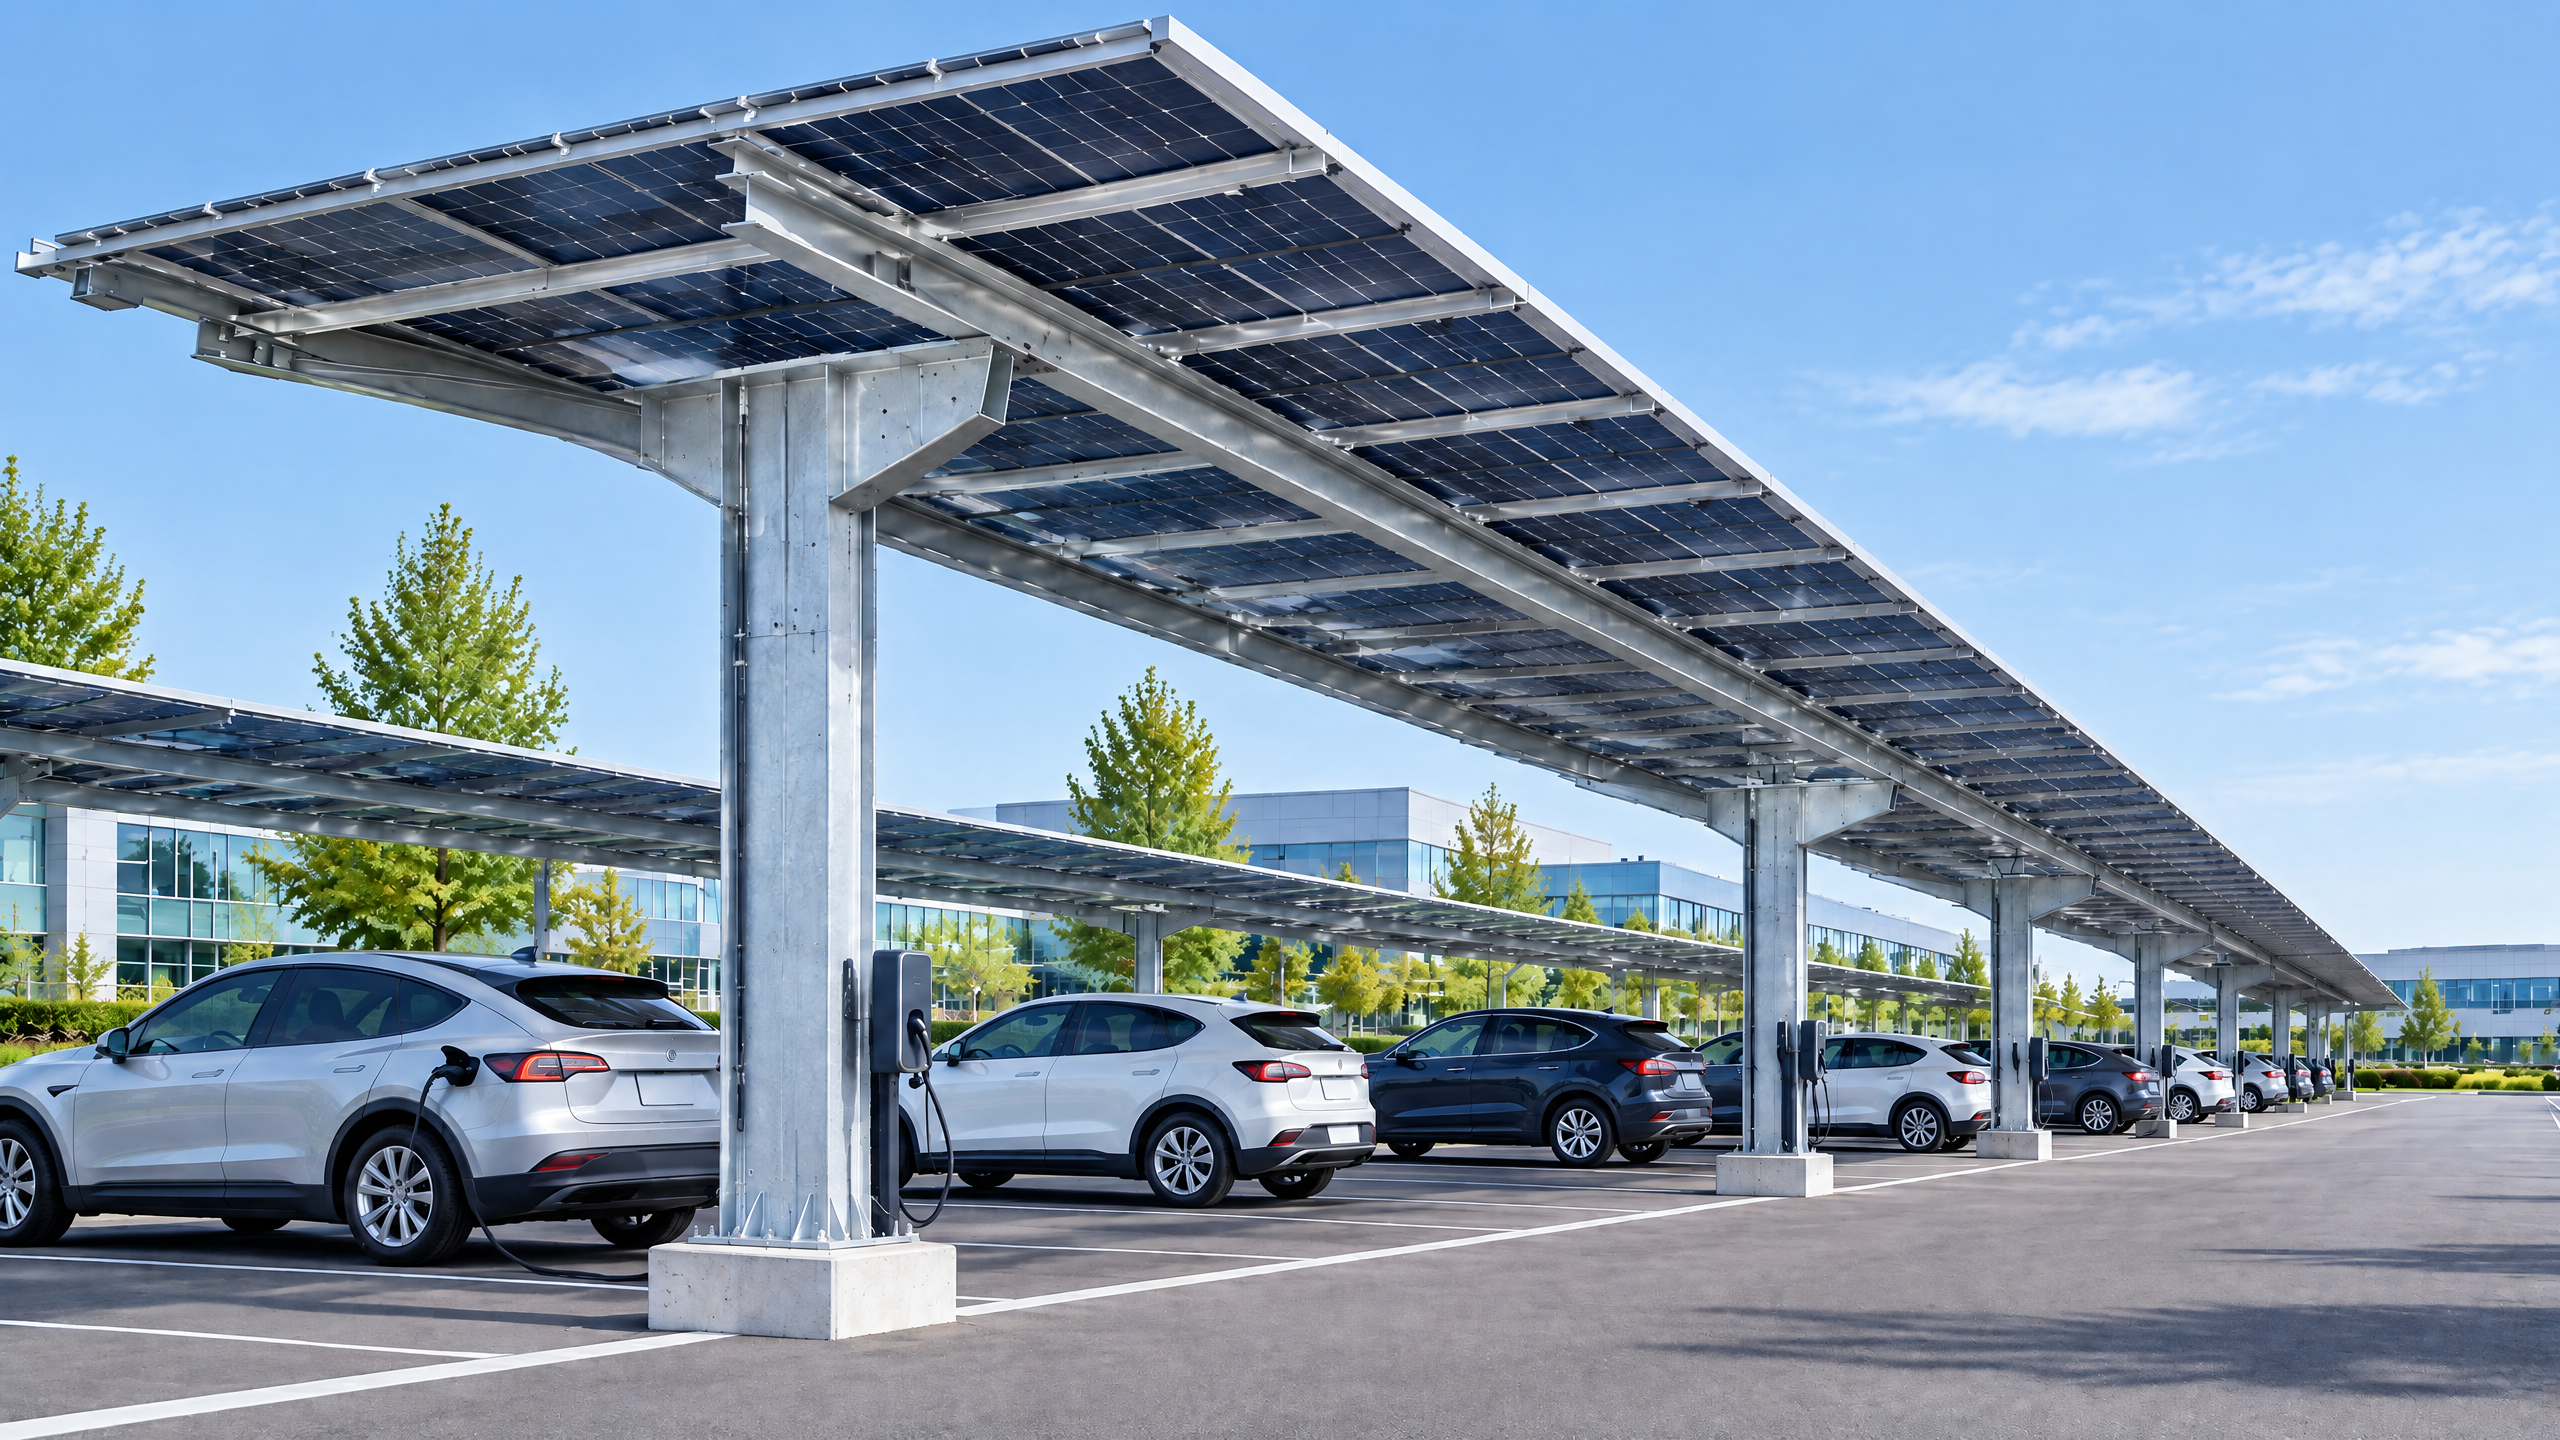
Industrial carport manufacturer supplier evaluation matters whenever a project’s cost, complexity, performance risk or lifecycle obligations are significant enough that supplier selection, contractual clarity and factory processes materially affect outcomes. For commercial or industrial carports — including architectural aluminium canopies, fleet shelters and commercial solar carports — the decision to perform structured supplier evaluation is driven by variables such as project value, bespoke structural requirements, electrical or PV integration, local permitting complexity, warranty exposure and logistics (cross-border export/import). Carrying out formal industrial carport manufacturer supplier evaluation reduces downstream delays, prevents scope gaps between supplier and installer, and converts qualitative trust into documented evidence (technical scope comparison, factory quality documentation, delivery responsibility matrix and project procurement controls). Where projects involve integrated electrical works, energy yield targets, long asset lives or multiple stakeholders, evaluation is not optional — it is a procurement control and risk-management activity that should be specified in the buyer’s documented project basis.
Buyer context and scope boundary
Who should read this guide
- Distributors, architects, contractors, developers, solar EPCs and fleet operators procuring commercial or industrial carports.
- Buyers managing either stand-alone shelter projects or integrated solutions (for example, solar carports with rooftop PV and electrical balance-of-system).
- Procurement leads who must translate project requirements into enforceable supplier obligations and documented evidence.
What “industrial carport manufacturer supplier evaluation” covers
- Evaluation focuses on the manufacturer(s) who supply primary metalwork, engineered frames, cladding, mounting interfaces and factory-assembled modules for commercial/industrial carports and fleet shelters.
- It does NOT replace site-specific structural engineering, foundation design, on-site electrical design or local permit approvals; those remain the responsibility of local qualified professionals, installers, utilities and authorities on a documented project basis.
Boundary examples (what the evaluation should and should not include)
- Included: manufacturing tolerances, structural loads and wind/ snow design assumptions as supplied by the manufacturer, connection details for electrical or PV interfaces, factory QA records, export packing coordination and logistics readiness.
- Excluded: geotechnical analysis, foundation design, local electrical distribution design (metering, main switchgear), building permits and grid interconnection approvals — these require local professionals and documented project deliverables.
Mandatory buyer statement for every project Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Core decision principle: when evaluation changes project outcome
The core decision principle is: perform supplier evaluation when doing so materially reduces the probability of a commercially significant adverse outcome (delay, rework, non-compliance, warranty exposure, energy shortfall or safety issue). Use three lenses to test materiality:
- Financial threshold — the absolute or relative value at which supplier failure would be financially significant (for many organisations this is a project spend, not a per-unit price).
- Technical complexity — bespoke spans, heavy-duty vehicle loading, integrated PV systems, or non-standard finishes increase the technical stakes.
- Integration and logistics — cross-border shipments, multi-vendor interfaces, and tight project schedules heighten the need for factory evidence and export packing coordination.
Decision guidance table: when to apply evaluation depth
| Decision driver | Light evaluation | Medium evaluation | Deep evaluation |
|---|---|---|---|
| Project value | <$50k or low relative exposure | $50k–$250k or medium exposure | >$250k or high exposure |
| Technical complexity | Standard, catalogued canopy | Larger spans, custom geometry | Integrated PV, bespoke structural loads |
| Logistics complexity | Local manufacture/delivery | Regional export/import | International shipping, phased deliveries |
| Stakeholders | Single buyer/installer | Buyer + installer + 3rd party | Multiple stakeholders, EPC, utility, developer |
| Recommended actions | Basic quotes, references | Detailed RFQ, sample approvals, site visit | Full B2B supplier due diligence, FAT, contractual delivery responsibility matrix |
Note: the financial thresholds above are illustrative guides—each buyer should set thresholds appropriate to their organisation and project portfolio.
Planning inputs: project procurement controls before supplier contact
Project procurement controls are the rules, thresholds and required documents you set before engaging suppliers. Clear planning inputs reduce ambiguity and speed technical scope comparison.
Essential planning inputs to prepare
- Documented project basis: scope narrative, owner, project location(s), estimated budget, preferred timeline and funding conditions.
- Design inputs: architectural drawings, structural load cases (basic wind, snow, live loads), canopy clearances, vehicle loading assumptions and connection points for electrical or PV systems.
- Interface matrix: who supplies foundations, who supplies PV modules/inverters, who is responsible for electrical interconnection, who handles signage or lighting.
- Procurement controls and approvals: single-point buyer contact, contract approver, technical approver, insurance requirements, inspection rights and acceptance criteria.
- Logistics and customs inputs: preferred Incoterm, import licenses, handling at port and inland haulage assumptions.
- Sustainability and lifecycle requirements: expected service life, coating or galvanizing longevity, maintenance regimes and spare parts plan.
RFI/RFQ package checklist
- Cover letter with procurement controls and submission deadline
- Scope split (supplier-supplied items vs buyer-supplied items)
- Drawings: general arrangement (GA), elevation and section views
- Load cases and structural notes (to be verified by manufacturer)
- Materials and corrosion protection specification
- Finish and colour standards
- Interface details for PV module racks and conduit entries
- Packing and shipping instructions (if buyer requires specifics)
- Acceptance criteria and inspection rights (pre-shipment and on-site)
- Commercial terms (warranty obligations, payment milestones, penalties)
- Contact details and required response formats
Embedding project procurement controls in the RFQ reduces change orders and helps when performing a technical scope comparison between suppliers.
Technical specification and interfaces
A precise technical scope comparison is the heart of effective industrial carport manufacturer supplier evaluation. It reveals where suppliers interpret requirements differently and where contract language must close gaps.
Key technical elements to compare
- Structural performance and design assumptions (code basis if applicable)
- Connection and interface details for foundations and civil works
- Corrosion protection: galvanizing, powder coat, duplex systems and expected lifecycle (refer to accepted practices for galvanizing) [1]
- Tolerances and assembly fit-up: bolt types, pre-drilled holes, slotted connections
- Electrical and PV interfaces: mounting rails, conductor routing, cable entry points, earthing provisions, penetrations and PV module clamp interface
- Thermal expansion and drainage details
- Transport and lifting points for pre-assembled modules
- On-site assembly sequence and recommended installers’ competencies
- LCA/recyclability or recyclable aluminium claims (if required)
Technical scope comparison table (example structure)
| Specification element | Buyer minimum requirement | Supplier response format | Verification/documentation required |
|---|---|---|---|
| Structural design standard | Project-specific load cases; statement of design code used | Declaration of code + signed engineer calculations | Engineering calculations, material mill certificates |
| Corrosion protection | Hot-dip galvanize to specified grade or duplex system | Process description + coating thickness | Factory quality documentation + coating thickness test |
| PV mounting interface | Module clamp compatibility, clamp spacing | 3D details and module layout | Interface drawings and mock-up / sample |
| Fixings & fasteners | Stainless or hot-dip galvanized per environment | Fastener specification and sourcing | Material certs and inspection records |
| Packing & transport | Export packing coordination to avoid damage | Packaging method, crate dimensions | Photos, packing list, export packing plan |
Include technical scope comparison early in the evaluation to align expectations and avoid later rework.
Procurement and factory evidence
B2B supplier due diligence should be evidence-led. The buyer needs verifiable artifacts rather than only sales statements. For manufacturing and logistics this means factory quality documentation, inspection plans, and clear agreements on export packing coordination.
Minimum factory evidence and documentation you should request
- Corporate information: legal entity, factory address, ownership and primary contact.
- Quality system statement: ISO 9001 or equivalent quality management system evidence where applicable (ISO [2]); if no formal certification, request internal QA manuals and process maps.
- Material traceability: supplier lists for primary materials and mill/test certificates for structural steel or aluminium.
- Factory quality documentation: incoming material inspection records, welding procedures, welders’ qualifications, coating application records, dimensional inspection protocols and non-conformance reports.
- Factory Acceptance Test (FAT) plan: test items, acceptance criteria, witness options and FAT documentation templates.
- Pre-shipment inspection procedures: third-party inspection arrangements or buyer inspection rights.
- Packing and shipping plan: export packing coordination including crating, internal bracing, desiccants, blocking, lifting points and shipping marks.
- Lead-time confirmation and production schedule with milestone dates (e.g., material release, fabrication completion, pre-shipment inspection date, shipment date).
Supplier evidence checklist decision table
| Evidence category | Acceptable evidence | Minimum buyer action |
|---|---|---|
| Quality system | ISO certificate or internal QA manual | Accept or request corrective action plan |
| Material traceability | Mill certificates or batch numbers | Verify sample certs for critical items |
| Welding & fabrication | WPS/PQR, welder IDs | Require on-site or third-party inspection for critical welds |
| Coating & corrosion protection | Coating application records; thickness test | Request test reports and take sample tests |
| FAT & inspection | FAT protocol; witness options | Schedule FAT or appoint third-party inspector |
| Packing & shipping | Packing plan; photos of pack types | Require export packing coordination and pre-shipment photos |
Important: when transport crosses borders, pack specifics and documentation affect customs and damage risk. For guidance on packing and import procedures, consult local customs advice and general import guidance [4].
Delivery responsibility and Incoterms Agreeing delivery responsibilities early prevents disputes. Reference widely-used Incoterms to define which party is responsible for export packing, shipment booking, insurance and import formalities (Incoterms, see ICC guidance) [3]. Use a delivery responsibility matrix to translate commercial terms into operational obligations.
Delivery responsibility matrix (illustrative)
| Activity | EXW | FCA | FOB | CIF | DDP |
|---|---|---|---|---|---|
| Manufacture & packing | Seller | Seller | Seller | Seller | Seller |
| Export packing coordination | Buyer unless specified | Seller if included | Seller | Seller | Seller |
| Inland transport to port | Buyer | Buyer or Seller as agreed | Seller | Seller | Seller |
| Export customs clearance | Buyer | Seller (if agreed) | Seller | Seller | Seller |
| International carriage | Buyer | Buyer or Seller as agreed | Buyer | Seller | Seller |
| Insurance | Buyer | Buyer | Buyer | Seller (minimum) | Seller |
| Import customs & duty | Buyer | Buyer | Buyer | Buyer | Seller |
Note: this table is illustrative — always specify precise responsibilities and expected documentation in the contract. See ICC Incoterms rules for formal definitions [3].
Practical procurement controls to deploy
- Require pre-production approval (PPA) drawings and get sign-off on critical dimensions and interfaces.
- Specify inspection rights and FAT witness options in the contract.
- Define packing standards and require pre-shipment photos and packing lists.
- Stipulate penalty or remedy clauses for missed milestones and non-conforming products.
- Use a staged payment schedule tied to verifiable milestones (material release, fabrication completion, shipment, site acceptance).
Standards and verification points
- Reference applicable standards where relevant (structural design codes as per project basis).
- For galvanizing and corrosion protection, rely on accepted industry guidance (American Galvanizers Association) for best practices and testing [1].
- For quality system expectations, request ISO 9001 documentation where appropriate [2].
CTA (mid-article) If you need bespoke procurement controls or help collecting factory evidence for a specific project, contact /inquiry or info@carportiva.com. For integrated PV projects, see our SolarGrid commercial solar system and review other all systems and sourcing guides.
Site installation and operations
Clear split of responsibilities between manufacturer, installer and buyer is essential for successful on-site works. The supplier’s obligations often end at delivery or site acceptance; the buyer must ensure installers are qualified and that site adaptations are planned.
Who supplies what: typical division
- Manufacturer: primary frame, prefabricated canopy modules, mounting rails for PV mounting, bolted connections and pre-drilled holes, material certificates, and packing lists.
- Buyer or appointed installer: foundations, anchor bolts, civil works, conduit routing, final PV/electrical termination and grid integration.
- Installer/contractor: erection supervision, torque checks, on-site adjustments, sealing and final coatings if site patches needed.
- Local authority/utility: permits, inspections and grid interconnection approvals.
Installation submittals to require from manufacturer
- Erection manual with supervised steps and recommended lifting tools.
- Bolt torque and tightening sequence documentation.
- Recommended tolerances for foundation anchor positions and acceptable rework limits (slotting allowances).
- On-site adjustment details for drainage and thermal movement.
- Spare parts list and recommended maintenance schedule.
Operational handover items
- As-built drawings and signed completion checklist.
- Manufacturer certificates and warranties (clearly stating limits and exclusions).
- Maintenance manual and spare parts location/ordering information.
- Final acceptance test reports and, for solar carports, a baseline energy yield modelling report prepared by relevant professionals (energy yield requires local validation).
Legal and regulatory reminder Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risk: common failure modes and mitigations
Identifying implementation risks early enables targeted mitigations. Below are typical failure modes for industrial carport procurement and recommended buyer controls.
Key risks and mitigations
- Misinterpreted scope (e.g., mounting rails not compatible with selected PV modules)
- Mitigation: technical scope comparison, interface mock-ups, pre-production approvals and explicit PV mounting compatibility requirements.
- Quality variance in factory production
- Mitigation: factory quality documentation review, FAT, third-party inspection, sample tests and tight material traceability.
- Damage during transport
- Mitigation: explicit export packing coordination, pre-shipment photos, robust crating and cargo insurance.
- Customs hold-ups or missing import documents
- Mitigation: early customs classification, shipping instructions, and ensuring documents match packing list/BL—consult import guidance [4].
- Late deliveries with knock-on effects to civil works or PV commissioning
- Mitigation: enforceable delivery responsibility matrix, staged deliveries, buffer time in schedule, and liquidated damages where appropriate.
- Warranty disputes and owner expectations
- Mitigation: clearly defined warranty terms, exclusions and a process for claims supported by factory documentation and site acceptance records.
- On-site installation clashes with foundations or adjacent structures
- Mitigation: precise foundation templates, site verification survey before fabrication, and an allowance for field adjustments documented in the contract.
Risk matrix example (high-level)
| Risk | Likelihood | Impact | Mitigation |
|---|---|---|---|
| Interface mismatch with PV modules | Medium | High | Require interface detail submission and a sample mock-up |
| Corrosion failure in aggressive environments | Low–Medium | High | Specify duplex corrosion system and require coating records |
| Customs/documentation delays | Medium | Medium | Early export packing coordination, verify HS codes and paperwork |
| Fabrication quality issues | Low–Medium | High | Third-party inspection, FAT, factory quality documentation review |
Carportiva Six-Step Supplier Evaluation Workflow
A repeatable, named workflow helps procurement teams convert evaluation into disciplined outcomes. Apply this workflow proportionate to project complexity.
Carportiva Six-Step Supplier Evaluation Workflow
Step 1 — Define: Documented project basis and procurement controls
- Deliverable: Project brief with scope split, timeline, critical interfaces, and procurement thresholds.
- Actions: Identify decision makers, set evaluation depth (see decision table), and prepare RFQ/RFI package.
Step 2 — Shortlist & due diligence
- Deliverable: Shortlist of 2–5 suppliers with company profiles.
- Actions: Run B2B supplier due diligence including corporate verification, references, financial stability check and high-level factory capability review.
Step 3 — Technical scope comparison & PPA
- Deliverable: Comparative technical scope table and pre-production approval (PPA) plan.
- Actions: Request technical clarifications, obtain PPA drawings for critical items and confirm PV mounting compatibility and structural assumptions.
Step 4 — Contractual clarity and delivery responsibility matrix
- Deliverable: Signed contract with clear Incoterm, delivery responsibility matrix and acceptance criteria.
- Actions: Specify packing standards, inspection rights, payment milestones, lead times, penalties and warranty language.
Step 5 — Factory approval, FAT & pre-shipment verification
- Deliverable: Factory quality documentation, FAT report and pre-shipment inspection certificate.
- Actions: Execute FAT, verify factory quality documentation, confirm export packing coordination and schedule shipment.
Step 6 — Delivery, site acceptance & post-delivery controls
- Deliverable: As-built drawings, site acceptance reports, spare parts and maintenance manual.
- Actions: Coordinate unloading, perform site acceptance, document non-conformances and record warranty handover.
Checklist summary for each step
- Who signs off (role)
- Documents required
- Timeline expectations
- Acceptance criteria
This workflow scales: for low-risk projects, compress steps; for high-risk or high-value projects, allocate more time and incorporate third-party verifications.
Frequently asked questions (FAQ)
Q: What is industrial carport manufacturer supplier evaluation? A: It is a structured, evidence-led process for assessing manufacturers supplying industrial/carport structures and integrated systems. It combines B2B supplier due diligence, technical scope comparison, factory quality documentation review, logistical planning and contractual delivery obligations to reduce procurement risk.
Q: How does B2B supplier due diligence differ from a normal supplier quote? A: Due diligence goes beyond price quotes to verify corporate status, factory capability, quality systems (ISO or equivalent), material traceability, past project references, and risk exposures. It produces documentary evidence for contract and project teams.
Q: What documentation should I insist on before production starts? A: Pre-production approval (PPA) drawings, material mill certificates, welding and coating records, a FAT plan, and a clear export packing coordination plan. These form the basis of factory quality documentation.
Q: Which delivery terms should I use? A: That depends on your logistics capability and risk appetite. Incoterms define responsibilities; use a delivery responsibility matrix to convert the commercial Incoterm into operational tasks and documentation [3]. If you want the seller to handle import customs, DDP is an option but requires caution and clear pricing.
Q: How do I manage PV integration for a solar carport? A: Require detailed PV mounting interface drawings, specify module clamp compatibility, and include an energy yield validation that will be prepared and verified by local professionals. See SolarGrid commercial solar system for system-level planning and our sourcing guides for procurement checklists.
Q: Should I rely on supplier quality certificates like ISO? A: A supplied ISO certificate (ISO 9001) is a positive indicator of documented processes, but it should be accompanied by factory quality documentation, mill certificates and inspection evidence. Ask for process records relevant to your project [2].
Q: What are practical steps to avoid damage in transit? A: Define export packing coordination requirements in the contract, require pre-shipment photos, mandate internal bracing and rated lifting points, and ensure cargo insurance during international transport. Check customs documentation guidance where applicable [4].
Q: Can I perform inspections remotely? A: Yes, in many cases remote inspections (photos, video calls, and third-party remote inspection reports) are effective, especially for repeat suppliers. For critical welds, coatings or complex assemblies, a witnessed FAT or third-party on-site inspection is recommended.
Q: What should a delivery responsibility matrix include? A: It should list each logistical and contractual responsibility (packing, export clearance, insurance, carrier booking, inland transport, import clearance) and assign seller or buyer roles for each activity. Map these roles to milestone payments and acceptance points.
Q: Does supplier evaluation replace local approvals? A: No. Supplier evaluation controls the manufacturer-supplier relationship and factory quality. Local approvals — structural sign-off, permits, grid interconnection — must be handled by local qualified professionals and authorities on a documented project basis.
Conclusion
Industrial carport manufacturer supplier evaluation becomes essential whenever the cost, complexity, logistics or integration of a carport project can materially affect schedule, quality or long-term performance. Use a structured, evidence-led approach: set project procurement controls, require technical scope comparison and factory quality documentation, define a clear delivery responsibility matrix, and perform targeted B2B supplier due diligence. For PV-integrated projects, ensure PV interface verification and coordinate with your electrical and grid professionals. For practical next steps, use the Carportiva Six-Step Supplier Evaluation Workflow, require pre-production approvals and factory acceptance testing, and embed contractual clauses that align responsibilities with risk.
If you would like assistance applying these controls to a live procurement, contact /inquiry or info@carportiva.com. For integrated system options, review SolarGrid commercial solar system, explore all systems, or consult our sourcing guides.
Final reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
References and further reading
- American Galvanizers Association: galvanizing best practices and testing [1]
- International Organization for Standardization: quality management systems and related standards [2]
- International Chamber of Commerce: Incoterms rules and responsibilities [3]
- U.S. Customs and Border Protection: import guidance and documentation best practice [4]
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion