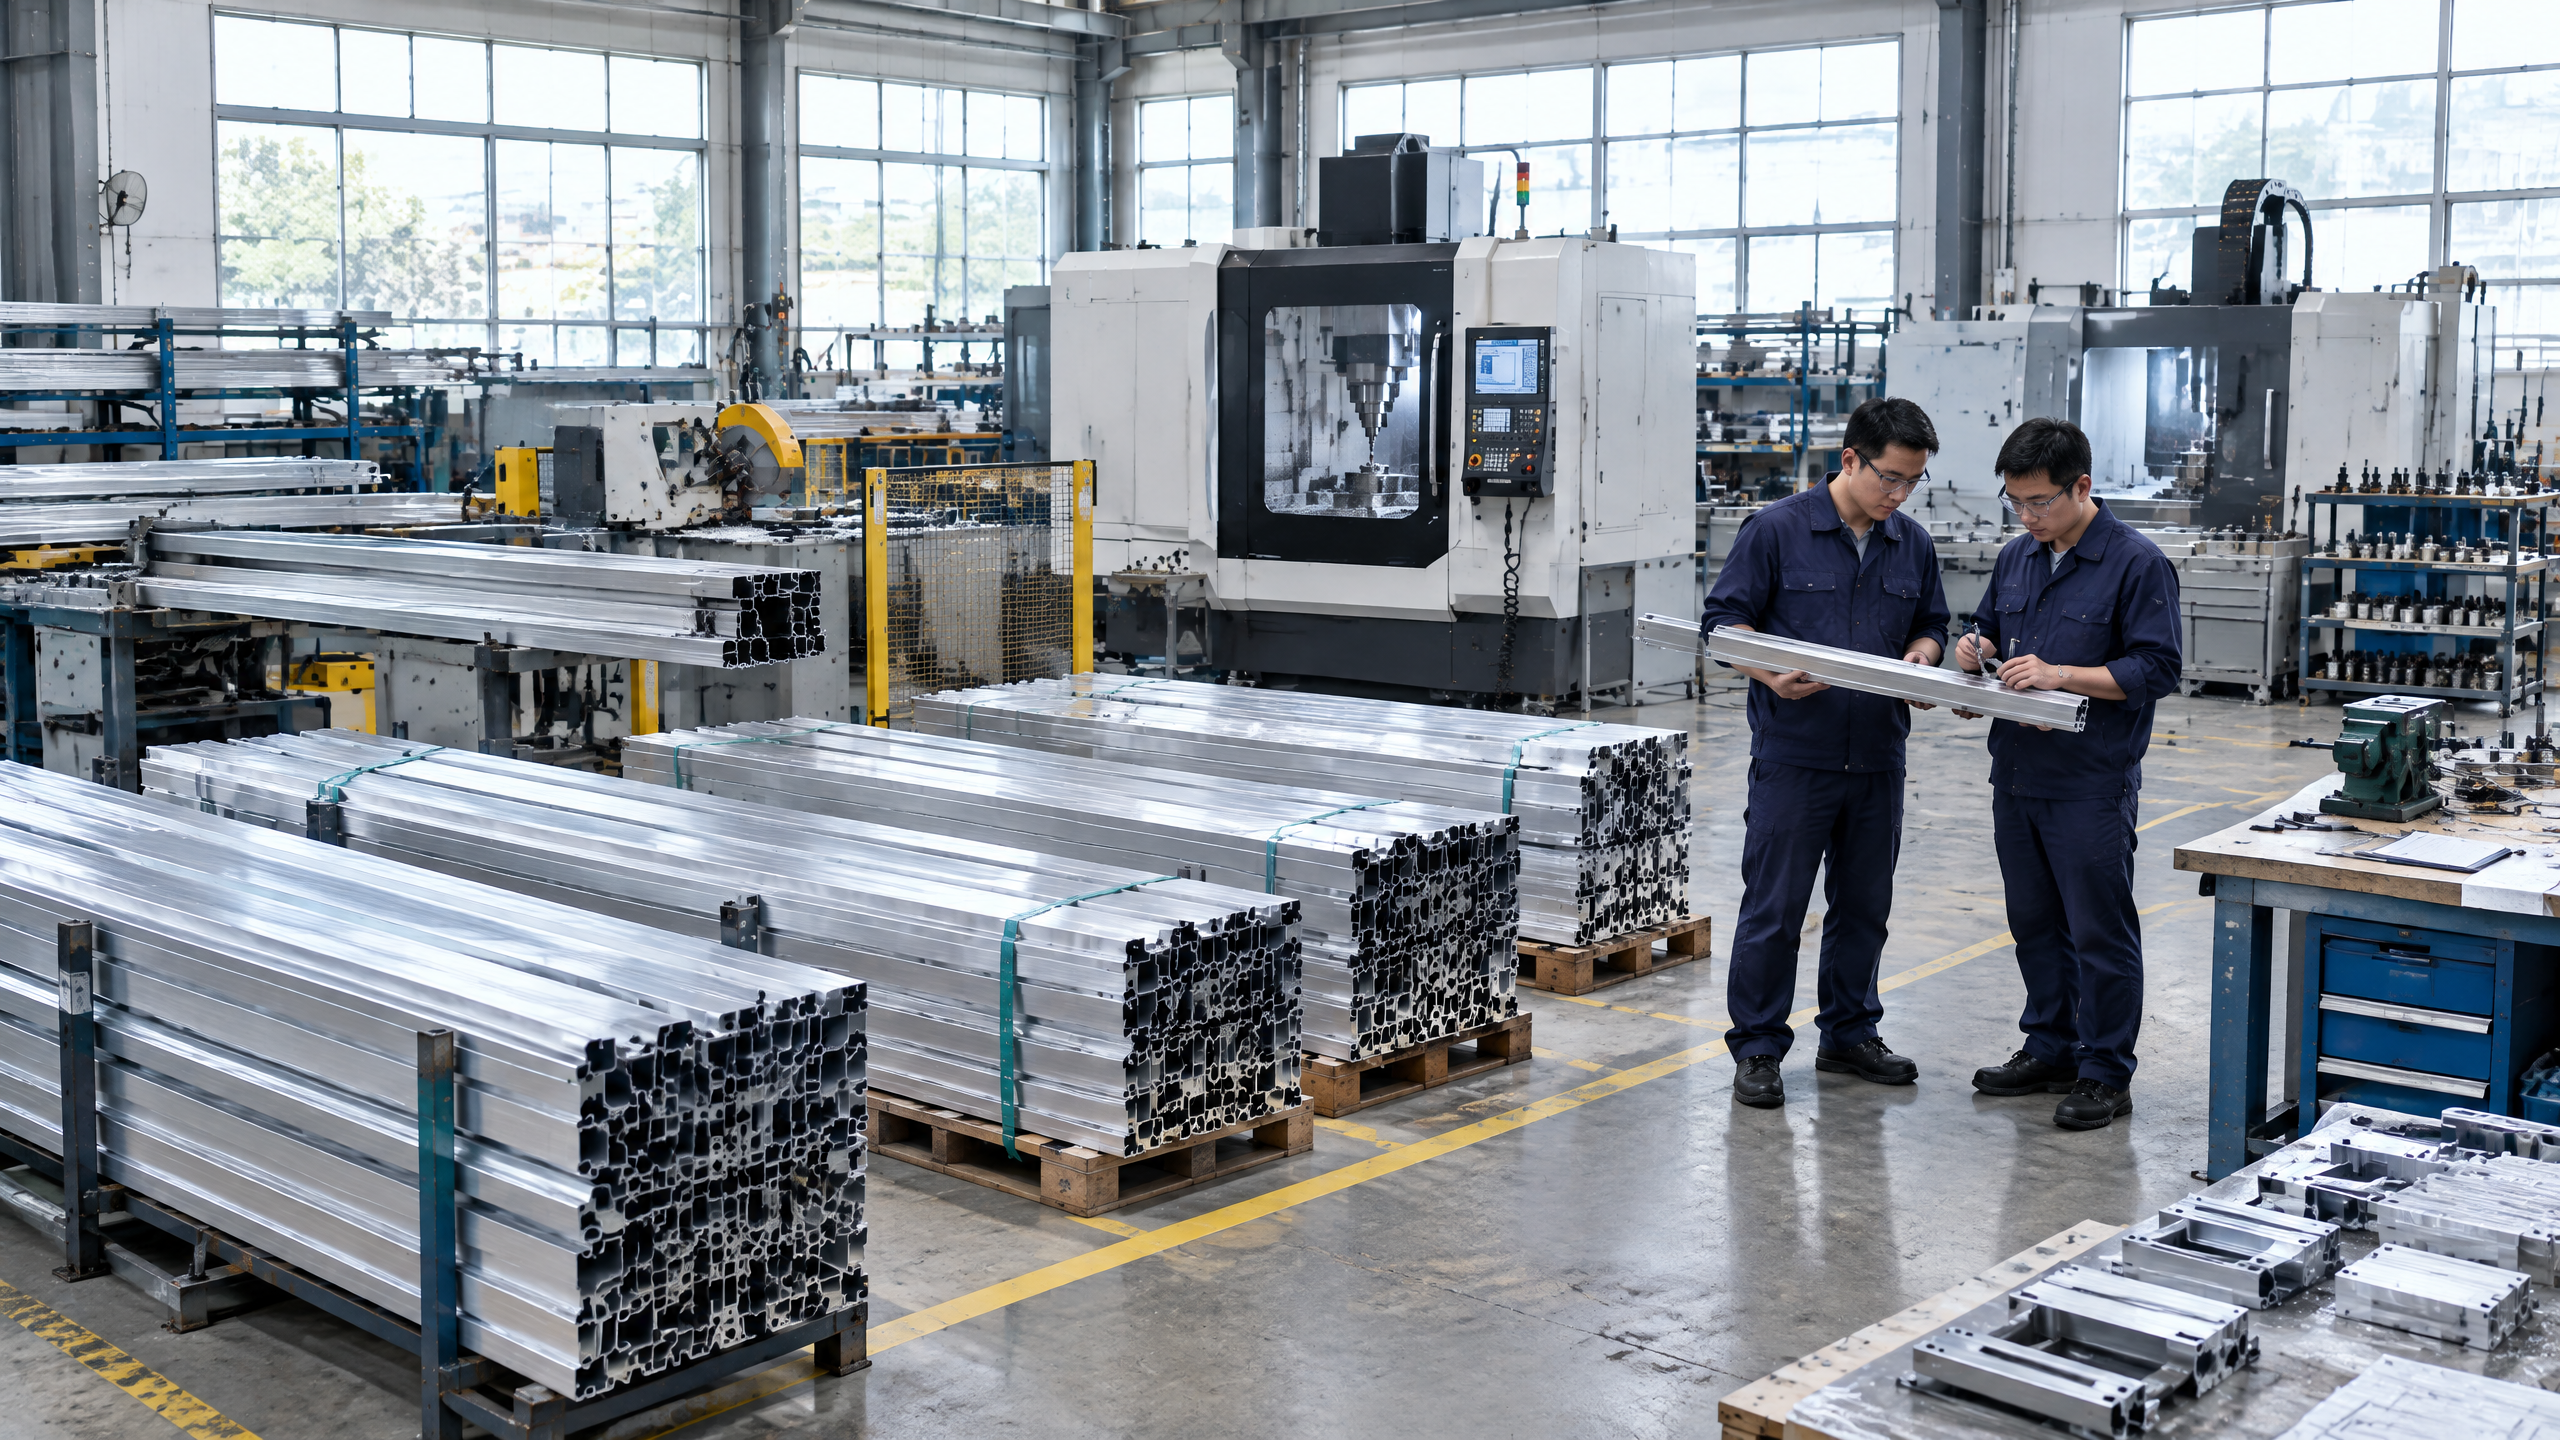
Answer (short): When a project team considers purchasing an aluminum carport manufacturer factory direct, the team must confirm the complete split of responsibilities between buyer and manufacturer, validate the manufacturer’s capacity and documented factory quality documentation, compare technical scope and site interfaces, and establish logistical and commercial controls that align with the project risk profile. Essential confirmations include: documented technical scope comparison showing included and excluded items (foundations, electrical works, PV mounting interfaces); written B2B supplier due diligence evidence (company profile, financial stability indicators, quality system alignment); an agreed delivery responsibility matrix using recognized Incoterms; export packing coordination and transport conditioning; and formal project procurement controls for approvals, inspections and change orders. Site-specific matters—structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty—require a documented project basis and the input of qualified local professionals, installers, utilities and authorities.
Buyer context and scope boundary: what "factory direct" typically means for aluminum carports
"Factory direct" commonly refers to procuring finished or semi-finished carport systems straight from the manufacturer rather than through a distributor or local fabricator. For aluminum carports and solar carports this can mean anything from full-supply of engineering-drawn primary frames and canopy members to “knock-down” kits that rely on local foundations, electrical works and on-site installation teams.
Key scope boundary considerations to confirm:
- Whether the manufacturer supplies design-to-manufacture services (shop drawings, structural calculations) or only produces to purchaser-supplied drawings.
- Which items are included: primary structure, purlins, canopies, fixing hardware, fasteners, solar PV modules or only module mounting rails, edge trims, and accessories.
- Who is responsible for foundations, local civil works, ground fixing, on-site erection and local electrical termination.
- Whether the manufacturer will supply spares, lifting/installation fixtures, and on-site supervision.
These scope boundaries should be captured in contract documents and illustrated in a delivery responsibility matrix (see later table). Early clarity protects both procurement scheduling and liability allocation during installation and warranty periods.
Core decision principle: risk allocation, total cost of ownership, and project controls
The core principle when deciding to buy aluminum carport manufacturer factory direct is to align commercial price advantage with effective risk transfer and the buyer’s capacity to manage site integration. A lower unit price from factory direct supply is only advantageous if the buyer can reliably manage the additional scope they take on: local structural interface, permits, storage, customs and logistics, and installation coordination.
Ask whether the project team has:
- The technical capability to verify manufacturer engineering (or budget for third‑party review).
- The operational capacity for inbound logistics, on-site staging, and supervising erection.
- Project procurement controls to manage change, inspections, and acceptance milestones.
- Access to local installers and authorities to accept as-built deviations.
If any of these are lacking, the buyer should either procure additional services from the manufacturer (engineering, installers, supervision) or work via a distributor/turnkey provider that bundles those responsibilities.
Planning inputs: essential information to assemble before issuing a factory-direct RFQ
A robust RFQ/IFB for factory direct supply reduces ambiguity. Minimum planning inputs to assemble:
- Project scope and objectives: target use (architectural, commercial solar, fleet shelters), capacity, desired finishes, photovoltaic integration if required, and service life expectations.
- Site data package: topographic survey, geotechnical report, climatic loading data (wind, snow), seismic zone, site access limitations, vehicle turning and clearance requirements.
- Permit and approval requirements: expected local approvals, statutory standards, and authority contacts.
- Foundation and ground conditions: anticipated foundation types or whether foundations are included.
- Electrical scope: whether PV stringing, DC combiner, inverter locations, and AC connection are included.
- Programme constraints: milestone dates, required installation window, and end-to-end lead time tolerance.
- Commercial terms: target Incoterm(s), insurance expectations, and currency and payment schedule.
Note: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Technical specification and interfaces: what to compare and verify in a technical scope comparison
When engaging a manufacturer factory direct, a formal technical scope comparison is critical. The comparison aligns buyer expectations with what the supplier will deliver and makes latent exclusions visible.
Elements to include in a technical scope comparison:
- Structural design basis: codes used, wind and snow load assumptions, seismic design approach, and safety factors.
- Material specification: aluminum alloy and temper, surface finish (anodised or powder coat), corrosion protection strategy for interface elements, bolting and fastener grades.
- Connection details: bolted vs welded connections, torque requirements, corrosion protection at joints.
- Dimensional and clearance tolerances: critical for vehicle shelters, turning radii and headroom.
- PV mounting and electrical interfaces: module clamping method, rail-to-module interface, grounding, and provision for cable trays/conduits.
- Transportation breakdown: number of packages, component weights, handling points, and export packing coordination responsibilities.
- On-site assembly documentation: erection drawings, torque charts, lifting drawings, and required installation plant (cranes, mobile elevating work platforms).
Include “technical scope comparison” as a stand-alone document appended to the commercial offer. This prevents disputes over what the manufacturer intended to supply and what the buyer expects.
Technical scope comparison table (example)
| Scope Item | Factory Direct Supply (Typical) | Buyer Responsibility (Typical) |
|---|---|---|
| Primary frame fabrication | Supplied to shop drawings | Provide site centerlines & foundation levels |
| Foundations | Optional — specify if included | Usually buyer; supply local concrete & reinforcement |
| Surface finish (aluminum) | Powder coat/anodize specified by supplier | Confirm colour and sample approvals |
| PV mounting rails | Supplied if PV option | PV modules, inverters, electrical termination |
| Erection supervision | Optional (paid) | Local installers unless supervision contracted |
| Certification/structural calculations | Supplier may provide | Buyer should require stamped calculations for local approvals |
Use the technical scope comparison to inform the contract and the acceptance tests. When structural calculations are supplied, confirm whether they are sealed for the project jurisdiction or whether buyer will obtain local stamp/review.
Procurement and factory evidence: B2B supplier due diligence and factory quality documentation
A disciplined procurement process for factory direct acquisition must include B2B supplier due diligence that goes beyond price. Evidence-based checks reduce downstream defects and delivery delays.
Minimum due diligence and factory evidence items:
- Corporate and financial background: company registration, years in operation, principal product lines, and references for comparable projects.
- Manufacturing capability and capacity: plant location(s), key equipment (CNC, extrusion presses for aluminum), production lead times and seasonality.
- Quality management systems: evidence of an ISO-aligned quality system, factory quality documentation (inspection plans, incoming materials control, non-conformance procedure). Cite ISO guidance where appropriate [2].
- Fabrication and finishing controls: process flow for extrusion, machining, anodising or powder coating, and final assembly.
- Traceability practices: batch/lot traceability for critical components and fasteners.
- Testing and inspection: factory acceptance test procedures, weld/connection inspection protocols, and nondestructive testing where applicable.
- References and site visit reports: completed projects (with client permission) and third-party audit reports.
- Export & customs experience: familiarity with export packing coordination, required export documents and customs forms for the buyer's import jurisdiction. Where applicable, confirm knowledge of import formalities using national customs guidance [4].
- Logistics capabilities: shipping partners, packaging methods for long transits, and handling specifics for oversized elements.
Factory quality documentation checklist (example)
| Documentation | Why it matters | Minimum expectation |
|---|---|---|
| Quality manual / QMS evidence | Shows process discipline | Evidence of ISO or written QMS procedures [2] |
| Inspection test plans (ITP) | Defines acceptance points | ITP per major assembly with buyer sign-off milestones |
| Material certificates | Verifies alloy/grade | Mill/test certificates for primary alloys and fasteners |
| Welding & joint procedures | Ensures joint integrity | Procedure and welder qualifications (if steel components) |
| Packing list & export packing plan | Prevents shipping damage | Detailed crate weights, dimensions and handling notes |
| Factory acceptance test (FAT) protocol | Gate for shipment | FAT criteria and witness options for buyer or agent |
In many projects, buyers specify a pre-shipment FAT or FAT sampling and reserve the right to withhold final payment until documented acceptance milestones are met. If the manufacturer will not host a buyer witness, arrange third-party inspection.
Export packing coordination and customs: confirm who prepares export packing lists, crate markings, and whether packaging is designed for sea, air or road transport. For complex cross-border shipments, align packaging and documentation with customs guidance relevant to the importer [4].
Delivery responsibility matrix (decision table)
| Responsibility Area | Manufacturer Factory Direct | Buyer / Local Contractor |
|---|---|---|
| Design & manufacture of structural components | Manufacturer | Provide site coordinates and design basis |
| Structural calculations & local stamping | Manufacturer provides calculations; buyer to obtain local stamp if required | Buyer engages local engineer for seal/approval |
| Export packing coordination | Manufacturer to prepare according to agreed packing plan | Buyer approves packing plan and arranges import clearance |
| International shipping & insurance | As per agreed Incoterm (see contract) | Buyer arranges customs clearance, inland transport if Incoterm indicates |
| On-site installation | Optional; typically buyer/installer | Buyer hires installers; manufacturer may provide supervision |
| Commissioning & handover | Provide installation manuals and certificates | Buyer carries out final acceptance with manufacturer support as needed |
When allocating delivery responsibilities, reference recognized Incoterms for clarity on costs, risks and insurance obligations [3]. For example, Ex Works shifts most responsibility to the buyer, while Delivered Duty Paid assigns more responsibility to the seller; choose the term that matches your logistics competence.
Site installation and operations: inbound logistics, lifting, installation sequencing and handover
Factory-direct deliveries must be planned for site realities. Even perfectly produced components can be delayed, damaged or misinstalled without clear site installation and operations planning.
Key site considerations:
- Staging and storage: ensure secure, level laydown areas with protection from weather or theft. Confirm package sizes and weights in advance so temporary storage and lifting equipment can be arranged.
- Offloading and craneage: provide lifting plans, lifting points and recommended crane capacities. Clarify who supplies cranes and slings—manufacturer-supplied lifting lugs may have specific orientation requirements.
- Foundations interface: verify as-built foundation positions with the manufacturer’s anchor-bolt template before fabrication completion. Where possible, lock down foundation design early and issue anchor-bolt templates to contractors.
- Sequence planning: develop a critical path schedule that incorporates installation windows, required weather conditions, and local authority restrictions (night works, noise).
- Supervision and training: decide whether factory supervision is included. If not, require the manufacturer to supply detailed erection drawings, torque values, and installer training documents.
- Spare parts and maintenance spares: procure a defined list of recommended spares (fasteners, clamps, gaskets) and agree on lead times for replacements.
- Handover documentation: require as-built drawings, installation records, torque logs, material certificates and warranty documentation as a condition of final acceptance.
Operational readiness checks: prepare a checklist for post-installation verification (plumb, level, torque checks, electrical continuity and earth bonding where relevant). These checks should be part of the formal handover.
Implementation risks and mitigations: risks unique to factory-direct aluminum carport procurement
Factory-direct procurement shifts several classes of risk to the buyer. Understanding and mitigating these reduces cost and schedule exposure.
Major risk areas and mitigations:
- Technical mismatch risk: shop drawings or structural assumptions not aligned to site as-built. Mitigation: require manufacturer to accept only when provided final site baselines; include a "review and approval" phase for shop drawings with clear RFI timelines.
- Lead time and supply chain risk: extrusion, finishing or shipping delays. Mitigation: demand clear lead-time commitments in contract, hold a manufacturing slot reservation clause, and develop contingency plans for partial deliveries.
- Customs and import clearance delays: paperwork errors or missing duty documentation. Mitigation: require manufacturer experienced with export packing coordination and provide complete export documentation; buyer to confirm importer registration requirements in advance [4].
- Damage in transit: long packaging chains expose components to damage. Mitigation: specify packaging standards, internal bracing and lifting protection; include pre-shipment inspection and insurance arrangements.
- Installation quality variance: local installers unfamiliar with proprietary connection details. Mitigation: procure installation supervision, or require manufacturer to provide certified installer training and a project-specific installation manual.
- Warranty and liability ambiguity: disagreements over what component or interface is covered. Mitigation: define warranty scope in the contract and require the factory to provide a clear warranty statement; record acceptance milestones to trigger warranty.
- Interface failure (foundations, electrical): incorrect anchor-bolt placement or conduit routing errors. Mitigation: use anchor-bolt template sign-off and incorporate electrical interface drawings into the contract.
Project procurement controls to manage these risks include staged payments tied to objective inspection milestones, retention amounts pending final acceptance, and a documented change control process that captures variations to the original scope.
Six-step buyer workflow for purchasing aluminum carports factory direct
A repeatable workflow helps B2B buyers ensure consistent outcomes. Here is a named six-step buyer workflow:
- Define and document project baseline
- Deliverables: project brief, site data package (survey and geotechnical), permit list, performance targets.
- Actions: identify critical interfaces and local code requirements; compile responsibilities list.
- Technical scope comparison and specification
- Deliverables: Technical scope comparison, Bill of Materials (BOM) template, installation requirements.
- Actions: circulate comparison to shortlisted manufacturers to ensure like-for-like offers.
- Supplier screening and B2B supplier due diligence
- Deliverables: supplier questionnaire, factory tour checklist, reference checks, QMS evidence.
- Actions: evaluate manufacturing capacity, factory quality documentation, export experience and logistic partners.
- Commercial offer, delivery responsibility matrix and contract negotiation
- Deliverables: signed delivery responsibility matrix (by Incoterm), detailed contract with acceptance milestones, FAT protocol.
- Actions: lock in lead times, payment schedule, penalties or incentives for milestones and define warranty terms.
- Pre‑production approval and factory acceptance testing (FAT)
- Deliverables: approved shop drawings, sample finishes, ITPs, FAT witness options.
- Actions: approve samples, perform pre-shipment inspections and sign off FAT results before shipment.
- Logistics, installation, commissioning and handover
- Deliverables: packing list, customs documentation, installation supervision arrangements, as-built documentation and warranties.
- Actions: execute transport and delivery, supervise erection, perform commissioning checks and sign final acceptance.
This workflow must be supported by project procurement controls: versioned document management, designated sign‑off authorities, an RFI register, and a change order log. These controls preserve auditability and reduce disputes.
Frequently asked questions (FAQ)
Q: How should I select the right Incoterm for factory-direct purchase? A: Select an Incoterm that reflects your logistics capability and appetite for risk. If you have strong customs, inland transport and site handling capacity, Ex Works may yield a better price but requires more buyer resources. If you prefer the seller to manage import duties and delivery to site, consider Delivered Duty Paid (DDP). Always align insurance and risk transfer milestones to the chosen Incoterm [3].
Q: What documentation should a buyer insist on before shipment? A: Minimum documentation: approved shop drawings, material mill test certificates, ITP and FAT reports, packing lists and export documentation, and shipping insurance certificates. For customs clearance, a complete commercial invoice and packing list are essential—confirm any additional forms with local customs guidance [4].
Q: Are manufacturer FATs sufficient, or should I use third-party inspection? A: A manufacturer FAT is necessary but may not be sufficient if buyer lacks technical presence. Third-party inspectors provide independent verification of dimensions, material certificates and packaging quality. Consider contractual right to witness or appoint an agent to attend FATs.
Q: How to manage warranty for hybrid supply chains (manufacturer/installer)? A: Split warranties into component warranties (manufacturer) and workmanship/installation warranties (installer). Ensure responsibilities and overlap are clearly documented, and define contact points for warranty claims and response times.
Q: Can I require the factory to provide anchor-bolt templates? A: Yes. Anchor-bolt templates are a low-cost, high-value deliverable that prevents misalignment during installation. Make acceptance of anchor-bolt templates a milestone prior to foundation pouring where feasible.
Q: What if the manufacturer refuses to provide stamped structural calculations for my jurisdiction? A: If the manufacturer cannot legally stamp calculations locally, require them to provide full calculation packages and coordinate with a local registered engineer to review and re-stamp for local approvals. This approach is commonly used for cross-border supply.
Practical procurement checklists and decision aids
Below are two compact decision aids you can reuse in procurement meetings.
Decision aid: Buy factory direct vs local turnkey
| Factor | Factory Direct Advantage | Local Turnkey Advantage |
|---|---|---|
| Unit price | Often lower for large volumes | May be higher due to markups |
| Control over quality | Higher if buyer enforces inspection | Turnkey provider manages end-to-end QA |
| Integration risk (foundations, electrical) | Higher — buyer must manage interfaces | Lower — turnkey bundles scopes |
| Lead time predictability | Depends on manufacturer capacity | Can be managed with local buffer stocks |
| Customs/logistics handling | Buyer responsibility (if Ex Works) | Turnkey may absorb customs and delivery risk |
Decision aid: When to require factory supervision
| Condition | Recommended Action |
|---|---|
| Project uses non-standard connections or custom geometry | Require manufacturer on-site supervision |
| Local installers inexperienced with product | Require manufacturer training and supervision |
| High-value PV-integrated carports with critical electrical interfaces | Require manufacturer coordination with electrical contractor |
| Strict warranty enforcement desired | Require supervision to validate installation method |
Mid-article next step
If you would like a tailored technical scope template or to discuss how Carportiva’s product range maps to factory-direct procurement, start a project conversation here: /inquiry. You can also review the Carportiva system range for product options and all systems for our complete portfolio.
Contractual and legal points: payment, acceptance and change control
Ensure contracts define:
- Payment schedule tied to objective milestones (deposit, pre-shipment, post-delivery, final acceptance).
- Acceptance criteria with discrete stage sign-offs (shop drawing approval, FAT sign-off, on-site erection acceptance).
- Change control procedures governing variations to scope, costs and schedule, including an agreed rate card for field changes.
- Retention amounts or warranty retention to protect the buyer from latent defects.
- Intellectual property and use of shop drawings (who may use the drawings for local permitting or future maintenance).
Use clear language to allocate risk rather than relying on general statements. Employ a delivery responsibility matrix that maps the exact responsibilities and link the matrix to contract clauses for clarity.
Quality assurance and testing: what to expect in factory quality documentation
Factory quality documentation should define the product lifecycle from incoming material to final packing:
- Incoming material inspection and traceability (mill certificates for aluminum).
- In-process inspection points (profile tolerances, hole alignment, surface finish checks).
- Final inspection and packing criteria (dimension checks, assembly fit tests).
- Non-conformance reporting and disposition records.
- Calibration records for testing equipment.
- Maintenance of the QMS and records retention policy.
Where available, insist on documentation that conforms to internationally recognized quality principles and seek third-party inspection where buyer risk is high. ISO guidance may be used as a reference in quality discussions [2].
Logistics and customs practicalities
Shipping and customs can erode factory-direct advantages if not planned early:
- Confirm packaging meets international shipping standards—components should be immobilised, protected from moisture and mechanically secured for stacking.
- Obtain accurate volumetrics and weights early to optimise container loading and avoid unexpected freight surcharges.
- Verify whether any components attract special duties or import licensing in the destination country and confirm who handles such payments.
- Plan for inland transport and delivery windows—site constraints (narrow roads, weight restrictions) can require special handling.
- For cross-border shipments, align documentation with local customs guidance [4] and ensure export packing coordination responsibilities are contracted.
Records and handover: closing the loop
Handover documentation is the primary defence against future disputes. Require:
- As-built drawings and deviation notes.
- Material certificates and traceability logs.
- Torque logs and critical measurement sheets.
- Installation training records and signed completion certificates.
- Warranties with clear start dates tied to handover milestones.
Retention of these records in a project document management system and designation of a single point of contact for warranty matters expedites future servicing.
Conclusion
Buying aluminum carport manufacturer factory direct can deliver competitive costs and technical consistency when the buyer rigorously documents scope, verifies factory capability, and implements strong project procurement controls. The essential confirmations include a robust technical scope comparison, vetted B2B supplier due diligence, complete factory quality documentation, and a clear delivery responsibility matrix tied to contract clauses and an appropriate Incoterm. Plan export packing coordination and logistics early, and require factory acceptance tests and as-built documentation before final payment. Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
If you want to discuss how these considerations apply to your next project or to review product compatibility, contact us: /inquiry or info@carportiva.com. For product details, see the Carportiva system range and related sourcing guides.
References
- American Galvanizers Association: guidance on corrosion protection and galvanizing practices where steel interfaces exist [1].
- International Organization for Standardization: quality management principles and system guidance [2].
- International Chamber of Commerce Incoterms: use Incoterms to define delivery, risk and cost transfer [3].
- U.S. Customs and Border Protection: example import/export documentation requirements and procedures [4].
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion