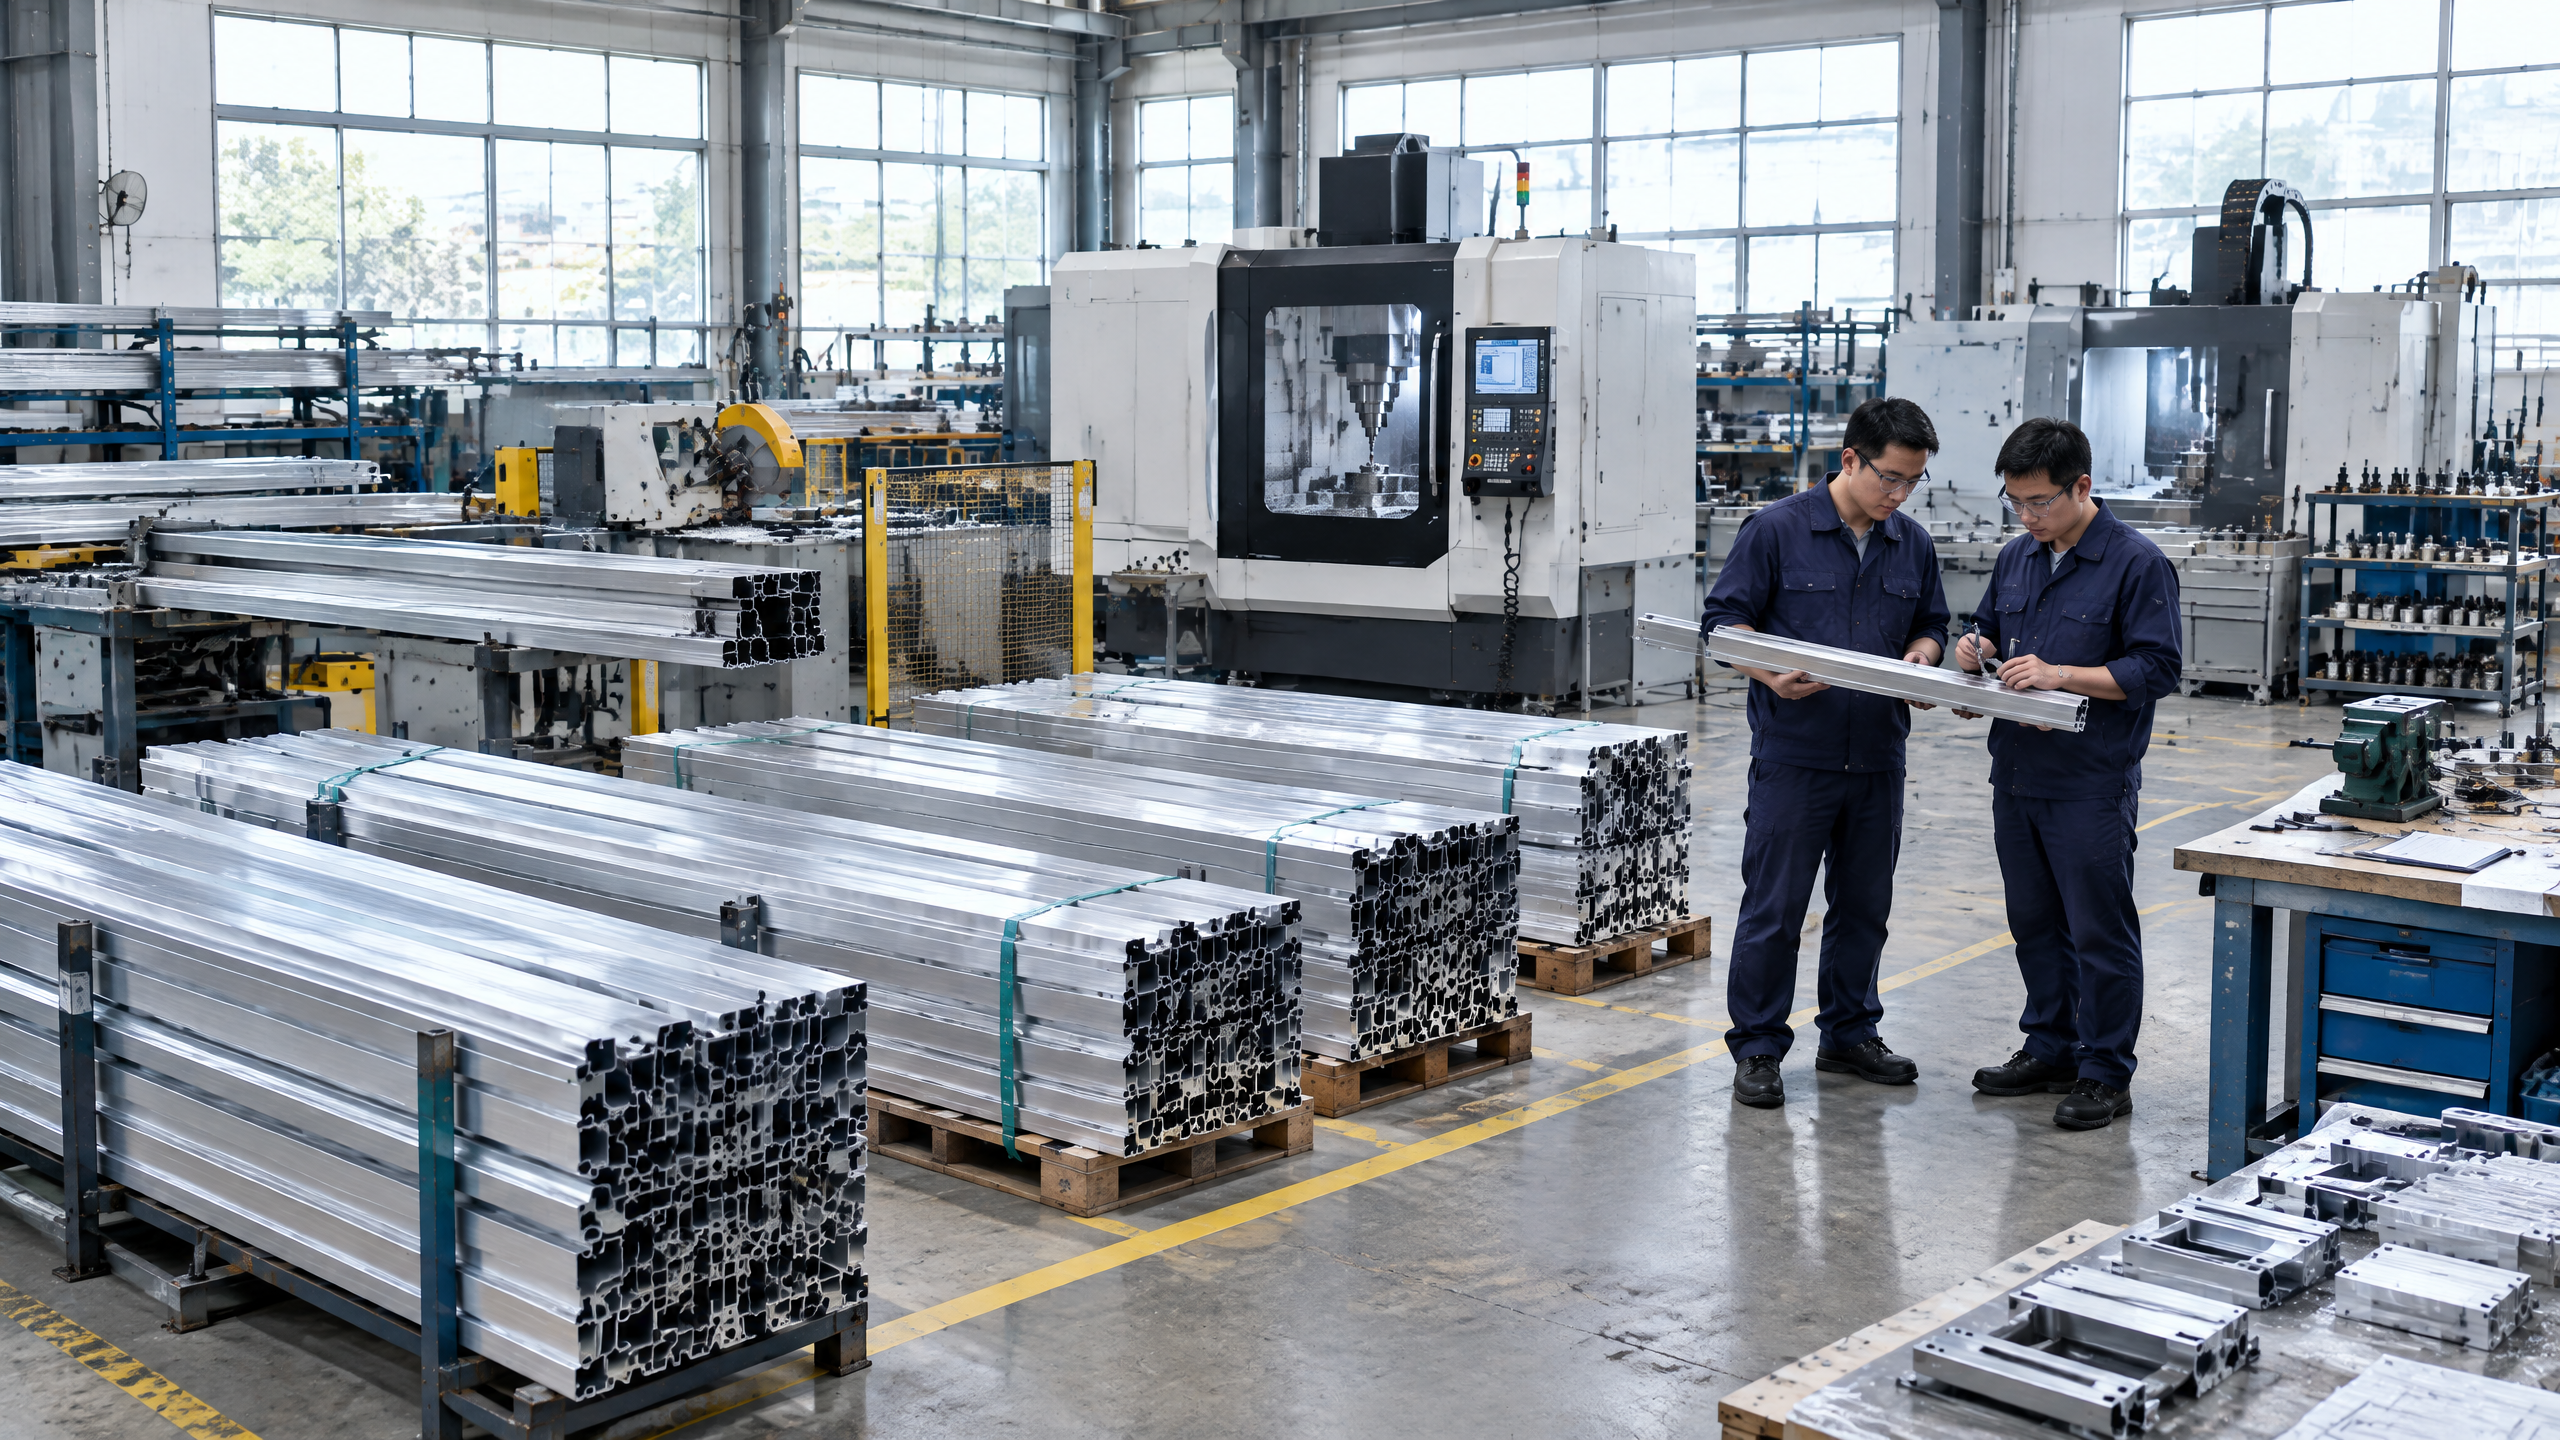
Direct answer (120–180 words) Carport container shipping delivery inspection matters whenever the buyer needs verifiable assurance that materials leaving the factory and arriving on site match the contracted technical scope, packing standard and acceptance criteria — and when the procurement, customs or installation chain exposes the goods to damage or substitution risk. For B2B carport procurement (architectural aluminium carports, commercial solar carports, industrial/fleet shelters) the inspection question should be decided against project procurement controls, supplier capability and chosen Incoterm. Key triggers include complex multi‑component deliveries, long sea voyages, high value or bespoke assemblies, and projects where delayed or damaged shipments would cause significant construction, revenue or safety impacts. A clear delivery responsibility matrix, factory quality documentation and coordinated export packing reduce uncertainty; pre‑shipment and container shipping delivery inspections then become risk‑based interventions within a six‑step procurement workflow that balances cost, schedule and acceptance certainty.
Buyer context and scope boundary
Audience and scope
- Intended readers: distributors, architects, contractors, developers, solar EPCs and fleet operators buying modular carport systems for commercial or industrial deployment.
- Product family: architectural aluminium carports, commercial solar carports, industrial and fleet vehicle shelters. See Carportiva system range for product variants and modular options: Carportiva system range and all systems.
- Focus: carport container shipping delivery inspection as the primary procurement decision lever — how and when to specify inspections, what evidence to require, and how inspection choices interact with sourcing, cost and factory delivery.
Scope boundaries and exclusions
- This guide addresses procurement and logistics up to and including delivery-to-site acceptance. It does not replace structural design, site-specific foundation design, local permitting or electrical design. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
- It does not prescribe national regulatory approvals or provide legal advice on customs or import law; refer to local authorities and CBP guidance where applicable [4].
Why inspect container deliveries for carports?
- Carport systems are multi‑component assemblies: extrusions, brackets, fasteners, PV mounting rails, cable trays, and pre‑assembled subframes. Errors in fit, finish or missing parts can create cascading project delays and cost.
- Sea freight and container handling expose parts to moisture, corrosion risk (particularly on raw steel interfaces), and mechanical damage. Proper factory packing and container stuffing are measurable mitigations that inspections can confirm.
Core decision principle
A single guiding principle
- Make inspection decisions based on the incremental expected value of reduced delivery failure versus the incremental cost and schedule impact of inspection. That expected value depends on (a) the probability of a delivery or quality failure without inspection, (b) the consequence of such a failure for the project schedule/cost/commissioning, and (c) the reliability of alternative controls (contract terms, packaging, supplier track record).
Translate principle into procurement controls
- If consequence × probability is high and alternative controls (supplier capability, documentation, insurance) are insufficient, require pre‑shipment and container shipping delivery inspection.
- If supplier has robust factory quality documentation, long track record, and you use conservative Incoterms with clear delivery responsibility matrix, the marginal benefit of an inspection may be small — but confirm via a documented risk assessment.
Decision levers (what buyers can vary)
- Inspection scope and timing (component-level checks, sample testing, full container loading supervision).
- Acceptance criteria and nonconformance workflows integrated into contracts.
- Responsibility, cost allocation and authority to reject shipments (aligned with Incoterms) — see the "delivery responsibility matrix" below.
- Use of factory quality documentation, photographic records, and third‑party inspection agencies.
Planning inputs
What you must define before deciding inspection requirements
- Documented project basis
- Clear scope drawings, quantities, site interfaces, foundation positions and allowable tolerances; load cases if structural attachments are required.
- Agreed project schedule and critical paths that quantify the cost of delayed acceptance.
- Explicit warranty expectations and commissioning criteria.
- Commercial terms and Incoterms
- Incoterm selection determines where the transfer of risk and responsibility happens; this materially affects inspection timing and payer for inspection services [3].
- Ensure your delivery responsibility matrix explicitly maps responsibilities for packing, loading, customs, and on‑site unloading.
- Supplier profile and B2B supplier due diligence
- Assess supplier history with similar carport systems (references, visit reports), production capacity, staff qualifications, and corrective action processes.
- Request factory quality documentation as baseline evidence before accepting a reduced inspection regime.
- Logistics chain and transit exposure
- Voyage duration, transshipment points, container handling exposures, and whether specialized export packing is needed for long sea legs.
- Availability of bonded warehouses, ability to hold containers for inspection before customs clearance.
- Technical interfaces and scope boundary
- Define exactly which items are factory‑supplied, which are site‑supplied, and interface tolerances (e.g., bolt patterns, foundation embed positions, cable entry points).
- Insurance and claims process
- Confirm marine cargo insurance policy scope, deductibles and insurer claims process for visible vs concealed damage.
Practical planning outputs as minimum deliverables
- Technical scope comparison table (supplier proposal vs buyer specification).
- Factory documentation packet (material certificates, welding procedure specs, painting/coating certificates).
- Shipping pack list and container stuffing plan.
- Acceptance test and nonconformance procedure documented in purchase order.
Technical specification and interfaces
What to inspect technically, and how it interfaces with site requirements
- Component conformity: extrusions dimensionally match drawings; brackets and rails have specified hole patterns and surface finishes.
- Coating and corrosion protection: aluminium profiles typically anodised or powder coated; any ferrous parts (steel anchors, brackets) require specified galvanizing or coating — confirm against galvanizer guidance and certificate [1].
- Welding and structural joints: factory QA records, weld procedure specifications and representative weld samples (if welds are structural).
- Fasteners and stainless steel grade: verify specified materials and corrosion grades for marine or coastal exposure.
- PV mounting and electrical pre‑fit: rails, clamps and grounding paths often need electrical continuity checks; confirm whether modules are shipped separately and who is responsible for module-to-rail interface.
- Foundation interface and embed plate alignment: provide accurate foundation drawings and tolerances. Misaligned embed plates are a common source of rework.
Technical scope comparison (single-row example to be used in procurement)
- Provide the buyer with a "technical scope comparison" inserter in the RFQ that maps each supplier deliverable to the buyer’s technical requirement. This comparison is the first line of defence and determines what needs inspection.
Inspection detail examples
- Dimensional check: sample 10% extrusions for critical dimensions and profile integrity.
- Surface finish: roughness, coating thickness readings (e.g., dry film thickness for powder coat).
- Packing and marking: verify packing lists, manufacturer markings, and container segregation.
- Load tests / witness tests: where applicable, witness a cut‑out tensile/weld test in the factory under agreed witnessing protocols.
Standards and traceability
- Ask suppliers to reference applicable ISO quality management elements (e.g., ISO 9001 quality processes) for process assurance, while recognising certification alone does not replace physical inspection [2].
- Request material traceability and mill certificates for steel elements; request batch/coil numbers for aluminium extrusions.
Procurement and factory evidence
What procurement should demand as minimum factory evidence
- Factory Quality Documentation checklist (table below): material certificates, process POs, welding procedure specifications, coating certificates, inspection test plans, packing lists and photos.
- Request a factory inspection schedule and evidence of internal audit results, nonconformance logs and corrective action records.
Factory evidence decision table
| Document / Evidence | Purpose | Minimum buyer expectation |
|---|---|---|
| Material certificates (mill test certs) | Verify base material meets spec | Batch traceability for structural parts |
| Welding Procedure Spec & WPS records | Confirm welding quality control | WPS and competent welder records for structural welds |
| Surface treatment certificates (galvanizing/paint) | Corrosion protection verification | Coating method, thickness range, and lot report [1] |
| Dimensional drawings and shop drawings | Fit and interfaces verification | As‑built shop drawings signed off before production |
| Packing list and container stuffing plan | Logistics, handling and claims | Itemised pack list + photos of stuffing plan |
| Internal inspection test records | Factory check evidence | IPT records showing acceptance sign-off |
| Photographic evidence of production/packing | Visual confirmation | High-resolution photos of components and packing |
| Third‑party inspection report (if used) | Independent check | Inspector report with scope and sample sizes |
How to use factory evidence
- Make certain documentation preconditions for shipment release: e.g., no shipment without delivery of shop drawings and packing list signed by buyer or authorized agent.
- Where acceptable risk is low, use factory evidence to reduce pre-shipment inspection scope (sampling rather than full inspection).
- Where risk is high, require third‑party inspection at final packing and witness container stuffing.
Pre-shipment vs. pre-loading inspection
- Pre‑shipment inspection (PSI) inspects goods in their packed state but before being moved to port. It is useful to confirm quantities, packing and visible conformity.
- Pre‑loading/container stuffing supervision is specifically designed to capture packing and lashing adequacy, segregation, blocking and bracing inside the container. For container shipping delivery inspection, supervised stuffing can materially reduce claims for damage in transit.
Role of third‑party inspectors
- Use independent inspection bodies with experience in solar carport or modular metal structures. Their scope should be strictly defined (sampling plan, pass/fail criteria, reporting format).
- Third‑party inspection reports are evidence; they are not a substitute for contractual acceptance clauses that define remedies for nonconforming deliveries.
Legal and customs implications
- Align inspection timing and documentation with customs and import procedures. Delayed or missing documentation can create demurrage and handling costs; ensure the shipping documents and inspection reports are issued in time for customs clearance [4].
Export packing coordination and delivery responsibility matrix
Export packing matters
- For modular carport systems, export packing must protect profile corners, painted surfaces and pre‑assembled subframes. Packing should be resilient to container stack loads, humidity and condensation.
- Consider desiccants, sealed lashing, and protective timber crating for fragile or high‑value subassemblies.
Export packing coordination
- Coordinate packing specs between buyer, supplier and freight forwarder:
- Define required packing standard and materials (e.g., film, corrosion inhibitor, blocking).
- Confirm stacking and loading patterns for container loads, and whether palletised vs skid packing is used.
- Include photos of packing and container stuffing as contractual deliverables.
Delivery responsibility matrix (decision table referencing Incoterms)
- The delivery responsibility matrix clarifies who pays, arranges and is responsible for inspection, packing and customs.
| Incoterm | Seller responsibilities (packing, loading, export) | Buyer responsibilities (unloading, import, inland) | Inspection leverage (who arranges/pays) |
|---|---|---|---|
| EXW (Ex Works) | Minimal — seller makes goods available at factory | Buyer arranges pickup, export, customs, and inland | Buyer arranges/controls inspection and pays inspector |
| FOB (Free on Board) | Seller handles export clearance and loading on vessel; packing to get goods to the port | Buyer pays freight and insurance; responsible after loading | Both parties may specify pre-loading inspection; buyer can engage third party to witness stuffing [3] |
| CIF (Cost, Insurance, Freight) | Seller arranges and pays for carriage to destination port and minimum insurance | Buyer handles import clearance and inland | Buyer still should specify pre-shipment inspection; seller arranges carriage but inspection can be at factory (buyer pays) |
| DDP (Delivered Duty Paid) | Seller responsible for full delivery including import and duties | Buyer receives goods at place of destination | Seller more likely to control export packing; buyer should require packing records and may opt for joint inspection |
Notes:
- Incoterms determine transfer of risk and responsibility; always align inspection clauses and payment terms with chosen Incoterm [3].
- For container shipping delivery inspection that includes supervision of stuffing, the buyer should clearly state whether they will fund and direct the inspector, even under CIF/CFR where the seller controls carriage.
Customs and import documentation
- Ensure inspection reports are acceptable to customs authorities (if customs inspection is required) and that documents are timed for clearance to avoid demurrage [4].
- Keep copies of photographic evidence, container stuffing plans and third‑party reports with shipping documentation.
Site installation and operations
Receiving and on‑site acceptance processes
- Reception planning: schedule delivery windows, confirm lifting capacity, laydown area, and protection from exposure.
- Unloading supervision: designate responsible party for unloading, inspect for visible damage, and capture photographic and signed records at time of receipt.
- Short‑term storage: define storage conditions on site to prevent corrosion or damage (e.g., storage off-ground, covered, protected from direct weather).
On‑site inspection checklist
- Container condition: visible breaches, water ingress, rust on container interior.
- Package integrity: wet or damp packaging, torn goods, lost or missing packages.
- Quantity verification: cross-check pack list against delivered SKUs and counts.
- Spot dimension checks on key components to detect obvious mis‑fabrication before installation.
Concealed damage and claims
- Many shipping damages are concealed (not visible until unpacking). Establish a conditional acceptance process:
- Note visible damages on delivery receipt.
- Reserve the right to reject upon discovery of concealed damage within a defined window (document this in the delivery receipt).
- Start claims with carrier/insurer immediately and retain all packaging for inspection.
Interface to installation teams
- Provide installation teams with full documentation: shop drawings, sub-assembly lists, torque and tightening specifications, and jointing sequences.
- If sub-assemblies arrive pre-drilled, confirm that fixings match site embed positions and pre-installed anchors.
Commissioning and warranty handover
- Final commissioning (if relevant for solar carports) requires electrical checks, earthing continuity and module mounting checks; coordinate these activities with installers and electricians who are locally qualified.
Important compliance note
- Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risks and mitigations
Common implementation risks
- Missing or incorrect parts that lead to site delays.
- Damage in transit: crushing, corrosion, water ingress.
- Misalignment between factory assemblies and site foundations.
- Customs holds due to missing documentation.
- Disputes over acceptance and responsibility driven by ambiguous Incoterm clauses.
- Quality deviations (coating failures, incorrect materials).
Risk mitigations
- Combine contractual controls (clear acceptance criteria, remedies), technical controls (shop drawings, marking), and logistical controls (pre‑shipment inspection, supervised stuffing).
- Insist on material certificates and batch traceability for critical steel components.
- Use photographic and video records during factory packing and container stuffing.
- Consider staged deliveries and buffer stocks for critical long‑lead items to reduce schedule sensitivity.
- Specify who will bear costs of inspection and rework in purchase orders.
Insurance and claims mitigation
- Ensure marine cargo insurance covers the full agreed value and includes terms for concealed damage claims.
- Capture condition reports at the port of discharge and organise immediate inspection if damage is suspected.
Decision heuristics
- High consequence + high uncertainty = require supervised container stuffing and PSI.
- Low consequence + low uncertainty + trusted supplier = factory evidence and random sampling may suffice.
Practical examples (generic, non‑project claims)
- For a large multi-site roll‑out where each site downtime costs significant revenue, supervised stuffing plus pre-shipment testing often pays for itself by avoiding a single delayed critical shipment.
- For a one-off small carport replacement, paperwork and photographic packing evidence may be proportionate.
Carportiva Six-Step Container Delivery Inspection Workflow
Name: Six-Step Carportiva Container Delivery Inspection Workflow Purpose: A standardised buyer workflow for deciding and executing carport container shipping delivery inspection activities.
Step 1 — Define the project basis (Scope & risk)
- Produce a documented project basis: drawings, quantities, schedule, warranty expectations and key milestones.
- State who is responsible for foundations, electrical connections and permits.
Step 2 — Perform B2B supplier due diligence
- Evaluate supplier capability, references and capacity.
- Request factory quality documentation and prior project photographs.
- Conduct a technical scope comparison between supplier proposal and buyer specification.
Step 3 — Lock technical scope comparison and acceptance criteria
- Complete a technical scope comparison table that maps deliverables, tolerances and acceptance tests.
- Decide which items require 100% verification vs sample inspection.
Step 4 — Specify factory evidence and inspection strategy
- Decide on factory quality documentation leverage (material certs, WPS, coatings).
- Specify whether to require pre‑shipment inspection, container stuffing supervision, or third‑party testing.
Step 5 — Coordinate export packing and logistics
- Agree packing standards and container stuffing plan.
- Decide who will arrange inspections and who will pay, reflecting the delivery responsibility matrix and Incoterm choice.
Step 6 — Execute delivery inspection and site acceptance
- Conduct agreed inspections (factory/port/site), capture photographic evidence and sign acceptance records.
- Implement nonconformance workflows and claim processes as required.
Workflow governance notes
- Each step should be recorded and versioned in the contract folder. Deviations should be approved by the buyer project manager.
- Where the buyer declines on-site inspection, require compensating controls: additional documentation, higher sampling at factory, hold-back payment, or extended warranty.
Decision tables
Decision Table A — When to require supervised container stuffing or sending an inspector
| Trigger condition | Suggested inspection strategy |
|---|---|
| High value / bespoke components and long lead time | Full pre‑shipment inspection + supervised container stuffing |
| Coastal or high‑corrosion exposure components (steel parts) | Require coating certificates and sample coat thickness checks + packing with desiccants |
| Supplier new to buyer or first production run | On‑site factory inspection + sample dimensional checks |
| Large multi‑site deployment with aggressive schedule | Witness stuffing + retain spare critical components in buffer stock |
| Low value, standardised product from trusted supplier | Rely on factory quality documentation + random PSI sampling |
Decision Table B — Minimum contract clauses to mitigate delivery risk
| Clause | Why it matters | Minimal contract text focus |
|---|---|---|
| Acceptance criteria & sampling plan | Avoid later disputes on acceptance | Define sample sizes, measurement methods, and pass/fail criteria |
| Inspection rights and schedule | Clarify when inspections can occur | Buyer or buyer‑appointed inspector may inspect at factory and at stuffing |
| Packing & marking standard | Prevent transit damage and claims | Specify packing materials, blocking/bracing and photo evidence at stuffing |
| Nonconforming goods & remedies | Remediation path for defects | Define repair/replacement, cost allocation and timeframes |
| Incoterm and delivery responsibility matrix | Who assumes risk and cost at each stage | State chosen Incoterm and map packing, loading, insurance and import duties |
Frequently Asked Questions (FAQ)
Q: When is a pre‑shipment inspection enough and when do I need supervised stuffing? A: Use a structured risk assessment. Pre‑shipment inspection checks quantity and visible conformity and may be enough for trusted suppliers and low consequence deliveries. Supervised stuffing is recommended when the packing method or container load configuration materially affects transit damage risk (e.g., heavy subframes, mixed palletised loads) or when the consequence of damage is high.
Q: Who pays for the inspection? A: That depends on contractual terms and chosen Incoterm. Buyers often pay for inspections when they require the service (e.g., buyer‑appointed inspector under EXW or FOB). Under CIF/CIF-like terms, sellers control carriage but buyers should still specify inspection rights and may elect to pay for third‑party verification. Document payment responsibilities in the purchase order and delivery responsibility matrix.
Q: How do I define acceptance criteria for carport components? A: Acceptance criteria should be measurable: dimensional tolerances in millimetres, coating thickness ranges in microns, torque specifications for mechanical joints, and functional checks (e.g., fitment of PV clamps). Include acceptable deviation ranges and remedial actions in the RFQ and purchase contract.
Q: Can photographic evidence replace an inspector? A: Photographs are useful but limited: they capture visual condition and packing but cannot substitute for dimensional checks, coating thickness measurement or destructive testing. Photographic evidence is best used as complementary evidence in a defined inspection package.
Q: Do Incoterms affect my inspection rights? A: Incoterms define risk transfer and cost allocation, but inspection rights should be contractually defined irrespective of Incoterm. For example, even under CIF the buyer can require PSI and supervised stuffing as a contractual condition for acceptance [3].
Q: What if damage is discovered on site after acceptance? A: If acceptance was unconditional, recovery may be limited; if acceptance was conditional (noting visible damage and retaining rights for concealed damage), open a claim with carrier/insurer, preserve evidence (packaging and goods), and follow contract nonconformance procedures.
Q: Are there standards for packing and corrosion protection to cite? A: Use industry best practices and supplier specifications. For galvanizing and corrosion protection of steel parts, refer to guidance by professional associations such as the American Galvanizers Association [1]. For quality management processes, require alignment to ISO practices where relevant [2].
Conclusion
When deciding whether a carport container shipping delivery inspection is necessary, treat inspection as a risk allocation and risk reduction instrument that must be designed against a documented project basis and the buyer’s tolerance for schedule disruption and rework. Use B2B supplier due diligence, a clear technical scope comparison, specified factory quality documentation and export packing coordination to reduce the need for intrusive inspections where appropriate. Where the expected cost of failure exceeds inspection and logistics costs, require pre‑shipment and supervised stuffing inspections and make these requirements contractual. Always align inspection clauses with the delivery responsibility matrix and chosen Incoterms, and ensure documentation timelines are compatible with customs and insurance processes.
For detailed product options and how inspection strategies integrate with specific system configurations, see all systems and our sourcing guides.
Mid‑article CTA /inquiry · info@carportiva.com
Final note (compliance and professional advice)
- Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
- This guide is intended to inform procurement decisions; use it alongside local legal, structural and regulatory advice.
Closing CTA /inquiry · info@carportiva.com
Footnotes and useful public references
- For galvanizing and corrosion guidance: American Galvanizers Association [1].
- For quality system frameworks: International Organization for Standardization [2].
- For Incoterms and delivery responsibility definitions: International Chamber of Commerce Incoterms [3].
- For customs and import procedural guidance: U.S. Customs and Border Protection [4].
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion