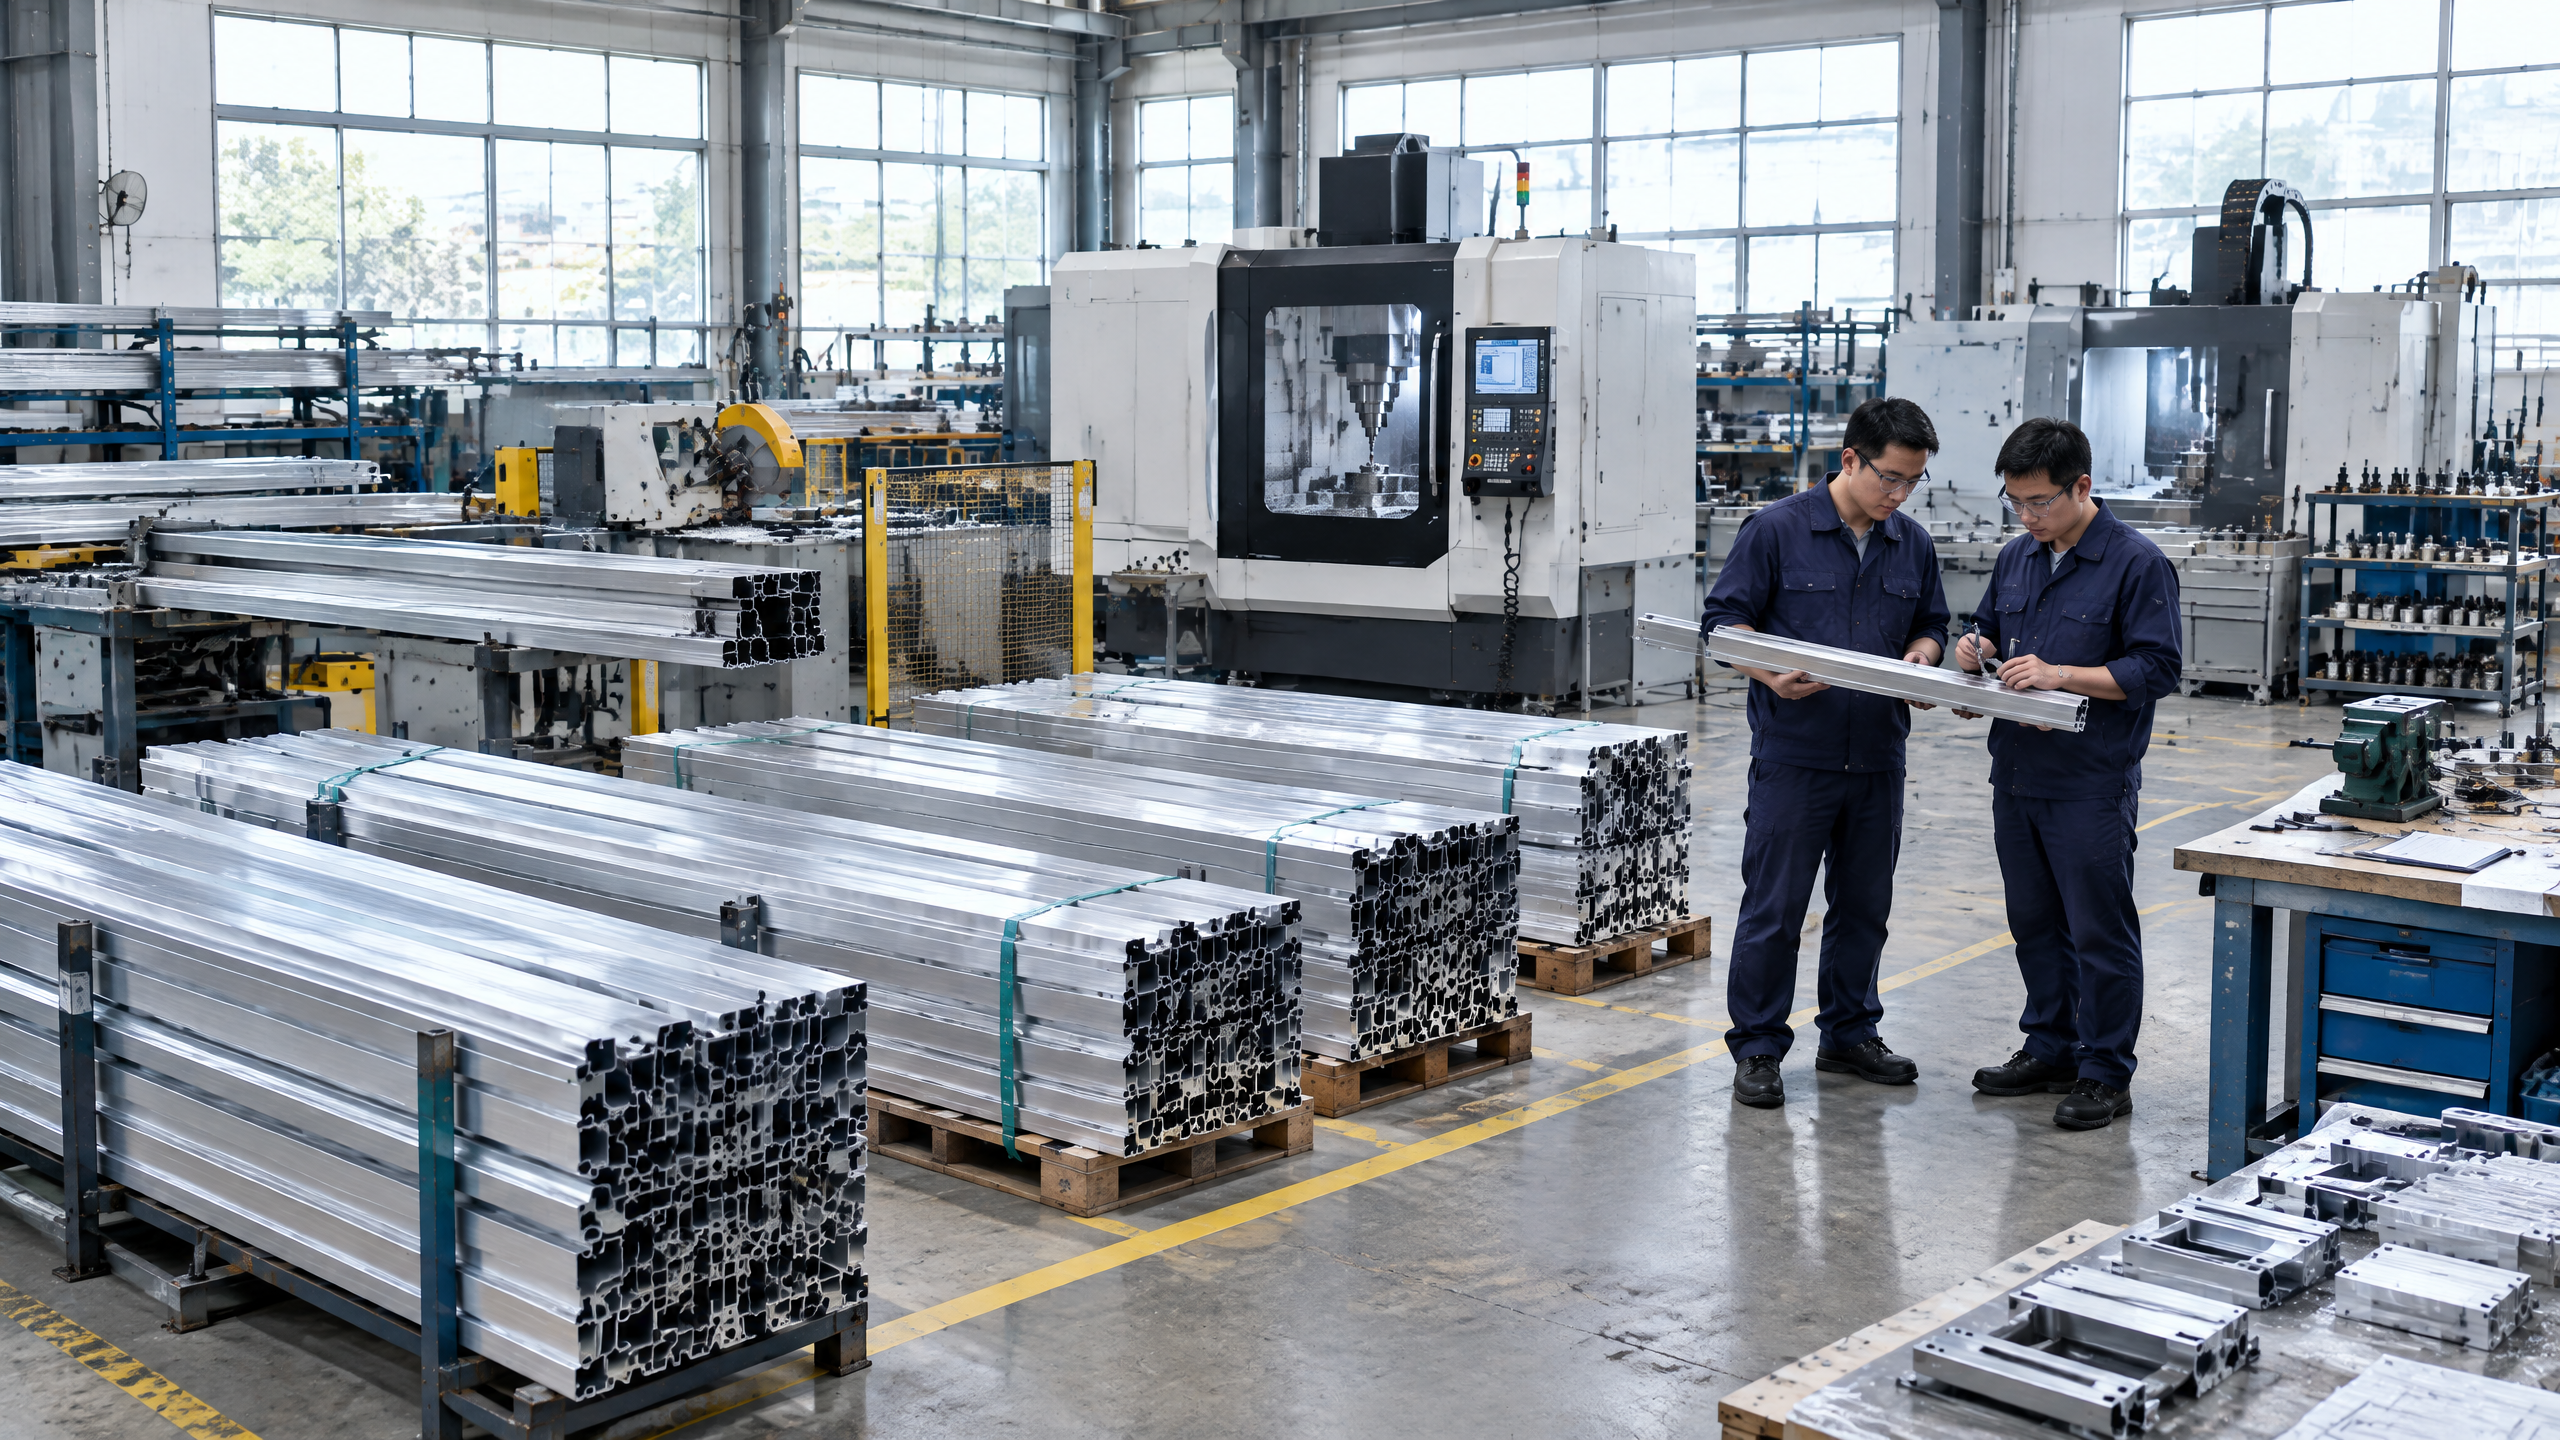
Direct answer (120–180 words)
A targeted carport factory audit quality system should be the single point of evidence that links your project requirements, procurement controls and delivery outcomes. For B2B buyers — distributors, architects, contractors, developers, solar EPCs and fleet operators — the audit quality system must be structured to verify (a) the technical scope comparison between tender documents and factory drawings, (b) factory quality documentation for materials and process controls, (c) export packing coordination for transport resilience, and (d) a clear delivery responsibility matrix aligned to your chosen Incoterms. Use the audit to confirm that contractual tolerances, protective coatings (per galvanizing or aluminium finishing guidance), welding and fastener traceability, and load-path interfaces are captured in the factory’s records. Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty all require a documented project basis and verification by relevant local qualified professionals, installers, utilities and authorities before procurement decisions are final.
Buyer context and scope boundary: why a carport factory audit quality system matters
A carport factory audit quality system is not a one-off checklist; it is a structured assurance process that aligns factory capability with project-specific outcomes. The typical procurement challenge for carport projects lies at the intersection of site constraints, product complexity and third-party integration:
- Architectural aluminium carports require aesthetic finishes, close dimensional tolerances and interface coordination with building facades and drainage.
- Commercial solar carports need mechanical structure and electrical integration for PV modules, inverters, combiner boxes and cable routing.
- Industrial/fleet vehicle shelters emphasize robustness, material durability and repairability under heavy use.
A factory audit should establish the boundary between what the supplier is contractually responsible for and what remains the buyer’s or installer’s responsibility (see delivery responsibility matrix section). It must therefore look beyond catalog claims and confirm the supplier’s ability to deliver to the documented project basis: drawings, structural calculations, finishing spec, electrical interface notes, and logistics constraints.
Key outcomes from a focused audit:
- Confirm technical conformance to the project-specific design intent.
- Validate the supplier’s documentation and process controls.
- Reduce ambiguity in procurement contracts and delivery obligations.
- Provide traceable evidence to support warranty, compliance and acceptance.
Core decision principle: evidence over assumption
The core principle driving every procurement decision should be evidence over assumption. An effective carport factory audit quality system produces auditable records that allow a buyer to answer: does the factory have documented, repeatable capability to meet my project requirements?
Evidence types to prioritise:
- Factory quality documentation (material Certificates of Conformance, weld procedure documents, non-conformance records, inspection/test reports).
- Traceability records for critical components (fasteners, structural members, surface treatments).
- Process flow and inspection checkpoints that map to project milestones.
- Photographic and dimensional records for assembled modules and packed shipments.
- Proof of personnel competency where specialized tasks are required (welding codes, coatings application).
Apply the same rigor to logistics and export controls: shipping plans, export packing coordination and loading trial records can be decisive where damage risk or customs scrutiny is high.
Wherever a capability gap is identified, quantify it in the procurement contract (e.g., additional hold points, third-party inspection, remedial testing) and ensure contractual acceptance by both parties.
Planning inputs: what you must provide and demand from suppliers
A factory audit is most effective when both buyer and supplier work from the same documented project basis. As a buyer you must prepare and communicate the following inputs before arranging an audit:
Mandatory buyer inputs
- Project scope and contract documents (drawings, specifications, structural calculations).
- Technical scope comparison matrix that maps tender items to factory components, responsibilities and acceptance criteria.
- Packaging, transport and site handling constraints (clearance, crane capacity, laydown area).
- Expected interface points (roof penetration locations, electrical entry, foundation bolt patterns).
- Critical lead-time milestones and permitted shipping windows.
Mandatory supplier outputs to request
- Factory layout, production capacity and key process flow diagrams.
- Quality management system description and relevant certifications (e.g., ISO-related practices) [2].
- Factory quality documentation: incoming material inspection records, process control instructions, welding qualification records, surface treatment records, inspection and test plans.
- Sample assembly inspection reports and photographs of representative assemblies.
- Export packing coordination plan and photos of standard package types.
Technical clarity at the planning stage reduces downstream queries and accelerates audit time. Use a technical scope comparison to convert broad specifications into checkpointable factory activities.
Technical specification and interfaces: audit checkpoints
The technical audit should verify that the factory’s production outputs map to the project’s functional and interface requirements. Key domains and typical checkpoint items:
Structural and materials
- Material certificates for aluminium alloys, fasteners and steel where present; ensure batch traceability.
- Weld procedure and welder qualification records where structural welding is used.
- Dimensional control processes for frame squareness, bolt hole alignment and module interfaces.
- Structural members’ corrosion protection strategy (aluminium finish, anodizing, paint systems, galvanizing for steel components) — verify coating thickness records and qualification of applicators. For galvanizing and related guidance consult the American Galvanizers Association [1].
Surface finishing and aesthetics
- Sample panels showing finish uniformity, edge protection and post-fabrication touch-up procedures.
- Process control for anodizing, powder coat or liquid paint; inspection checkpoints for adhesion and appearance.
- Handling and storage protocols to prevent surface damage during transport and on-site storage.
Mechanical interfaces and fasteners
- Bolt grades and supplier traceability; tensioning/tightening procedures; torque specifications.
- Accessory mounting details (signage, lighting) and pre-drilled or slotted patterns.
- Assembled module checks: fit, clearances, and attachment feasibility under standard site lifting methods.
Electrical and solar integration (where applicable)
- Module racking interface drawings and module layout templates.
- Cable tray and junction box mounting details that show electrical entry/exit locations; clearance for conduit and cable bend radii.
- Grounding and bonding points, and evidence of electrical interface coordination with the client’s electrical designer or EPC scope.
Packaging and transport
- Export packing coordination: padded supports, timber framing, internal bracing for cross-country movements, weatherproofing, and unitized container packing plans.
- Lashing points and handling instructions to avoid unintended stresses.
Dimensional and tolerance check
- Go/no-go dimensional sample reports for critical bolt patterns and baseplate dimensions.
- Template validation for site anchor locations.
Every checkpoint should be linked to an acceptance criterion (measurement tolerance, sample size, inspection method) to avoid subjective pass/fail decisions.
Procurement and factory evidence: what to collect and how to validate it
A robust carport factory audit quality system yields both documents and demonstrable outputs. Structure the evidence into discrete categories and require a minimum acceptable deliverable against each.
Recommended evidence pack (minimum)
- Quality management overview and process flow (documented).
- Factory quality documentation:
- Incoming inspection records.
- Process control instructions (work instructions).
- In-process inspection checklists.
- Final inspection reports with measured values.
- Non-conformance records and corrective action logs.
- Material traceability:
- Certificates of Conformance for aluminium extrusions, fasteners and steel parts.
- Batch/heat numbers linked to assembly records.
- Welding and assembly qualifications:
- Weld procedure specifications and welder qualification IDs.
- Surface treatment records:
- Coating specification sheets and historical thickness test records.
- Packing and shipping records:
- Export packing coordination plans, palletization drawings, and photos of typical packed units.
- Photographic evidence of sample assemblies and pre-shipment units.
- Factory test records (e.g., dimensional surveys, load test reports if specified in the contract).
How to validate documents effectively
- Cross-reference drawing revision numbers with the factory assembly records.
- Use witness points where critical; require photos, time-stamped where possible, and third-party inspection for critical items.
- Spot-check material certificates with supplier references and, where necessary, request mill test reports.
- Confirm non-conformance closure with documented root cause analysis and verification steps.
- Use the technical scope comparison to ensure each contractual requirement has a corresponding piece of evidence.
Decision table — audit evidence mapped to buyer risk profile
| Buyer risk profile | Minimum factory evidence required | Recommended additional measures |
|---|---|---|
| Low-risk (standard-site, non-electrified carports) | Material CoC, final inspection photos, packing photos | Random third-party inspect pre-shipment |
| Medium-risk (electrified/commercial projects) | Full factory quality documentation, welding and coating records, assembly photos | Third-party witnessed assembly, FAT for modules |
| High-risk (solar PV & integration, critical infrastructure) | Complete evidence pack plus traceability logs and load test records | Third-party FAT, on-site hold points, extended warranty terms |
Decision table — delivery responsibility matrix (example)
| Activity | Supplier responsibility (typical EXW/FOB) | Buyer responsibility (typical EXW/FOB) |
|---|---|---|
| Packaging for export | Provide export packing coordination plan and standard packing | Confirm special packing or handling on inquiry |
| Loading onto vessel | Load to seller’s terminal (FOB) | Arrange main carriage and insurance (FOB) |
| Customs export | Provide export documentation per export rules | Pay duties and handle import clearance (buyer) |
| Inland delivery to site | Deliver to port/terminal | Arrange inland transport and site offload |
For legal clarity, align the delivery responsibility matrix with the chosen Incoterms and document these in procurement contracts [3].
Caveat: Incoterms and customs/import obligations vary by route and destination; consult your customs broker and the local authorities and follow import guidance [4].
Site installation and operations: what the factory audit must inform on
An audit should not end at factory doors. It must produce outputs that enable predictable site installation and long-term operations.
Essential outputs for installation
- Installation drawings with clear anchor bolt patterns, tolerances and orientation marks.
- Lifting and handling instructions per unit (weight, center of gravity, sling points).
- Pack-to-install mapping: which packed units assemble into which site structures.
- Site acceptance checklists matching factory inspection points.
- Pre-assembly requirements or on-site welding/bolting instructions where applicable.
- Spare parts list and recommended spares to be supplied with the shipment.
Operational readiness and handover
- Maintenance schedule and recommended inspection intervals.
- Coating repair procedures and acceptable touch-up materials.
- Warranty scope and process for claim handling (documented).
- If the system integrates PV, provide O&M points for electrical components and interface documents for the EPC.
Note: Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities to accept and sign off. The factory audit should flag any areas where factory output expects on-site verification or specialist installation steps.
Implementation risks and mitigation: what audits must highlight
Procurement and implementation risks can be grouped into technical, logistical and contractual categories. Use the audit to pre-identify risks and decide mitigations.
Technical risks
- Mismatched tolerances between factory drilling and site anchor cast-in items.
Mitigation: require template checks and 1:1 trial assembly reports; include hold points for anchor installation verification.
- Inadequate coating/durability for local environment (marine/industrial).
Mitigation: demand coating specification and thickness test results; add field touch-up procedures and spare parts.
- Incomplete electrical interface information for solar carports.
Mitigation: require electrical interface drawing and on-site coordination clause with EPC.
Logistical risks
- Damage during transport due to insufficient export packing.
Mitigation: require export packing coordination photos and strong packing specification with shock/strain limits.
- Delays from customs or missing documents.
Mitigation: confirm export/import document list in advance and align with customs broker; use Incoterm-clarified delivery responsibility matrix [3][4].
Contractual and schedule risks
- Lead-time slippage due to capacity or material shortages.
Mitigation: audit production capacity, critical-path activities and ask for confirmed production slot bookings.
- Ambiguous acceptance criteria.
Mitigation: convert acceptance to measurable criteria in the technical scope comparison and contract.
Insurance and liability
- Ensure clarity of risk transfer at each shipment stage using Incoterms; where value or risk is high, consider third-party inspection at handover points [3].
Risk register template (short)
- Risk ID; Description; Likelihood; Impact; Mitigation; Owner; Verification point.
Document and close risks with specific contractual remedies (e.g., price hold, delay penalties, rework obligations) only after consultation with legal and procurement teams.
Project procurement controls: audit-integrated controls to include in contracts
Project procurement controls are the contractual mechanisms that ensure the factory audit translates into enforced performance. Embed these controls in the contract and purchase order.
Essential procurement controls
- Technical scope comparison annex: map each contract requirement to factory deliverable and inspection/acceptance criteria.
- Hold points and witness points: define where work cannot proceed without buyer or third-party approval.
- Pre-shipment inspection clause: permit buyer or third-party access for final inspection, with defined scope.
- Non-conformance process and rectification timelines: define acceptable remedial actions.
- Packing and transit risk requirements: define export packing coordination deliverables and damage thresholds.
- Delivery responsibility matrix: specify risk transfer border per Incoterms and list responsibilities for export/import tasks.
- Documented lead-time confirmations and milestone penalties or remedies if applicable.
- Spare parts and documentation delivery timelines: require delivery of operation and maintenance manuals and spare parts lists with the initial shipment.
Linking procurement controls to audit outputs
- Each procurement control must reference corresponding factory quality documentation.
- Use contractual obligations to force corrective action plans when audits reveal systemic issues.
Project procurement controls should be practical and measurable; avoid vague stipulations that are difficult to verify on-site or in the factory.
Six-step buyer workflow: Carportiva audit-ready procurement pathway
A named six-step workflow that B2B buyers can adopt to integrate a carport factory audit quality system into their procurement processes.
- Define documented project basis
- Compile drawings, loads, electrical interfaces, site constraints and acceptance criteria. Prepare the technical scope comparison to translate requirements into factory checkpoints.
- Pre-qualification and supplier due diligence
- Conduct B2B supplier due diligence including financial, legal, and capability checks. Request a preliminary factory evidence pack.
- Audit scoping and checklist development
- Create a tailored factory audit checklist based on the technical scope comparison, risk profile and procurement controls. Include export packing coordination and packing photos as mandatory checkpoints.
- Factory audit execution
- Execute the audit (buyer, buyer’s agent or third-party). Verify factory quality documentation, process controls, sample assemblies and pre-shipment packing. Produce an audit report with non-conformances and required corrective actions.
- Contract alignment and hold points
- Update the purchase order and contract to reflect audit findings: hold points, pre-shipment inspection, spare parts, delivery responsibility matrix and penalty/remedy clauses.
- Pre-shipment verification and handover
- Validate corrective actions, confirm packing and logistics plans, perform final inspection and handover per agreed Incoterms. Record photographic and dimensional evidence for acceptance and future warranty claims.
This workflow is iterative: for repeat projects or series production, lessons learned should update the checklist and supplier assessment criteria.
FAQ — practical answers for common procurement questions
Q: How often should I audit a carport factory? A: Frequency depends on risk and volume. Single pilot projects or high-risk integrations (PV, custom finishes) favour 100% audit coverage for the first shipment and periodic audits thereafter. For repeat production, schedule audits at defined production milestones or annually, depending on supplier performance.
Q: Can a factory audit replace third-party inspection? A: No. A buyer-led audit and third-party inspection serve different purposes. The audit checks systems and capability; a third-party inspection provides independent pre-shipment verification. Use both where risk or contract value justifies independent validation.
Q: What is the minimum factory quality documentation required for a solar carport? A: At minimum, provide: material CoCs, assembly and welding records, electrical interface drawings, coating records, packing plans, and final inspection reports. For electrical integration, include module and racking interface templates and cable routing drawings.
Q: How should I handle differences between factory drawings and my structural engineer’s anchor plan? A: Capture differences in the technical scope comparison. Require the factory to produce as-built survey templates and coordinate anchor bolt templates with the project’s structural engineer. Include a hold point for anchor verification on-site.
Q: Are sample assemblies necessary? A: Yes. Sample assemblies validate fit, finish and assembly procedure. Photos, dimensional checks and, where relevant, load tests should be documented.
Q: What if the factory cannot meet the tendered finishing spec? A: Treat it as a non-conformance. Require corrective action or define acceptable alternatives in the contract with documented visual and performance acceptance criteria.
Q: How do Incoterms affect responsibility for damage in transit? A: Incoterms determine when risk transfers from seller to buyer. Always specify the Incoterm in the contract and reflect it in the delivery responsibility matrix. For more on Incoterms, refer to ICC guidance [3].
Q: What role does export packing coordination play in audit outcomes? A: It is critical. Poor packing is a leading cause of damage. Ensure the factory provides documented packing methods, photos and loading plans; include these as mandatories in pre-shipment checks.
Two decision tables for procurement choices
Table 1 — Choosing audit intensity by project type
| Project type | Audit intensity | Rationale |
|---|---|---|
| Small aesthetic carport (single site) | Low-moderate: document review + sample assembly photos | Lower technical integration; focus on finish and fit |
| Large commercial carport (multi-site, non-PV) | Moderate: factory visit + pre-shipment inspection | Scale increases logistics risk and consistency requirements |
| Solar carport (PV integrated) | High: full audit + FAT + third-party inspection | Electrical safety, PV mounting, and interface complexity demand high assurance |
| Industrial/fleet shelters (heavy use) | Moderate-high: structural verification + material traceability | Durability and heavy-use scenarios require material traceability and assembly robustness |
Table 2 — Packing and shipping decision guidance
| Transport mode | Minimum packing features | Audit checkpoints |
|---|---|---|
| Container export | Unitized crating, internal bracing, moisture barriers | Photos of packed units, lashing plans, container fill diagrams |
| RoRo / breakbulk | Structural supports, weatherproof covers, lifting points | Lashing point checks, handling instructions, weight distribution plan |
| Palletized inland | Protective wrapping, edge protection, strapped pallets | Packing list alignment, palletization photos, de-stacking plan |
Mid-article call-to-action
For a project-specific audit scope and checklist tailored to your Carportiva product selection, start an inquiry: /inquiry
If you are evaluating system options, review the Carportiva system range and compare all systems or consult our sourcing guides.
Practical checklists and templates to include in procurement documentation
Checklist: Pre-audit supplier pack request
- Company capability statement and factory layout.
- Description of quality management system and responsible quality manager.
- List of recent comparable projects (references; do not request confidential data).
- Key process documents: welding procedures, coating specs, inspection plans.
- Standard export packing coordination plans and photos.
Checklist: On-site audit focal points
- Production capacity vs. planned order volume and schedule.
- Process control points and in-process inspection frequency.
- Material handling, storage and segregation measures.
- Environmental controls for coatings and sensitive components.
- Training and certification records for key operators.
Template: Non-conformance report minimum fields
- NCR ID, date, description of non-conformance.
- Affected assemblies/parts (by part ID or batch).
- Root cause analysis.
- Corrective action plan with owners and dates.
- Verification of corrective action and closure evidence.
Procurement negotiation and change control
Use the audit outputs to inform negotiation, not to reopen the entire commercial deal. Typical remediation-based negotiation levers:
- Agree on a corrective action plan with deadlines rather than price reductions.
- Convert identified additional scope (e.g., extra packing) into priced contract change orders.
- For high-value or high-risk gaps, negotiate third-party inspection paid by the seller or shared cost model.
Change control process essentials
- Any deviation from the documented project basis must be issued as a change request with technical approval.
- Establish approval authority levels; minor fit adjustments can be managed by buyer’s project manager, major technical changes by the design/engineering lead.
- Maintain a traceable revision log for drawings and specifications used in production.
Audit reporting and acceptance: structuring your final report
A final audit report should be concise, evidence-led and actionable. Include:
- Executive summary with overall conclusion (pass/conditional/fail) and key risks.
- Mapping to technical scope comparison and contractual checkpoints.
- Photographic library with captions (linked to specific items).
- List of non-conformances, severity classification, corrective action required and due dates.
- Document list of all factory quality documentation reviewed and their revision status.
- Recommendations for contract amendments, hold points or third-party tests.
Acceptance criteria
- Close all critical non-conformances before production release or require third-party verification.
- Accept minor non-conformances as long as they have documented action plans and verifiable closure.
Integrating audit records into project close-out and warranty claims
Maintain audit documents as part of the project’s technical records. Benefits:
- Supports claims under warranty by demonstrating initial condition and agreed acceptance.
- Provides traceability for repairs or retrofits.
- Informs future procurement and supplier selection.
Store documents in a secure, searchable format and ensure parties agree on retention period during contract formation.
Conclusion: treat the carport factory audit quality system as procurement infrastructure
A carport factory audit quality system becomes procurement infrastructure when it is routinised: integrated into your sourcing, contract templates and project controls. It bridges the gap between design intent and delivered assemblies by converting expectations into verifiable evidence. Use the technical scope comparison and factory quality documentation as contract annexes, require export packing coordination plans, and define a clear delivery responsibility matrix aligned with your chosen Incoterms. For complex solar or integrated projects, combine factory audits with third-party inspections and FATs. Always remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and verification by relevant local qualified professionals, installers, utilities and authorities.
For procurement support, document review or to discuss how Carportiva aligns audit checkpoints with your project delivery, contact: info@carportiva.com
Further reading and standards
- Consider quality system alignment with ISO fundamentals where applicable [2].
- For galvanizing and corrosion-protection guidance, see the American Galvanizers Association [1].
- Use ICC Incoterms for clarity on delivery obligations and risk transfer [3].
- Consult local customs guidance for import/export documentation [4].
For product options, see the Carportiva system range and our broader materials at sourcing guides.
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion