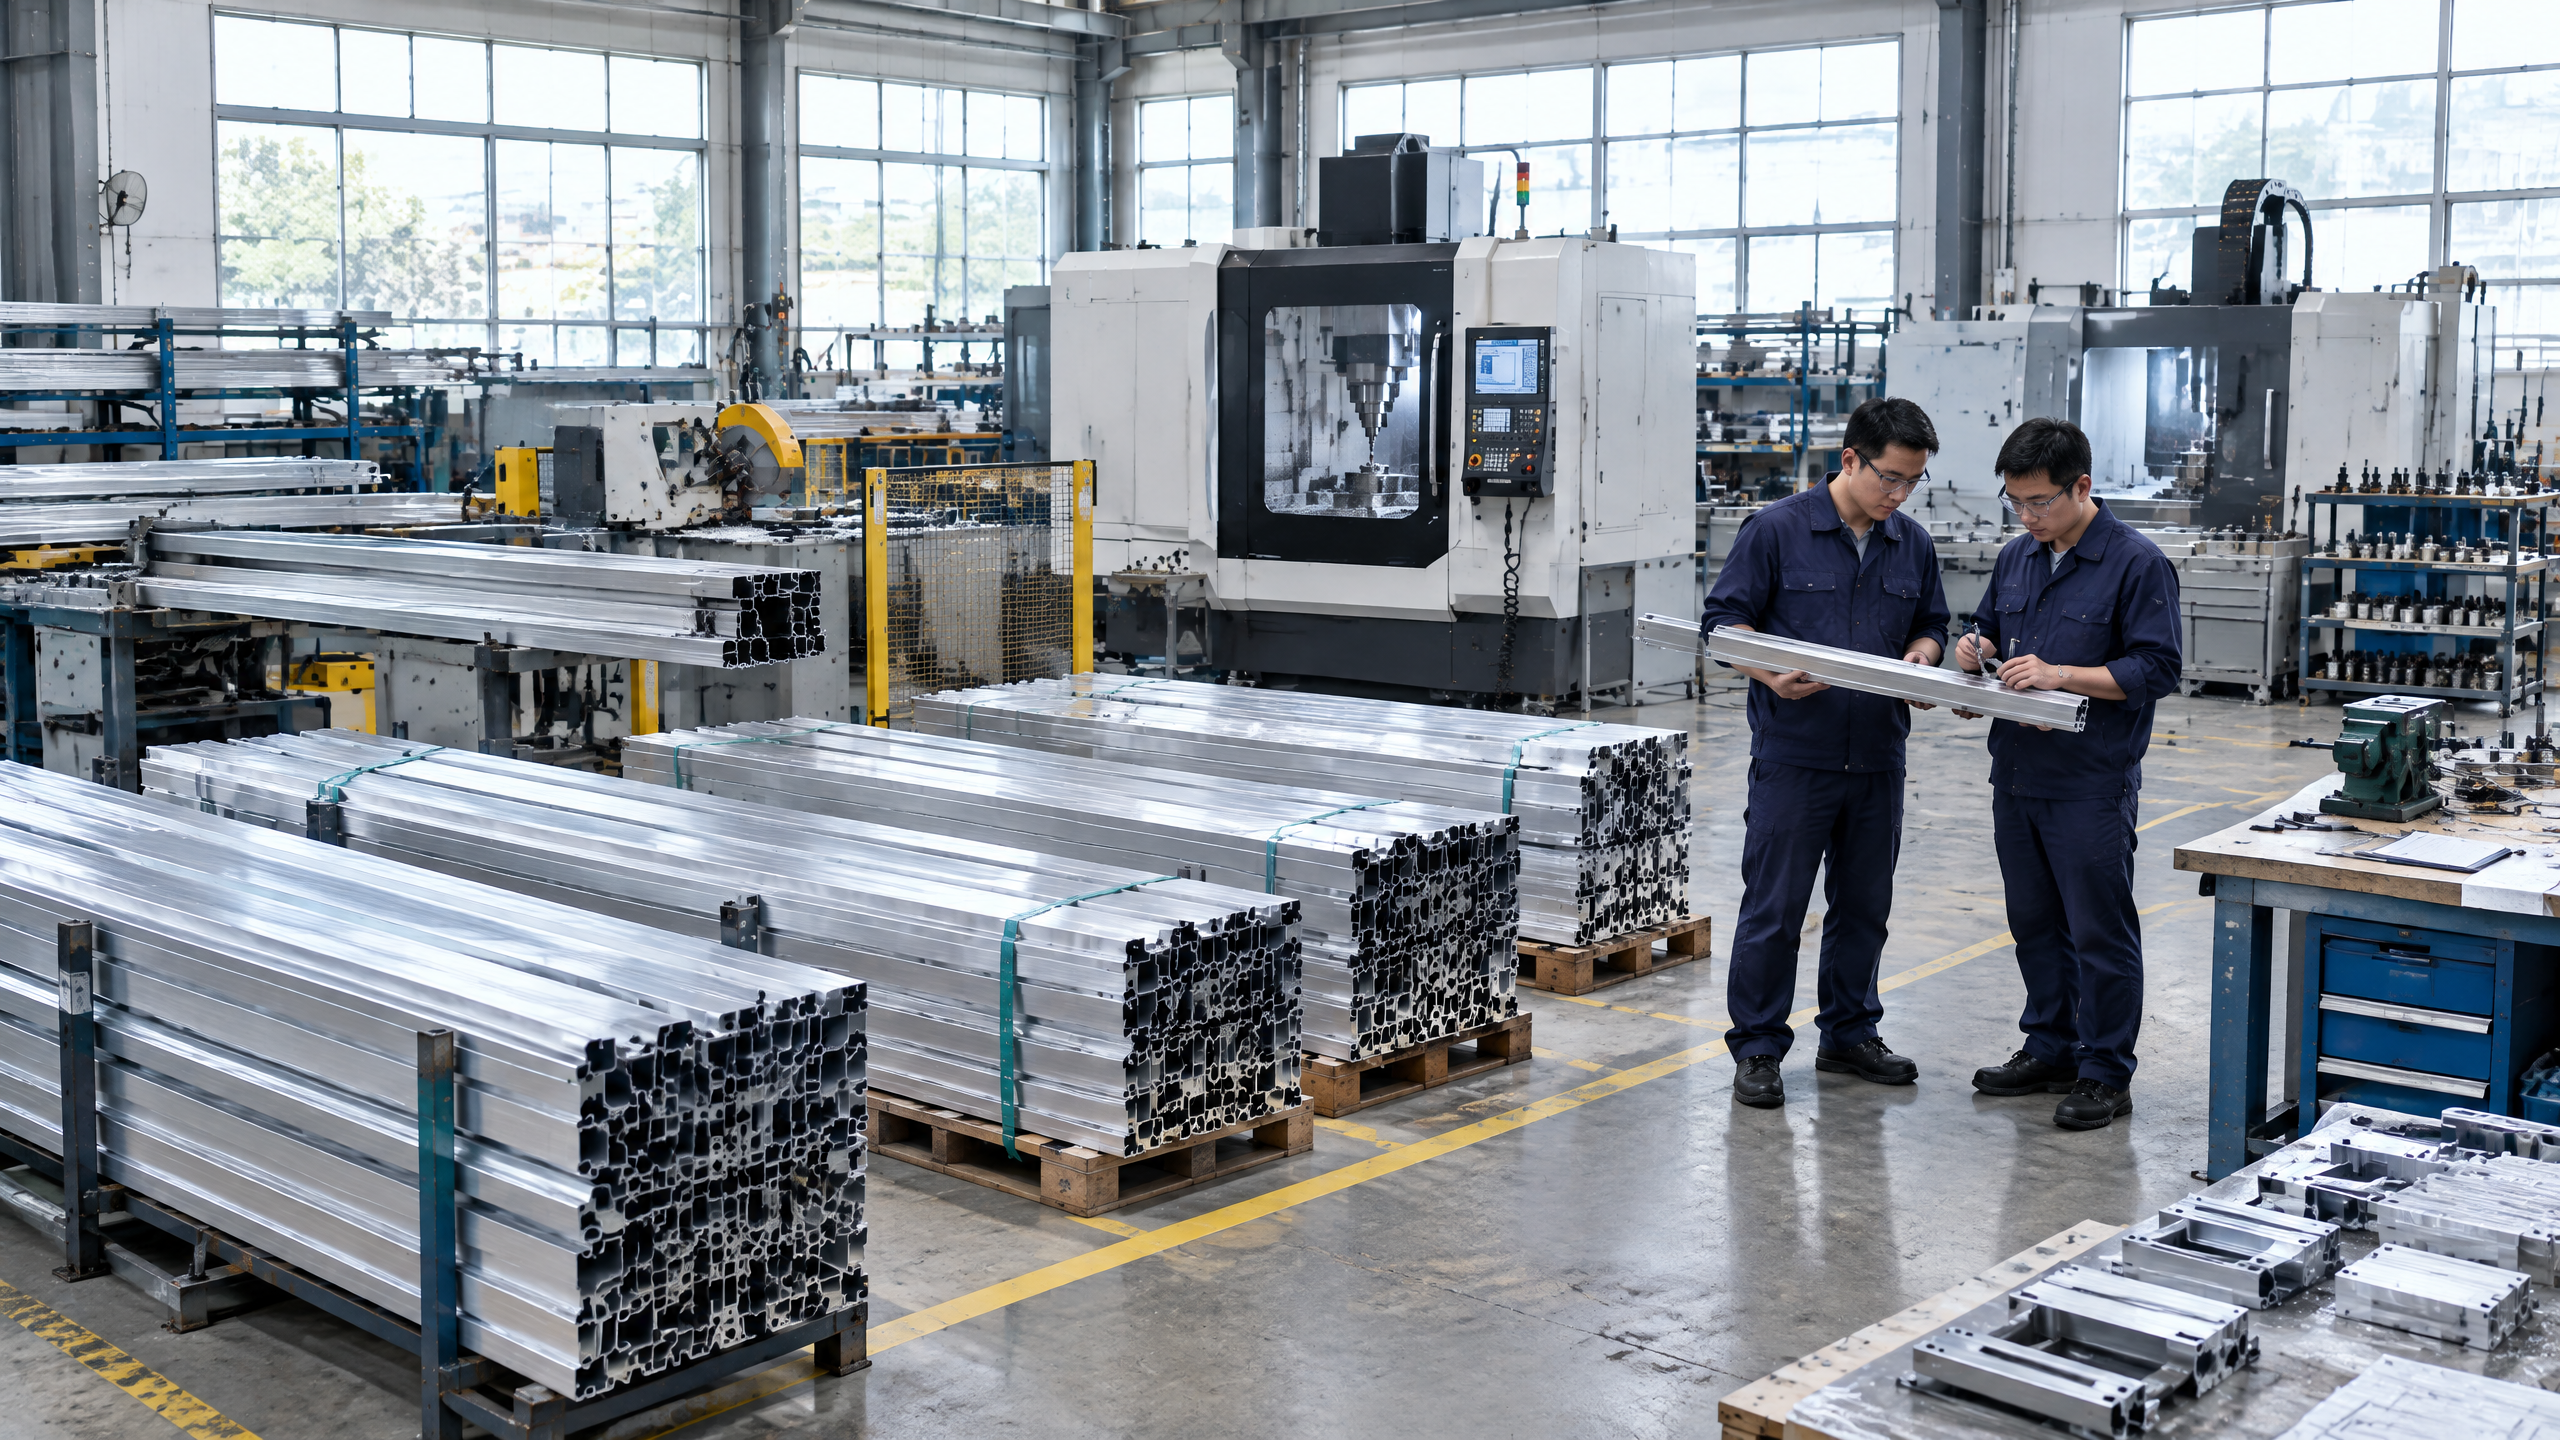
Answer (120–180 words) Effective evaluation of carport quality control fabrication checks requires a structured, project-led approach that converts technical acceptance criteria into verifiable factory evidence and procurement controls. Start by defining a technical scope comparison that captures materials, dimensional tolerances, surface treatments, welds, fasteners, and interfaces (foundations, anchors, electrical). Use B2B supplier due diligence to verify factory capability, quality systems, and previous work; require factory quality documentation and agreed hold points for witness inspections. Clarify logistics early with an export packing coordination plan and a delivery responsibility matrix using established Incoterms. Integrate these outputs into project procurement controls: purchase orders with hold points, inspection plans, and documented acceptance criteria. Finally, require on-site verification and documented handover. Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and review by relevant local qualified professionals, installers, utilities and authorities.
Buyer context and scope boundary: why fabrication checks matter for carports
Carport fabrication is the conversion of architectural and structural design into assembled, transportable components. For aluminium carports, commercial solar carports and fleet shelters the fabrication phase determines long-term performance across corrosion resistance, structural capacity, dimensional fit, and interface reliability with foundations and electrical systems.
Key reasons fabrication checks matter:
- Fabrication defects propagate: misplaced bolt holes, incorrect member lengths, or improper welds compromise on-site fit and safety.
- Coating failures and corrosion accelerate lifecycle costs; appropriate surface treatment evidence reduces risk [1].
- Solar carports add electrical and PV interface risks; precision in module rails, cable routes and grounding is essential.
- Global deliveries introduce handling and customs exposure; packaging choices influence arrival condition and installation efficiency.
Define scope boundaries at the start: what the supplier provides (components, bolting kits, PV substructure), who is responsible for site works (foundations, electrical interconnection), and which items require third-party verification. Use this boundary to create the procurement and inspection plan.
Core decision principle: verifiable acceptance criteria over vendor claims
The core decision principle is simple: accept objective, verifiable evidence tied to stated acceptance criteria rather than relying on supplier assertions. Translate design tolerances and performance expectations into measurable checkpoints that can be observed in the factory, on shipment and at site handover.
Examples of verifiable checkpoints:
- Material certificates traceable to mill batch and standard.
- Dimensional inspection reports with measured deviations vs. drawing tolerances.
- Coating system datasheets and independent test reports (salt spray or adhesion) where applicable.
- Welding records and operator qualifications where welding affects structural continuity.
- Packing lists and export-ready photos showing protective packing for long sea voyages.
This principle reduces ambiguity and enables consistent decision-making across bidders and projects.
Planning inputs: what you must define before requesting fabrication checks
Before you request factory inspections, define the project inputs that set the acceptance criteria and inspection logistics.
Minimum required planning inputs:
- Project basis: scope drawings, loads and environmental conditions, electrical single-line diagrams (if PV), and local code references. These form the documented project basis necessary for structural and electrical design decisions.
- Acceptance criteria matrix: tolerances, surface finish standards, coating system performance, and critical weld sizes/locations.
- Delivery constraints: preferred Incoterm, delivery windows, and site receiving capabilities.
- Inspection plan: hold points (e.g., material receipt, pre-assembly, post-coating, packing), required witness rules, required test types.
- Documentation schedule: which factory quality documentation will accompany shipments (mill certificates, inspection reports, packing lists).
- Personnel: who will witness remote/onsite checks and who will approve releases.
Note: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Technical specification and interfaces: measurable checks you should require
Break the technical scope into discrete items with measurable acceptance criteria. The list below can be used to build inspection checklists and acceptance templates.
Primary technical areas and suggested checks:
- Materials
- Require mill test certificates or material traceability for aluminium alloys, stainless fasteners, and steel (if any).
- Verify material grades match the contract drawings and design statutes.
- Dimensions & tolerances
- Dimensional reports for critical members (lengths, hole centers, squareness) with measured deviation and ID of measurement method.
- Jigs/fixtures used for assembly should be documented.
- Welds & mechanical connections
- Welding procedure specifications and operator qualifications where applicable.
- Visual weld acceptance criteria and non-destructive test (NDT) requests if structural continuity is critical.
- Surface treatment
- Powder coat or anodizing specifications and process control data.
- Salt-spray or adhesion test methods referenced in specifications; request recent test reports from the coating supplier (do not assume pass).
- For hot-dip galvanizing on mixed-metal areas, request certificate and process controls [1].
- Fasteners & consumables
- Supplier traceability for high-strength bolts, torque specs and inspection of torque assemblies.
- PV & electrical interfaces (if applicable)
- Mounting rail straightness, clamp positions and earthing continuity checks.
- Cable tray routing, grommets, and conduit penetrations should be checked against electrical drawings.
- Paint, labelling and documentation
- Part and kit labelling for site ease of assembly.
- Packing lists and BOM to match the physical shipment.
- Packaging & handling
- Export packing coordination to demonstrate that the load is protected for sea transport, handling, and local unloading.
In each case, request explicit acceptance criteria and the measurement method (calipers, laser measure, torque wrench, NDT method, salt spray hours).
Procurement & factory evidence: what documents and audits reduce risk
B2B procurement must demand documentary evidence and factory checks that convert the acceptance criteria into verifiable records. This is where B2B supplier due diligence and factory quality documentation interplay.
Requested factory evidence (minimum):
- Quality management evidence: ISO system registration or equivalent process documentation with scope statements; reference to ISO standards where relevant [2].
- Factory capability: photos of production lines, welding bays, coating booths, and sample production run capacity.
- Material certificates: mill test reports, batch numbers, and traceability logs.
- Inspection and test reports: dimensional checklists, coating thickness readings, salt spray test reports (if required), welding records and NDT reports.
- Production routing: step-by-step process control documents showing hold points and inspections.
- Final inspection sign-off: completed checklists with signatures of responsible quality personnel.
- Packing and shipment records: packing list, crate tagging, export packing photos and strength notes.
- Third-party or buyer-witness evidence: inspector reports, video records, or authenticated photos taken at hold points.
B2B supplier due diligence should include:
- Financial and legal background checks.
- Reference checks on comparable projects and client contact verification.
- On-site or remote factory audit focusing on capacity, process control, workforce skill levels, and calibration systems.
- Review of past non-conformities and corrective action history.
Do not accept unverified claims. Where possible, arrange qualified third-party inspections or buyer witness. Use the inspection outputs to drive contractual acceptance and payment milestones.
Decision table 1 — Fabrication checkpoints vs. acceptable evidence
| Fabrication checkpoint | Acceptable factory evidence | Recommended inspection method |
|---|---|---|
| Material grade for beams/rails | Mill test certificates with batch number | Document review + sample material ID |
| Dimensional tolerances (holes, lengths) | Dimensional inspection report + jig/template records | Full measurement checklist; buyer witness optional |
| Weld integrity on primary members | Welding procedure spec + WPS sign-off + NDT report | Visual + NDT where critical |
| Surface coating (powder/ anodize) | Coating datasheet + thickness readings + process log | Thickness gauge readings; sample adhesion test |
| Fasteners & torque assemblies | Traceability certificate + torque logs | Audit records + torque spot checks |
| Packing for export | Packing list + photos + securing list | Review + load-securing check at dispatch |
Logistics, export packing coordination and delivery responsibility
Coordinating packing and delivery requires alignment between procurement, logistics and project receiving teams. Two areas are essential: export packing coordination and a clear delivery responsibility matrix.
Export packing coordination considerations:
- Ensure packaging design protects against common sea transport risks: corrosion from condensation, impact damage, crushing.
- Request packaging material specs (treated timber, corrosion inhibitors, desiccants) and photographic evidence of packing assembly.
- Ensure crates/kits are labelled with part IDs, orientation and handling instructions.
- Confirm freight unit dimensions and weight for road/port handling constraints.
Delivery responsibility matrix Create a delivery responsibility matrix that aligns contract incoterms with responsibilities for loading, risk transfer, customs, insurance and unloading. Use Incoterms definitions to standardize responsibilities [3].
Decision table 2 — Example delivery responsibility matrix (illustrative)
| Responsibility area | EXW (Seller minimal) | FCA / FOB (shared) | DAP / DDP (Seller bears more) |
|---|---|---|---|
| Export packing | Seller usually packs for collection | Seller packs to agreed standard | Seller arranges export packing for transit |
| Domestic loading | Buyer arranges transport & loading | Seller/Buyer split per FCA/FOB | Seller arranges loading to carrier |
| Export customs | Buyer arranges (unless otherwise agreed) | Seller may assist under FCA | Seller clears export and sometimes import |
| Risk transfer | At factory gate | At carrier/ship’s rail or agreed point | At agreed destination point |
| Insurance | Buyer responsibility | Buyer or seller per clause | Seller often arranges and may include insurance |
Use the International Chamber of Commerce Incoterms as the authoritative guide when assigning obligations and risks [3]. Document the chosen Incoterm in the contract and map it to inspection and release responsibilities.
For export documentation and customs compliance, consult relevant import/export guidance and ensure the supplier can supply accurate commercial invoices, packing lists, certificates of origin and any required export licences [4].
Site installation, interfaces and operational handover
Factory checks are necessary but insufficient alone — interfaces with site works determine ultimate success. Factory evidence must be complemented by on-site verifications and coordinated handover.
Key site responsibilities to confirm:
- Foundation and anchor design: confirm embed plate locations and tolerances against as-built conditions.
- Structural capacity and uplift conditions: local geotechnical and wind/seismic inputs must be checked by qualified local engineers.
- Electrical interconnection: accept module rails, conduit entries and earthing continuity.
- Interface kits and spares: ensure bolting kits and critical spares are delivered with parts labelled for ease of installation.
- Installation training and documentation: request assembly drawings, torque specifications, and an installation sequence from the supplier.
- Quality acceptance at site: agreed installation hold points (e.g., before PV module mounting, mechanical completion, electrical commissioning).
Handover deliverables:
- As-built drawings and updated BOM.
- Final inspection report inclusive of site measurement records.
- Spare parts list and maintenance instructions.
- Warranties and conditions of coverage — note warranty terms are project-specific and should be documented in the contract.
Reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risks and mitigations
List the typical implementation risks and practical mitigations that link directly to fabrication checks.
Risk: Incorrect materials supplied
- Mitigation: Require mill certificates; inspect on receipt; use batch tagging.
Risk: Dimensional non-conformance causing rework
- Mitigation: Dimensional reports, jigs, 1:1 templates; buyer witness points for critical assemblies.
Risk: Coating failure in marine or aggressive environments
- Mitigation: Specify coating system and testing; request pre-ship adhesion test or recent supplier test results; use corrosion handling protocols [1].
Risk: Damage during transit
- Mitigation: Export packing coordination; photos of packing; insurance per contract terms.
Risk: Customs delays and missing documents
- Mitigation: Confirm export documentation list in advance; use customs brokers and check guidance [4].
Risk: Misaligned responsibilities leading to disputes at arrival
- Mitigation: Use an agreed delivery responsibility matrix and clear incoterm definitions [3].
Risk: Local permit or approval delays
- Mitigation: Early engagement with authorities; include timeline contingencies and permit-holder responsibilities in procurement.
Risk: Unskilled installers at site
- Mitigation: Supplier-provided installation supervision, training sessions, or approved installer lists.
For each identified risk, attach deadlines for mitigations and responsibility owners in the procurement schedule.
Six-step buyer workflow for evaluating fabrication checks
This named workflow consolidates prior sections into an actionable procurement process.
Step 1 — Define project acceptance baseline
- Deliverables: project basis documents, environmental inputs, structural and electrical design constraints, and acceptance criteria matrix.
- Output: a documented project basis used in all supplier communications.
Step 2 — Supplier selection and B2B supplier due diligence
- Tasks: shortlist suppliers, request factory capability info, financial checks, references and sample production evidence.
- Output: due diligence report and recommended supplier shortlist.
Step 3 — Technical scope comparison and bid evaluation
- Tasks: issue RFP with explicit technical scope; perform technical scope comparison of supplier responses, including deviations and clarifications.
- Output: comparison matrix and technical clarifications log.
Step 4 — Factory inspection plan and factory quality documentation
- Tasks: agree inspection plan with hold points; request factory quality documentation and method statements; schedule buyer-witness or third-party inspections.
- Output: approved inspection plan and list of required documentation.
Step 5 — Procurement contracts, export packing coordination and delivery responsibility matrix
- Tasks: finalize POs with clear commercial terms, incoterm selection, packaging requirements, delivery responsibility matrix and payment milestones tied to inspection holds.
- Output: signed contracts and logistics plan.
Step 6 — Pre-shipment verification, site acceptance and project procurement controls
- Tasks: final pre-shipment inspection, packing verification, shipping records; on-site installation checks, handover and closing QA.
- Output: final acceptance certificate, as-built documentation and warranty handover.
Embed project procurement controls through each step: defined sign-off authorities, hold points, QA records, and payment triggers linked to verified deliverables.
Practical checklist and templates for factory checks
Use the following checklist as a template for factory inspections. Adapt quantities and criticality per project.
Factory check template (core items):
- Document review
- PO and technical scope confirmation
- Material mill certificates for all structural alloys
- Welding procedure and operator lists
- Coating specifications and process logs
- In-process inspection
- Dimensional checks for critical items (holes, bolt centers)
- Weld visual inspection and NDT where applicable
- Coating thickness and visual finish
- Part labelling and kit completeness
- Pre-packing
- Packing list matches assembled kits
- Protective packaging applied; photographs taken
- Handling instructions labelled
- Shipping documentation
- Commercial invoice, packing list, certificate of origin (if required)
- Export licence (if applicable) and freight booking details
- Insurance details (as per contract)
- Handover
- Final inspection report signed by factory QA and buyer/inspector
- Photographic evidence of packaged units
- Release for dispatch only after signed acceptance
Frequently asked questions (FAQ)
Q: Which factory documents are essential and non-negotiable? A: Material mill test certificates, dimensional inspection reports for critical parts, final inspection sign-off, packaging photos, and any specified testing reports (e.g., coating testing). Welding procedure documentation is essential when welds are structural.
Q: Can remote video replace a physical factory audit? A: Remote video is valuable for preliminary assessments and to review specific hold points, but it cannot fully replace in-person audits for complex or high-risk projects. Use remote inspections to supplement, not substitute, where travel is impractical.
Q: How do I handle differences in technical scope between bidders? A: Use a formal technical scope comparison that lists every deviation, the supplier claim, and the buyer decision (accept with cost, accept with mitigation, or reject). This ensures apples-to-apples evaluation and protects procurement outcomes.
Q: Are ISO registrations sufficient proof of quality? A: ISO registration (e.g., quality management claims) indicates a management system exists, but it does not guarantee product conformance. Always request factory quality documentation, inspection reports and samples even from ISO-registered suppliers [2].
Q: Who should witness critical tests — buyer, third-party, or supplier QA? A: Prefer buyer or independent third-party witness for critical tests. Where buyer attendance is impossible, require authenticated third-party inspection reports and time-stamped photographic or video evidence.
Q: How to ensure packing survives sea transit? A: Require export packing coordination that specifies materials, securing methods, desiccants, and straps. Request photos and confirm packing has been tested against handling scenarios common to the intended transport mode.
Q: How to tie inspection outcomes to payment? A: Use project procurement controls: define payment milestones in the contract and link release of payment to documented, signed inspection reports and shipping release evidence.
Conclusion
Carport quality control fabrication checks are the pivotal link between design intent and operational performance. B2B buyers reduce project risk by converting technical specifications into measurable acceptance criteria, applying rigorous B2B supplier due diligence, and insisting on complete factory quality documentation. Coordinate export packing and logistics decisions through an explicit export packing coordination plan and define responsibilities in a delivery responsibility matrix aligned to Incoterms. Implement project procurement controls with defined hold points, inspection plans and contract-linked payment milestones. Finally, integrate factory checks with thorough on-site verification; remember that structural, electrical, permitting, lead time, price, energy yield and warranty outcomes all require a documented project basis and review by local qualified professionals, installers, utilities and authorities.
Mid-article CTA If you would like help aligning technical acceptance criteria with supplier checks for a specific project, start an enquiry: /inquiry
For product fit and system options see the Carportiva system range and explore all systems. For broader procurement templates and checklists consult our sourcing guides.
Closing CTA and contact If you need a project consultation or a copy of our standard factory inspection checklist, contact: info@carportiva.com
Cited sources
- American Galvanizers Association — galvanizing practice and guidance [1].
- International Organization for Standardization — standards and management system guidance [2].
- International Chamber of Commerce Incoterms — responsibility and risk allocation reference [3].
- U.S. Customs and Border Protection — import/export compliance guidance [4].
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion