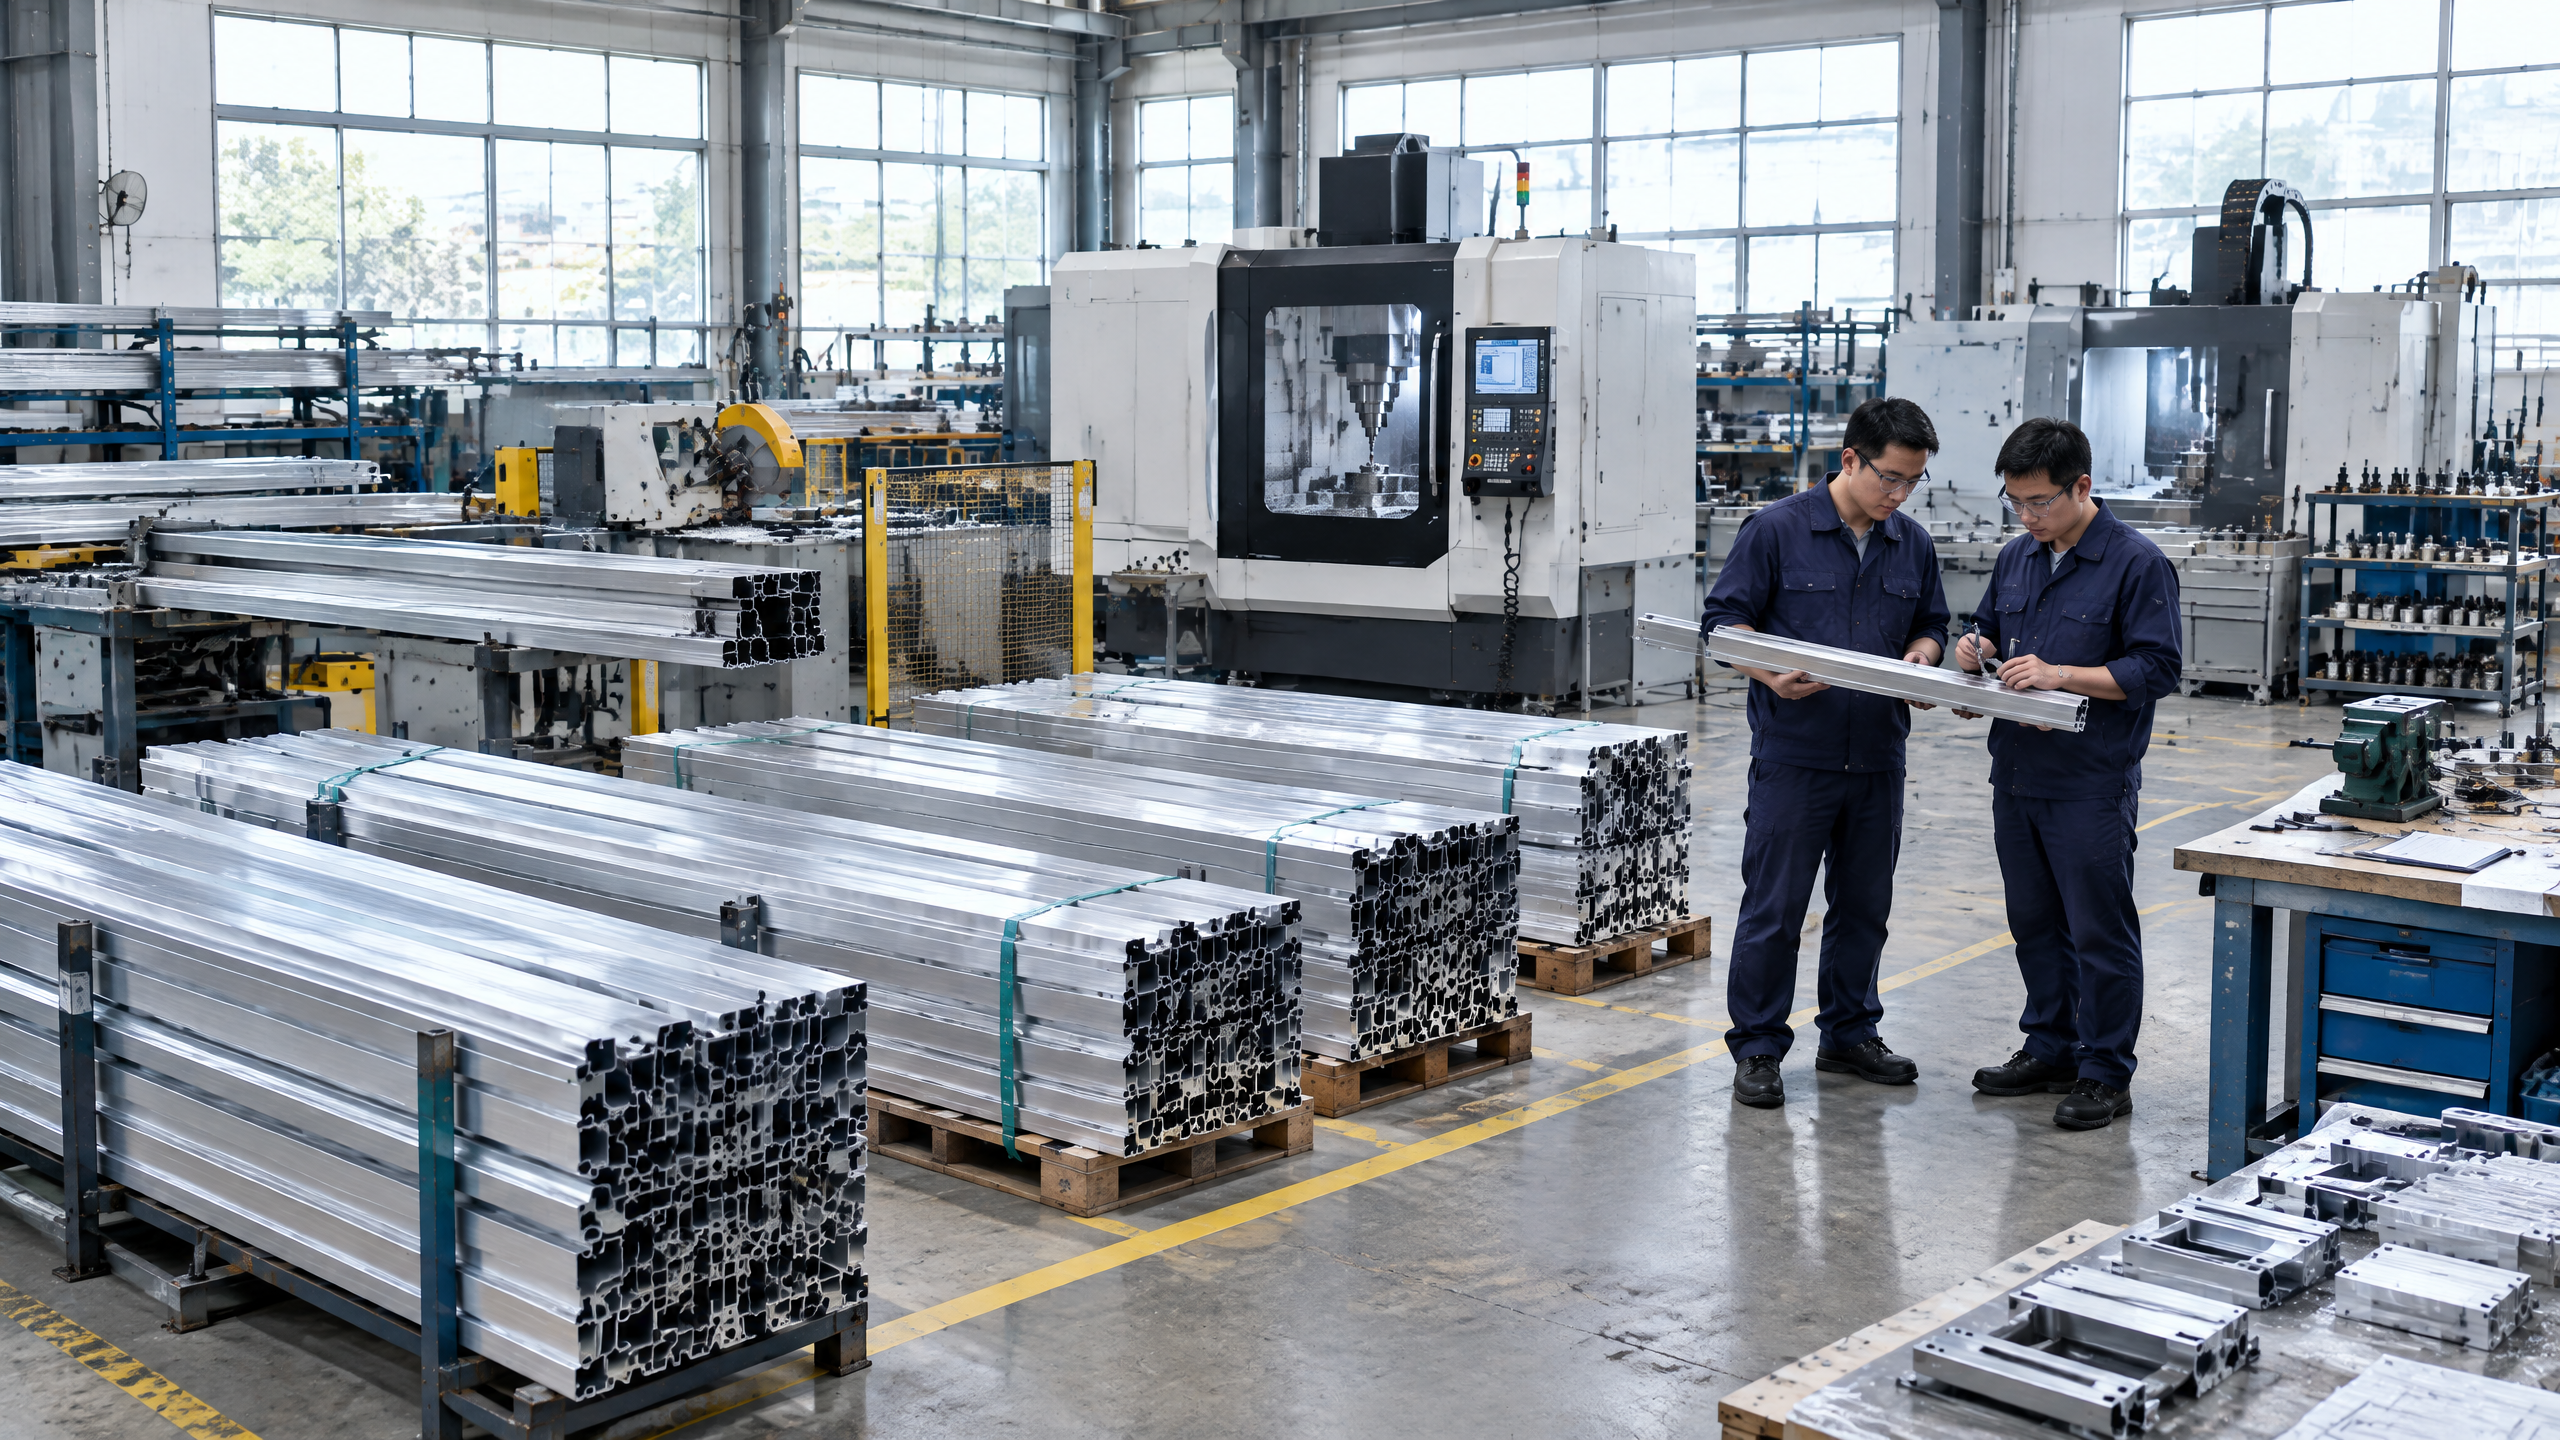
A carport quality control finish inspection is the single most important checkpoint that connects factory production standardization to successful site installation and long-term performance. The project team should confirm that the finished carport components meet the contractual technical scope, documented surface and structural acceptance criteria, and packing and shipping conditions that protect those finishes in transit. Confirmation must be evidence-led: signed shop drawings, material mill certificates, factory quality documentation, photographic records of the finished assemblies, pre-shipment inspection reports, and agreed rectification plans for any non-conformances. The team must also ensure fit-for-purpose interfaces with the site (foundations, penetrations, electrical works), clear responsibility for delivery and customs, and that any remaining items are controlled via the project procurement controls and delivery responsibility matrix. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Buyer context and scope boundary
Why this matters for procurement
- A carport quality control finish inspection is not only a cosmetic check: for aluminium architectural carports, commercial solar carports and industrial/fleet shelters the finish directly affects corrosion resistance, warranty eligibility, PV mounting integrity, and long-term maintenance cost.
- In B2B procurement the inspection bridges supplier production and buyer-site readiness. The buyer’s decision to accept shipments should be based on documentary and physical evidence, not on assumptions.
Who is the audience for inspection outputs
- Distributors and resellers need documentary evidence to support warranties and claims.
- Architects and contractors require confirmatory records that delivered geometry, tolerances and finishes match the construction documents.
- Developers, solar EPCs and fleet operators require assurance that coatings, load interfaces and PV-fixings meet project environmental and operational specifications.
- Installers require clear pack contents, labeling and fitment guides for efficient on-site work.
Scope boundaries you must define in contracts
- Define whether the inspection covers surface finish only, or includes dimensional conformity, fit-up of PV rails, fastener torque and type, and electrical interfaces.
- Specify whether inspection is performed at shop-level, at assembly (sub-system) level, or on completed units after packaging.
- Explicitly record excluded items: site foundations, final electrical connection, civil penetrations, local permits and approvals.
- Note that site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Define acceptance at the outset
- Acceptance criteria must be in procurement documentation — color codes, coating thickness targets, anodize class, powder-coat systems, acceptable surface defects and tolerance bands for dimensional checks.
- Include acceptance thresholds for packaging integrity and labels used during export packing coordination to reduce transit damage risks.
Core decision principle
Adopt a risk-based, evidence-led acceptance rule
- Principle: accept only against documented, contractually agreed acceptance criteria and verified evidence. If evidence is incomplete, stop shipment until resolved.
- Prioritize controls by risk: safety-critical elements and interfaces (anchor plates, PV mounting rails, standoff isolators) get the highest inspection priority; purely cosmetic elements get secondary checks.
- Use a sample-based approach where appropriate — specify sample sizes and acceptance sampling method in procurement documents — but require full-documentary verification for all shipped lots.
How to balance speed and certainty
- For standard repeat production for an approved supplier, rely on periodic extended audits plus routine pre-shipment samples. For new suppliers, prototypes or changed designs, require full shop inspection and copies of all factory quality documentation.
- Include hold-points in the schedule: e.g., "no shipment without signed finish inspection report and photographic evidence."
Decision triggers for rework, rejection or acceptance
- Non-conformance to safety-critical items → mandatory rework or retained at factory for rectification.
- Non-conformance to cosmetic items within agreed thresholds → accept with noted concession and price/repair arrangement.
- Documentation gaps (missing test reports, missing marking) → withhold acceptance until documentation is complete.
- Use a formal non-conformance report (NCR) process with timelines and responsibilities defined in the delivery responsibility matrix.
Planning inputs
Documents and inputs you need before inspection
- Contractual technical specification and scope drawings (baseline).
- Approved shop drawings and record of revisions (revision-controlled).
- Material certificates (mill certs) for aluminium alloys, fasteners and steel parts.
- Coating system specifications: manufacturer data sheets, target dry film thickness (DFT) ranges, and surface preparation methods.
- Sampling and acceptance plans describing number of units to be inspected, test points and hold-points.
- Schedule and supplier lead time with planned inspection windows.
- Logistic plan including export packing coordination, transport modes and incidental insurance.
Procurement controls and governance
- Project procurement controls should be explicit: define who can approve waivers, sign inspection reports and accept shipments. Assign signatories and alternates.
- Maintain a master document register that links each shipped lot to its factory quality documentation and inspection records.
- Include clauses that allow the buyer to appoint an independent inspector or third-party verifier for critical lots.
B2B supplier due diligence
- Perform B2B supplier due diligence early: factory capabilities, ISO registrations [2], health and safety practices, references for similar carport systems, and sample production runs.
- Evaluate logistics partners for export packing coordination and experience with aluminium extrusions and long-span assemblies.
Timeline and lead time inputs
- Build time for inspections into the procurement schedule. Include contingency for repairs and re-inspection.
- Clarify whether lead time is contractual (fixed) or estimated; exceptional lead time changes should trigger escalation and re-evaluation.
Technical specification and interfaces
Essential finish and material specifications
- Aluminium alloy and temper, anodizing class or powder-coat system, expected DFT ranges, and acceptable surface defect classification.
- For galvanised steel components (if used), verify galvanizing process and acceptance tests; consult galvanizer best practice for specification details [1].
- Fastener materials and corrosion class: stainless steel grades, coating compatibility with aluminium to avoid galvanic corrosion.
Interfaces to building and systems
- Structural interfaces: anchor plate layout, bolt patterns, tolerances, and grout or embedment requirements.
- Electrical interfaces: PV array mounting points, cable entries, junction boxes and earthing/grounding arrangements. Note: final electrical design and approvals are site-specific and require qualified electrical engineers and utilities.
- Drainage and roof interfaces: ensure wash-through, water proofing and flashing are coordinated with site designs.
- Thermal movement: design for expected thermal expansion cycles and verify slotted holes where required.
Acceptance parameters you must specify
- Dimensional tolerances for key members and bolt hole positions (coordinate reference system).
- Coating thickness and adhesion test methods (wet film vs dry film, cross-hatch adhesion tests).
- Surface cleanliness and preparation: acceptable pre-treatment processes and tests.
- Color and gloss: sample panels with signed approval to be used as reference in finish inspection.
Testing and verification methods
- Non-destructive visual and dimensional inspection for all units.
- Coating thickness by meter or gauge at agreed points.
- Adhesion and cross-cut tests on representative samples.
- Torque checks for fasteners on assembled components (where assembly is completed in factory).
- Photographic documentation of issues and of final accepted parts.
Regulatory and standards references
- Encourage suppliers to reference recognized standards for quality systems [2] and to use appropriate galvanizing guidance where relevant [1]. For commercial aspects of delivery and who bears risk in transit, reference and use Incoterms [3]. For customs documentation and import readiness see guidance from relevant authorities [4].
Procurement / factory evidence
What qualifies as acceptable factory evidence
- Approved shop drawings with revision numbers and sign-off stamps.
- Factory quality documentation: inspection checklists, material mill certificates, coating datasheets, non-conformance reports, corrective action records and test results. Use the exact term factory quality documentation in procurement clauses.
- Photographic records showing entire assemblies and detail close-ups of high-risk interfaces.
- Pre-shipment inspection (PSI) or factory acceptance test (FAT) reports signed by buyer or third-party inspector.
- Packing lists and export packing coordination instructions included with each shipment.
Sample factory inspection checklist (example)
- Visual surface inspection against reference panel.
- DFT measurements at specified points where coatings are applied.
- Hole position and dimension checks at primary anchors and rail mounts.
- Fastener specification and applied torque confirmation.
- Packaging verification: cushioning, blocking, edge protection and labeling.
Decision table — Accept/Reject actions for common finish findings
| Finding | Accept / Reject | Required next step |
|---|---|---|
| Surface contamination or oil spots in small isolated areas within agreed cosmetic tolerance | Accept with notation | Spot-clean and note in packing list; buyer to accept with concession |
| Powder-coating delamination or bubbles on structural interface | Reject | Hold for rework; re-inspect; no shipment until cleared |
| Dimensional out-of-tolerance at anchor bolt pattern (> specified tolerance) | Reject | Rework or remanufacture components; consider on-site modification only with engineered approval |
| Minor scuffs on protected, non-exposed edges | Accept | Repack with additional protection; document and accept |
| Missing material certificates | Reject | Provide mill certs before shipment; hold goods if already packed |
Delivery responsibility and logistics evidence
- Require a delivery responsibility matrix in the contract. This should allocate who is responsible for packing quality, insurance during transit, customs clearance documentation, and claims for damage.
- Include export packing coordination clauses specifying handling instructions, strapping locations, maximum bundle weights, and preferred carrier handling.
Decision table — Example delivery responsibility matrix
| Item / Activity | Supplier | Buyer | Forwarder / Carrier |
|---|---|---|---|
| Packaging design and materials | Primary | Review/approve | Execute |
| Export packing coordination | Lead | Provide requirements | Execute |
| Loading at factory | Lead | Witness/right to inspect | Execute |
| Shipping insurance | Option (depending on Incoterm) | Option | Facilitate |
| Customs export documentation | Supplier | Review | Agent |
| Customs import clearance | Varies by Incoterm | Varies by Incoterm | Agent |
| Damage claim handling | Initiate | Support | Carrier/Insurer |
Note: Align responsibilities with chosen Incoterm; use Incoterms to determine transfer of risk and costs [3]. For import documentation guidance, consult customs guidance specific to the importing country [4].
Third-party inspection and certification use
- Where risk or regulatory needs are high (e.g., fire-rated components, specialized coating systems or large-scale solar arrays), include the right to appoint an independent inspection body for FAT/PSI and require supplier acceptance in contract.
- Require inspection agencies to provide clear, timestamped reports and photographic evidence and to follow defined sampling methods.
Documentation control and traceability
- Ensure every shipment is traceable to the inspected lot. Reference inspection reports, mill certificates, and packing lists with lot numbers.
- Require retention of factory quality documentation for a contractually specified period.
Site installation and operations
Pre-installation site checks
- Confirm that foundations are built to the design tolerance band and that anchor locations are within specified positional tolerances.
- Verify that site access, crane or lifting equipment, and temporary storage areas meet the handling requirements for longest extrusions and heaviest bundles.
- Confirm that permits, local approvals and electrical supply arrangements are in place. Note: final electrical design and approvals require local qualified professionals and utilities.
Receiving and unpacking best practice
- Open and inspect critical components on arrival according to the packing list and pre-agreed inspection checklist.
- Photograph any transit damage and segregate affected parts. Notify the supplier and forwarder immediately; begin a parallel evaluation for possible on-site repairs or exchange.
- Check that labels and part numbers match shop drawings and that any jigs, templates and assembly instructions are present.
On-site fit-up and commissioning checks
- Check alignments and hole positions against as-built shop drawings.
- Torque fasteners to specified values and record torque test results for critical connections.
- For solar carports: verify PV rail and clamp positions before PV module delivery; confirm earthing continuity and cable routing; final electrical commissioning requires certified electricians and compliance with local regulations.
- Confirm that protective measures for finishes are removed only when work area is clean and until final commissioning.
Operations and maintenance handover
- Provide the operator with a complete handover pack: as-built drawings, factory quality documentation, coating and maintenance data sheets, and spare part list.
- Create a maintenance schedule for cleaning, coating checks and fastener inspections and include recommended inspection intervals based on site environment.
Implementation risks and mitigation
Common risks tied to finish inspection and how to mitigate
Risk: Unclear acceptance criteria leading to late discovery of non-conformances
- Mitigation: Specify finish acceptance criteria and sample panels in the contract. Use technical scope comparison exercises during bid evaluation.
Risk: Transit damage to long extrusions or fragile finishes
- Mitigation: Define export packing coordination, require edge protection and blocking, and specify acceptable palletization. Capture photographic packaging sign-off in the factory quality documentation.
Risk: Supplier documentation gaps or falsified certificates
- Mitigation: Use third-party verification for critical certificates and perform B2B supplier due diligence. Require traceable mill certs and maintain an auditable record trail.
Risk: Interface misalignment between factory-made items and site work (foundation anchors mismatch)
- Mitigation: Freeze anchor positions only after approved shop drawings and coordinate a site-template verification. Consider using a pre-shipment anchor template check.
Risk: Lead-time-driven compromises (rush shipments)
- Mitigation: Project procurement controls should trigger escalation when lead times shorten and demand rework of acceptance sampling or increased inspection coverage.
Risk: Warranty disputes on finish degradation
- Mitigation: Keep photographic baseline during final factory inspection and ensure maintenance requirements are provided to the owner at handover. Warranties should be explicit about what finish behaviors are covered and for how long.
Risk: Customs delays and regulatory hold-ups
- Mitigation: Align delivery responsibility matrix with Incoterms and verify customs documentation is complete; use an experienced forwarder and confirm import procedures in advance [3][4].
Controls to implement in procurement
- Hold points and sign-off gates tied to shipment.
- Documentary completeness checklists that must be cleared before goods leave the factory.
- Acceptance sampling plan and dispute resolution timelines.
- Defined responsibilities in a delivery responsibility matrix and contractual remedies for repeated non-conformances.
Mid-article action (if you want to review inspection requirements with our team): /inquiry
Carportiva six-step buyer workflow for finish inspection
Name: Carportiva Six-Step QC Finish Inspection Workflow
Step 1 — Define the technical baseline and acceptance criteria
- Produce a single-source technical scope and approved shop-drawing set. Include finish system, DFT targets, sample panel sign-off, and dimensional tolerances.
- Cross-reference this scope with the procurement contract, warranty obligations, and maintenance expectations.
Step 2 — B2B supplier due diligence and selection
- Validate supplier capabilities, previous project references for similar products, and quality system maturity (ISO references where relevant) [2].
- Conduct a technical scope comparison between suppliers to ensure like-for-like compliance and to reveal deviations early.
Step 3 — Prototype verification and sample approval
- Acquire physical sample panels and full-size mock-ups for critical interfaces (anchor assemblies, PV clamp areas).
- Approve sample panels in writing and attach them to procurement documents as a mandatory acceptance reference.
Step 4 — Factory quality documentation and inspections
- Require factory quality documentation to include material certificates, inspection checklists, NCRs, photographic evidence and signed pre-shipment inspection reports.
- Hold the supplier to documented corrective actions and require re-inspection prior to shipment for any previously recorded NCRs.
Step 5 — Export packing coordination and shipping control
- Finalize export packing coordination details: packing lists, strapping diagrams, labeling, bundling and carrier instructions.
- Use a delivery responsibility matrix to allocate roles for packing, insurance, customs and claims handling. Ensure Incoterm choice is documented and understood by all parties [3].
Step 6 — Site receipt, fit-up, and handover
- Conduct receiving inspection immediately and verify against the pack list and FAT/PSI reports.
- Execute onsite fit-up checks, record torque results, and sign off the final acceptance once commissioning and site tests are complete.
- Handover full documentation and maintenance instructions to the owner/operator.
Workflow controls and records
- Maintain an audit trail for each step, including sign-offs, inspection reports and photographs.
- Define SLA timelines for supplier responses to NCRs and for rework completion.
FAQ
Q: What exactly is covered by a carport quality control finish inspection? A: It covers verification that finished parts meet the contractually-defined material, coating and dimensional requirements, plus packaging standards intended to protect those finishes in transit. It can be scoped to include assembly checks, fastener torque, and packing verification.
Q: Who should perform the inspection — the buyer, the supplier or a third party? A: The buyer can perform or witness inspections if resources are available. Where impartiality or expertise is needed, appoint a qualified third-party inspector. Contracts should clarify inspection rights and lead times for inspector access.
Q: How many samples should be inspected? A: Sample size must be specified in the procurement documents and based on production lot size and risk. High-risk or novel designs require larger sampling or full inspection prior to shipment.
Q: What is factory quality documentation and why is it required? A: Factory quality documentation is the set of records (inspection checklists, test reports, mill certificates, NCRs) that demonstrate conformance to the contract. It creates traceability and is essential for claims and warranty validity.
Q: If a finish issue is discovered after installation, who is responsible? A: Responsibility depends on the root cause (manufacturing, transport damage, site conditions or improper maintenance) and on the allocation set out in the delivery responsibility matrix and warranty clauses. Determination often requires joint inspection and review of factory quality documentation.
Q: Are there standard references or rules to help allocate delivery responsibilities? A: Yes — Incoterms provide standard definitions of when risk transfers from seller to buyer for goods in international trade, which should be used alongside a contractually agreed delivery responsibility matrix [3].
Q: How do I protect finishes during export and transit? A: Require export packing coordination with written packing instructions, edge protection for extrusions, moisture barriers for vulnerable items, correct labeling, and claims procedures. Record packing photos at the factory as part of the pre-shipment evidence.
Q: Can I accept goods with cosmetic defects if I need them urgently? A: Accepting concessions must be pre-authorized and documented. Use project procurement controls to record any agreed concessions and the financial or remedial arrangements.
Q: What is the role of maintenance documentation after handover? A: It defines cleaning regimes, inspection intervals and approved repair processes for finishes. It is key to preserving warranty eligibility and long-term performance.
Q: Do I need local professionals for site checks and final approvals? A: Yes. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Conclusion
A comprehensive carport quality control finish inspection process protects project value from factory production through to field performance. The buyer’s control points are the contractual technical scope, evidence-based factory quality documentation, clear export packing coordination, and a delivery responsibility matrix that allocates risk and actions. Use the Carportiva Six-Step QC Finish Inspection Workflow to translate specification into verifiable outcomes: define the baseline, perform supplier due diligence, approve samples, require factory documentation and inspections, coordinate export packing and logistics, and verify on-site fit-up and commissioning.
For system-specific details and sample panels, review the Carportiva system range and our all systems technical summaries. For procurement checklists and templates that complement this guide, see our sourcing guides.
If you wish to coordinate a review of inspection protocols for a live procurement package, contact us: info@carportiva.com.
Note on professional responsibilities: Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion