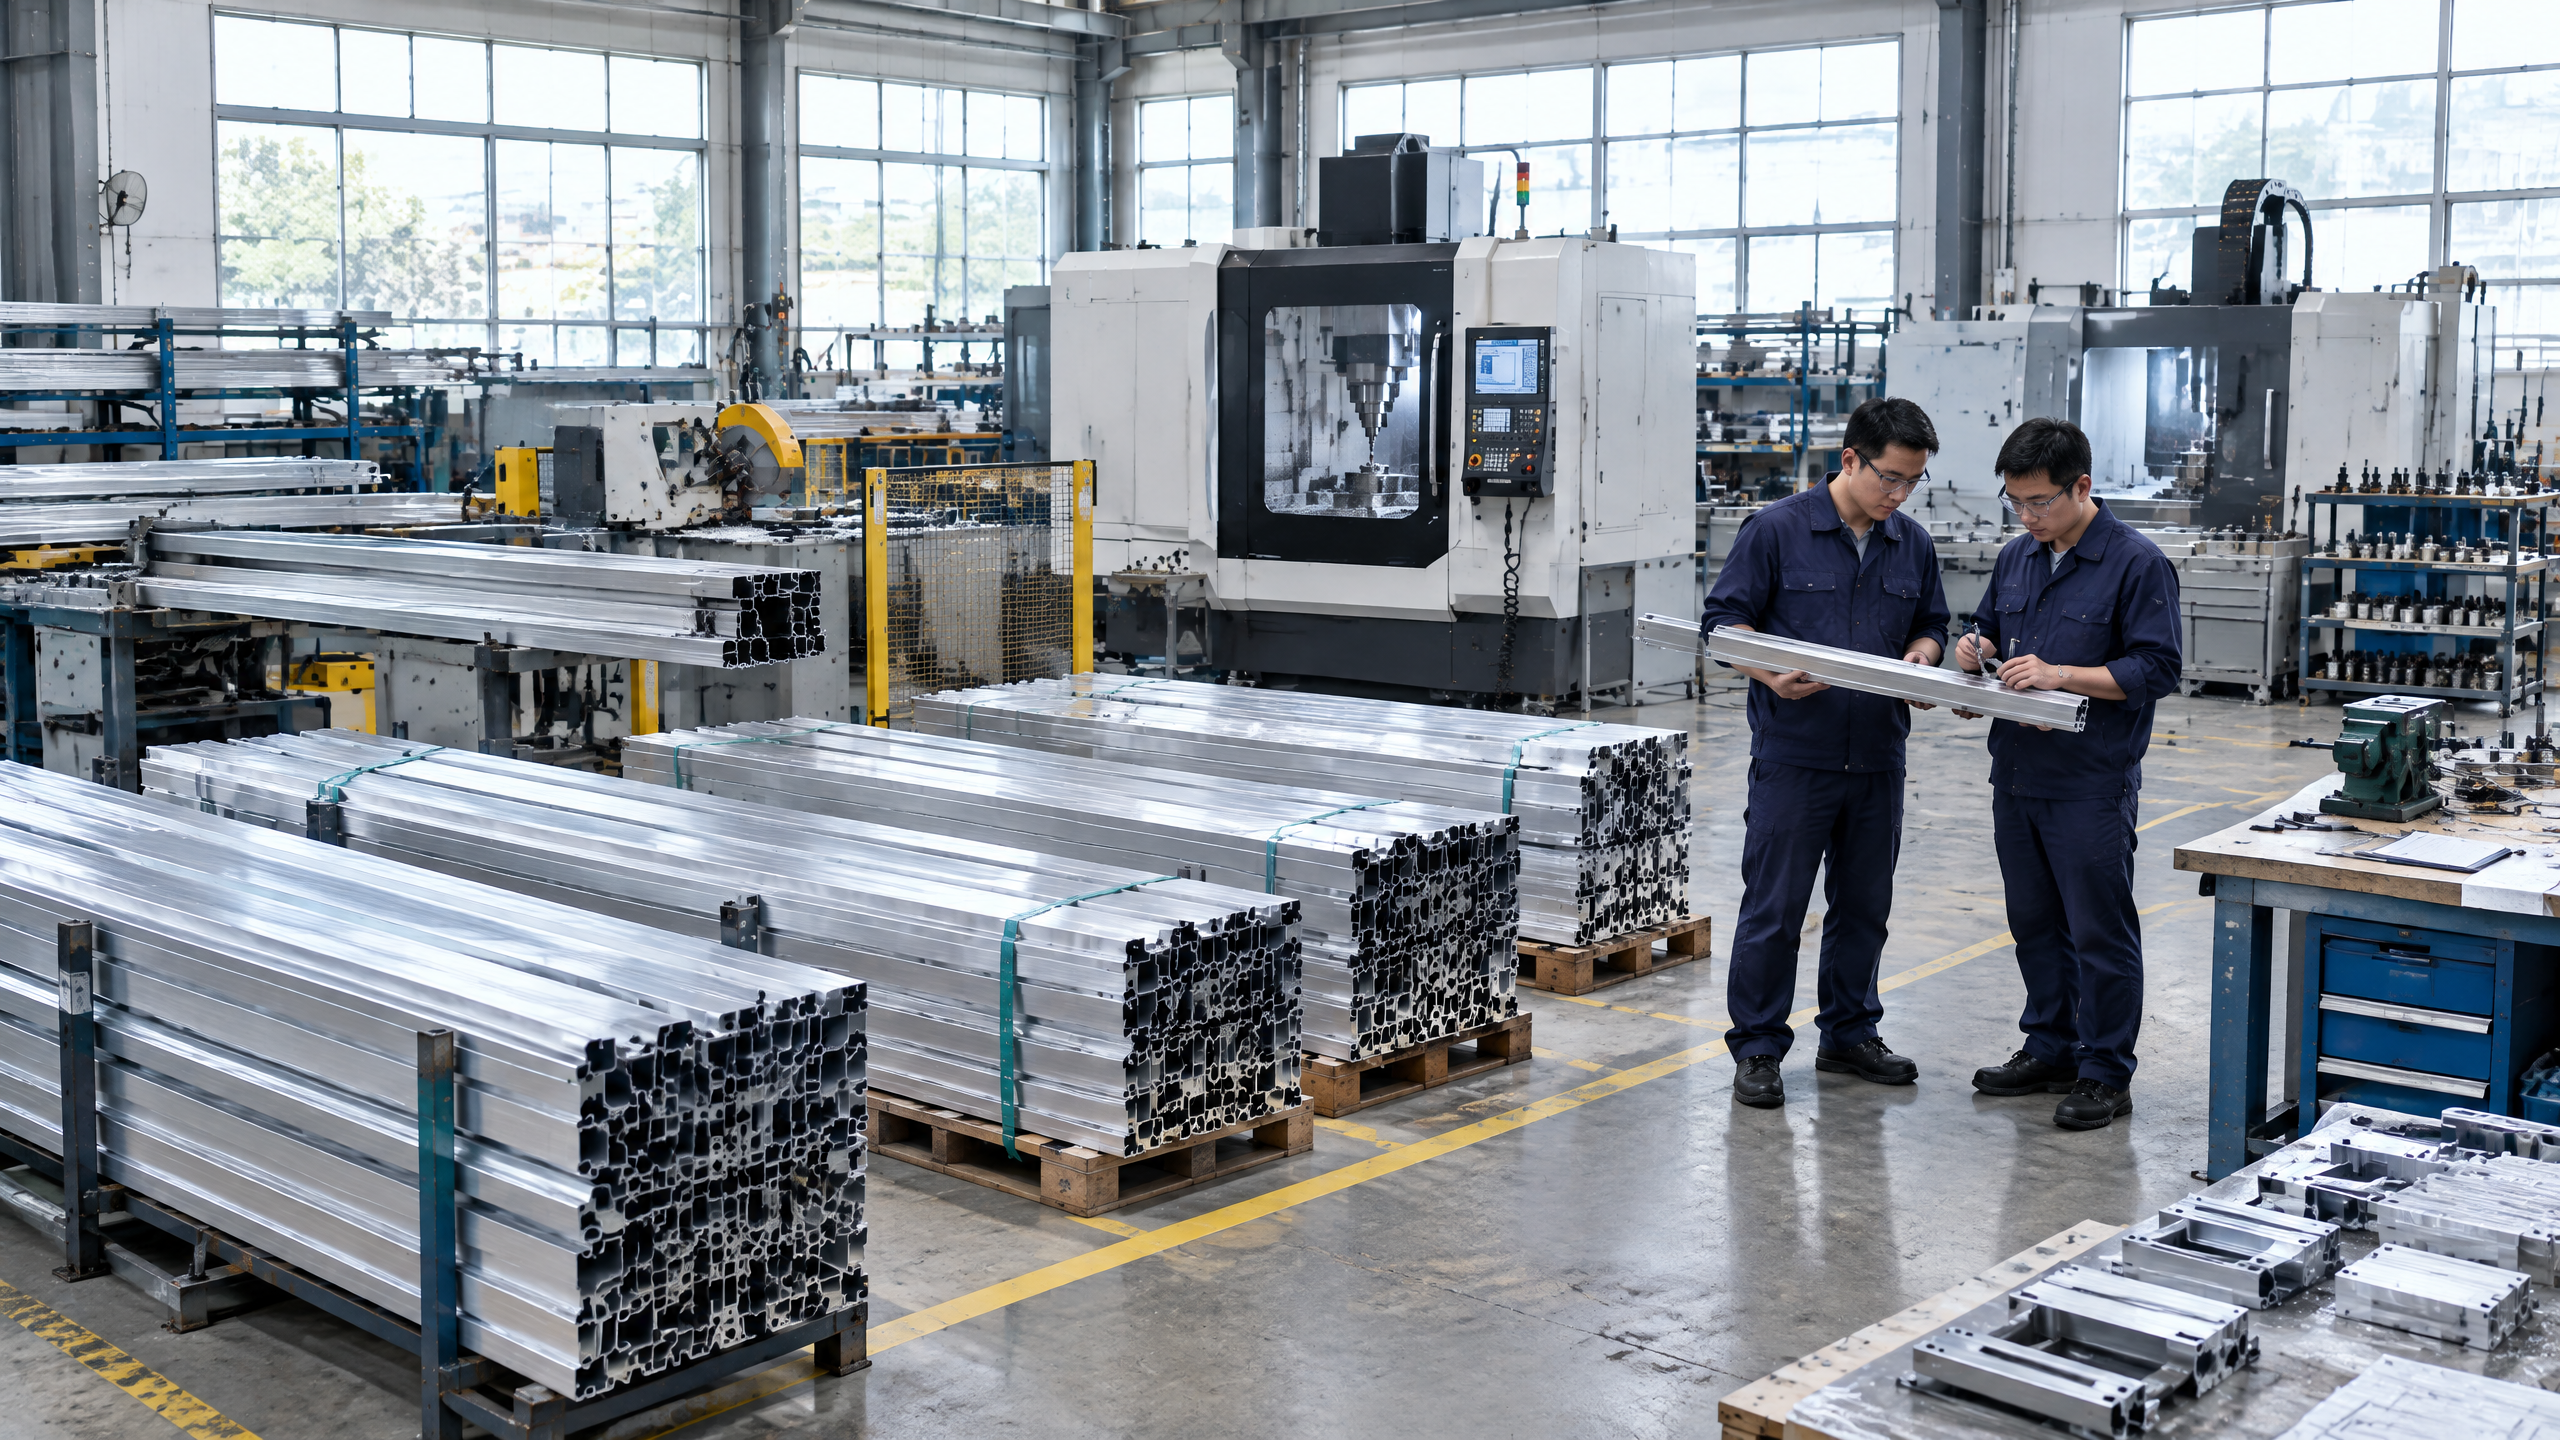
A carport supplier factory audit should answer whether the supplier can consistently deliver the design, quality and delivery behavior your project requires — demonstrated by verifiable factory quality documentation, process evidence and controls that map to your project's technical and commercial boundary conditions. A focused factory audit for carport systems validates production capability (materials, profiles, galvanizing or coatings, assembly jigs), quality management and inspection processes, export packing coordination and logistics readiness, and the contractual delivery responsibilities that affect risk allocation on site. For B2B buyers this audit is part of B2B supplier due diligence: it must be compared against a documented technical scope comparison, integrated into project procurement controls and translated into a delivery responsibility matrix so procurement, construction and operations teams have a single source of truth for handover, warranties and non-conformance handling.
Buyer context and scope boundary: why a carport supplier factory audit matters
A carport supplier factory audit is not a single checkbox. It must be scoped to the project’s commercial and technical boundaries: who supplies foundations and fixings, who supplies electrical balance of system (BOS) items for solar carports, what tolerances are acceptable for module mounting and roof pitch, and who carries responsibility for packaging, export and inland delivery. The audit reduces surprises that arise at site handover by verifying that factory processes and documented outputs match the procurement documents used by the project team.
Audience considerations:
- Distributors and contractors need confidence in reproducibility, spare parts and installation clarity.
- Architects and developers need assurance that delivered elements match approved drawings and interface conditions.
- Solar EPCs need evidence that module rails, clamp positions and cable penetrations are factory-aligned to electrical designs.
- Fleet operators need clarity on warranty, maintenance interfaces and on-site resilience.
Key boundary questions to confirm before and during the audit:
- Which party provides foundations, anchor bolts and piling design?
- Is the supplier responsible for structural engineering in the destination jurisdiction, or only for fabrication?
- Which items are supplied factory-assembled vs site-assembled?
- What is included in export packaging, and who manages inland transport?
This section sets the frame for the audit: define what is in-scope (fabrication, QA, packing, export documentation, pre-shipment testing, module mounting interfaces) and what is out-of-scope (local civil works, electrical final connections, grid approvals).
Core decision principle: evidence over assertion
The primary procurement decision principle for a carport supplier factory audit is “evidence over assertion.” Suppliers commonly make capability claims; the audit converts those claims into inspectable, verifiable evidence and contractual requirements. Evidence types include management system records, process flow charts, inspection records, material traceability, calibration certificates, routine test logs, non-conformance histories, and packaging lists.
What to expect from evidence:
- Factory quality documentation that directly links processes to part numbers and final inspection outcomes.
- Traceability for structural aluminium profiles and steel fixings (batch numbers, mill certificates where applicable).
- Records of weld parameters and fixture jigs for repeatable assembly accuracy.
- Photographic records of packing methods and completed pallets.
- Documented corrective action for previously raised non-conformances.
Where formal certification exists (e.g., ISO system registration), it provides context but does not replace project-specific evidence. Use ISO or other standards as a baseline for process consistency rather than project acceptance criteria alone [2].
Planning inputs: define what the audit must measure
Before the auditor(s) visit, the project team must assemble a clear inputs pack so the factory audit focuses on what matters for the project’s success. Inputs should be structured and version-controlled in your procurement system.
Essential planning inputs:
- Technical scope comparison (see below) that compares buyer specifications, drawing interfaces, BOM and supplier offered scope.
- Contractual documents: purchase order, commercial terms, delivery conditions and warranty clauses. Cross-reference Incoterms for risk transfer and payment triggers [3].
- Critical dimensions and tolerances: roof span, column spacing, module row spacing, water drainage details.
- Materials and coatings list: aluminium grades, surface treatments, galvanizing requirements (reference guidance on hot-dip galvanizing) [1].
- Packing and transport constraints: unit loads, pallet dimensions, export packing coordination expectations, and container stuffing requirements.
- Test and inspection plan: inspections to be witnessed, hold points, and pre-shipment inspection criteria.
- Project schedule constraints: required lead times, milestone dates for delivery and stage payments.
Technical scope comparison is a controlled deliverable that should be produced before the audit. It is the primary benchmark the audit uses to confirm compliance.
Decision table: minimum audit inputs checklist
| Required input | Why it matters | Acceptable evidence |
|---|---|---|
| Technical scope comparison | Establishes baseline for acceptance | Documented side-by-side comparison signed by buyer/supplier |
| Purchase order / contract | Defines commercial terms and obligations | Contract and referenced annexes |
| BOM and part numbers | Prevents substitution risk | Master BOM linked to drawings |
| Packing list / export packing rules | Drives export readiness and inland handling | Written packing spec and sample photos |
| Test & inspection plan | Defines hold points and witness requirements | Plan with inspection criteria & acceptance limits |
| Project schedule | Frames lead time and delivery windows | Confirmed milestone dates |
Technical specification and interfaces: what the audit must verify
The technical verification must be practical, measurable and tied to the project interface conditions: module rails, mounting clamps, drainage, column base plates and tolerances that affect foundations. The factory must demonstrate it consistently builds to the specified configuration or documents approved deviations.
Key technical checkpoints:
- Dimensional control: verify that jigs, fixtures and measurement processes produce tolerances required by the project. Request records from prior identical assemblies or witness in-process measurement routine.
- Structural components: material grade certifications, section tolerances, weld procedures and inspection (visual, dimensional). For galvanized parts, confirm pre-treatment and coating process (see galvanizing guidance) [1].
- Pre-assembly and bolting: check torque control and torque tool calibration records, bolt grade traceability and anti-seize/thread-lock procedures.
- Module rail interfaces (for solar carports): confirm hole pitch, slot tolerances, and clamp compatibility with the specified PV module vendor(s).
- Drainage and water management: roof pitch and edge details that affect on-site drainage tie-ins.
- Surface finishes: record process controls for powder coat ovens, adhesion tests and CIELab color consistency where required.
- Test plates: request sample component test results where destructive or non-destructive testing is part of the acceptance criteria.
Technical scope comparison: an actionable deliverable
The technical scope comparison is a table that maps buyer requirements to supplier confirmations. It should be an auditable document attached to the purchase order and used as the acceptance baseline.
Example technical scope comparison table (excerpt):
| Requirement | Buyer specification | Supplier confirmation | Evidence location / document |
|---|---|---|---|
| Column steel grade | S355 or equivalent | Supplier confirms S355 supplier mill certificates | Mill certificate ref. # |
| Module rail hole spacing | 190 mm ±1 mm | Factory pilot measurement 189.8–190.1 mm | Dimensional inspection report |
| Powder coat thickness | 60–80 µm | Process control: inline thickness meter; records retained | Coating QC logs |
| Packing per module | Individual pallet crates matching container heights | Supplier packing spec + photos | Packing spec and photos annex |
Do not accept supplier confirmations that are not backed by objective evidence.
Procurement and factory evidence: the audit checklist
A core outcome of the factory audit is an evidence pack that can be retained in procurement records and used to drive project procurement controls. The pack should be itemised, dated and linked to specific lot numbers or shipments.
Audit evidence categories and examples:
- Management system: copy of relevant ISO registration (if held) and the scope, plus quality manual sections relevant to metallurgical controls and fabrication [2].
- Material traceability: mill certificates, heat numbers, and supplier invoices tying batches to finished parts.
- Inspection and test records: dimensional inspection sheets, torque test logs, test certificates for welding consumables, and NDT reports where applicable.
- Calibration records: calibration certificates for torque wrenches, thickness meters, torque testers and dimensional gauges.
- Non-conformance records: NCRs, root causes, corrective actions and the status of open issues.
- Packing documentation: packing lists, sample photos of crates and palletization, export packaging materials specification (fumigation/phytosanitary where applicable).
- Logistics readiness: container stuffing diagrams, transport provider confirmations, and export documentation readiness (commercial invoices, packing lists, certificates of origin if required).
- Pre-shipment inspection reports and signoff: third-party inspection reports or buyer witness reports.
Decision table: evidence acceptance criteria
| Evidence type | Minimum acceptability | Follow-up action if missing/insufficient |
|---|---|---|
| Mill certificates | Certificates traceable to batch and part | Require replacement certificates or retest samples |
| Dimensional inspection | Records for the lot with pass/fail marks | Hold shipment until re-inspection |
| Calibration records | Current calibration within interval | Require calibration before next production run |
| Packing photos | Photos for representative pallets and container simulation | Request packing trial or witness packing |
| NCR history | Closed or documented CAPA for repeat issues | Escalate to contract condition or impose hold points |
| Export docs | Drafts aligned to Incoterms and required permits | Coordinate with buyer logistics and customs broker [3][4] |
Use these criteria in your procurement system to grade supplier readiness and trigger contractual remedies or acceptance hold points.
Logistics, export packing coordination and delivery responsibility matrix
Logistics readiness is part of the factory audit. Inspectors should confirm pack design, lashing, dunnage, cushioning and container stuffing options for sea and air freight. Export packing coordination must be explicit in the supplier’s responsibilities and aligned with carrier constraints and customs processes.
Key logistics checks:
- Packing design for environmental exposure, handling impacts and stacking loads.
- Container stuffing diagrams and maximum packing density to avoid damage.
- Hazardous materials declaration (if any) and compliance with carrier rules.
- Export documentation drafting and preliminary customs classification.
- Coordination with buyer’s nominated freight forwarder or an agreed third party.
Delivery responsibility matrix — a procurement must-have
A delivery responsibility matrix defines who does what and where risk transfers. Use Incoterms as the baseline for legal risk allocation, and then detail specific tasks and handovers.
Example delivery responsibility matrix
| Activity | Supplier responsibility | Buyer responsibility | Typical document / acceptance |
|---|---|---|---|
| Manufacturing to PO spec | X | Factory QA report | |
| Export packing | X | Packing list + photos | |
| Inland transport to port/terminal | X (if FCA) | Waybill / terminal receipt | |
| Ocean freight booking | X (if buyer-arranged) | Bill of Lading | |
| Customs export clearance | X or nominated agent | Export declaration | |
| Import clearance | X | Import customs release | |
| Delivery to site | X (DDP) or | Site delivery report | |
| On-site unloading and placement | X | Handover certificate |
Note: apply the matrix consistently across all purchase orders. Incoterms provide the legal backbone for risk and cost transfer but do not prescribe operational tasks such as packing method — these must be specified separately [3].
Site installation and operations: translation of factory outputs to site performance
A factory audit must tie manufacturing output to installation and long-term operation. On-site issues often stem from misalignment in interfaces between site-supplied elements and factory-supplied components.
Installation interface checkpoints:
- Anchor bolt template checks: confirm as-built anchor bolt templates match foundation drawings and column base plates.
- Pre-staged spares and critical fasteners: ensure quantity and part numbers for long-lead replacement parts are delivered with the first shipment.
- Handover packs: as-built drawings, operation and maintenance manuals, torque charts, and spare parts lists.
- Installer training: evidence of installation manuals, training materials, and factory-led installation trials if required.
- Electrical interfaces for solar: site cable entry points, combiner box supports and cable routing provisions must match factory placements.
Operational documentation to require from factory:
- As-built BOM and drawings with revision control.
- Maintenance schedule and spare parts list with recommended stock levels.
- Warranty terms and claims process clearly stating which party is responsible for what scope and the claim submission procedure.
Important project caveat: the following items require a documented project basis and relevant local qualified professionals, installers, utilities and authorities: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty. Do not accept factory or supplier representations in place of local professional inputs.
Implementation risk: what commonly fails and how to mitigate it
Risk arises when one or more of the expected audit outcomes are absent or incomplete. Typical failure modes and mitigation measures are:
- Material substitution or undocumented changes
- Mitigation: require mill certificates and batch traceability; include hold points for material release.
- Dimensional drift between factory and site interfaces
- Mitigation: require pre-shipment dimensional reports, and sample part templates sent to site for verification.
- Inadequate packing leading to transit damage
- Mitigation: mandate packing trials, photographed packing records, and insurance conditions.
- Misunderstood delivery responsibilities
- Mitigation: use a delivery responsibility matrix tied to contract clauses and incoterm-based risk transfer.
- Non-conformances without corrective action
- Mitigation: inspect NCR history; require CAPA evidence and close-out before final acceptance.
- Unclear warranty scope and claims path
- Mitigation: include warranty schedules, exclusions and contact points in the purchase order.
- Logistics or customs delays
- Mitigation: ensure early coordination with freight forwarder, check customs classification and permits, and prepare contingency plans for redelivery.
Risk grading: use a three-tier matrix (High/Medium/Low) for each audit finding and require a supplier remediation plan with owner, timeline and verifiable evidence.
Example risk grading table
| Finding | Impact on project | Risk level | Immediate mitigation |
|---|---|---|---|
| No mill certificates for a lot | Potential structural non-compliance | High | Stop shipment; require third-party verification |
| Incomplete packing photos | Increased damage risk | Medium | Request packing trial and photo sign-off |
| Outdated calibration | Measurement errors in QA | Medium | Re-calibration before next lot; inspect previous lot tolerances |
| Minor cosmetic finish variance | Aesthetic concern only | Low | Record acceptance with buyer sign-off or rework plan |
Six-step buyer workflow for a carport supplier factory audit
The following named workflow is designed for purchasing teams to operationalise audits and integrate outcomes into project procurement controls.
- Define and document the audit brief (ScopeLock)
- Produce the technical scope comparison, contractual references, inspection plan and risk register. Include packing and logistics requirements.
- Pre-audit evidence exchange (EvidenceExchange)
- Request factory quality documentation, mill certificates, calibration records, packing specs and previous inspection reports. Grade sufficiency before scheduling.
- On-site factory audit (FactoryVerify)
- Execute the audit with checklists for material traceability, dimensional control, welding/assembly, coatings, and packing. Witness a sample assembly if possible.
- Non-conformance capture and remediation planning (NCRResolve)
- Log findings with severity grading. Require supplier CAPA with owners and timelines. Tie remediation to procurement hold points.
- Pre-shipment verification and packing sign-off (PackApprove)
- Verify packing trials, container stowage plans and export docs. Confirm logistics readiness and update the delivery responsibility matrix.
- Handover & close-out into operational controls (HandoverClose)
- Receive as-built documentation, spare parts, O&M manuals and training records. Update maintenance inventories, warranty registers and procurement records.
This named workflow, when enforced through your procurement system, becomes the backbone of project procurement controls and reduces downstream defects, delays and disputes.
Frequently asked questions (FAQ)
Q: What is the single most important thing to confirm during a carport supplier factory audit? A: Evidence that the factory can reproduce the project-specific technical scope consistently: dimensional tolerances, material traceability and packing methods tied to the purchase order.
Q: How does a factory audit differ from an ISO certification? A: ISO or similar certifications indicate a management system; a factory audit verifies project-specific processes, records and deliverables against the buyer’s technical and contractual requirements [2].
Q: Should I require third-party testing or inspectors? A: Use third-party inspections where internal trust is low, for critical structural lots, or where local authorities or financiers require independent verification. Third-party inspectors provide an auditable trail for procurement and warranty triggers.
Q: Who signs the delivery responsibility matrix? A: Both parties should sign or formally accept the matrix: the supplier takes responsibility for the activities it commits to, and the buyer must coordinate site tasks. Use Incoterms as the legal reference for risk transfer [3].
Q: What about packing for international shipments? A: Export packing coordination must be explicit: packing materials, crate strength, container egress, and any phytosanitary or fumigation requirements. Include container stuffing diagrams and responsibility for damages during transit.
Q: Can the factory audit replace local approvals? A: No. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities. The factory audit complements, but does not replace, those responsibilities.
Q: What if the supplier cannot supply required evidence? A: Treat missing evidence as a contractual non-conformance. Escalate via procurement controls: hold shipments, require third-party certification, or re-negotiate remedy terms. Decisions should be recorded and approved by project leadership.
Mid-article action If you need a standard audit checklist tailored to aluminium carports, commercial solar carports or vehicle shelters, request a project-specific pack through /inquiry. For technical alignment with Carportiva products, review the Carportiva system range and compare with your technical scope.
Integrating audit findings into contract, logistics and operations
Translate audit findings into contractual language and operational plans. Specific clauses to consider:
- Hold points and release conditions: Define which documents must be provided and accepted before shipment release (e.g., mill certificates, calibration, packing photos).
- Liquidated damages or remedies for late delivery: tie to milestones and evidence of factory readiness.
- Warranty and spare parts obligations: specify quantity, lead time and who bears shipping costs for spare components.
- Inspection clauses: define rights for buyer witness inspections or third-party inspectors and the consequences of rejected lots.
- Returns and remediation: establish a clear process for returning or repairing non-conforming items, including responsibilities for travel, labour and customs.
Logistics integration:
- Align packing specs with your forwarder and the destination port/terminal handling rules.
- Confirm customs classification and required permits; provide draft export documents for pre-clearance.
- Establish an agreed escalation procedure for damaged or delayed shipments, including insurance claims and acceptance testing at site.
Operations integration:
- Ensure training for installers is scheduled and documented; include factory-led supervision for first arrays where warranted.
- Update maintenance systems with BOMs, torque charts and recommended spare parts.
- Clarify escalation and contact points for warranty claims, and set SLAs for first response.
Conclusion: how audit evidence protects project outcomes
A carport supplier factory audit is an essential component of B2B supplier due diligence. It converts supplier claims into verifiable evidence (factory quality documentation, test records, packing trials) and ties them to the contractual mechanisms that control delivery, quality and risk. Use structured deliverables — a technical scope comparison, a delivery responsibility matrix, and documented project procurement controls — to manage the audit outcome and reduce the probability of defects, delays and disputes on site.
Remember: an audit is only effective if its findings are integrated into contract clauses, logistics plans and installation procedures. Maintain version control for the technical scope comparison and ensure that site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty are handled by local qualified professionals and authorities on a documented project basis.
For product-specific alignments and to see how Carportiva systems map to typical audit checkpoints, compare your scope against all systems or consult our sourcing guides. For procurement assistance or to request a tailored audit checklist, contact info@carportiva.com.
Further reading and references
- Hot-dip galvanizing and best practice guidance: American Galvanizers Association [1]
- Management systems and standards context: International Organization for Standardization [2]
- Risk and responsibility in commercial shipment terms: International Chamber of Commerce Incoterms [3]
- Export documentation and customs guidance: U.S. Customs and Border Protection [4]
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion