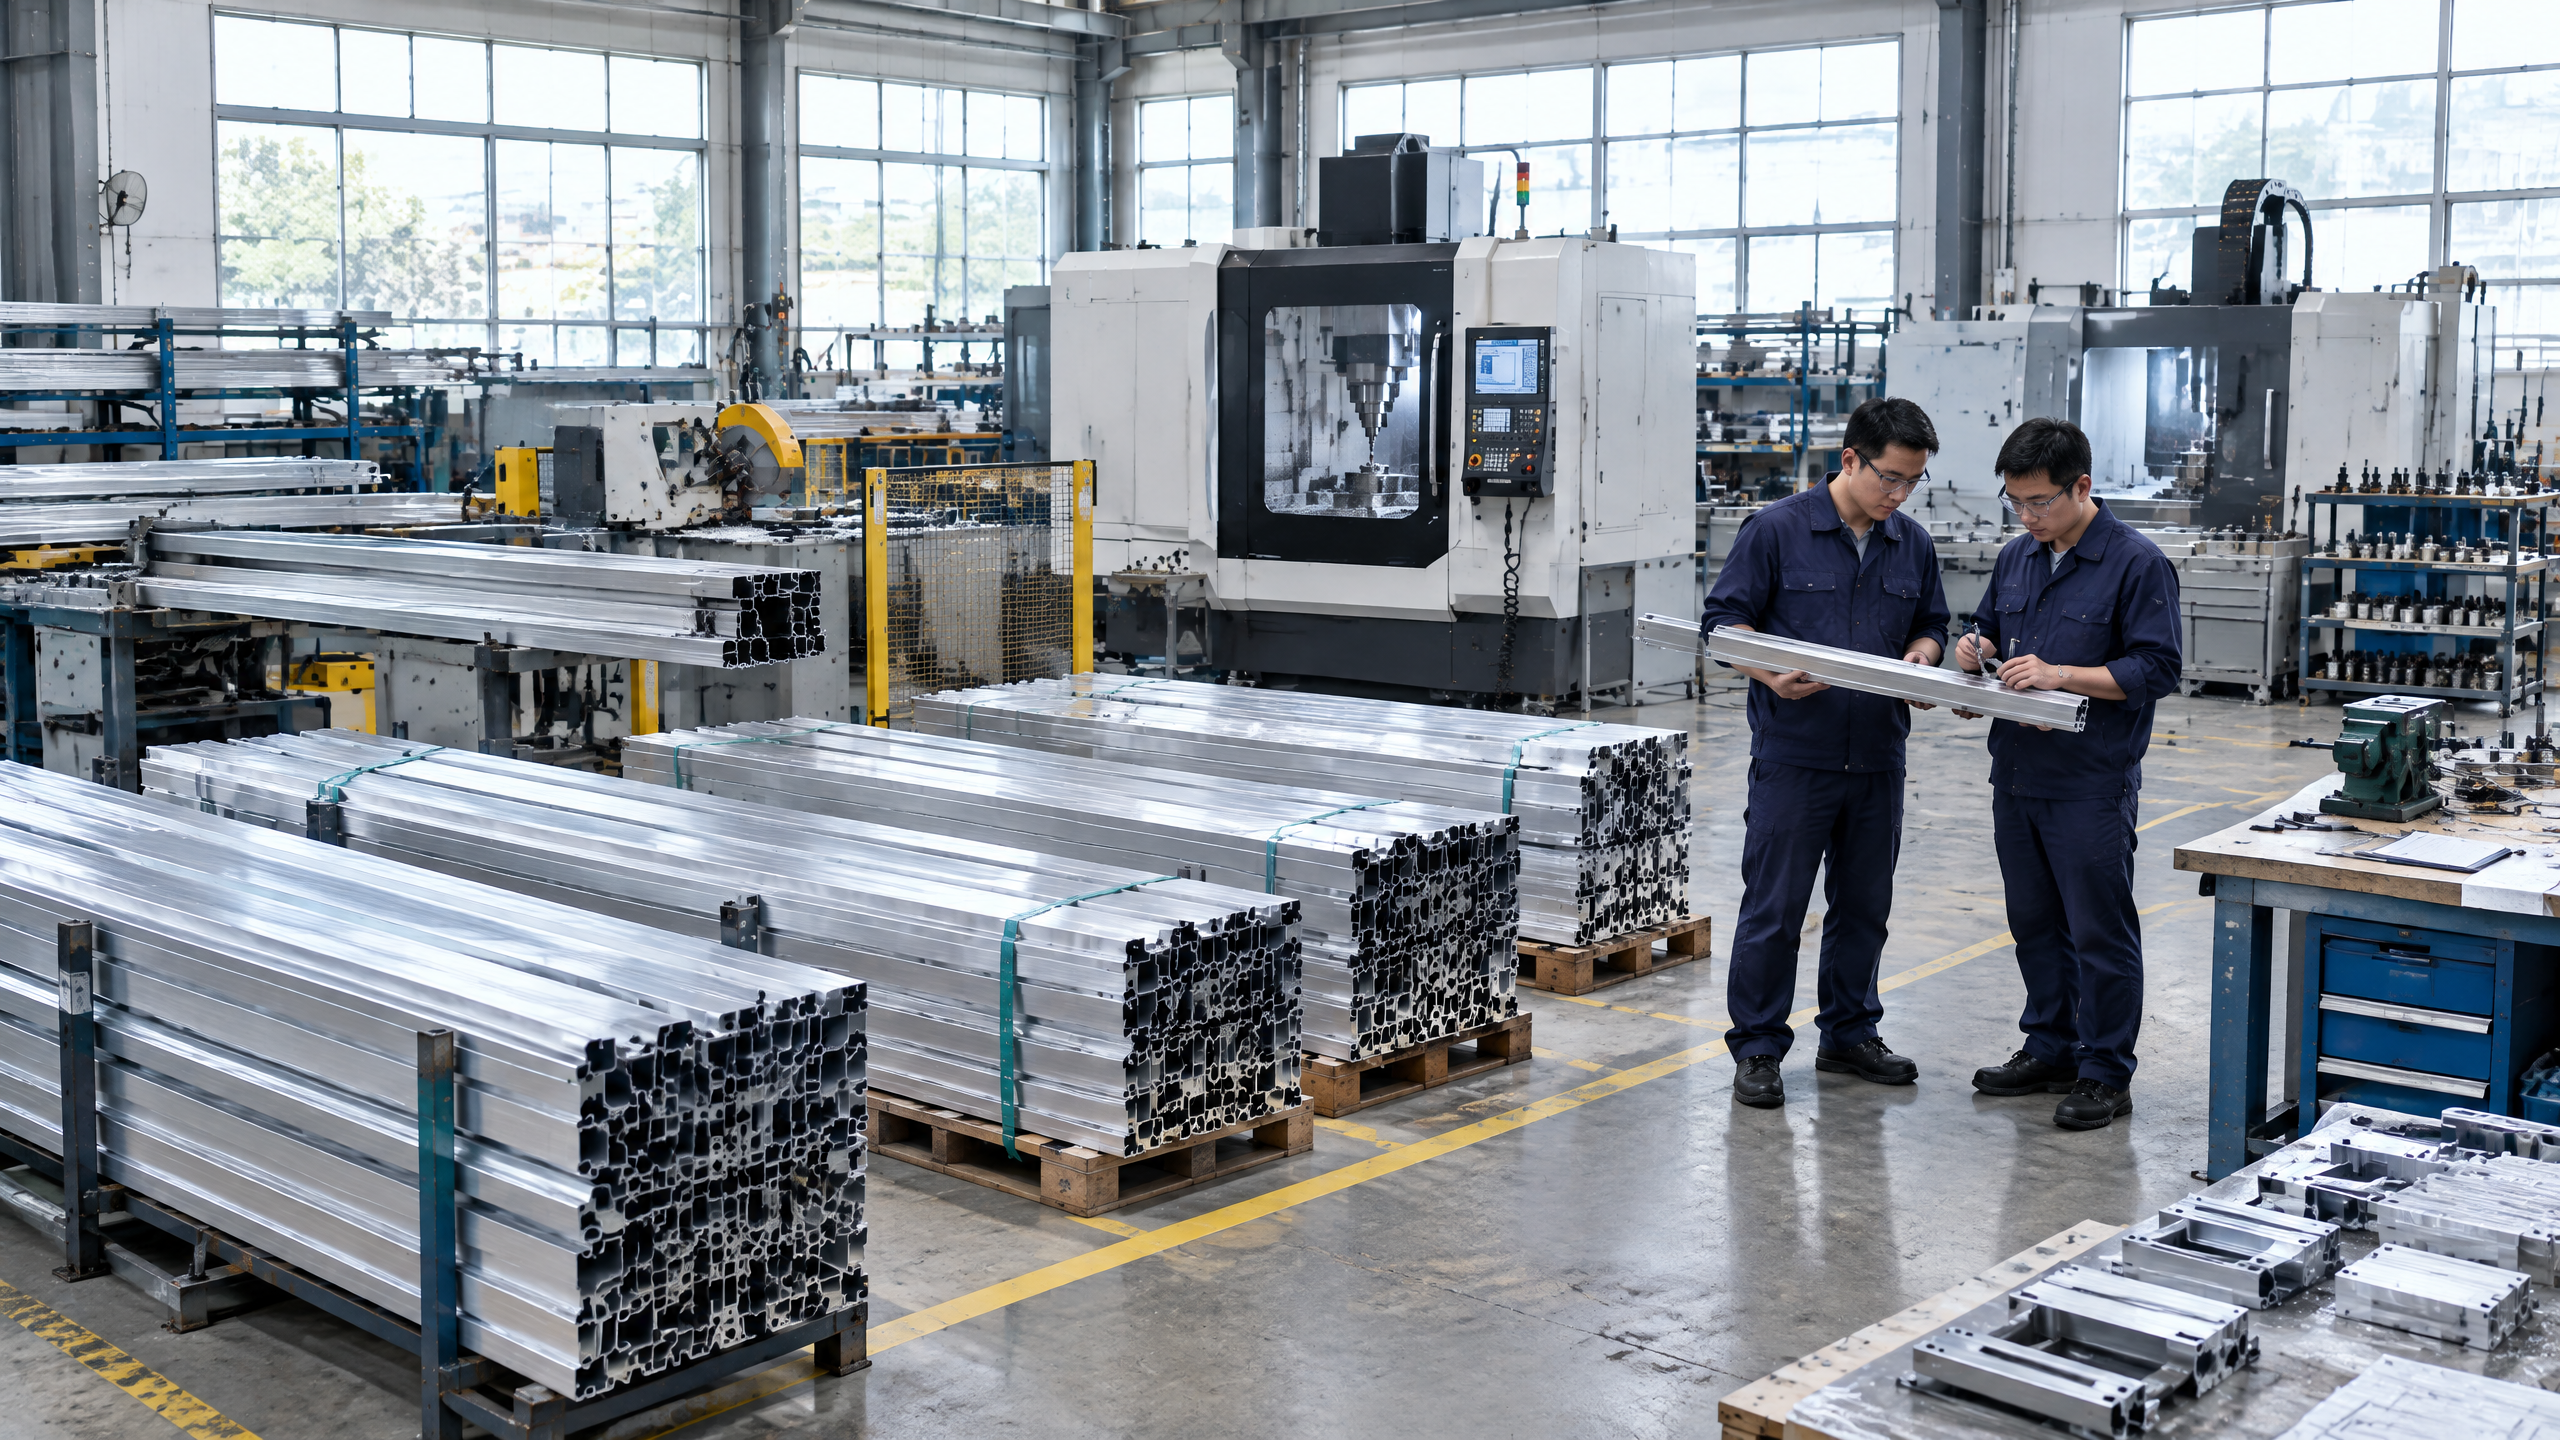
A carport wholesale container order requires decisions that span design, manufacturing, logistics and on-site installation. The immediate question for a buyer is not only “Is the price competitive?” but “Does the proposal deliver the documented technical scope, verifiable factory quality, transportable packing and a clear allocation of responsibilities across the supply chain?” This guide focuses on practical evidence you should require to convert a commercial quotation into an executable procurement package for aluminium carports, solar carports and fleet shelters. It explains which documents, tests and contractual terms materially reduce execution risk; how to compare technical scopes; how to audit factory output and export packing; and how to set project procurement controls so a single container order can be scaled and integrated reliably into a construction or EPC programme. Use this guide to build a defensible purchasing decision and a delivery responsibility matrix that aligns price, schedule and warranty obligations with your project’s execution constraints.
Buyer context and scope boundary
Why a targeted procurement approach matters
- Carport wholesale container order decisions affect structural, electrical and site-delivery outcomes across multiple stakeholder groups: distributors, architects, contractors, developers, solar EPCs and fleet operators.
- A typical container order aggregates hundreds of discrete parts (posts, beams, fasteners, solar mounts, glazing, ancillaries) and interface specifications that must be documented, reconciled with local code and installed by competent teams.
- The commercial quotation is only the start. Buyers must translate supplier proposals into a documented project basis with defined responsibilities, acceptance criteria and handover processes.
Define the procurement boundary early
- Product scope: Which specific Carportiva profiles, mounting systems and accessories are included? See the Carportiva system range for system-level references and options.
- Supply boundary: Which items are supplied factory-installed (pre-assembled modules, kits), which are loose-packed, and which remain local scope (foundations, electrical connection, final testing)?
- Logistics and customs: Are the goods shipped to a port, an inland depot or delivered door-to-door? Clarify Incoterms early to avoid ambiguity in the delivery responsibility matrix [3].
- Installation boundary: Which tasks are to be performed by the supplier’s nominated installer, by the buyer’s contractor, or by third parties (e.g., electrical contractors, civil works providers)?
Required project documentation to fix scope
- Detailed bill of materials (BOM) with part numbers and quantities.
- Assembly drawings and exploded views for shipped kits.
- Foundation layouts keyed to local soil and structural conditions.
- Electrical interface schedules for solar carports (if applicable).
- Factory QA/QC checklist and acceptable non-conformance criteria.
Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Core decision principle: evidence over assumption
Make decisions on documented evidence rather than assumptions
- Evidence reduces ambiguity: a BOM linked to drawings, factory quality records and a defined export packing plan convert price comparisons into comparable deliverables.
- Risk is a transfer and mitigation exercise: lower unit price that transfers risk without documentation often increases total project cost. Conversely, higher unit price with verified factory quality documentation and clear lead times can reduce schedule and rework risk.
- Focus on outcomes: ask whether the order, once landed and unpacked, will allow the site team to install, commission and hand over the asset without supplier-dependent clarifications.
Essential evaluation questions
- Does the supplier provide a clear technical scope comparison between tender options?
- Are the factory quality assurances traceable (material certificates, galvanizing reports, inspection checklists)?
- Is export packing coordinated to protect finished profiles and ensure customs compliance?
- Do Incoterms align with your logistics capability and local import requirements?
- Is there a delivery responsibility matrix that maps risk and cost through delivery to site?
Keywords to embed into procurement governance
- Require a "technical scope comparison" and a "delivery responsibility matrix" in all proposals.
- Build "project procurement controls" into the contract to lock acceptance criteria, inspections and release milestones.
Planning inputs: information to gather before issuing RFQ
Accurate planning inputs reduce ambiguous bids
- Site coordinates and constraints: access routes, crane availability, storage footprint, lift points, prevailing winds and edge-clearances.
- Local structural and geotechnical report: necessary to specify foundation types (pad, pile, bolt-down) and embed plate details.
- Electrical information (for solar carports): local utility interconnection conditions, inverter locations, DC/AC routing, earthing and lightning protection requirements.
- Local approvals and permits: timeframes, documentation needed, and any delegated responsibilities.
- Schedule constraints: critical milestones for fleet handover, construction sequencing or solar commissioning.
Minimum RFQ documents checklist
- Performance specification: load design criteria, wind and snow loads, corrosion environment class.
- BOM template: allow suppliers to fill in part numbers and supply options.
- Interface drawings: foundation grid and roof elevation to check module and rafter fit.
- Packing and export requirements: container loading diagrams, stacking limits, and palletization expectations.
- Acceptance testing: site inspection protocol, factory witness inspection scope.
Use the planning inputs to create a fair "technical scope comparison" matrix to ensure apples-to-apples evaluation of competing bids.
Technical specification and interfaces
What to include in the specification
- Structural design basis: reference international or national codes that will govern structural calculations (e.g., Eurocodes, ASCE, local code). Ask for the design load assumptions used in manufacturer calculations.
- Material specification: aluminium alloy grades, structural yield strength, anodizing or powder-coat systems, fastener metallurgy and corrosion protection.
- Solar interface (if applicable): module mounting interface, tilt angle, stringing strategy, cable routing, combiner box and inverter adjacency points.
- Connection details: bolt grades, torque specifications, and recommended thread-lock or anti-corrosion measures.
- Tolerances and fit-up: fabrication tolerances that will affect field assembly (hole patterns, profile lengths).
Interfaces that commonly cause disputes
- Foundations: If the supplier’s drawings assume a given embedment or bolt pattern, reconcile with local soil capacity. The supplier’s foundation detail must be stamped or validated by a qualified local engineer.
- Electrical handover points: Define whether the supplier supplies DC/AC wiring to string combiner, or whether the electrical contractor provides final cabling and testing.
- Roof finishes and drainage: ensure water routing and roof edge flashings are compatible with site drainage and building façades.
Technical scope comparison: a simple decision table
| Item | Buyer baseline requirement | Supplier A response (tick if meets) | Supplier B response (tick if meets) |
|---|---|---|---|
| Structural design basis & load report | Required | ✅ | ✅ |
| Aluminium material grade specified | Required | ✅ | ❌ (proposed alternate) |
| Galvanizing/coat system documented | Required | ✅ (doc provided) | ✅ (doc pending) |
| Foundation drawings included | Required | ❌ (buyer to supply) | ✅ (standard layout) |
| Solar mounting interface drawings | If solar | ✅ | ✅ |
Notes on material and corrosion protection
- For hot-dip galvanizing of steel components or fasteners, consult recognized practices for coating thickness and inspection (see American Galvanizers Association) [1]. Galvanizing inspection reports are commonly part of factory quality documentation.
- For aluminium finishes, ask for detailed coating system data sheets and accelerated weathering procedures used by the coating supplier.
When to involve professional reviewers
- Structural calculations, foundation designs and electrical interconnection must be reviewed and stamped by locally qualified professionals before procurement sign-off.
- If the carport is part of a larger construction interface (e.g., façade tie-ins, rooftop carparks), involve the detail designers early to prevent rework.
Procurement and factory evidence: what to require and why
What evidence materially reduces execution risk
- Factory drawings and shop drawings with revision control: ensure bolt patterns and part counts are verifiable.
- Factory quality control (FQC) records: dimensional inspection, weld records and non-conformance logs.
- Factory inspection and test plans (ITP): the ITP should map activities to inspection points, witness points and hold points.
- Material test certificates (MTCs): raw material certificates for structural aluminium alloys and steel fasteners.
- Surface treatment records: coating batch numbers, paint film thickness measurements, anodizing certificates or pre-treatment logs.
- Packing and container loading plan: to confirm that profiles are protected, that weight distribution in container is safe and that any oversized items are documented for permit handling.
Factory evidence decision table (example)
| Evidence type | Why it matters | Acceptable buyer action |
|---|---|---|
| Shop drawings with mark numbers | Ensures on-site assembly matches delivered parts | Require sign-off prior to production |
| Material test certificates (MTCs) | Verifies material grade and mechanical properties | Require submission with first shipment |
| ITP with witness points | Allows buyer / third-party inspections at critical stages | Insert witness/hold points in contract |
| Coating thickness and adhesion reports | Corrosion resistance and warranty basis | Require batch reports with coating labels |
| Packing & loading plan | Prevents transport damage and customs delays | Approve prior to container loading |
B2B supplier due diligence checklist
- Corporate and legal: company registration, export license, export packing coordination capability and references for container shipments.
- Financial: payment terms, trade finance options, and verified bank details (avoid reliance on unverifiable accounts).
- Production capacity: confirmed lead times, workshop photos, and recent production cadence for similar container volumes.
- Quality systems: request factory quality documentation (ISO-style QMS records, inspection logs) and any third-party inspection reports.
- Logistics competency: documented ability to handle sea container bookings, fumigation or phytosanitary requirements, and export packing coordination for stowage and protection.
Using third-party inspection and audits
- Third-party inspection (TPI) at the factory provides objective verification of adherence to specifications. Define scope in your purchase order: hold/witness points, destructive tests (if required), and acceptance criteria.
- Use a standard report format so supplier responses are comparable. Require the inspector to reference drawing revision and mark numbers.
Contractual levers and "factory quality documentation"
- Make submission of factory quality documentation a contractual milestone tied to staged payments.
- Require supplier to maintain traceability of parts to production batches and packing units to reduce dispute risk on site.
Caveat: do not assume certifications are equivalent to project compliance. Ask for relevant documents and verify in context.
Export packing, coastal logistics and delivery responsibility matrix
Export packing coordination
- Export packing must protect finished surfaces and maintain part identification for rapid field assembly. A good packing plan will include:
- Piece marking and packing lists keyed to shop drawings.
- Cushioning and bracing inside containers.
- Weatherproof wrapping for coated surfaces and electrical components.
- Palletization rules and lashing points to prevent shifting.
- Confirm whether the supplier uses container dunnage or timber bracing and whether phytosanitary certificates are needed for wooden pallets in the destination market.
Delivery responsibility and Incoterms
- Specify Incoterms explicitly in the contract and confirm allocation of risk, cost and responsibility for export documentation, customs clearance and inland delivery. Use the ICC Incoterms rules as the reference framework [3].
- Reference in the delivery responsibility matrix who handles loading, export documentation, insurance, import duties and final delivery to the site.
Delivery responsibility matrix (example)
| Responsibility | EXW | FOB | CIF | DAP |
|---|---|---|---|---|
| Seller arranges export packing | ✓ | ✓ | ✓ | ✓ |
| Seller loads container at factory | ✓ | ✓ | ✓ | ✓ |
| Seller arranges main carriage | ✗ | ✗ | ✓ | ✓ |
| Seller arranges customs export clearance | ✗ | ✓ | ✓ | ✓ |
| Seller arranges import clearance/ duties | ✗ | ✗ | ✗ | ✗* |
| Buyer arranges on-site offloading | ✓ | ✓ | ✓ | ✓ |
*Under DAP the seller delivers to an agreed place and assumes export customs clearance, but import clearance and duties typically remain buyer responsibility unless specifically agreed.
Customs and import documentation
- For importing into the United States, consult CBP guidance for required documentation, classification and valuation [4]. For other destinations, ensure supplier coordinates with your nominated freight forwarder or customs broker.
- Ask the supplier to provide a pre-shipment packing list, commercial invoice, certificate of origin and any required test certificates.
Insurance and damage protocol
- Define who insures the goods at what stage and how damage claims will be handled. For high-value shipments, consider cargo insurance that covers war, theft and marine perils.
Site installation, commissioning and operations
Preparing the site
- Prior to arrival of the container(s), confirm foundations are cast and dimensions and anchor patterns are within fabrication tolerances. If bolt cages are used, verify position tolerances before shipping.
- Confirm the site has adequate storage space, protection from the elements and security for staged assemblies.
- Plan lifting and access: determine crane or telehandler capacities and the required slings and spreader beams for large assemblies.
Receiving and unpacking procedures
- Implement an unpacking checklist that traces delivered parts to the shop drawing mark numbers and identifies damaged or missing items.
- Use the factory packing lists and shop drawings to expedite the inventory reconciliation process.
Assembly and quality acceptance
- Ensure installers have access to the correct torque settings, dihedral and camber tolerances, and bolt pre-tightening sequences specified in the supplier’s installation manual.
- Define final acceptance tests: plumb/level verification, torque re-checks, and functional checks for moving parts or drainage.
- For solar carports, perform electrical continuity, insulation resistance tests and inverter commissioning in alignment with the electrical contractor and local interconnection rules.
Maintenance and operations handover
- Obtain maintenance manuals, spare parts lists and the recommended schedule for inspections (e.g., annual fastener checks, re-torquing schedule, and surface repair instructions).
- Clarify warranty claim processes and the required evidence package for any claim (photos, serial numbers, installation records).
A critical reminder
- site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risks and mitigation strategies
Common implementation risks with container orders
- Scope mismatch: missing items, wrong finishes or incomplete interfaces.
- Packaging damage: insufficient protection leading to surface damage or bent profiles.
- Lead-time slippage: factory backlogs or shipping delays cause programme disruptions.
- Customs hold-ups: incorrect documentation, classification disputes or non-compliance with import rules.
- On-site incompatibility: foundation bolt positions or dimensions not matching delivered components.
Mitigation strategies
- Use staged approvals: shop drawing approval, pre-production sample or prototype, and pre-shipment inspection (PSI).
- Hold payment milestones to deliverables: material release after PSI and documentation submission.
- Nominate a freight forwarder early and verify import document requirements per destination with a customs broker.
- Implement a delivery responsibility matrix into the PO to define who pays for extra demurrage, rework or returns.
- Require clear marking and part numbering to accelerate site reconciliation and reduce idle workforce waiting.
Risk allocation checklist
- Who accepts risk for hidden shortages discovered on-site within X days?
- Who bears the cost of remedial transport for missing parts?
- If rework is needed due to incorrect drawings, who bears engineering and production costs?
- How will force majeure be handled and what notification windows apply?
Legal and contractual controls
- Include a dispute resolution clause that specifies governing law and an escalation path.
- Consider performance bonds or a letter of credit for high-value, multi-container orders where supplier reliability is unproven.
Six-step buyer workflow for a compliant carport wholesale container order
This named workflow integrates the evidence and controls discussed above into a practical procurement process.
Step 1 — Project Basis and RFQ Preparation
- Collect site surveys, geotechnical and electrical pre-requisites.
- Issue RFQ with a detailed BOM template, required drawings and explicit Incoterm.
- Require suppliers to provide a technical scope comparison against your baseline.
Step 2 — Supplier Shortlist and B2B supplier due diligence
- Conduct supplier checks for export packing coordination, production capacity and factory quality documentation.
- Request references for similar container shipments and third-party TPI capability.
Step 3 — Technical Clarification and Shop Drawing Sign-off
- Approve material choices and finish specifics.
- Sign off shop drawings and mark numbers with revision control before production starts.
Step 4 — Factory Production Oversight and Pre-shipment Inspection
- Implement ITP with key witness points and final pre-shipment inspection.
- Obtain MTCs, coating reports and a packing/loading plan.
Step 5 — Logistics Execution and Delivery Responsibility Matrix Activation
- Confirm container bookings, cargo insurance and customs arrangements.
- Use the delivery responsibility matrix to track transfers of liability and cost.
Step 6 — Receiving, Assembly, Commissioning and Handover
- Reconcile unpacked parts to shop drawings and address any shortages/damages per contract.
- Perform installed acceptance tests and lodge warranty records and maintenance manuals.
Contractual controls to include at each step (project procurement controls)
- Milestone-based payments linked to documentary evidence (approved shop drawings, MTCs, PSI report).
- Retainage or warranty hold-back until final acceptance.
- Defined response times and remedies for missing or non-conforming items.
Links for further reference
- Start by reviewing the Carportiva system range to confirm system options and interfaces, then consult all systems and our sourcing guides for template documents.
Mid-article call to action If you need project-specific documentation or clarification about Carportiva systems, open an inquiry: /inquiry or email info@carportiva.com.
Frequently asked questions (FAQ)
Q: How do I compare two container quotes where one is cheaper? A: Don't compare price alone. Require both suppliers to complete a technical scope comparison and submit factory quality documentation, packing plans and a delivery responsibility matrix. Lower price may exclude critical deliverables or transfer risk to your team, increasing total cost.
Q: What inspection points should I mandate during production? A: At minimum: material verification on receipt, dimensional checks at the mid-production stage, weld and assembly checks, coating inspections, and a pre-shipment inspection that confirms packaging and part counts.
Q: Should I insist on third-party inspection? A: For large or unfamiliar suppliers, third-party inspection reduces asymmetric information. Specify the inspector scope and acceptance criteria in the contract.
Q: How are Incoterms relevant to a carport wholesale container order? A: Incoterms determine who arranges and pays for transport, insurance and customs at each stage. They are central to the delivery responsibility matrix and reduce disputes over loss, damage and demurrage [3].
Q: Can the supplier design foundations for local conditions? A: Suppliers may provide generic foundation drawings, but for site-specific structural capacity and geotechnical issues you must obtain local professional certification and designer sign-off. site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Q: What paperwork should arrive with the shipment? A: Common documents include commercial invoice, packing list, bill of lading, certificate of origin, MTCs, coating reports and pre-shipment inspection certificate. For imports into specific countries, consult local customs guidance (e.g., CBP for the U.S.) [4].
Q: How should warranty claims be handled? A: Define warranty scope and claim procedures, required evidence, timelines and repair/replace remedies in the contract. Keep a record of shop drawings, MTCs, installation records and acceptance certificates as part of warranty evidence.
Conclusion
A carport wholesale container order is not a single commercial transaction — it is a sequence of technical and logistical commitments that must be aligned with your project’s schedule and local constraints. The most effective B2B decisions are evidence-led: require a technical scope comparison, insist on factory quality documentation, formalize export packing coordination, and build a delivery responsibility matrix into the agreement. Apply project procurement controls that tie payments to verifiable milestones and use third-party inspection where uncertainty exists. Finally, validate the design, foundations and electrical interfaces with local qualified professionals before final acceptance.
For project-specific guidance or to discuss how our product range can align with your procurement controls, contact us via /inquiry or info@carportiva.com.
References
- American Galvanizers Association — galvanizing practices and inspection guidance.
- International Organization for Standardization — for quality management context and standards referencing.
- International Chamber of Commerce Incoterms — rules that define delivery responsibilities and risk transfer.
- U.S. Customs and Border Protection import guidance — documentation and compliance considerations.
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion