Direct answer (120–180 words)
A carport wholesale manufacturer matters most when a B2B procurement decision depends on repeatable factory outputs, accountable delivery interfaces, and technical scope that affects cost, schedule and long-term operability. For distributors, architects, contractors, developers, solar EPCs and fleet operators the manufacturer becomes the critical party where: (1) product design and repeatable quality are central to risk allocation; (2) production lead times, export packing coordination and logistics drive schedule; (3) traceable factory evidence and warranty interface determine acceptability; and (4) integration with site civil, electrical and commissioning teams is required. In other cases — single bespoke structures, turnkey EPC projects, or when installation and warranties are primarily local — the manufacturer is one component among consultants, installers and EPCs. Use documented project inputs, clear technical scope comparison and contractual project procurement controls to decide how far upstream manufacturer responsibility must extend.
Buyer context and scope boundary
Who should use this guide
- Distributors procuring stock or made-to-order modular carport systems.
- Architects and contractors specifying systems into building projects.
- Developers and facility managers procuring for multi-site rollouts.
- Solar EPCs integrating PV into canopies and requiring predictable yields.
- Fleet operators and logistics hubs needing durable, maintainable shelters.
What “manufacturer matters” means in practice
- Responsibility: the manufacturer supplies finished assemblies, test evidence and packaging; may accept partial installation obligations.
- Control: specifying materials, tolerances and factory processes influences delivery quality.
- Risk allocation: when defects, delays or missing documentation would materially affect the project, the manufacturer’s role should be contractual and auditable.
Scope boundary examples
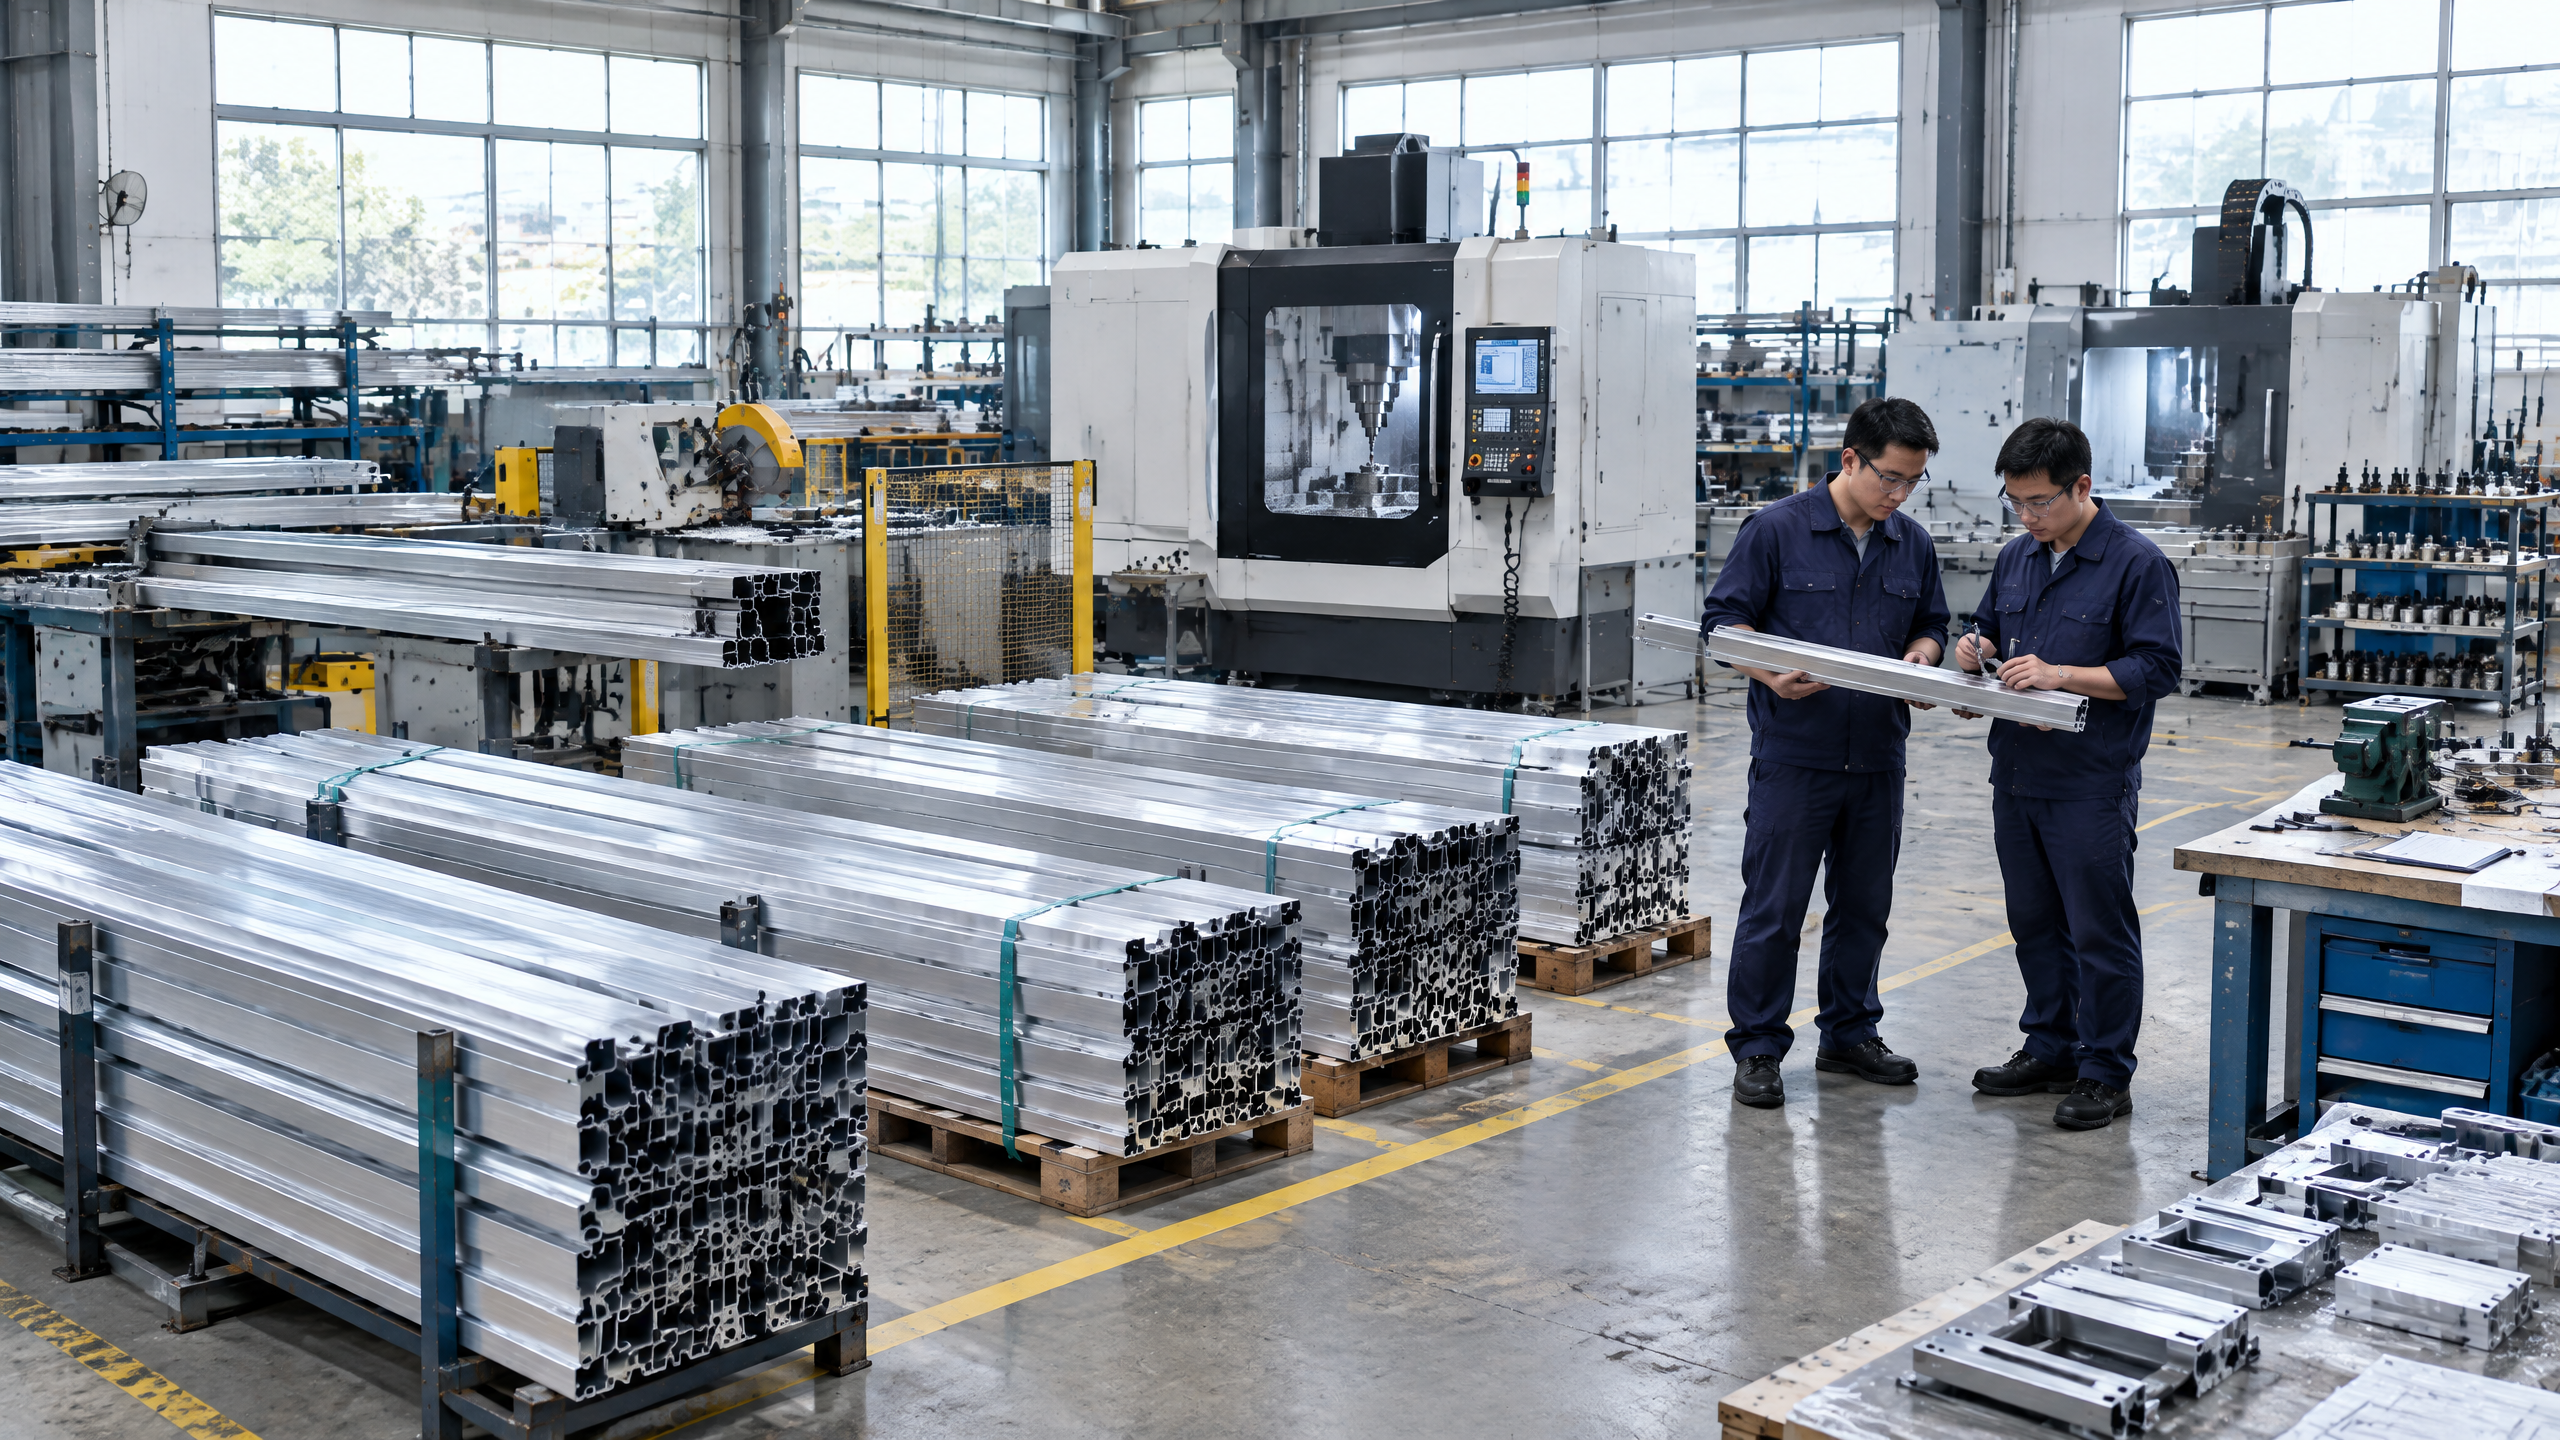
- Included from manufacturer: extruded aluminium members, powder-coating, pre-assembled module frames, factory-fitted PV racking (if specified), factory-applied corrosion protection, parts packing and export documentation.
- Typically outside manufacturer scope: foundations, local electrical wiring and grid connection, civil site works, final commissioning of PV generation (unless contracted), and local permits/approvals.
Note: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Core decision principle: when to make the manufacturer the primary contractual lever
For B2B buyers the core principle is this:
- Make the carport wholesale manufacturer the primary contractual lever when product consistency, factory traceability, and global logistics materially affect cost, schedule or long-term liability.
Practical thresholds where this applies
- Multi-site rollouts: You need reproducible assemblies and controlled lead times.
- Integrated solar canopies: Manufacturer must align mechanical design with PV racking and electrical interface.
- Architects specifying high-tolerance architectural finishes: Factory control of powder coat, anodizing, or joint tolerances matters.
- Long-term maintenance and warranty obligations: Factory traceability and documented quality systems reduce downstream uncertainty.
When not to centralize on the manufacturer
- One-off custom site builds where local installers and engineers are primary risk owners.
- Turnkey EPC contracts where the EPC accepts full delivery and warranty to the buyer and manages supplier relationships.
Planning inputs: the data that determines manufacturer importance
Essential project inputs (documented project basis)
- Scope of works and functional requirements (shelter type, canopy span, roof pitch, PV provision).
- Structural design criteria and applicable codes (local wind, snow, seismic loadings).
- Site survey and geotechnical information (bearing capacity, soil conditions).
- Architectural finish requirements (color, joint detailing, visibility of fasteners).
- Schedule milestones, acceptance criteria and commissioning gates.
- Lifecycle expectations, maintenance intervals and warranty duration.
- Logistic constraints (port access, import handling capacity, crane availability).
Stakeholder matrix
- Client / Owner: defines objectives, budget and O&M priorities.
- Architect / Consultant: specifies aesthetic and interface details.
- Structural Engineer: defines foundation and load criteria.
- EPC / Electrical Contractor: defines PV/electrical interfaces and commissioning.
- Local Installer: performs foundations, on-site erection and finishing.
- Manufacturer: supplies assemblies, packing, and factory QA evidence.
Project procurement controls Integrate project procurement controls into the planning phase: procurement milestones, document approval gates, supplier KPIs and dispute mechanisms. These controls should define when factory quality documentation is acceptable, the standards for shipping, and acceptance testing performed at site.
Technical specification and interfaces
Why technical specification matters Misaligned specifications lead to scope gaps, change orders and delayed handover. A clear technical scope comparison between supplier proposals reveals hidden assumptions about tolerances, finishes, and interfaces.
technical scope comparison Document, in parallel for each bid or manufacturer:
- Primary materials and grades (aluminium alloy, fastener grade, coatings).
- Structural member profiles and connection details.
- Design load assumptions and calculation deliverables.
- Surface finish (powder coat, anodize, galvanize where used).
- Prefabrication level (fully pre-assembled modules vs. kit-of-parts).
- PV integration provisions (racking interface, cable routing, junction box positions).
- Interface provisions for foundations and electrical work.
Decision table — technical scope comparison (example)
| Topic | Manufacturer A (factory-focused) | Manufacturer B (component-focused) | Buyer implication |
|---|---|---|---|
| Prefab level | Pre-assembled canopy modules, factory bolted | Kit-of-parts requiring significant site assembly | Pre-assembly reduces site time but needs larger transport and crane capacity |
| Structural calculations | Supplier provides stamped calculations for superstructure | Buyer/engineer expected to produce all site-specific calculations | Determine who supplies stamped deliverables and certificates |
| PV interface | Integrated racking rails, factory routing pockets | PV supplier mounts to generic top rails on-site | Interface responsibilities must be contractually clear |
| Surface finish | Multi-stage application with factory QA | Single-stage treatment with local touch-up expected | Inspect factory quality documentation and sample panels |
Design interfaces to lock-in
- Foundation interface details: anchor type, plate size, grout tolerance.
- Electrical interfaces: string inverter location, DC/AC cable entry, earthing points.
- Drainage and water run-off: ensure canopy pitch and gutter details are specified.
Standards and materials
- Aluminium alloys and anodizing: define alloy series and treatment requirements.
- Corrosion protection for any galvanised components: reference best practices and guidance (see galvanizing guidance) [1].
- Manufacturing quality systems: require supplier quality plans that reference internationally recognised standards when applicable (e.g., ISO 9001) [2].
Procurement: evidence, audits and documentation
B2B supplier due diligence B2B supplier due diligence should include corporate, financial and operational checks:
- Legal entity verification, insurance limits and export license status.
- Financial stability checks to assess continuity risk for long-lead orders.
- Production capacity and lead-time confirmation against demand profile.
- Reference projects and client contacts (verify, do not rely solely on supplier claims).
- Local agent or representative presence for after-sales support.
Factory quality documentation Require the manufacturer to provide factory quality documentation that maps to the purchase contract:
- Material mill certificates and traceability records.
- Welding procedure specifications, welder qualifications and NDT reports (if applicable).
- Coating application records and thickness measurements.
- Dimensional inspection reports and assembly checklists.
- Final inspection and pack-off certificates.
Factory evidence decision table
| Evidence type | Minimum acceptable form | Why it matters |
|---|---|---|
| Material certificates | Mill test reports with traceability | Traceability to alloy/grade ensures expected mechanical and corrosion properties |
| Coating records | Batch report, thickness measurement, adhesion test | Coating defects are frequent warranty issues; factory control reduces risk |
| Dimensional inspection | Control plan with as-built measurements | Ensures field fit with foundation plates and pre-drilled holes |
| Packing list & photos | Pre-shipment photos and detailed pack list | Confirms content and packing method for export claims |
Audit types and frequency
- Desktop audit: review documentation and processes remotely before sample order.
- Witness testing: attend factory testing or third-party testing for critical items.
- Full-site audit: inspect production lines, processes, storage and QA systems before full production runs.
Quality systems and standards
- Where relevant, seek suppliers that can demonstrate adherence to formal quality systems such as ISO 9001; audit evidence should demonstrate translation of that system into project-level procedures [2].
- For corrosion protection and galvanizing practices, validate that supplier practices align with recognized industry guidance [1].
Contractual quality clauses
- Define acceptance tests, hold points and non-conformance management.
- Specify remedial actions, replacement rules, and dispute resolution mechanisms.
- Require documented factory quality documentation before releases or commercial milestones.
Export packing, logistics and delivery responsibility
Export packing coordination Export packing coordination must be contractual when goods leave the factory. Specify:
- Packing method (crates, frames, bulk pallets), packing materials and dunnage.
- Lashing points and load restraint for long-haul shipping.
- Packaging dimensions and weights for booking and port handling.
- Special instructions for oversized or out-of-gauge shipments.
Reference guidance for export/import procedures
- Incoterms define who delivers, insures and clears at each stage; select and agree terms early [3].
- For import handling and documentation, align with local customs and authority expectations; U.S. importers should refer to official guidance for recordkeeping and packing for compliance [4].
Export packing coordination table — packaging options and suitability
| Packaging type | Typical use | Advantages | Constraints |
|---|---|---|---|
| Crated assemblies | Smaller pre-assembled modules | Protection, weather resistance, easier stacking | Increased volume and cost |
| Steel frame skids | Long extruded members | Secure restraint, reusable frames | Heavier, may need special handling |
| Bulk banded on pallets | Components or small parts | Cost-efficient, flexible | Less protection from impact and corrosion |
| Containerised | Fully packed into containers | Secure, standardized handling | May require break-bulk for oversized elements |
Delivery responsibility matrix A clear delivery responsibility matrix allocates tasks from factory to site. Use this to avoid handover disputes.
Decision table — delivery responsibility matrix (example)
| Activity | Manufacturer | Freight Forwarder / Shipper | Buyer / Local Agent | Notes |
|---|---|---|---|---|
| Pack goods for export | X | Manufacturer supplies packing per agreed specifications | ||
| Obtain export paperwork (commercial invoice, packing list) | X | Manufacturer prepares originals for handover | ||
| Inland transport to port | X or Buyer (depends on Incoterm) | X | Incoterm determines responsibility | |
| Export customs clearance | X (if appointed) | Otherwise handled by forwarder/agent | ||
| Marine/air carriage | X | Forwarder arranges carriage per booking | ||
| Import customs clearance | X or buyer's agent | Buyer responsible unless DDP agreed | ||
| Unloading at site | X | Crane, storage, and site handling by buyer or nominated installer | ||
| Unpack and inventory check | X (recommend manufacturer oversight) | Inspect immediately for transport damage | ||
| On-site assembly supervision | Optional | X (may be manufacturer-assisted) | Agree supervision scope in contract |
Incoterms, insurance and risk transfer
- Agree the transfer point of risk and responsibility using Incoterms [3]. Be explicit about insurance cover and claims handling.
- For complex projects consider CIF or CPT for sea/air carriage and clear local clearance responsibilities separately.
Customs and documentation
- Require manufacturer to provide complete commercial invoices, packing lists, certificates of origin and any other regulatory documents required for clearance [4].
- Where export licences or special inspections are required, plan lead times accordingly.
Site installation, commissioning and operations
On-site integration responsibilities Define who will provide:
- Foundations and concrete works sized to manufacturer-supplied anchor plates.
- Crane and lifting equipment for placing pre-assembled units.
- Local installers and welding/bolt torque verification.
- Electrical contractors for PV connection, inverter installation and earthing.
Installation quality controls
- Pre-installation checks: inventory, damage inspection, dimensional check of anchor bolts and plate alignment.
- Hold points: before bolting, verify correct sequence and torque; before commissioning, verify electrical continuity, earthing, and PV string integrity (if applicable).
- Punch-list and acceptance: define completion criteria and handover documents.
Operational commissioning and handover
- Commissioning tests: visual inspections, mechanical alignment checks, PV electrical tests (IV curves, inverter commissioning) — note that PV commissioning is normally carried out by qualified electrical professionals.
- Handover pack: as-built drawings, factory quality documentation, maintenance manuals, spare parts list and warranty certificates.
Maintenance and spare parts
- Agree minimum spare parts list for first-year maintenance and lead times for replacement components.
- Define preventive maintenance schedules for mechanical checks and coating inspections.
Important compliance reminder site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Implementation risks and mitigation
Common implementation risks
- Production quality variance: batch differences in coatings or extrusions.
- Lead-time slippage: factory backlog, raw material shortages, or shipping delays.
- Damage in transit: improper packing, poor handling, or inadequate stowage.
- Interface failure: misaligned anchor patterns or undeclared site conditions.
- Regulatory hold-ups: local approval delays or import inspection holds.
- Warranty disputes: unclear responsibilities for corrosion, paint failure, or structural defects.
Mitigation strategies
- Contractually require factory quality documentation and preshipment inspection reports.
- Insert schedule buffer for production and shipping; include supplier penalties or liquidated damages if appropriate.
- Insist on pre-shipment photos and, for critical shipments, third-party inspection or witness testing.
- Conduct a technical scope comparison of all bids to highlight discrepancies before contracting.
- Define a delivery responsibility matrix and escalate unresolved handover items to a nominated project manager.
- Require the supplier to provide clear spares availability and lead times in the offer.
Insurance and claims handling
- Verify cargo insurance covers transit to the agreed risk transfer point (per Incoterms).
- Keep evidence of packing and handling for claims support; manufacturers should provide packing photos and pack lists.
Escalation paths and change control
- Set clear change control procedures with cost and time evaluation steps.
- Define dispute resolution: mediation, expert determination, or arbitration clauses.
Six-step buyer workflow for using a carport wholesale manufacturer
This named six-step workflow converts strategy into procurement practice:
Step 1 — Project definition and decision gate
- Deliverable: documented project basis with scope, site data, functional requirements and acceptance criteria.
- Who: Buyer, Architect, Structural Engineer.
- Output: Go/No-Go decision on whether to centralize manufacturer responsibility.
Step 2 — Technical scope comparison and shortlist
- Action: Issue the same technical brief to all bidders; perform a side-by-side technical scope comparison.
- Deliverable: comparative matrix highlighting differences in prefab level, finishes, PV interface, and documentation.
- Tools: Request Carportiva system range details as a baseline where applicable.
Step 3 — Due diligence and sample order
- Action: Conduct B2B supplier due diligence, review factory quality documentation, and request sample/coating panel.
- Deliverable: factory evidence pack and pre-production sample approval.
- Note: include third-party inspection for critical items.
Step 4 — Contract and procurement controls
- Action: Finalize contract with explicit project procurement controls: acceptance tests, delivery responsibility matrix, penalties, and warranties.
- Deliverable: signed contract with agreed Incoterms and delivery milestones.
Step 5 — Production oversight and logistics
- Action: Approve shop drawings, witness production (if required), confirm export packing coordination, and arrange freight booking.
- Deliverable: pre-shipment inspection reports, packing photos, and logistics plan.
Step 6 — Site delivery, installation and close-out
- Action: Coordinate site offload, install per manufacturer guidance, perform acceptance tests, and complete handover.
- Deliverable: as-built drawings, factory quality documentation, spare parts, and final acceptance certificate.
Buyer checkpoints and acceptance gating
- Gate A: Technical sample and scope lock before production start.
- Gate B: Pre-shipment inspection and packing approval before release.
- Gate C: On-site acceptance and handover.
Tools and templates
- Use the supplier evidence checklist, delivery responsibility matrix and a document register integrated into the contract.
For additional procurement templates and sector-specific guidance see sourcing guides and explore technical choices in all systems.
Mid-article CTA If you want help aligning manufacturer responsibilities with your project requirements, contact our team at /inquiry or email info@carportiva.com.
Frequently asked questions (FAQ)
Q: How should I choose between pre-assembled modules and kit-of-parts? A: Choose pre-assembled modules when site installation time, on-site labour capacity and crane availability make single lifts efficient and when transport constraints (width/height) are manageable. Kit-of-parts suits restricted access sites and lower unit transport cost. Balance transport cost, on-site labour availability and risk of site rework.
Q: What level of factory documentation is reasonable to ask for? A: At minimum: mill certificates, coating batch reports, dimensional checklists and pre-shipment photos. For safety-critical or high-value projects ask for weld records, inspection reports and dimensional control plans.
Q: Who is responsible for anchor bolt positions and foundation tolerances? A: Typically the buyer or their structural engineer verifies and provides foundation details to the manufacturer. The manufacturer should indicate anchor plate tolerances and grout requirements; responsibility must be explicit in contracts to avoid interface errors.
Q: Should I require third-party inspections? A: For high-value orders, long supply chains, or when acceptance is contractually critical, third-party inspections or witness testing are advisable.
Q: How do Incoterms affect my project schedule? A: Incoterms determine who arranges carriage, customs clearance, and at which point risk transfers. Misunderstanding Incoterms can cause schedule slippage; agree terms early and align with logistics partners [3].
Q: What documentation is essential for customs? A: Commercial invoice, packing list, certificate of origin (if preferential duties applied), and any regulatory certificates. Prepare for country-specific requirements and check local customs guidance [4].
Q: Can a manufacturer be held responsible for energy yield shortfalls on solar carports? A: Only if the contract explicitly covers energy yield guarantees and the manufacturer accepts responsibility for PV system performance; typically PV EPCs or asset owners take performance risk. Energy yield depends on site shading, inverter selection, and system commissioning — local professionals should validate projections.
Q: How much lead time do I need? A: Lead time depends on manufacturing backlog, surface treatments, and logistics. Include manufacturing and shipping buffers in procurement controls and confirm with the supplier documented lead-time commitments.
Conclusion and practical next steps
Summary Deciding when a carport wholesale manufacturer matters requires aligning product consistency, factory traceability, and logistics control with your project’s risk profile. Use documented project inputs, a rigorous technical scope comparison, B2B supplier due diligence and enforceable project procurement controls to define how much contractual responsibility the manufacturer should carry. Insist on factory quality documentation, clarify export packing coordination and draw a delivery responsibility matrix that prevents handover disputes.
Final checklist before awarding to a manufacturer
- Completed documented project basis and scope locked.
- Side-by-side technical scope comparison and acceptance of samples.
- Satisfactory B2B supplier due diligence and factory evidence.
- Contractual project procurement controls with clear delivery responsibility matrix and Incoterms.
- Logistics plan with export packing coordination and pre-shipment inspection.
- Local installation, commissioning and warranty handover agreed with qualified professionals.
If you want to discuss alignment of manufacturer responsibilities with your project scope, review our product lines at Carportiva system range, or contact us directly through /inquiry or info@carportiva.com.
Sources and further reading
- Best practice guidance on hot-dip galvanizing and corrosion protection: American Galvanizers Association [1]
- International standards and quality system references: ISO [2]
- Delivery and risk terminology: International Chamber of Commerce (Incoterms) [3]
- Import and customs documentation guidance: U.S. Customs and Border Protection [4]
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion