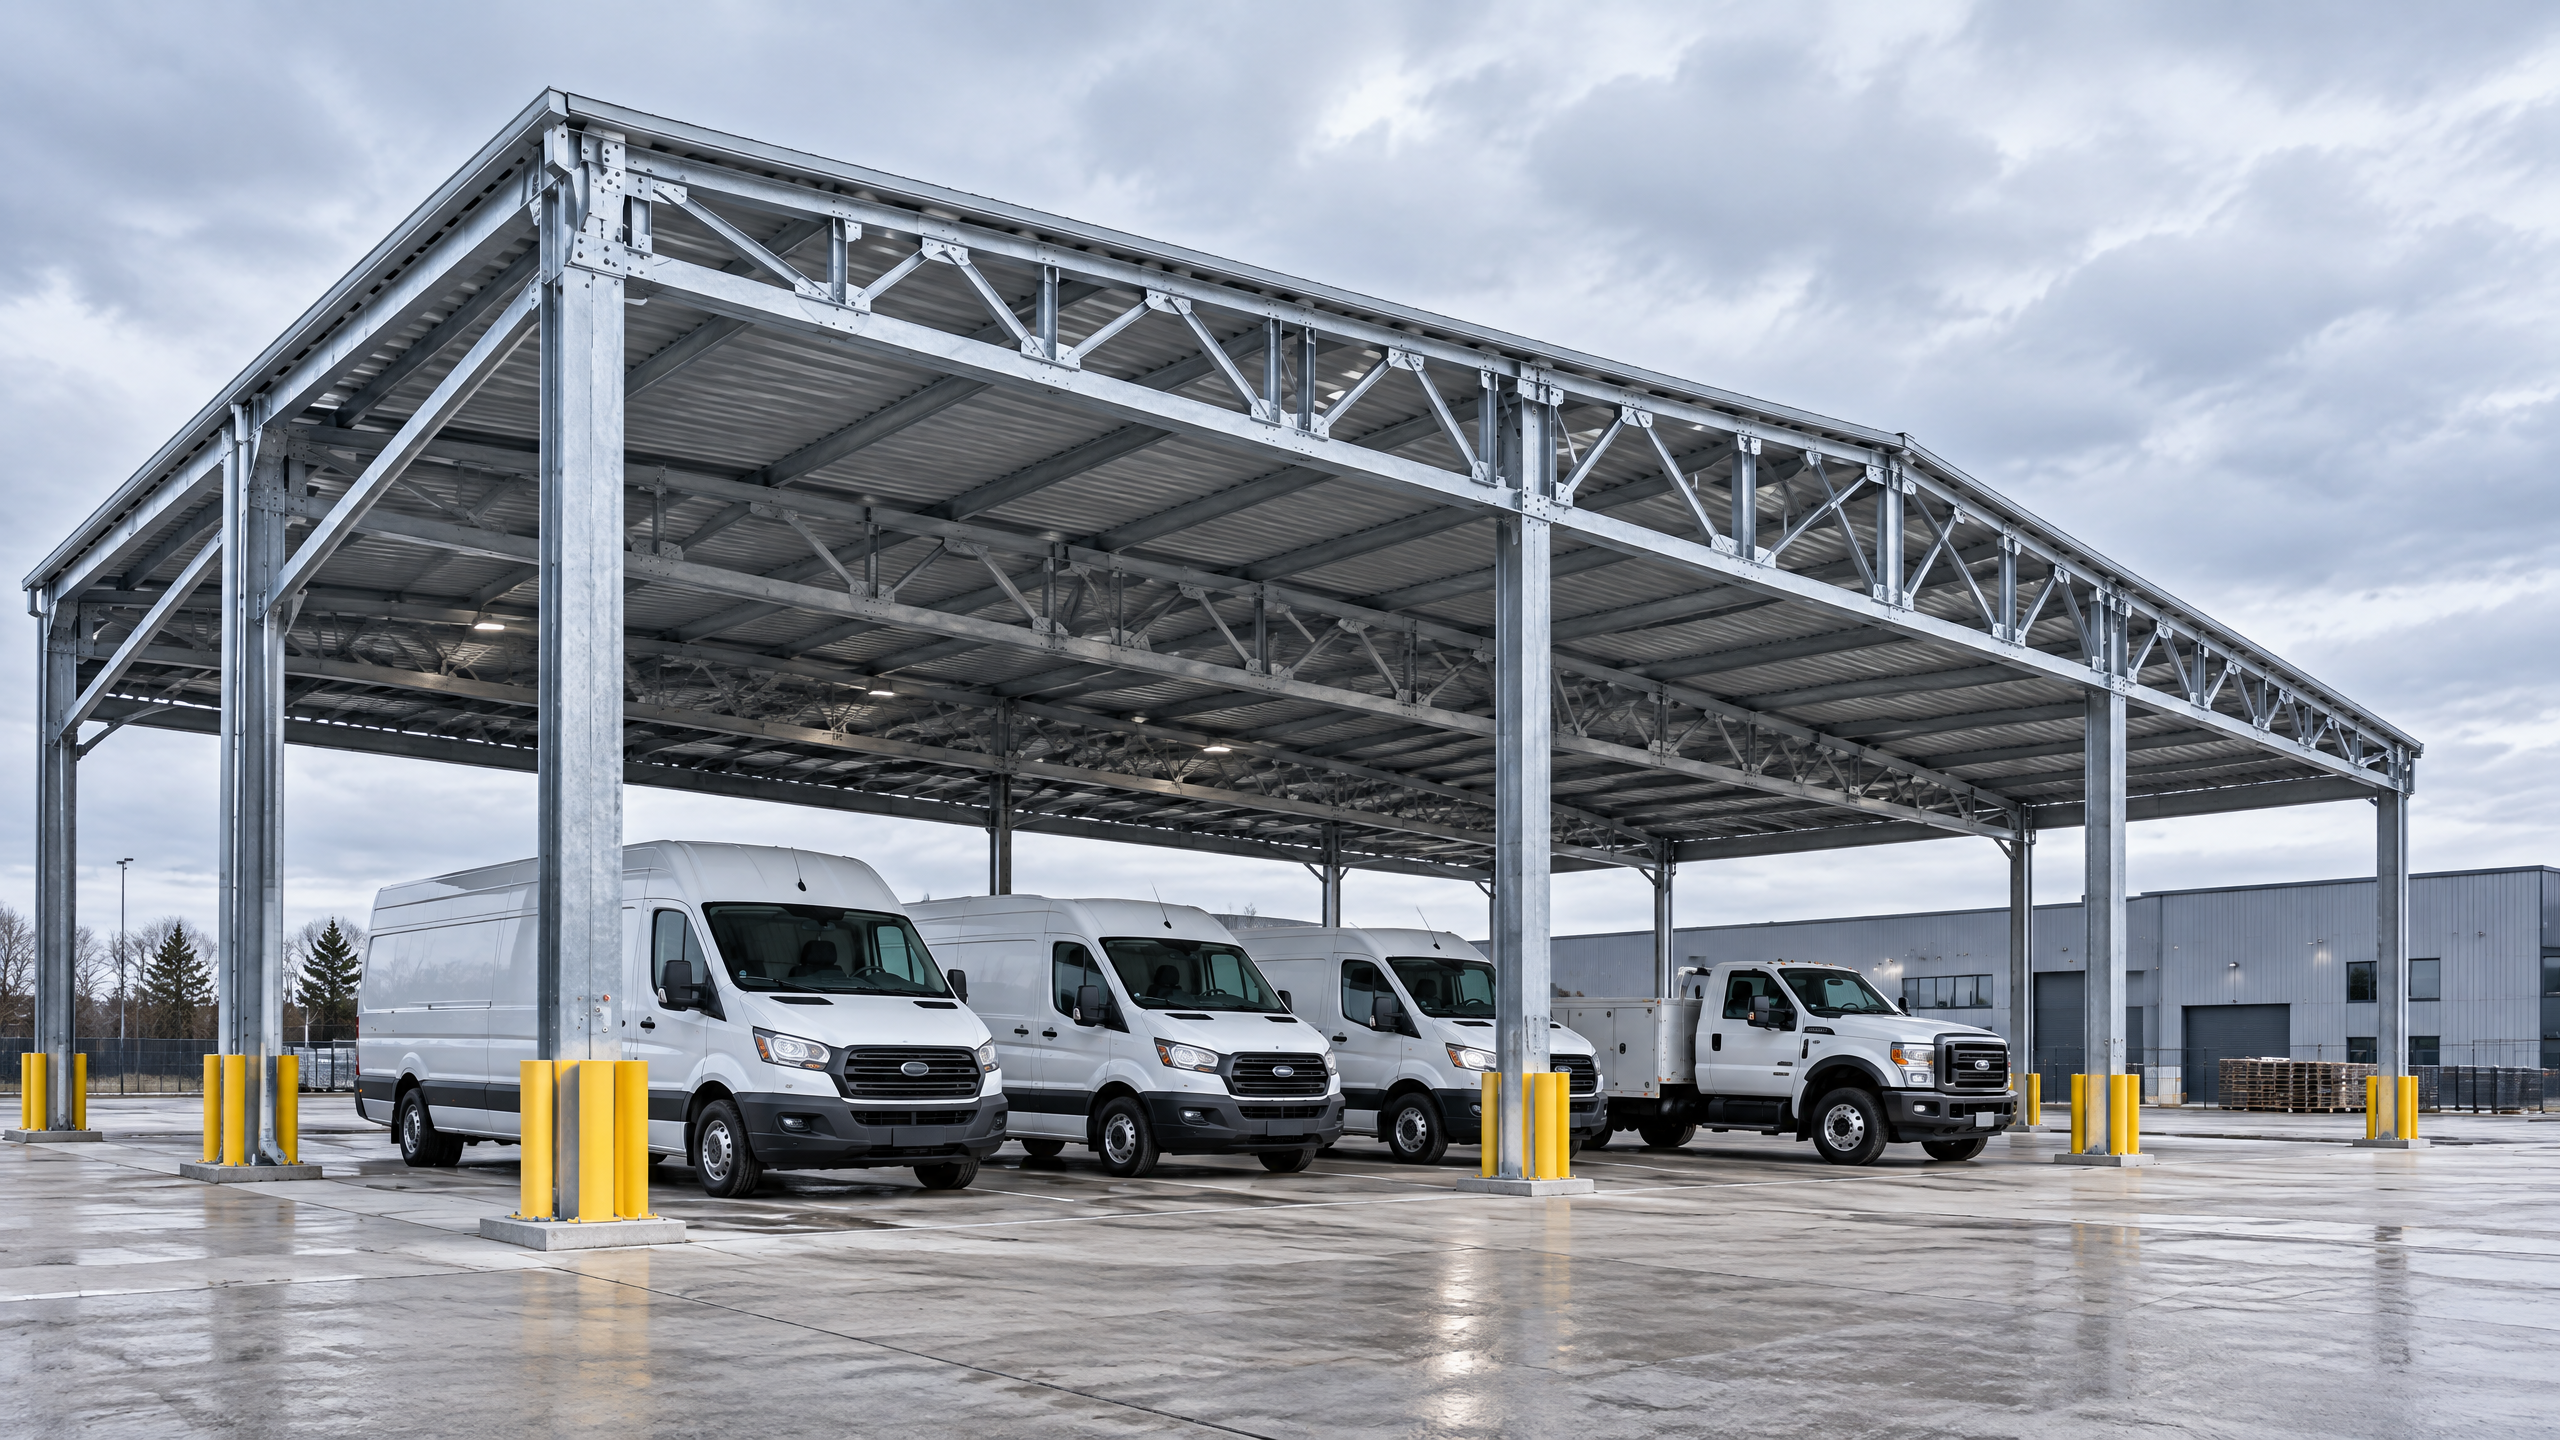
Direct answer (140 words): For a successful industrial carport manufacturer fleet project, buyers must treat supplier selection as a technical procurement exercise with layered evidence: verified factory capability, clearly comparised technical scope, documented responsibilities for delivery and installation, and measurable project procurement controls. Begin with a bounded scope and performance requirements (vehicle sizes, canopy loads, PV integration if required). Use formal B2B supplier due diligence, a technical scope comparison, and factory quality documentation to reduce ambiguity. Require an export packing coordination plan and a delivery responsibility matrix tied to Incoterms and local import rules. Validate installation competence, warranty terms and service pathways before contract. Ensure every commercial term is mapped to acceptance criteria, lead time commitments and project milestones. For site-specific items — structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty — assemble a documented project basis and involve qualified local professionals, installers, utilities and authorities.
Buyer context and scope boundary
Why a fleet project is different
- Scale: Fleet projects typically require repeatable modular solutions across multiple units and sites. Repeatability increases the need for factory consistency and controlled tolerances.
- Interface complexity: Vehicle shelters interact with civil works, electrical systems (for lighting and EV charging), and sometimes PV systems. These interfaces demand clearer technical handoffs than a single private carport.
- Procurement cadence: Fleet rollouts may be procured as pilot → tranche → full deployment. Each tranche should carry lessons that are contractually enforceable and measurable.
Define scope boundaries up-front
- Functional scope: shelter footprint, clearances, turning templates for largest vehicle, clearance for maintenance access, snow/wind load design criteria, fire escape routes.
- Product scope: primary structure, secondary members (purlins, gutters), fasteners, anchorages, coatings, integrated PV or electrical conduits if any.
- Services scope: transport, export packing coordination, on-site assembly, testing, commissioning, spare parts supply and warranty handling.
- Contractual scope: acceptance tests, milestone payments, lead time windows, retention, liquidated damages and change-order processes.
Scope boundary checklist (use this to lock the RFP)
- Site coordinates and geotechnical report
- Local wind and snow loads and design standards
- Vehicle templates and MEP interface points
- Permitting lead times and responsible party
- Preferred or mandatory materials (e.g., aluminium alloy, galvanizing)
- Finish and colour requirements
- Warranty period, coverage, and exclusions
Note: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Core decision principle: evidence over rhetoric
Make supplier selection evidence-led
- Requirement traceability: Every functional requirement must map to a deliverable, test, or document in the contract and be verifiable.
- Risk-based acceptance: Prioritise requirements by consequence. Critical items (structural adequacy, anchorage design, corrosion protection) have higher verification needs than cosmetic finishes.
- Proven manufacturing reproducibility: For fleet projects the ability to deliver consistent parts repeatedly is more important than one-off aesthetic projects.
Evidence types to demand
- Factory quality documentation (shop drawings, material certificates, fabrication process audits)
- Site installation competency (references, proof of trained installers, project-specific method statements)
- Logistics and packing plans (export packing coordination, transport load plans)
- Commercial evidence (fixed lead times, payment milestones tied to deliverables, penalties for late or non-compliant shipments)
Use samples and factory visits selectively
- For structural systems, request sample connections, full-scale mockups if the budget allows, and weld test records or non-destructive testing where specified.
- Factory visits should be scheduled with an agenda (process walkthrough, quality control records review, inspection of finished assemblies). Where visits are impractical, insist on live video inspection and recorded factory acceptance testing.
Planning inputs: what the buyer must provide
To obtain realistic proposals, buyers must deliver baseline inputs. The fewer assumptions the supplier must make, the more comparable proposals will be.
Minimum planning package to provide to bidders
- Site plan with coordinates, datum and access routes
- Geotechnical report showing bearing stratum and groundwater
- Local structural design criteria: code citation, characteristic wind/snow loads
- Vehicle templates and maximum vehicle dimensions (including service vehicles)
- Utilities and MEP interface points, including proposed locations for EV chargers, transformers or PV inverters
- Project timeline with hard milestones, and any staging constraints for phased delivery
- Local permit and approval processes timelines and responsible authority contacts
Procurement document structure recommendations
- Section A — Technical Specifications and Acceptance Criteria (non-negotiable)
- Section B — Commercial Terms, Incoterm, Payment Milestones, Penalties
- Section C — Factory and Inspection Requirements (including factory acceptance tests)
- Section D — Installation, Commissioning and Handover (site acceptance tests)
- Section E — Drawings, approvals and record-keeping obligations
Deliverables you should demand in response
- A detailed technical bid with material callouts and manufacturing tolerances
- A Gantt that shows lead times for procurement, fabrication, packing and shipping
- A delivery responsibility matrix that specifies when legal and practical responsibility shifts
- A preliminary installation method statement and resource plan
Technical specification and interfaces
Technical clarity reduces rework and disputes. For industrial carport manufacturer fleet project tenders, break the technical scope into discrete interface modules.
Key technical modules
- Primary structural system: columns, beams, moment connections, corrosion protection of structural steel or aluminium profiles
- Secondary system: purlins, rails, gutters, roof sheeting or PV mounting
- Foundations and anchorage: bolt sizes, embedment depths, grout and baseplate detailing (buyer or supplier responsibility must be explicit)
- Electrical and PV interfaces: cable entry, earthing, inverter mounting, combiner box locations
- Drainage and water handling: downpipes, overflow paths
- Finishes and coatings: powder coat types, chromate treatments, or galvanizing standards
- Fasteners and consumables: type, grade, corrosion class
Technical scope comparison
- Use a technical scope comparison to align bidder proposals against a common checklist. This produces apples-to-apples evaluation rather than headline price comparisons.
Decision table 1 — Technical scope comparison (example)
| Technical Area | Buyer Spec / Requirement | Supplier A Response | Supplier B Response | Conforms (Y/N) |
|---|---|---|---|---|
| Column section & alloy | 6061-T6 (aluminium) or equivalent | 6005-T6, μ=±2mm | 6061-T6 confirmed | Y |
| Corrosion protection | Hot-dip galvanize to spec or powder coat for aluminium* | Galvanized per AGA guidance [1] | Powder coat (no galvanize) | N |
| PV mounting interface | Designed for framed modules, 35–40 mm clamp zone | Integrated rail system | Separate rail, additional clips required | Y |
| Anchor bolts | M24 stainless or specified grade | M24 grade 8.8 (galv) | M20 supplied — will change if approved | N |
*If specifying galvanizing, refer to industry guidance for coating thickness and inspection protocols [1].
Interfaces and tolerances
- Define allowable tolerances for column positions, levelness and datum relative to the finished site. For fleet projects, small cumulative tolerances can cause alignment failure across repeated units.
- Specify connection accessibility and expected torque levels for critical bolted joints.
Standards and quality expectations
- Reference applicable material standards, and request the supplier’s factory quality documentation that maps outputs to those standards. Where a specific standard is not mandatory, require a conforming test or certificate.
- Encourage suppliers to show their quality management system (e.g., ISO 9001) and relevant process controls [2]. Do not accept unsubstantiated claims — request certificates and audit trails.
Procurement and factory evidence
This is the section where procurement rigor wins contracts that deliver reliably.
B2B supplier due diligence checklist
- Corporate credentials: legal entity, years trading, list of principal markets
- Financial stability: audited accounts or bank letters (as allowed by policy)
- Manufacturing capability: plant capacity, number of production lines, typical output per month
- Quality systems: certificates, internal QA procedures and inspection frequency
- Traceability: batch and heat-number tracking for structural materials
- Labour competency: training records for welders, fitters and assembly teams
- Health & Safety records and policies
Factory evidence to demand
- Factory quality documentation: standard working drawings, welding procedures, NDT reports, material mill certificates and purchase records. Ask for specific examples where similar items were produced and inspected.
- Bills of materials (BOM) with supplier source details and substitution policy
- Factory Acceptance Test (FAT) plan and acceptance criteria, including measurement methods and software or gauges used
- Photographic and dimensional records from previous production runs (with anonymisation where necessary)
Export packing and transport
- Insist on detailed export packing coordination plans showing pack sizes, palletisation, protective materials and weight distribution — this protects product integrity and simplifies port handling.
- Export packing plans must show how corrosion-sensitive parts are protected and where sacrificial skins are placed.
- For overseas shipments, verify compliance with import documentation and packaging restrictions; consult customs guidance for documentation expectations [4].
Decision table 2 — Delivery responsibility matrix (aligned to Incoterms)
| Activity | Buyer Responsibility | Supplier Responsibility | Recommended Incoterm | Notes |
|---|---|---|---|---|
| Manufacture | N/A | Supplier | EXW / FCA | Supplier must provide factory quality documentation |
| Export packing coordination | Supplier provides plan; Buyer to approve | Supplier prepares and executes packing | FCA (seller loads at terminal) | Clear approvals reduce damage claims |
| Customs export clearance | Supplier | Supplier | FCA (export handled by seller) | Provide export docs for buyer import clearance |
| International carriage | Buyer or seller per contract | Responsible party per Incoterm | DAP / DDP for fixed price clarity | DDP transfers import risk to seller — negotiate carefully using Incoterms guidance [3] |
| Import customs clearance | Buyer (unless DDP) | Seller (if DDP) | See Incoterms [3] | Check local CBP or authority requirements [4] |
Use Incoterms and local import guidance
- Map the delivery responsibility matrix to the chosen Incoterm and require the supplier to demonstrate experience in the buyer’s port or country. Refer to ICC Incoterms for legal delivery definitions [3] and to national customs guidance for documentation [4].
- Where the supplier proposes DDP (Delivered Duty Paid), verify their capacity to manage local customs and taxes in the buyer jurisdiction.
Factory Acceptance Testing (FAT)
- FATs should be witnessed, recorded and have sign-off templates with explicit pass/fail criteria.
- Require digital records (video and measurement logs) for each shipment batch, especially when you cannot witness FAT in person.
Supplier performance KPIs
- On-time delivery rate, conformity rate (first-pass acceptance), defect frequency and corrective action timeliness.
- Build performance bonds or retention where appropriate for high-value contracts.
Site installation, commissioning and operations
Clarify responsibilities for site works
- Explicitly assign responsibilities for foundations, grouting, anchor inspection, and interface with site drainage and electrical systems.
- If the supplier installs, require installation method statements, site health and safety plans, and a crew competency matrix.
- If the buyer uses local installers, require the supplier to provide assembly drawings, training and supervision as part of a handover package.
Site acceptance testing (SAT)
- Tests should verify structural alignment, torque checks on critical bolts, water tightness (where applicable), drainage, and electrical continuity for PV or lighting circuits.
- For PV-enabled carports, commissioning must include inverter start-up, earthing tests, and energy yield baseline checks (record pre-commissioning conditions).
Operations and maintenance (O&M)
- Request an O&M manual with a parts list, preventive maintenance schedule, recommended cleaning regimes (for aluminium finishes), and anticipated spare parts lead times.
- Define warranty response SLAs — time-to-acknowledge and time-to-repair or replace — and include escalation contacts.
Training and knowledge transfer
- For fleet rollouts, include a training package for at least two local representatives per region. Training should include assembly supervision, torque checks, and maintenance tasks.
Warranty clarity
- Define warranty start date (typically site acceptance date), what constitutes a warranty defect, and what voids the warranty (unauthorised modifications, improper foundations, etc.).
- Avoid vague statements: require the supplier to provide a warranty matrix that maps component to warranty term and remedy.
Implementation risks and mitigations
Common risks in industrial carport manufacturer fleet project and mitigations
- Ambiguous scope leading to change orders
- Mitigation: rigorous technical scope comparison and locked RFP documents. Use drawings with dimensions and tolerances.
- Factory quality drift over a long campaign
- Mitigation: staged FATs, random batch inspections, and KPI-triggered audits. Require factory quality documentation for each batch.
- Logistics damage and customs delays
- Mitigation: approved export packing coordination, pre-shipment inspections, and assignment of clear delivery responsibilities (use Incoterms) [3]. Validate import paperwork with local customs guidance [4].
- Local regulatory / permit hold-ups
- Mitigation: early engagement with authorities; explicit allocation of permit responsibility; include time contingencies in the programme.
- Misalignment between foundations and supplied baseplates
- Mitigation: early anchor bolt templates and confirmation of as-built levels. Consider vendor-supplied baseplate positioning jigs.
- Inadequate installation competence
- Mitigation: require supplier-provided supervision or training, specify installer qualification levels, and include performance guarantees.
- Warranty disputes
- Mitigation: clear warranty matrix, SAT records, photographic evidence of defects, and agreed remediation timelines.
- Exchange rate and inflation exposure across a multi-tranche project
- Mitigation: contract currency clauses, price adjustment mechanisms and hedging where appropriate.
Contract clauses that reduce risk
- Defined acceptance criteria and test protocols
- Escrow or performance bond for critical milestones
- Liquidated damages for late delivery and non-conformance
- Clear change order procedure with rates and approval timelines
Six-step buyer workflow (named and actionable)
"Structured Fleet Procurement Loop" — a practical six-step workflow to evaluate, award and manage an industrial carport manufacturer fleet project.
Step 1 — Define and fix the project basis
- Deliver the planning package listed earlier, commission geotechnical and survey reports, define vehicle templates. Lock non-negotiable technical requirements.
Step 2 — Issue a technical RFP with evaluation matrix
- Include technical scope comparison tables, FAT requirements, packaging expectations and a delivery responsibility matrix. Use mandatory pass/fail gates for critical items.
Step 3 — B2B supplier due diligence and shortlist
- Execute the supplier due diligence checklist. Validate factory capability and request references for similar scale work. Require factory quality documentation and sample FATs.
Step 4 — Evaluate proposals with weighted scoring
- Use a matrix that weights technical compliance (40–50%), factory evidence and FAT plan (20–30%), logistics and delivery responsibility (10–15%), commercial terms and price (10–20%). Adjust weights per buyer risk appetite.
Step 5 — Contract negotiation and pilot order
- Negotiate contract terms including project procurement controls, payment milestones, warranty matrix, and KPIs. Run a paid pilot or first tranche to confirm factory processes and installation workflows.
Step 6 — Rollout, monitor and continuous improvement
- For each tranche, perform FATs, site acceptance tests, and KPI reviews. Maintain a lessons-learned register and require corrective action plans from the supplier for non-conformances.
Practical checklist per step
- Step 1: Entrust someone to assemble the technical baseline and sign-off authorities.
- Step 2: Provide bidders with a clear timeline for queries and addenda.
- Step 3: Perform at least one independent reference check and require financial viability proof.
- Step 4: Use the decision tables in this guide to compare proposals uniformly.
- Step 5: Document the pilot results and require supplier corrective action for deficiencies before broader deployment.
- Step 6: Hold monthly performance reviews and retain a small retention sum until 90 days post-commissioning for each tranche.
Mid-article call to action If you would like bespoke procurement templates or a project-specific questionnaire for your industrial carport manufacturer fleet project, request them via /inquiry. Also see our systems approach in Titan industrial and logistics system and explore all systems and sourcing guides for related procurement resources.
Procurement controls and governance
Define project procurement controls
- Change control board (CCB): small group with authority to approve technical and commercial changes, including budget impacts.
- Document control: single source of truth for revisions to drawings, specifications and approvals.
- Financial controls: pre-approved thresholds for change orders, approvals for retention release, and audit trails for payments.
- Quality gates: defined FAT and SAT sign-offs before milestone payments.
Sample procurement control matrix
| Control Area | Gatekeeper | Required Evidence | Release Condition |
|---|---|---|---|
| Fabrication start | Project Engineer | Approved shop drawings, material certificates | 100% drawings approved |
| Packing and dispatch | Logistics Manager | Export packing coordination plan, FAT report | Packing approved, insurance arranged |
| Site handover | Site Manager | SAT reports, as-built drawings | All SAT passed |
Auditability and record-keeping
- Retain inspection reports, measurement logs, packing photographs and shipping documents for the project archive. These support warranty claims and dispute resolution.
Compliance with standards and traceability
- Request traceability from raw material to finished assembly, including mill certificates and batch numbers. If galvanizing is specified or expected for ferrous components, align acceptance criteria with galvanizing guidance [1]. For quality management systems and process control evidence, request applicable ISO certificates [2].
Frequently asked questions (FAQ)
Q: How do I compare bids that use different delivery terms? A: Insist on a delivery responsibility matrix mapped to the chosen Incoterms. Translate cost, risk and responsibilities into a common comparator (e.g., landed cost to site) and account for customs, duties and local handling [3][4].
Q: How much factory evidence is reasonable? A: For fleet projects, require sample FATs for the first tranche and FAT records for subsequent batches. Demand factory quality documentation for critical parts (material certificates, welding procedures) and at least photographic evidence for non-critical items.
Q: Should I require galvanizing for metal parts? A: That depends on material and environment. If galvanized coatings are specified, align acceptance and inspection with industry guidance [1]. Aluminium systems may use anodising or powder coating — specify the exact coating system and inspection tests.
Q: Can a supplier use local installers? A: Yes, but require supplier-provided supervision, training and sign-off on final acceptance. Define installer qualifications and require a handover training session with documented competency checks.
Q: What role do FATs play? A: FATs verify that modular elements meet design intent before they leave the factory, which reduces rework and delays on site. Make FATs contractual with pass/fail criteria and digital records.
Q: How should I manage multi-country rollouts? A: Use a pilot tranche to validate the supply chain and documentation. Standardise technical specifications and procurement controls across countries, but allow for local amendments driven by permits and site conditions.
Q: What are appropriate KPIs? A: On-time delivery, first-pass acceptance rate, defect density per tranche, response time to defect reports, and adherence to agreed packing standards.
Q: Are warranties enforceable across jurisdictions? A: They can be, but enforcement depends on contractual law and local courts. Include clear dispute resolution clauses and warranty remedy definitions. If warranty coverage extends to replacement parts in-country, verify the supplier’s capability to deliver.
Conclusion
Selecting and managing an industrial carport manufacturer fleet project requires structured procurement controls, a defensible technical scope comparison and verified factory evidence. B2B supplier due diligence, explicit factory quality documentation, and contractual clarity on packing and logistics (including export packing coordination) materially reduce project risk. Use a delivery responsibility matrix that maps to Incoterms and national import rules and insist on FATs and site acceptance tests. Maintain a project governance loop—define, issue, shortlist, pilot, roll out and monitor—to ensure consistency across tranches.
Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
For tailored procurement templates or to discuss a specific fleet project, contact us at info@carportiva.com.
References
- American Galvanizers Association: https://galvanizeit.org/
- International Organization for Standardization: https://www.iso.org/
- International Chamber of Commerce Incoterms: https://iccwbo.org/business-solutions/incoterms-rules/
- U.S. Customs and Border Protection import guidance: https://www.cbp.gov/trade/basic-import-export
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion