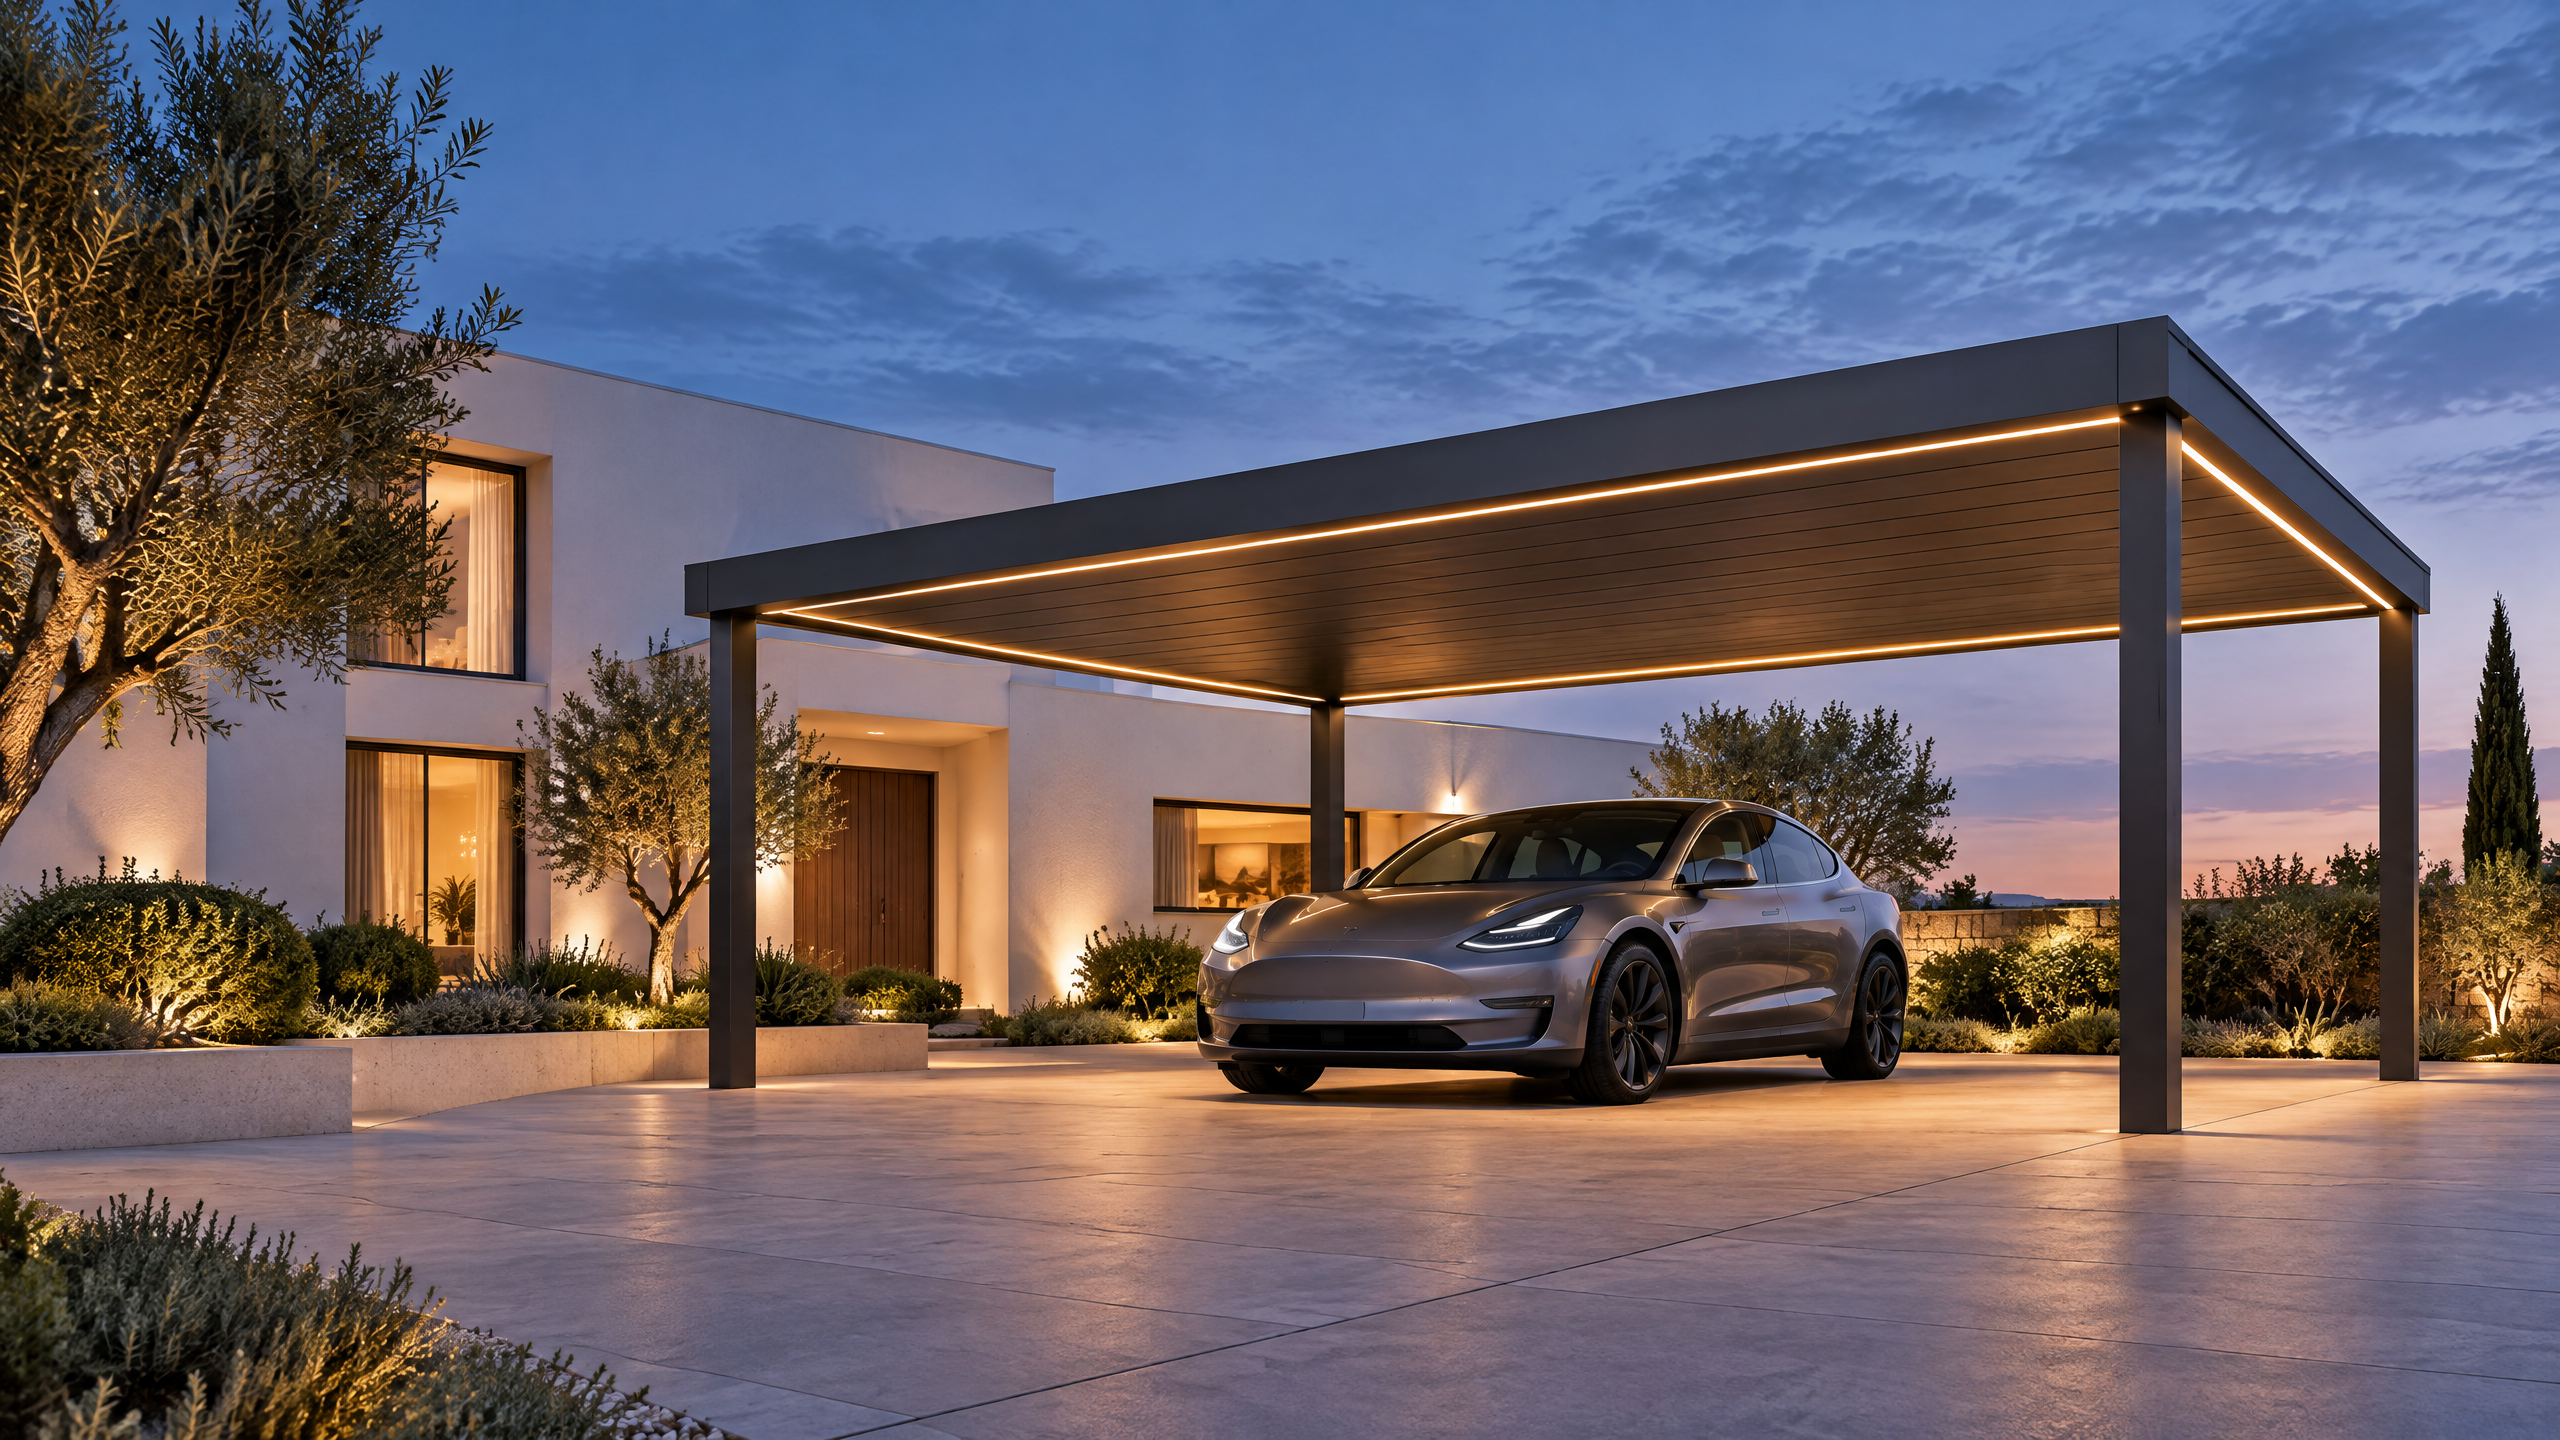
A modern carport manufacturer must be selected on the basis of capability to deliver an integrated architectural aluminium system that meets project performance, risk and procurement constraints. The right decision balances a clear architectural carport specification, tested and documented aluminium profile selection, coordinated roof drainage coordination and compatible finish and fastener compatibility with demonstrable factory QA, shop drawing review, and installation readiness. For commercial projects (parking, solar canopies, fleet shelters) purchasers need objective evidence: structural calculations tied to local loads, material traceability, manufacturing tolerances, factory acceptance testing, and a defined supply‑chain lead time and installation scope. This guide translates those requirements into checklistable procurement evidence, technical interface rules, a six‑step buyer workflow, and practical risk controls so distributors, architects, contractors, developers, EPCs and fleet operators can specify and buy from a modern carport manufacturer with confidence.
Buyer context and scope boundary: who needs what from a modern carport manufacturer
Commercial carport projects span small retail parking to large commercial solar carport arrays and industrial/fleet shelters. The buyer role (distributor, architect, contractor, developer, solar EPC or fleet operator) defines the technical and contractual boundaries you must control when specifying a modern carport manufacturer.
Key scope dimensions to declare early
- Project function: sheltered parking, solar canopy (PV), covered logistics/maintenance area, or mixed use.
- Design intent: architecturally exposed structure, integrated rooftop photovoltaics, or purely functional shelter.
- Regulatory context: wind, snow and seismic loads per local standards (normative references may include Eurocodes or equivalent) [1].
- Procurement model: supply‑only, supply + site installation, design & build, or turnkey with civil foundations.
- Delivery constraints: phased delivery, factory preassembly, or on‑site modular erection.
Limitations this guide does not cover in depth: site‑specific structural capacity, foundation design, permitting processes, electrical design for PV, utility interconnection, local approvals, precise lead time, firm price, predicted energy yield or specific warranty wording. Those items require a documented project basis and involvement of relevant local qualified professionals, installers, utilities and authorities — see the explicit note at the end of this guide.
Why the manufacturer matters A modern carport manufacturer is the technical and contractual anchor for prefabricated architectural aluminium systems. Their responsibilities commonly include aluminium extrusion supply, finishes, accessory supply (flashings, gutters, fasteners), structural verification, production quality control, shop drawings, factory acceptance and supply logistics. Selecting a manufacturer with aligned systems, documented evidence and relevant references reduces downstream variations and latent defects.
Related Carportiva product lines and resources
- See the NordFlat architectural villa system for a compact example of an architectural aluminium approach.
- For broader options, review all systems.
- For procurement templates and checklists consult our sourcing guides.
Core decision principle: match technical deliverables to contractual evidence
The core principle is simple: require the manufacturer to deliver verifiable technical deliverables that map 1:1 to the contract milestones and to installation acceptance criteria. In practice this means that for each technical claim you require corresponding documentation — not words alone.
Primary deliverables to require in the specification
- Structural design package (loads, calculations, stamped drawings).
- Materials declaration (alloy temper, mill certificates, corrosion class).
- Finish specification and test evidence (adhesion, salt spray where applicable).
- Detailed shop drawings and 3D coordination models for review.
- Manufacturing QA records and dimensional tolerance tables.
- Factory Acceptance Test (FAT) protocol and results.
- Packing, logistics and installation scope matrix.
- Warranty scope and conditions (what is covered, what is excluded).
These deliverables should be tied to acceptance gates: design approval, pre‑shipment inspection, delivery acceptance and practical completion.
Decision table 1 — matching project need to minimum manufacturer deliverables
| Project type | Minimum structural deliverable | Finish / durability evidence | Installation scope expected |
|---|---|---|---|
| Small architectural carport (commercial retail) | Structural calculations + shop drawings | Material certificates + finish spec | Supply + bolt‑up installation |
| Solar carport (EPC) | Structural calcs for combined dead, wind, snow, PV loads | Coating system spec; fastener corrosion control | Supply + electrical interfaces; cable penetrations |
| Large fleet shelter or industrial | Site‑specific stamped structural package; connection details | Mill certs, compatibility tests for chemical exposure | Supply + specialist erection team; crane lifts |
Note: structural calcs must reference applicable standards; for European projects consult Eurocodes for wind and snow load principles [1].
Planning inputs: data you must provide before issuing a manufacturer specification
A manufacturer cannot responsibly price or accept installation readiness without a documented project basis. Provide these inputs to all tendering manufacturers:
Essential planning inputs
- Site coordinates and topography — to determine wind directionality, exposure and snow loads.
- Local governing codes and standards, or identified national equivalents of Eurocodes [1].
- Basic utility layout for grid connection (for PV): point of connection, availability of AC/DC infrastructure.
- Geotechnical report showing soil bearing capacity and groundwater level for foundation design.
- Architectural intent drawings showing canopies relative to buildings, access, and egress clearances.
- Functional loads: design vehicle profile, live loads for maintenance, and crane pick points if required.
- Finish expectations: colour palette, gloss level, visible fastener requirements, anti‑graffiti or other protective demands.
Reference documents to request from the manufacturer at tender
- Typical foundation detail range (anchor bolt loads, baseplate sizes).
- Module mounting details (for PV) and cable routing strategy.
- Drainage strategy (roof drainage coordination) connecting canopies to site stormwater systems.
- Installation manpower and plant list by erection stage.
Minimum tender question set you should include
- Can you provide site‑specific stamped structural calculations for the value of imposed loads described? If not, describe limits and assumptions.
- Provide aluminium alloy and temper designations and mill test certificates.
- How do you handle roof drainage coordination to adjacent buildings and the local storm system?
- Provide standard lead times per quantity and options for partial deliveries.
- List exclusions: foundations, electrical, crane, groundworks.
Technical specification and interface rules
This is the section where the architectural intent becomes procurement language. Use explicit, testable statements rather than qualitative claims.
Architectural carport specification: what to include
- Scope: supply, surface treatment, accessories, shop drawings, factory testing, delivery and installation scope.
- Materials: specify aluminium alloy series (e.g., 6000 series) and temper where appropriate, with required mill certificates on supply.
- Structural criteria: reference governing standards and design combination factors (dead, live, wind, snow, seismic) — note where Eurocodes are used [1].
- Connections: design for bolted connections with grade of fasteners, torque settings, and corrosion protection specified.
- Finishes: specify class (e.g., architectural powder coat class, fluoropolymer) and acceptable performance evidence; request adhesion and colour‑fastness data from manufacturer; see AAMA guidance for architectural finish expectations [3].
- Tolerances: dimensional and flatness tolerances for extrusions and assemblies; acceptance criteria for out‑of‑plumb and level.
Aluminium profile selection
- Request cross‑section drawings, moment of inertia (Ix, Iy), section modulus, and connection zones.
- Require mill certificates for alloy and temper and declare required mechanical properties.
- Provide gross allowable stresses or require the manufacturer to provide allowable values based on tested or code‑compliant values [2].
Roof drainage coordination
- Define design rainfall intensities and stormwater discharge points.
- Require manufacturer to show gutter sizing, downpipe positions, overflow provisions, and interface to site stormwater.
- For PV installations, ensure cable penetrations and junction boxes do not compromise watertightness. Drainage paths should be coordinated in the shop drawing review.
Finish and fastener compatibility
- Require a compatibility statement for finish and fastener material combinations (e.g., aluminium profile to stainless steel fasteners with insulating washers where required).
- Ask for evidence of galvanic corrosion mitigation strategy, sealant compatibility and cleanliness for painted surfaces (AAMA and Aluminum Association references can guide acceptable practice) [2][3].
Shop drawing review and approvals
- Specify a shop drawing review workflow: initial manufacturer submission, architect/engineer review comments, resubmission, and approval milestone. Define maximum review times to avoid delays.
- Require 3D BIM or model exports (IFC or equivalent) for clash detection with site utilities and other trades.
Installation readiness
- Define what constitutes installation readiness: foundations completed to specified tolerance, anchor bolts set and checked, cranes and plant available, pre‑installation inspections complete, and interface trades scheduled.
- Require a pre‑installation checklist from the manufacturer showing lifted items, pre‑assembled modules, torque procedures, and QA hold points.
Decision table 2 — Technical interface checklist (acceptance criteria)
| Interface item | Minimum manufacturer evidence required | Accept/Reject criteria |
|---|---|---|
| Structural connection to foundations | Anchor bolt load drawings, baseplate drill template | Drill template matches site anchors within +/-10 mm and baseplate stiffness verified |
| Roof drainage | Gutter/downpipe size, overflow location, tie‑in detail | Calculated discharge rates match design rainfall; overflow prevents ponding |
| Finish and fasteners | Finish spec, fastener material, compatibility statement | Material pairing documented; coating thickness and adhesion data provided |
| PV mounting & electrical interface | Module clamp detail, cable routing, penetration seals | Clamps indicated for module type; penetrations shown with flashing and seal details |
| Shop drawings | 2D/3D drawings, revision log | All open comments closed and revision stamp applied |
Caveat on standards and calculations: require that any structural verification quoting code sections references the project’s governing standards (Eurocodes or national equivalents) and that load combinations are explicitly listed [1].
Procurement, factory evidence and inspection regimes
Procurement should be evidence‑driven. Contractually require the manufacturer to provide discrete, verifiable quality evidence at defined procurement gates.
Factory evidence matrix (what to require by contract)
- Material and mill certificates (traceable to batch/heat numbers).
- Production tolerances and dimensional control reports.
- Coating batch records including oven profiles and pre‑treatment checks.
- Torque and fastener assembly records.
- Pre‑shipment inspection checklist and photographic record.
- FAT protocol and results (dimensional checks, functional checks of moving parts, drainage trials where applicable).
- Packing and transport instructions, with bolstering points and handling diagrams.
Specifying inspection regimes
- Design approval: require manufacturer structural package sign‑off by licensed engineer for the project region.
- Pre‑production inspection (PPI): optional, for critical projects — client or third‑party can audit line readiness.
- In‑process inspection: supplier submits hold‑point photos and dimensional checklists.
- Pre‑shipment inspection (PSI): confirm assemblies, packaging and labelling on site before loading.
- On‑site inspection: require manufacturer representative or approved installer to perform fit‑up verification.
Factory audit checklist (sample items)
- Traceability system linking extrusions to mill certificates.
- Surface treatment process control (pre‑treatment, coating thickness monitoring).
- Welding procedure specification (if any) and welder qualification records.
- Calibration records for dimensional measuring equipment.
- QA/QC management system description (ISO references are acceptable; see ISO [4]).
Procurement contract language examples (do not copy verbatim; use for reference)
- "Supplier will provide mill certificates for all aluminium extrusions and confirm alloy and temper."
- "Supplier will present pre‑shipment inspection photographs and dimensional checks for all pre‑assembled modules."
- "Supplier will provide certified shop drawings and a signed statement of conformity from a licensed structural engineer prior to fabrication."
Note on certifications: require product and process statements that can be audited. Do not accept vague claims; insist on certificate numbers, dates and issuing bodies where appropriate. Where suppliers reference general standards, ask for specific clause conformance.
Mid‑article CTA If you need assistance converting your architectural performance brief into a procurement package or want a manufacturer QA checklist tailored to your project, contact us at /inquiry or info@carportiva.com.
Site installation and operations: from delivery to handover
Installation is where many specification failures manifest. Control this phase by clarifying responsibilities, acceptance criteria and practical logistics.
Installation readiness criteria
- Foundations and anchor templates accepted by the manufacturer or project structural engineer.
- Crane and plant schedule agreed, with lifting plans and certified slings and spreader bars.
- Weather and access contingency plans (hot, cold, wind restrictions).
- Labour competencies verified; installer certification or manufacturer training records supplied.
- Parts inventory and spares list delivered with site shipments.
- Site safety and temporary works plan signed off.
Typical installation phases and key checks
- Receiving and inspection: check counts, inspect packaging, record dents or transit damage.
- Baseplate and anchor verification: confirm bolt positions and elevations to tolerances.
- Erection of primary columns and beams: plumb and level checks; bolted connections torqued to spec.
- Secondary members and modules: cross beams, PV module rails and cladding fixed per torque charts.
- Roof finishes and drainage: gutters set, downpipes installed, water test where possible.
- Electrical and PV handover: verify module clamping, cable dressing, earthing, and DC combiner locations.
- Final alignment, sealant application and protective film removal.
- Practical completion inspection with manufacturer and client; create snag list and acceptance record.
Operational considerations and maintenance
- Provide an operations and maintenance manual covering routine checks (fastener torque, sealant condition), cleaning regimes for finishes, and spare parts list with part numbers.
- Define inspection intervals for drainage clearing and for PV canopy systems, module cleaning schedules, and thermal expansion checks for long spans.
Documented handover
- Require a signed handover pack with as‑built drawings, mill certificates, finish batch records, torque records and the installation completion certificate. This pack should be a contractual deliverable.
Implementation risk: common failure modes and mitigation
Understanding common failure modes lets you write effective risk controls into the contract.
Risk: ambiguous scope of responsibility
- Symptom: manufacturer assumes supply‑only; contractor expects fit‑up.
- Mitigation: contractual scope matrix that lists who is responsible for foundations, sealing, electrical, and crane hire.
Risk: mismatched materials or electrochemical incompatibilities
- Symptom: premature corrosion at fastener sites.
- Mitigation: require finish and fastener compatibility statements and specify insulating washers or sacrificial materials where needed [2].
Risk: drainage failures and ponding
- Symptom: water ponding on canopy, leaks at penetrations.
- Mitigation: require roof drainage coordination drawings and water tests before handover.
Risk: late shop drawing changes causing delays
- Symptom: manufacturing delays, additional costs.
- Mitigation: fixed shop drawing review windows and change order pricing rules; require revision logs.
Risk: insufficient QA at source
- Symptom: dimensional mismatches, missing parts on site.
- Mitigation: pre‑shipment inspection and photographic evidence; hold payments pending PSI completion.
Risk: installer skill gaps
- Symptom: improper torque, sealant application or alignment.
- Mitigation: require certified installers or manufacturer supervision during critical phases; include training and acceptance testing.
Risk: PV/electrical interface problems
- Symptom: module clamps incompatible, cable routing not accessible for maintenance.
- Mitigation: require PV mounting detail and electrical interface diagram during procurement; define electrical testing and earthing checks in handover.
How to price and allow contingencies
- Include explicit allowances for variations between tender documents and as‑built site conditions: a small contingency for anchor bolt repositioning works and a clear variation pricing schedule.
- Insist on fixed prices for supply of components where possible and separately priced installation rates.
Six‑step buyer workflow for selecting and contracting a modern carport manufacturer
This is a named, repeatable workflow for B2B buyers to follow — suitable for tenders, negotiated procurement, or single‑source supply.
Step 1 — Define project basis and minimum inputs
- Produce the documented project basis: site coordinates, geotechnical report, architectural intent and required standards. Circulate to shortlisted manufacturers.
Step 2 — Issue technical RFP with evidence requirements
- Request structural package commitments, mill certificates, finish evidence, and a detailed scope matrix that clearly states inclusions and exclusions.
Step 3 — Evaluate technical submissions against decision matrix
- Score submissions for structural capability, factory QA, finish compatibility, lead time, and logistics. Use the two decision tables in this guide as a template.
Step 4 — Conduct factory and sample inspections
- Arrange PPI or supplier audit for critical projects. Inspect sample extrusion, coated samples and representative bolted assemblies.
Step 5 — Finalise contract with gates and acceptance criteria
- Insert design approval, pre‑shipment inspection, delivery acceptance and installation readiness milestones. Include escrowed retainage linked to acceptance gates.
Step 6 — Manage installation and handover with QA records
- Use the installation readiness checklist, require manufacturer presence for first lift, and obtain a signed handover pack with as‑built drawings and QA records.
This workflow enforces the core decision principle: every technical claim is tied to a deliverable and an acceptance gate.
Frequently asked questions (FAQ)
Q: How prescriptive should I be about aluminium alloys? A: Prescribe the alloy family and temper suitable to your exposure and load requirements (e.g., 6000 series are common for structural extrusions). Always require mill certificates and a minimum mechanical property statement. The manufacturer should provide section properties and design allowable stresses in compliance with recognised standards [2].
Q: Can a supplier provide a generic design instead of site‑stamped calculations? A: Generic designs can be suitable for small, repeatable units where the buyer accepts a defined design envelope. For site‑specific projects, require stamped calculations by a licensed engineer for the project location. Eurocodes and national standards require design verification against local loads [1].
Q: How to handle finish warranties and maintenance? A: Request finish warranty terms in the contract and require evidence of coating process control. Warranties often come with maintenance conditions (cleaning, touch‑up). Avoid relying solely on length of warranty; require performance evidence and defined remedies.
Q: What's the typical scope of shop drawing review for architectural carports? A: Shop drawing review should include 2D and 3D geometry, connection details, drainage routes, PV mounting interfaces, and coordination with other trades. Define a time‑bound review cycle and require revision logs (shop drawing review).
Q: Who defines installation readiness? A: Installation readiness should be defined collaboratively between the client, installer and supplier in the contract: foundations toleranced, anchor bolts present, cranes available and weather windows agreed. The manufacturer should provide a checklist that the client signs off before arrival.
Q: Do I need to review finish and fastener compatibility? A: Yes — a compatibility statement (finish and fastener compatibility) is critical. Improper material pairings create galvanic corrosion risks and premature deterioration.
Q: How important is factory traceability? A: Traceability (mill certificates, batch numbers) is essential for warranties, recalls, and long‑term asset management. Require traceability records as part of the handover pack.
Conclusion: specifying to reduce uncertainty and cost over the asset lifecycle
Selecting a modern carport manufacturer is a procurement decision that sits at the intersection of architecture, structural engineering, manufacturing quality and installation logistics. By converting architectural intent into a testable architectural carport specification, by demanding aluminium profile selection evidence and finish/fastener compatibility statements, and by controlling shop drawing review and installation readiness through contractual gates, buyers materially reduce project risk and lifecycle cost.
- Insist on documented, auditable deliverables at each procurement gate.
- Require manufacturer evidence for materials, finishes and factories.
- Make installation readiness a contractual milestone, not an assumption.
Remember: site‑specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
If you would like tailored procurement support, specification templates or a manufacturer QA checklist aligned to your project, contact us at /inquiry or info@carportiva.com.
Further reading and standards
- Eurocodes for structural design guidance referenced for wind, snow and seismic principles [1].
- Guidance on aluminium materials and best practice from the Aluminium Association [2].
- Architectural finish and fenestration expectations — consult AAMA guidance where relevant [3].
- For QA system references and standard identification consult ISO standards [4].
Appendices (useful attachments to include in a tender)
- Draft technical specification template (materials, loads, finishes).
- Sample shop drawing review checklist.
- Factory inspection checklist and pre‑shipment inspection form.
This guide is part of Carportiva’s Architectural aluminium systems cluster; see all systems and our sourcing guides for complementary templates and procurement resources.
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion