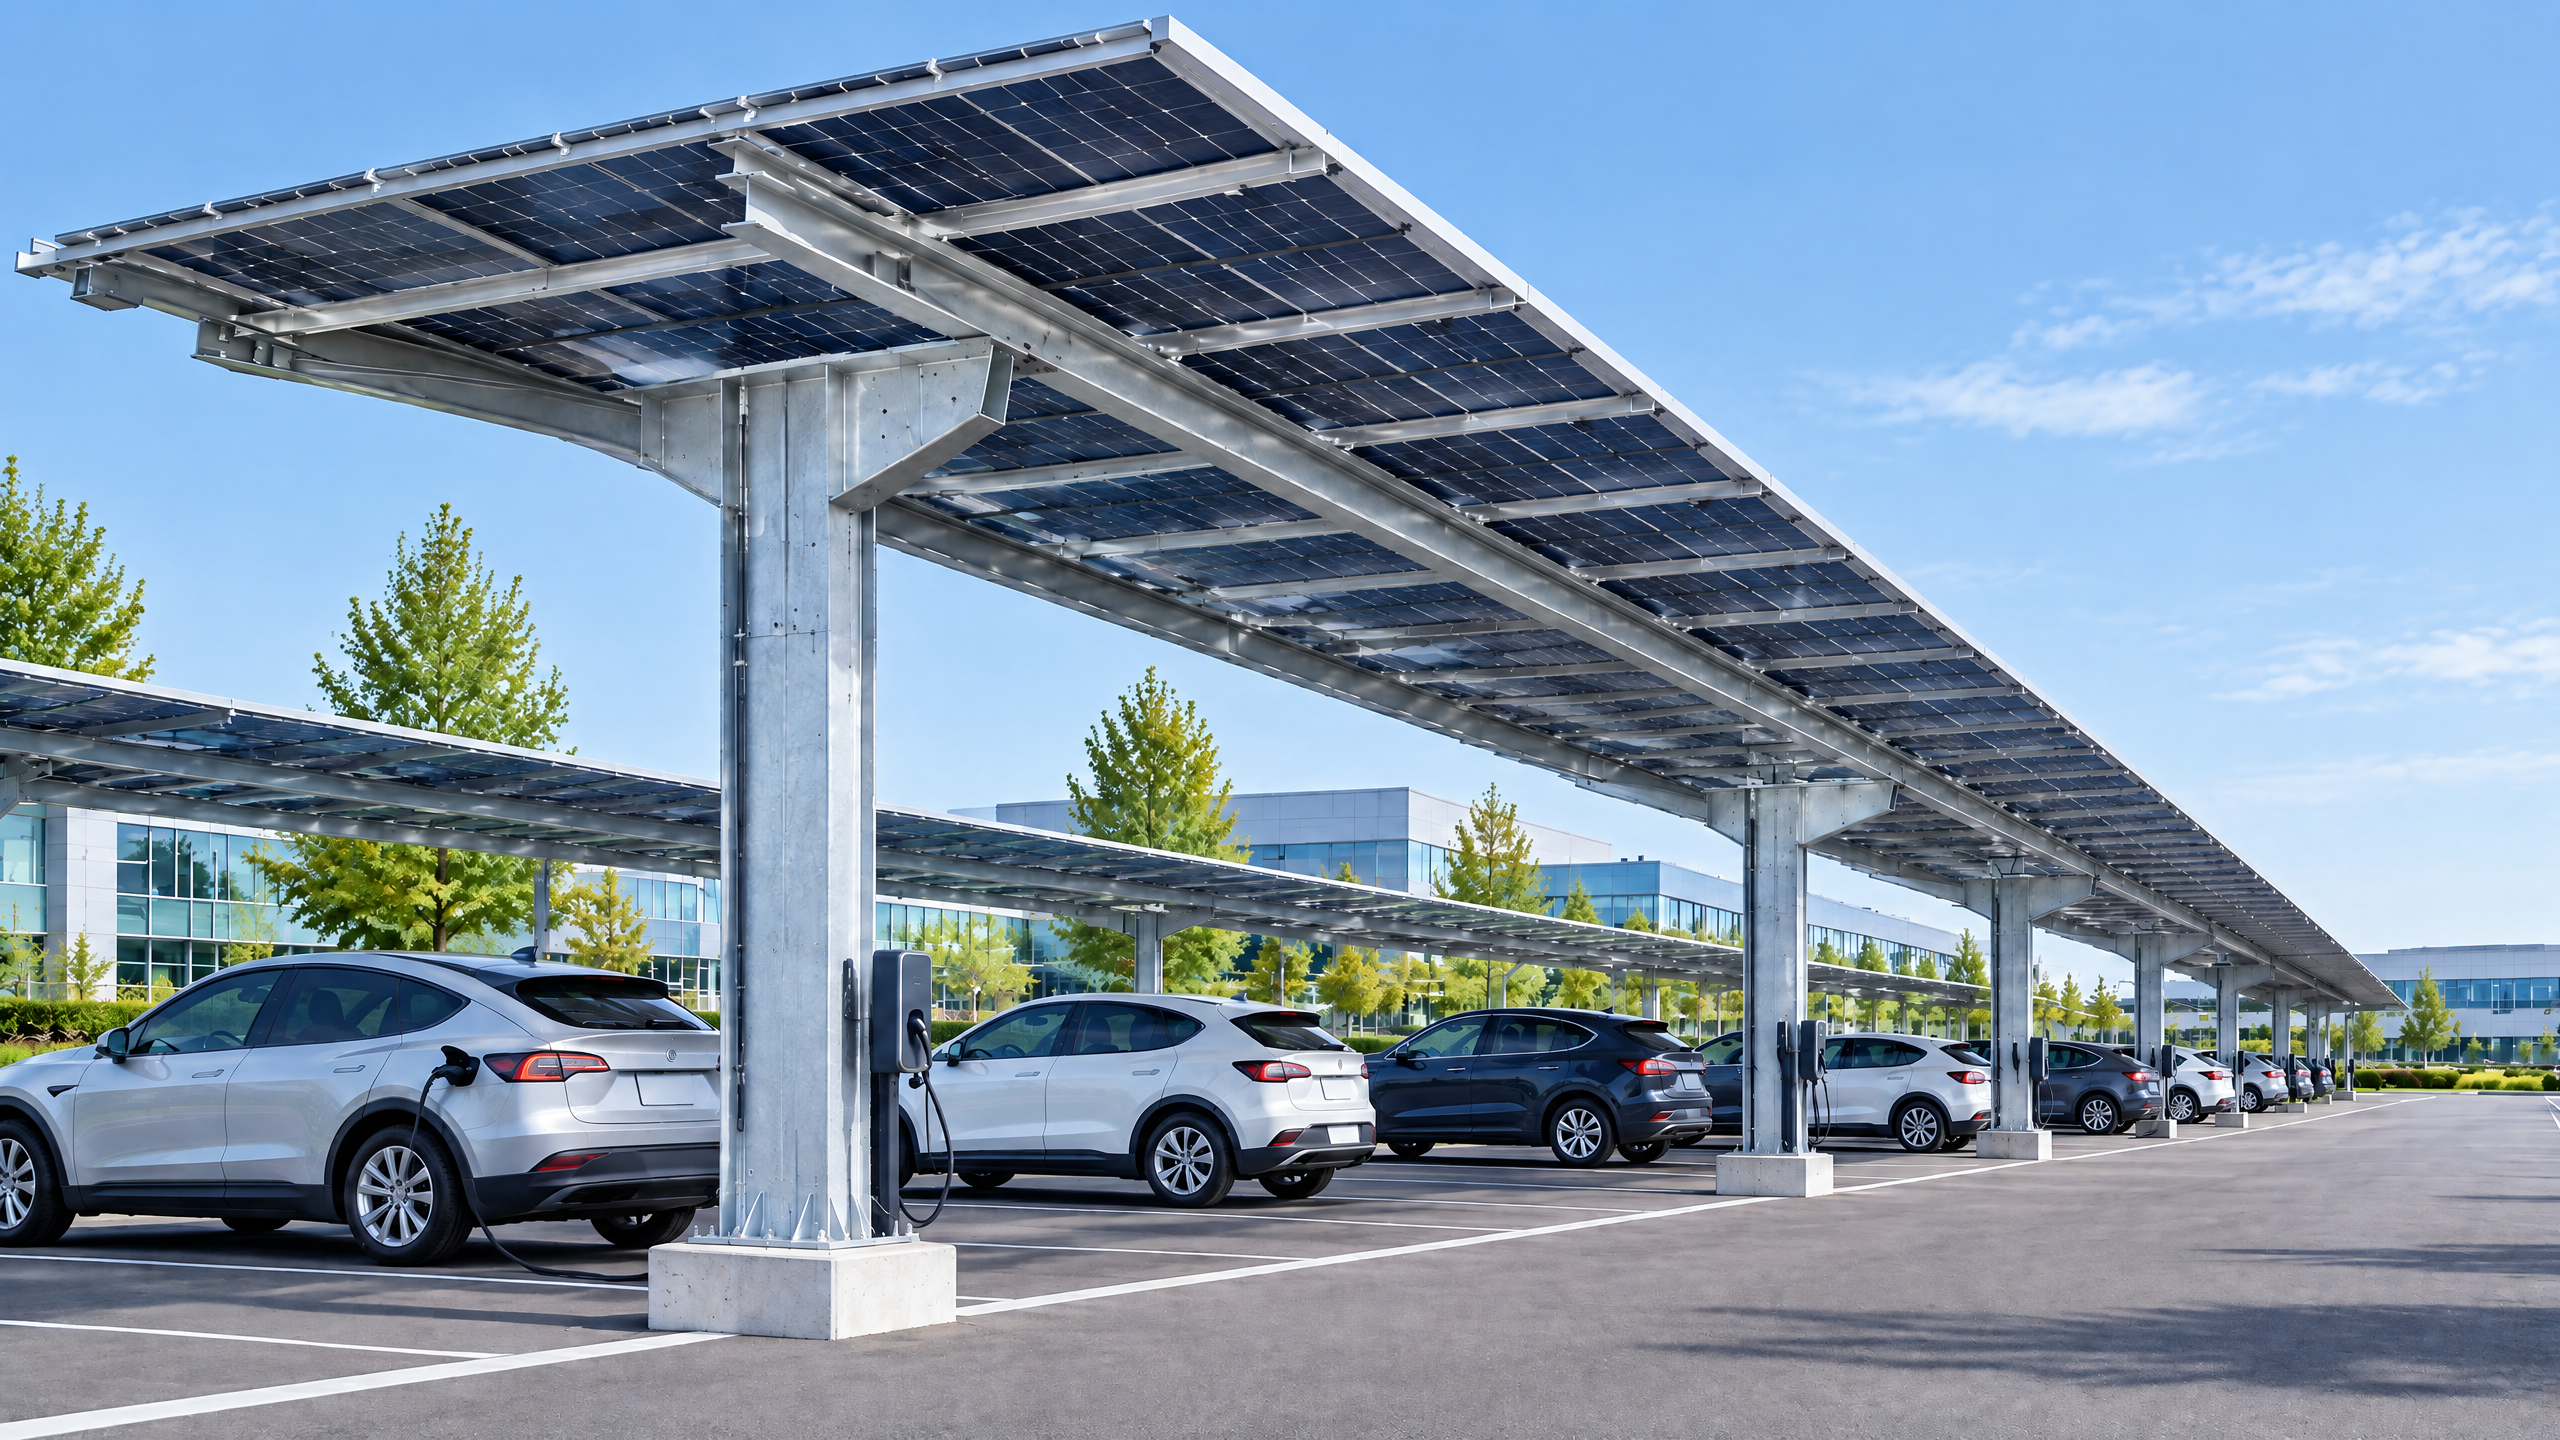
Direct answer (120–180 words): A project team must treat solar carport modules clamp zones as a primary technical control point that links PV modules, mounting rails, and the carport structure into a single load path. Confirming clamp zones means validating where clamps contact module frames, how that interface transmits wind, snow and uplift loads into the carport primary members, and whether the clamp positions are compatible with specific module frame geometries and rail systems. It also requires coordinated verification across structural, electrical and access disciplines so that grounding, wiring routes and maintenance clearances do not conflict with clamp locations. Practically, this means documented evidence: manufacturer mounting drawings, module mechanical datasheets showing allowable clamp zones, detailed connection load calculations, factory BOM and torque specifications, and a site-specific installation plan. In procurement and design conversations, insist on explicit supplier confirmation that clamp-zone details are compatible with the chosen carport beams, rails and module part numbers before fabrication.
Buyer context and scope boundary: why clamp zones matter to commercial carports
Solar carports are an integrated civil, structural and electrical assembly. For architects, EPCs, contractors, developers, distributors and fleet operators the clamp zone is a focused, high-impact detail:
- It is the mechanical contact area where modules are restrained and loads are transmitted into rails and structure.
- The clamp zone governs local bearing stresses on the module frame, the permitted locations for grounding clips and mid-clamps, and the spacing for wire runs beneath the module.
- Errors or ambiguity in clamp-zone definition lead to delayed installations, warranty disputes, on-site rework, or unsafe load paths.
This guide focuses specifically on solar carport modules clamp zones as the unique procurement and execution topic. It maps how clamp-zone confirmation intersects with the larger project responsibilities around solar carport structural interface, PV equipment coordination, electrical pathway planning, utility and permit interface, and maintenance access planning, so that commercial solar procurement decisions reduce risk and avoid hidden costs.
Important project boundary: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Core decision principle: verify documented compatibility before fabrication
Decision principle: do not commit to fabrication or module procurement until you have cross-checked the exact module frame, clamp type and clamp positions against the carport rail/beam geometry, with signed-off documentation from the carport supplier and the module/mount manufacturer.
Why:
- Fabrication is high-cost and cannot be reversed easily on site.
- Clamp-zone errors are often discovered only at fitment or after modules arrive; correcting them can mean remanufacturing rails or replacing module hardware.
- Clear, version-controlled documentation creates the contractual lever both for procurement negotiations and for warranty/acceptance testing.
What "documented compatibility" should include:
- Module mechanical datasheets with allowed clamp-zone locations and maximum clamping pressure or bearing width.
- Mounting system drawings indicating clamp interface, torque, fastener types, and allowed module frame thickness.
- Structural connection detail tying clamp loads into carport primary members, with load paths and calculations for wind/snow uplift, shear and bearing.
- Assembly and installation drawings showing maintenance clearances and wiring routes relative to clamp positions.
Planning inputs: what the team should collect and who should provide it
Collect these items early (procurement package / early design stage). Assign an owner for each item (EPC, structural engineer, carport vendor, module vendor, electrical designer).
- Module mechanical datasheet: owner = module vendor; includes frame cross-section, allowable clamp zones, recommended fastener types.
- Mounting-system drawings: owner = rail/mount vendor or carport supplier; includes rail geometry, clamp seating details, torque values, clamp height and material data.
- Carport structural drawings: owner = carport supplier/structural engineer; beam section sizes, hole schedules, flange thicknesses, and design load envelope.
- Site wind & snow loading envelope: owner = project structural engineer or local authority; necessary for clamp-load calculations.
- FEMA/local seismic requirements (if applicable): owner = structural engineer.
- Electrical single-line diagrams and string layouts: owner = electrical designer / EPC.
- Access and maintenance plan: owner = operations/facility manager; aisle widths, safe access points, and PV module removal strategy.
- Utility interconnection requirements and permit checklists: owner = developer/EPC; includes any restrictions that affect conduit routing or grounding arrangements.
- Schedule constraints and logistics: owner = project manager; lead times for modules, custom rails, and fasteners.
PV yield and energy calculations should be prepared using validated tools (for example PVWatts) and local irradiance data; treat energy yield as an input to sizing, not clamp-zone design [1][2].
Assign these roles in the project procurement notice and require confirmation from each owner before issuing final fabrication drawings.
Technical specification and interfaces: the detailed checklist for clamp zones
A clamp zone is not only a geometric location; it is a compound technical interface that must satisfy mechanical, electrical and serviceability requirements.
Key technical checkpoints
- Module compatibility
- Confirm module frame cross-section, flange width and sleeve geometry.
- Confirm permitted clamp locations (usually specified by module vendor) and any location forbidden due to junction-box, microinverter or optimizers.
- Ensure clamp pressure distribution avoids concentrated bearing exceeding the module frame’s allowable bearing stress.
- Clamp hardware and materials
- Specify clamp type (mid-clamp, end-clamp, top clamp, edge-clamp) and whether a protective pad or OEM-approved spacer is required.
- Material specification: list alloy and corrosion class (for example anodized aluminium or stainless steel options), and supplier material certificates to confirm composition.
- Fastening details: bolt grade, torque value, pre-load range and any required threadlocker or anti-corrosion treatment.
- Rail and beam interface
- Detail how clamp loads transfer into the rail and through to the carport primary members.
- Provide rail cross-section and T-slot or channel geometry; confirm clamp-to-rail seating and lateral restraint provisions.
- Where clamps connect directly to beams or bespoke extrusion shapes, provide finite-element or bolt-shear calculations when loads approach design limits.
- Grounding and bonding
- Confirm grounding clip positions relative to clamp zones, or alternate methods (separate bonding fasteners).
- Avoid placing grounding clips where they compromise clamp torque or module frame integrity.
- Verify continuity and single-point bonding requirements from clamp to structure per electrical design.
- Electrical pathway planning
- Map wire and conduit routes for module-to-junction box and string combiner boxes. Confirm that clamp locations do not obstruct cable trays, clip routes, or access to junction boxes.
- Reserve sufficient clearance and routing space under modules near clamp positions; confirm conduit penetration/wireways avoid clamp zones.
- Maintenance access planning
- Provide clear aisle widths and module removal zones; confirm clamps can be accessed with standard tools without removing neighboring modules unnecessarily.
- For optimized systems (power electronics beneath modules), confirm clamps do not touch or compress sensitive components.
- Environmental loads
- Account for wind uplift, snow, and thermal expansion. Clamp zones are part of the primary uplift-resistance strategy.
- For high-corrosion environments (coastal or chemical exposure), specify materials and finish treatments suitable for local conditions.
- Thermal expansion and differential movement
- Allow for longitudinal movement of rails relative to clamps where thermal expansion is significant; use slotted or floating clamp provisions where required.
- Anti-theft and tamper resistance
- Decide if security fasteners are required and verify that security fasteners still permit maintenance access.
- Documentation required
- Installation torque and sequence, clamp placement pattern, and photo-annotated installation checksheets.
Include all these items in the technical specification and require suppliers to respond point-by-point in bids.
Decision table: clamp-zone documentation and acceptance evidence
| Required document / evidence | Purpose | Acceptable evidence examples |
|---|---|---|
| Module mechanical datasheet | Identify allowed clamp locations and frame geometry | Manufacturer datasheet with drawing, allowed clamp-zone note |
| Mounting system detail drawing | Show clamp seating and rail geometry | CAD/Shop drawing with itemized part numbers and revision date |
| Clamp hardware certificate | Verify materials and finish | Mill test certificate or material declaration from supplier |
| Torque and installation procedure | Ensure proper preload and long-term behavior | Written installation procedure with torque values and sequence |
| Structural connection calculation | Confirm clamp loads are carried to primary members | Signed structural calculation or load check from structural engineer |
| Electrical bonding diagram | Verify clamp grounding or alternate bonding | Single-line with bonding points annotated; electrical acceptance test records |
Procurement and factory evidence: what to require from suppliers
In commercial solar procurement, you must turn requirements into contractual deliverables. For clamp zones, require explicit, verifiable factory evidence before signing off production.
Minimum procurement deliverables to require in bids and purchase orders:
- Bill of Materials (BOM) that specifies clamp part numbers, materials, and finish.
- Shop drawings (PDF and native CAD) showing clamp positions relative to module array, rail extrusions, and beam interface with revision control.
- Module vendor confirmation: written confirmation that the chosen clamp locations comply with the module’s allowed clamp zones for the module lot or model.
- Factory Quality Control (FQC) plan that includes clamp torque checks, clamp seating inspection process, and joining procedures executed at the factory or pre-assembly yard.
- Test samples and inspection protocol for the clamp-to-rail interface (visual, torque, and fit).
- Material traceability and certificates for corrosion-critical components.
- Packing and shipping plan that preserves clamp and rail geometry (avoid shipping-induced distortions).
Procurement contract wording (guidance):
- Require supplier to warrant that clamp-zone locations are compatible with the specified module make/model and any module changes require written approval.
- Include hold points in manufacturing where shop drawings and sample clamps are approved before full production.
- Include a rework and cost-liability clause for mismatches between approved drawings and delivered parts.
Document acceptance criteria quantitatively: allowable misalignment tolerance (e.g., ±X mm), and torque measurement tolerance ranges. Avoid qualitative-only acceptance.
Decision table: procurement hold points and acceptance triggers
| Hold point | Who approves | Documentation required | Consequence of failure |
|---|---|---|---|
| Pre-production shop drawing approval | Buyer and structural engineer | Approved shop drawings, module compatibility letter | No fabrication until approved |
| Sample clamp fit / mock-up | Buyer/EPC | On-site or factory mock-up photos, torque readings | Rework or sample replacement |
| Pre-shipment inspection | Buyer or third-party inspector | FQC sign-off, packing list, photos | Ship hold; corrective action required |
| Site acceptance | Site superintendent or EPC | As-built drawings, torque records, photographic evidence | Non-acceptance triggers remediation |
Require these hold points in the purchase order and the supplier quality plan.
Site installation and operations: installation checks and maintenance implications
Installation-phase confirmations
- Pre-installation verification: On site, verify that modules match the model stated on the approved drawings. Check module frame dimensions before mounting.
- Clamp placement checks: Use a template or jig derived from approved shop drawings to ensure consistent clamp placement across arrays.
- Torque verification: All clamped fasteners must be torqued to specified values. Document with calibrated torque wrenches and logged records.
- Grounding continuity: Measure and record continuity tests across clamped bonding points as per electrical acceptance criteria.
- Cable routing: Confirm that conduit and cable trays avoid clamp zones and that wire stress reliefs do not bear on module frames.
Maintenance and operations implications
- Access: Ensure maintenance staff can remove clamps and modules with standard tools without risk to adjacent modules. Document safe removal sequence.
- Spare parts: Maintain a stock of spare clamps and fasteners that match the installed lot and material treatment (do not substitute without verification).
- Inspection schedule: Include clamp and clamp-torque checks in regular PV operations inspections and in post-storm checks.
- Record keeping: Keep as-built clamp-zone drawings, torque logs, and photos for warranty claims and future audits.
Electrical pathway planning and routing must be coordinated with clamp locations to avoid rework. Ensure that any power optimizers, microinverters, or conduit entry points are located clear of clamp zones at design stage.
Implementation risk: common failure modes and mitigations
Common failure modes
- Mismatched module/model: Modules delivered that differ slightly in frame height or flange geometry from those used to design clamp placements.
- Incorrect clamp selection: Selecting clamps that produce excessive bearing stress on the module frame or that do not seat properly on the rail.
- Insufficient bolt torque: Under-torqued fasteners leading to movement and fatigue; over-torqued fasteners crushing module frame.
- Interference with electrical components: Clamps placed where they contact junction boxes, optimizers, or cable runs.
- Corrosion and material incompatibility: Galvanic corrosion at clamp-rail-module interfaces in mixed-metal assemblies, especially in coastal environments.
- Thermal expansion constraints: Rigid clamps preventing rail movement, causing stress cycles on module frames.
Mitigations
- Early mock-up: Build a small mock-up (one bay) with the chosen module and clamp hardware to validate fit and procedure.
- Approved sample policy: Require supplier to produce and ship approved clamp samples before full production.
- Vendor sign-off: Procure written confirmation from both module and clamp/rail vendors that the clamp solution is compatible with the specific module batch.
- Layered inspection: Use factory checks, pre-shipment inspection, and site verification to catch errors at the earliest point.
- Corrosion review: Specify compatible materials and coatings for the environment; require material certificates.
- Detailed as-built records: Maintain records to resolve disputes during warranty or performance issues.
Quantify risk allocation in the contract: identify which party is responsible for mismatches discovered on site, and how costs and times for remediation will be handled.
Six-step buyer workflow: confirm clamp zones with defensible evidence
Follow these named steps before committing to long-lead orders or final fabrication.
- Collect technical inputs
- Gather module datasheets, mounting system drawings, site wind/snow load, and structural member geometry.
- Preliminary compatibility review
- Carport supplier and module vendor perform an initial fit-check. Produce annotated shop drawings indicating proposed clamp zones.
- Mock-up and sample approval
- Fabricate a representative sample bay or clamp samples. Approve fit, seating and torque behavior.
- Contractualize clamp-zone requirements
- Insert hold-points in procurement documents. Require material certificates, BOM, and FQC plan before full production.
- Pre-shipment and site verification
- Conduct pre-shipment inspection and confirm module lot match. Perform on-site verification of clamp fit during first array installation.
- Install, test and document
- Torque checks, grounding continuity tests, and installation photos are filed. Confirm operational access and maintenance plan.
This workflow assigns clear responsibilities and creates decision points that prevent costly retrofit.
PV equipment coordination and utility/permit interface
PV equipment coordination
- Coordinate clamp-zone layout with other PV equipment: inverters, optimizers, junction boxes, combiner boxes, and cable trays.
- Identify fixed equipment locations during design so clamp positions can avoid conflicts with device footprints.
- For carports incorporating EV chargers or lighting, ensure these additional services do not conflict with clamp and conduit routes.
Electrical pathway planning and utility interface
- Early in design, produce conduit and cable trays routing plans showing relation to clamp zones and structural members.
- Discuss interconnection transformer locations and utility metering positions with utility contacts; certain transformer or meter placements may constrain conduit entries under modules. Engage the utility early to confirm preferred routing and any site-specific requirements [4].
- If the design requires underground duct banks through foundations or footings where clamps induce concentrated loading, coordinate foundation design with the structural engineer.
Permits and approvals
- Provide permit authorities with typical details showing clamp-to-structure connections to expedite structural and electrical permits.
- Some authorities require evidence of continuous bonding and certified torque records for rooftop or elevated PV installations—address these requirements through documented procedures.
Note: Utility interconnection and permitting processes vary significantly between jurisdictions. Allocate time in the schedule for permit reviews, utility studies and any modifications that impact clamp-zone arrangements.
Maintenance access planning
Maintenance access planning is frequently under-documented and directly affected by clamp zones.
Consider:
- Narrow aisles and overhanging clamps can impede module removal. Define the "module removal envelope" for each bay on as-built drawings.
- Tool access: specify whether standard tools (ratchet/torque wrench) can reach clamp fasteners in the installed position. If not, design service platforms or removable panels.
- Replacement strategy: for replacement modules, define whether adjacent modules must be temporarily removed or if clamps can be unfastened independently.
- Safety: include fall-protection attachment points or safe access procedures where clamps are located near edges.
Implement a maintenance manual that includes:
- Clamp torque values and the sequence for safe removal and reinstallation.
- Spare parts list and procurement contacts.
- Photographs indicating clamp locations and potential pinch points or cable conflicts.
Maintenance access planning must be coordinated with facility operations to minimize downtime and ensure that warranty procedures can be executed without prolonged outages.
FAQ: common buyer questions about clamp zones
Q: Why can’t we rely on generic clamps and assume they fit all modules? A: Module frame geometries and allowable clamp zones vary between manufacturers and even between product lines. Generic clamps may seat incorrectly, apply unacceptable bearing stress, or conflict with module-mounted electronics. Require manufacturer confirmation for the exact module model.
Q: Who signs off the clamp-zone structural calculations? A: The structural engineer of record (engineer-of-record) or a qualified structural engineer should sign off any calculations that demonstrate clamp loads are transferred safely into the primary structure.
Q: Are clamp torque values universal? A: No. Torque values depend on fastener grade, clamp geometry, substrate material, and use of washers or pads. Specify and document torque values; use calibrated tools.
Q: Can clamps be used as grounding points? A: Only if the module vendor and the electrical designer specify such use. Grounding via clamps must not compromise the mechanical integrity of the module or violate the module manufacturer’s warranty terms.
Q: What is a pre-assembly mock-up and is it necessary? A: A mock-up reproduces the clamp, rail and module in a representative bay to validate fit, torque behavior and installation sequence. It is a low-cost risk reduction step, highly recommended for new module/mount combinations.
Q: How do we address mixed-metal corrosion at the clamp interface? A: Specify compatible materials and finishes. Where dissimilar metals meet, consider insulating pads or coated fasteners and request material certificates. Include corrosion mitigation in the procurement specs.
Q: How much time should be allocated for clamp-zone coordination in the schedule? A: Time allowance depends on project complexity. As a rule of thumb, include design and approval hold points before fabrication and a mock-up phase—organize procurement so that clamp confirmation is complete before releasing long-lead orders.
Implementation risks and contract language to mitigate them
Risk transfer clauses to include in procurement documents:
- Module/Clamp compatibility warranty: supplier warrants that clamp hardware delivered is compatible with specified module models; changes to module models require written acceptance.
- Hold point enforcement: no fabrication before buyer-approved shop drawings and sample approvals are completed.
- Remediation liability: supplier accepts liability for rework costs if clamps or rails do not conform to approved shop drawings.
Recommended acceptance language:
- "Supplier shall provide factory FQC records, torque calibration certificates, and material certificates for all clamp hardware at time of pre-shipment inspection. Any variance from approved shop drawings discovered on site will be the supplier’s responsibility to remediate at supplier cost unless variance results from buyer-approved changes."
Escrow documentation:
- Store the final approved clamp-zone drawings, torque logs, and supplier confirmations in a central document repository to be used for warranty resolutions.
Remember: commercial solar procurement must include explicit contractual controls around clamp-zone design because retrofit costs are high.
Mid-article call to action
If you would like help translating clamp-zone requirements into shop drawings or procurement documents, contact our team for a project review and SolarGrid commercial solar system specification alignment. Start a conversation via /inquiry.
Practical examples (non-proprietary) and checklists
Use these checklists during design review meetings.
Design-review checklist
- Module model confirmed and datasheet on file.
- Module allowed clamp zone explicitly identified.
- Mounting rails and clamp hardware part numbers on shop drawings.
- Structural engineer sign-off on clamp load path and connection details.
- Grounding and bonding details annotated and approved.
- Maintenance removal envelope documented.
- Pre-shipment inspection and mock-up hold points scheduled.
Installation checklist
- Module Lot verification at site.
- Clamp seating template in use.
- Torque wrenches calibrated and torque log started.
- Grounding continuity test completed and logged.
- Cable routing and conduit clearance verified.
- Photographic record of installed clamps and module alignment.
Closing guidance: what to require in final deliverables
At project close, the buyer should take ownership of a complete handover package that includes:
- As-built clamp-zone drawings embedded in the as-built set.
- Torque logs and bonding continuity tests.
- Material certificates and FQC sign-off.
- Spare parts list and procurement sources for clamps and fasteners.
- Maintenance instructions and access planning documents.
These deliverables support operations and maintain the integrity of warranties and insurer requirements.
Final reminder about professional scope
Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities. Engage the structural engineer of record, a licensed electrical designer and your local permitting authority early for all final sign-offs.
Conclusion
Solar carport modules clamp zones are a small physical area with outsized influence on schedule, costs and long-term system reliability. For B2B buyers—distributors, architects, contractors, developers, solar EPCs and fleet operators—the right approach is disciplined, evidence-led confirmation: specify clamp-zone requirements clearly in procurement documents, obtain vendor and module manufacturer confirmations, use mock-ups and hold points to avoid surprises, and document everything for operations and warranty. Integrate clamp-zone verification with PV equipment coordination, electrical pathway planning, utility and permit interface, and maintenance access planning so that the carport functions as a single coordinated system.
For more information about system options and integration guidance, see our all systems page and consult our sourcing guides. If you want a detailed project review tied to SolarGrid commercial solar system options, contact our team at info@carportiva.com.
FAQ (continued): quick-reference answers
Q: Who should approve the clamp-zone shop drawings? A: Buyer, structural engineer of record and the module vendor (or their authorized representative) should approve.
Q: Are clamp-zone mock-ups reimbursable? A: That is a contractual question; many buyers treat mock-ups as part of the supplier’s responsibility or as a reimbursable change order if not included in original scope.
Q: What if the module manufacturer updates their datasheet after procurement? A: Treat product changes as a potential change order. Contract should require notification of relevant module changes and re-approval for clamp compatibility.
References
- For irradiance, energy yield and PV performance modeling, consult public PV resources such as the National Renewable Energy Laboratory (NREL) and PVWatts [1][2].
- For equipment siting and interconnection considerations, consult local utility guidance and the Federal Energy Regulatory Commission interconnection resources where appropriate [4].
- For EV and alternative fuel infrastructure coordination at carports, reference national alternative fuels resources where applicable [3].
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion