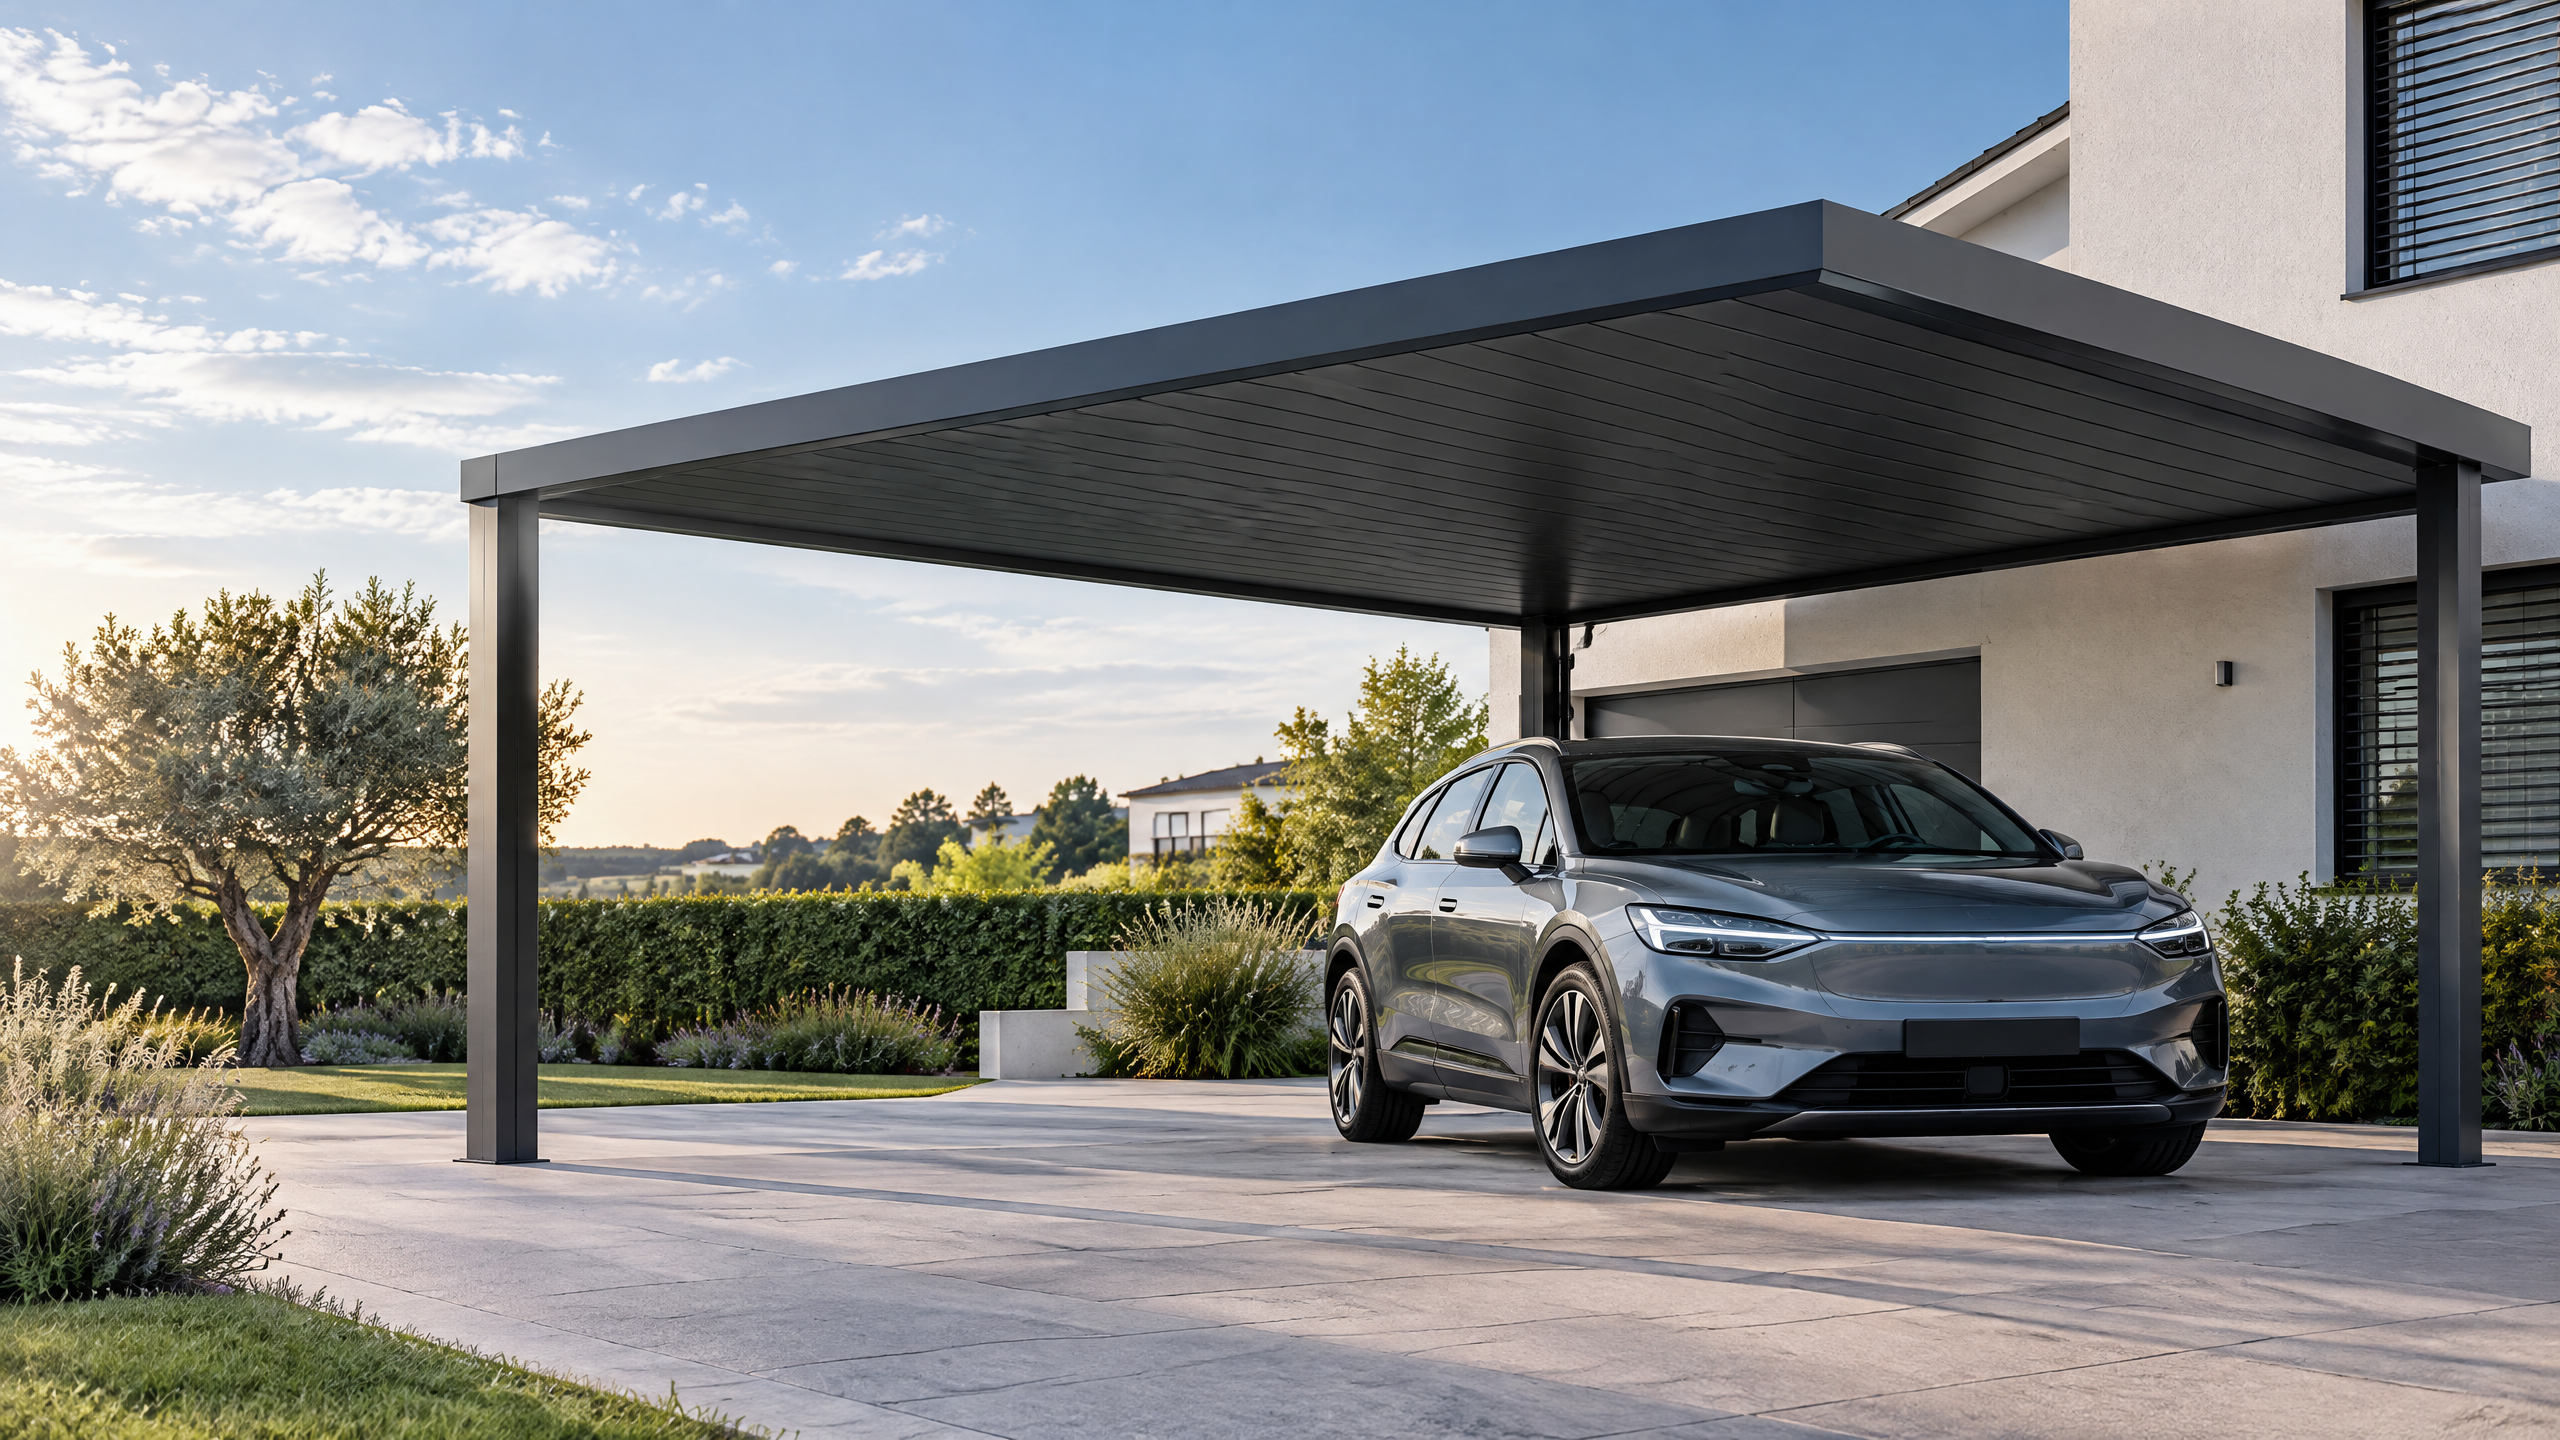
Deciding how to specify an aluminium carport canopy factory begins with treating the factory as an extension of the project delivery team: the factory must deliver engineered components, verified shop drawings and installation-ready assemblies that integrate with site foundations, services and local approvals. A concise, evidence-based specification clarifies performance requirements (structural loads, weather, corrosion, finish, attachment interfaces), factory capabilities (rolling, extrusion, fabrication, quality systems), and acceptance criteria (material certificates, dimensional tolerances, shop drawing review, packaging and logistics). For commercial carports — including solar and fleet shelters — early alignment on aluminium profile selection, roof drainage coordination, finish and fastener compatibility and electrical/PV interfaces reduces on-site risk and schedule friction. This guide sets a practical procurement and implementation approach: what inputs to gather, which technical interfaces to resolve in the factory, what factory evidence to require, how to judge installation readiness, and a six‑step buyer workflow you can apply to global procurement decisions.
Buyer context and scope boundary: what the factory should deliver versus what the client must provide
Clarify responsibilities early. Typical boundary lines that should be documented in procurement and contract documents:
- Factory responsibility (deliverable examples)
- Extruded and fabricated aluminium profiles, brackets and roof assemblies.
- Shop drawings, connection details, and packing lists.
- Pre-assembled modules or subassemblies to agreed dimensional tolerances.
- Material traceability documents and mill certificates for alloys used.
- Coating or anodizing to specified finish standards and documented process controls.
- Lifting and handling instructions for safe site receipt and erection.
- Client / project team responsibility (deliverable examples)
- Site-specific structural capacity verification, foundation design and soil reports.
- Local permits, planning approvals and utility connections.
- Electrical design and PV layout (if solar carport), including conduit routes and inverter locations.
- On-site installation labour, scaffolding/crane, and temporary works.
- Final acceptance tests on site (e.g., drainage, electrical interconnection, PV commissioning).
Note: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Defining these boundaries prevents scope gaps — for example, whether the factory supplies post‑installed anchors, sealants or only pre-drilled anchor plates. Including a clear Appendix A (Responsibilities Matrix) in the procurement package reduces later claims and delays.
Core decision principle: balancing standardisation, modularisation and project-specific engineering
The primary commercial decision when specifying an aluminium carport canopy factory is how much you rely on standard product families versus custom engineering. There are three common strategies:
- Standardised modular systems:
- Faster procurement, lower unit cost and predictable supply chain.
- Best for repeatable projects or large distribution rollouts.
- Requires the factory to hold stock of profiles and finishes.
- Semi-custom (engineered variants of standard systems):
- Useful where spans, roof pitch or clearances differ but common interfaces remain.
- Balances cost control and site adaptation.
- Fully bespoke engineered systems:
- Required where architectural intent or complex site constraints exist.
- Higher lead time and engineering cost; requires thorough shop drawing review and factory engineering capacity.
Decision table — selecting the right approach
| Project objective | Recommended approach | Typical factory capability to require |
|---|---|---|
| Speed and repeatability (multiple sites) | Standardised modular systems | Stocked profiles, configurable modules, short manufacturing lead times |
| Site-specific adaptation (unique spans/pitches) | Semi-custom (variants) | Design-for-manufacture engineering and configurable jigs |
| Signature architecture or irregular geometry | Fully bespoke | Dedicated engineering team, finite element analysis capability, workshop prototyping |
Concrete selection depends on cost, schedule, available site tolerances and the acceptable level of design risk. Even standardised systems require project-specific checks for structural loads and roof drainage.
Planning inputs: the minimum data package to give an aluminium factory
A competent factory needs a consistent minimum information package to produce accurate shop drawings and quotations. Provide this information up front to avoid scope drift:
- Site and project identity
- Project name, address, local authority, primary contact and document control references.
- Site survey deliverables
- Topographic survey and finished floor levels.
- Vegetation, adjacent structures and access restrictions for delivery/cranage.
- Geotechnical and foundation information
- Soil report, recommended bearing pressures, existing underground services and any constraints on piling or excavation.
- Structural design inputs and load cases
- Design live loads, snow and wind loads (or jurisdictional load cases). Reference applicable standards (e.g., Eurocodes where used) [1].
- Seismic parameters where relevant.
- Clearance and operational envelopes
- Vehicle clearance requirements, aisle widths, lighting, signage and any fleet-specific dimensions.
- Roof and drainage data
- Rainfall intensity and local drainage strategy; indicate roof pitch, gutter locations and stormwater outlet points.
- Drainage interface elevations to enable roof drainage coordination.
- Building services and electrical design
- Conduit runs, inverter and metering positions (for solar carports), and where factory-supplied cable penetrations are required.
- Architectural finish expectations
- Color references (RAL, BS), intended coating type (specify performance requirements rather than brand names), and finish and fastener compatibility requirements.
- Project delivery constraints
- Target dates for delivery and site installation windows, site access constraints and expected on-site storage capacities.
- Contractual and regulatory constraints
- Permitting conditions, local approvals to be satisfied and designated inspection authorities.
Provide these inputs as a coordinated package. A missing datum — e.g., required drainage invert elevation — is a common cause of rework and site delays.
Technical specification and interfaces the factory must resolve
A factory’s scope should include not only fabrication but also engineering and interface coordination. Below are critical technical areas to define and the verification you should require.
Structural design and materials
- Specify acceptable aluminium alloys (reference material standards) and require mill certificates for each delivery. The Aluminum Association provides guidance on alloy selection and properties that you may reference for material characteristics [2].
- Specify connection design parameters and allowable tolerances; require calculations or engineer’s stamp when local regulation demands.
Aluminium profile selection
- Define load-bearing profiles, secondary members and roof purlins by functional requirement rather than only by cross-section. The phrase aluminium profile selection should appear in procurement to ensure the factory confirms extrusions meet the structural requirements.
- State tolerances for bends, straightness and hole locations; require dimensional inspection reports for profile runs.
Surface finishes and fasteners
- State finish performance criteria (e.g., expected outdoor exposure class, color retention, chalking limits) rather than brand names; reference finish standards (see AAMA guidance for coating performance standards) [3].
- Specify finish and fastener compatibility to avoid galvanic corrosion — aluminium components must be isolated or use compatible fasteners/coatings. Fastener material, plating and head type should be specified to match exposure and structural load needs.
Roof systems and drainage
- Define roof cladding type (e.g., profiled metal, composite panels, glazing), its water-tightness criteria and interface details.
- Require roof drainage coordination: factory must confirm gutter sizes, outlet locations and downpipe fixation compatible with site drainage elevations.
- Require details of saddles, expansion joints and continuous seals at junctions.
Shop drawing review
- Shop drawing review must be a contractual milestone. The factory should submit detailed shop drawings showing all connections, cut lengths, welds, hole positions and assembly marks. The buyer’s engineer or architect should log comments within an agreed review period.
Electrical and PV interfaces (if applicable)
- For commercial solar carports, define PV module mounting interface, cable trays, earthing/grounding provisions and locations for DC and AC equipment. Factory scope may include PV mounting rails but usually not the PV modules or inverters unless specified.
- Clarify whether the factory will provide pre-cut conduits or sleeves through roof members for on-site wiring.
Tolerances and pre-assembly
- Define acceptable dimensional tolerances for factory pre-assembled modules and site assembly tolerances. Purchasing officers should require a tolerance table as part of the factory submission.
Thermal and acoustic considerations
- If climatic control, condensation risk or acoustic attenuation are concerns, state these requirements and require the factory to propose mitigation (thermal breaks, drainage paths, acoustic liners).
Testing, documentation and marks
- Require non-proprietary evidence: material mill certificates, coating batch documentation, dimensional inspection reports and packing lists.
- Require a single-point packing list and an assembly index keyed to shop drawings so site crews can identify components immediately on receipt.
Decision table — technical verification checklist for factory submittals
| Submittal item | Minimum evidence required | Who verifies |
|---|---|---|
| Material certificates | Mill/test certificates for alloys delivered | Buyer’s materials engineer or third party |
| Shop drawings | Full assembly drawings, connection details, cut lists | Buyer’s architect/engineer (shop drawing review) |
| Finish process | Coating/anodizing process description and batch documents | Buyer’s specifier or independent coatings lab if required |
| Dimensional inspection | Tolerance report and pre-assembly trial / photograph evidence | Buyer’s site manager or QA representative |
| Packaging & logistics | Packing list, handling instructions, lifting points | Buyer’s logistics coordinator |
Include acceptance criteria and review turnaround times in the purchase order to avoid late changes.
Procurement and factory evidence: what to require and how to assess it
Procurement for architectural aluminium systems should emphasize verifiable factory capability and documented evidence. Consider these procurement levers:
Factory capability and capacity
- Request evidence of extrusion capacity, machining capability, and finishing capacity (anodizing/coil coating outsourced or in-house). For complex or large projects, ask for a capacity plan or floor layout to judge production flow and potential bottlenecks.
- Ask for references for similar scope (not inventing projects) and request contactable referees; validate with site visits where possible.
Quality management and traceability
- Require documented quality management processes. If the factory claims ISO or similar certification, request certified copies and confirm scope (e.g., ISO 9001 for quality management) using public records [4].
- Require traceability lists that map profiles to mill certificates and heat numbers.
Fabrication controls and tolerances
- Ask for typical tolerance tables used by the factory and examples of previous shop drawing coordination logs.
- Require evidence of jigs or fixtures that ensure repeatable accuracy for critical assemblies.
Logistics and deliveries
- Require a delivery and installation plan: number of crates, weight per crate, special handling requirements and expected delivery windows. Ensure the factory specifies lead time from approval of final shop drawings.
Commercial terms and warranties
- Require clear terms for latent defects, corrosion beyond normal exposure, and finish performance; ensure warranty scope is explicit in contractual terms. Do not accept vague warranty language; request written conditions.
Factory acceptance and pre-shipment checks
- Define pre-shipment acceptance tests and inspections (dimensional checks, coating inspection, packaging inspection). Specify whether buyer or third-party inspection is permitted and whether witness points are required.
Evaluating factory evidence — a scoring example (procurement tool)
- Technical capability (30%)
- Quality systems and traceability (20%)
- Delivery performance and logistics (15%)
- Financial and commercial stability (10%)
- Past project fit and references (15%)
- Responsiveness and engineering support (10%)
Use weighted scoring during tender evaluation and keep technical scoring separate from commercial scoring to avoid conflating price with technical compliance.
Mid-article CTA: For project-specific guidance and to review how NordArch architectural aluminium system can be configured for your project, contact our team via /inquiry or info@carportiva.com.
Site installation, logistics and commissioning: confirming installation readiness
Installation readiness is a critical milestone and must be explicitly stated in contracts. The exact activities that confirm installation readiness include:
- Foundations: certified construction of foundations and anchor pads to the factory’s template and within allowable tolerances.
- Crane and access: confirmation of crane lift plan, approach routes and temporary storage areas.
- Site consumables: confirmation that required site consumables (sealants, fasteners if provided by installer, site-applied touch-up paint) are available.
- Pre-delivery inspections: check of incoming components against packing list; identify damage and reconcile missing items.
- Erection tolerances: alignment templates and shims to manage deviations between factory datum and site conditions.
- On-site verification of drainage interfaces and conduit penetrations.
- Safety and training: induction of site erectors, access to erection drawings, and confirmation of fall protection and edge protection measures.
Installation readiness is not just a checklist; it is a contractual milestone linking factory delivery to on-site acceptance. Include a closing procedure that requires sign-off by the site engineer and factory representative where appropriate.
Practical tips for minimizing site risk
- Deliver in sequence aligned with erection schedule to avoid on-site damage.
- Label all components with item numbers matching shop drawings for rapid identification.
- Provide a dedicated “kit” for critical nodes (e.g., baseplates, anchor bolts, hex keys) and a small spares pack for damage or loss.
- If factory provides pre-drilled holes for anchors, ensure anchor sleeve type and bolt length are verified against foundation contractor’s as-built conditions.
Implementation risk and mitigation: common failure modes and how to avoid them
Identifying risks early allows buyers to create practical mitigation plans.
- Tolerance mismatch between foundation and factory datum
- Risk: Misaligned columns leading to rework.
- Mitigation: Provide foundation templates and require the factory to confirm anchor plate dimensions and hole locations; require a flexible connection detail for minor deviations.
- Corrosion due to incompatible finishes and fasteners
- Risk: Galvanic corrosion between dissimilar metals.
- Mitigation: Specify finish and fastener compatibility and require passivation or non-conductive barriers where dissimilar metals meet.
- Insufficient roof drainage
- Risk: Ponding, leaks and premature coating failure.
- Mitigation: Confirm roof drainage coordination with local rainfall data and factory-provided outlet locations; require flow calculations for gutter sizing.
- Incomplete electrical/PV interface documentation
- Risk: On-site delays because of missing conduit penetrations or incorrect cable trays.
- Mitigation: Integrate PV and electrical designers into the shop drawing review process and require factory provision of sleeves and penetrations as specified.
- Logistic constraints and damage in transit
- Risk: Damaged extrusions or assemblies on arrival.
- Mitigation: Require factory packing standards, shock indicators on crates for critical shipments, and photographic evidence of packaging.
- Long lead-times and single-supplier bottleneck
- Risk: Program slippage if a single factory cannot meet schedule.
- Mitigation: Stagger orders, maintain a contingency supplier list, or select a factory with proven capacity planning.
- Regulatory and permitting changes
- Risk: Mid-project code updates requiring rework.
- Mitigation: Include a change control clause, and require the factory to provide drawings stamped by local engineers when necessary.
Document these risks in a project Risk Register and assign owners and mitigations before procurement.
Six-step buyer workflow for procuring from an aluminium carport canopy factory
A repeatable workflow helps buyers reduce ambiguity. Name: Six-step Factory Procurement Workflow for Commercial Carports
Step 1 — Project definition and scope freeze
- Deliverables: Project brief, scope matrix (who does what), and procurement schedule.
- Action: Freeze critical inputs (site survey, loads, drainage invert levels).
Step 2 — Pre-qualification and factory selection
- Deliverables: Pre-qualification questionnaire, site visit notes, capability scoring.
- Action: Evaluate extrusion, fabrication and finish capabilities; request references and evidence.
Step 3 — Concept alignment and preliminary drawings
- Deliverables: Concept elevation and load summary.
- Action: Ask the factory to confirm feasibility and provide indicative costs.
Step 4 — Detailed design and shop drawings
- Deliverables: Final shop drawings, cut lists, tolerance schedule and packaging plan.
- Action: Initiate shop drawing review with deadlines; resolve PV and drainage interfaces.
Step 5 — Manufacturing, QA and pre-shipment verification
- Deliverables: Material certificates, dimensional inspection reports, photographs of pre-assembled modules.
- Action: Conduct witness inspections or third-party checks if required; confirm packing and transport.
Step 6 — Delivery, installation and handover
- Deliverables: Delivery sign-off, installation as-built drawings, maintenance manuals and spare parts list.
- Action: Confirm installation readiness, perform site acceptance and handover of responsibility.
This workflow should be codified into the purchasing contract with acceptance criteria at each step and defined review durations.
Related B2B sourcing terms
For the same project brief, buyers may also encounter these connected search terms: architectural carport specification. They must be interpreted against the actual project scope rather than treated as independent technical guarantees.
FAQ — practical buyer questions
Q: What is the most important single document to get from the factory? A: Detailed shop drawings that include all connection details, anchor templates and a keyed parts list. This is the main document used to validate manufacturing and installation.
Q: How do I specify corrosion resistance for a coastal site? A: Specify the exposure category, expected lifespan and finish performance rather than a nominal coating. Require compatible fasteners and, for critical joints, isolation barriers. Reference finish performance standards and consult a corrosion engineer for severe marine environments [3].
Q: Does the factory usually supply anchor bolts? A: It depends on the contractual boundary. Clarify in the responsibility matrix. When factories supply anchors, require anchor bolt setting templates and bolt QA certificates.
Q: Can a single factory manage both structural aluminium and PV mounting hardware? A: Many factories can provide structural members and PV mounting rails, but PV modules, inverters and electrical commissioning are typically supplied by an electrical contractor or solar EPC. Define the exact scope in the contract.
Q: What standards should be referenced for structural design? A: Use jurisdictional standards. For European projects, Eurocodes provide harmonised structural rules and load combinations [1]. For material and manufacturing references, consult aluminium and finish standards [2][3].
Q: How to handle changes discovered after shop drawing approval? A: Create a formal change control process with pricing and time impacts. Minor dimensional variations may be handled with approved field modification details, but structural changes require re-engineering.
Q: Should I require factory witness testing? A: For critical structural components or large-batch runs, third-party or buyer witness inspections add confidence. Define which stages require witness points in the contract.
Q: Where do I find standard product families to compare? A: Review factory product literature and system catalogues. For broader options across Carportiva’s portfolio, see all systems and sourcing guides.
Procurement checklist: a condensed buyer-ready list
- Confirm project-specific inputs: site survey, geotech, loads, clearances, electrical/PV layout.
- Issue a pre-qualification questionnaire to factories.
- Require shop drawing review milestones and turnaround times.
- Demand material traceability and mill certificates.
- Specify finish performance and ensure finish and fastener compatibility.
- Insist on packing, delivery sequencing and installation readiness documentation.
- Establish acceptance criteria at delivery and for site handover.
- Include contingency and change control clauses.
Useful decision tables and selection comparisons
Table — Factory capability vs buyer requirement (scoring guide)
| Requirement | Critical? | Evidence to request | Pass/Fail |
|---|---|---|---|
| Extrusion capacity for specified profiles | Yes | Production capacity statement, sample extrusions | |
| Machining accuracy for hole/slot locations | Yes | Tolerance tables, inspection reports | |
| Coating/anodizing quality | Yes | Coating process description, batch docs, AAMA reference | |
| Engineering support for bespoke details | Medium | CVs of engineering leads, examples of complex shop drawings | |
| Packing and logistics for site sequence deliveries | Medium | Delivery plan and packing list |
Table — Finish and fastener decision comparison
| Finish type | Typical durability (outdoor) | Fastener compatibility | Pros | Cons |
|---|---|---|---|---|
| Powder coat (polyester/PVDF) | High when specified to performance standards [3] | Use stainless steel fasteners or coated steel with isolation | Wide colour range; good UV resistance | May require touch-up for cutting/exposure at edges |
| Anodized | Good corrosion resistance for marine and harsh environments | Compatible with stainless fasteners; avoid bare steel | Durable and abrasion resistant; natural metallic look | Limited colour range; not suitable for deep colours |
| Mechanical galvanic isolation (barrier tape, polymer washers) | N/A (method, not finish) | Enables use of dissimilar metals without galvanic action | Prevents galvanic corrosion | Adds labour and must be specified consistently |
Note: The table is a guide—specify performance criteria and require factory to confirm compatibility in shop drawings.
Final considerations: legal, procurement and technical best practices
- Contractual clarity: Make sure purchase orders link to the approved shop drawings, include acceptance criteria and define remedy for defects.
- Staged payments: Link payments to milestones such as shop drawing approval, production start, pre-shipment inspection and on-site acceptance.
- Insurance and indemnity: Confirm transport insurance and site erection liability in the contract.
- Training and manuals: Require the factory to provide installation manuals, as-built drawings and maintenance schedules.
- Spare parts and lifecycle planning: Agree a spare parts kit and lead time for replacement profiles and finish options.
Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Conclusion — specifying the right aluminium carport canopy factory for commercial success
Specifying an aluminium carport canopy factory is an exercise in reducing ambiguity: define clear responsibilities, supply a coordinated technical input package, require verifiable factory evidence (materials, drawings, process controls), and manage interfaces (roof drainage coordination, electrical/PV, foundations) up front. Emphasise shop drawing review, agree installation readiness milestones, and use the six-step buyer workflow to make the procurement process repeatable and auditable. When architectural intent or sustainability outcomes are central, involve architects, structural engineers and local authorities early and use documented evidence to support decisions.
For assistance aligning factory capabilities with your project requirements or to discuss how Carportiva’s product range can be configured — including the NordArch architectural aluminium system — contact our team via /inquiry or info@carportiva.com.
References (examples of public standards and guidance)
- Eurocodes and structural design guides [1]
- Material and alloy guidance from The Aluminum Association [2]
- Architectural coating performance guidance from AAMA [3]
- ISO certification and standard references [4]
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion