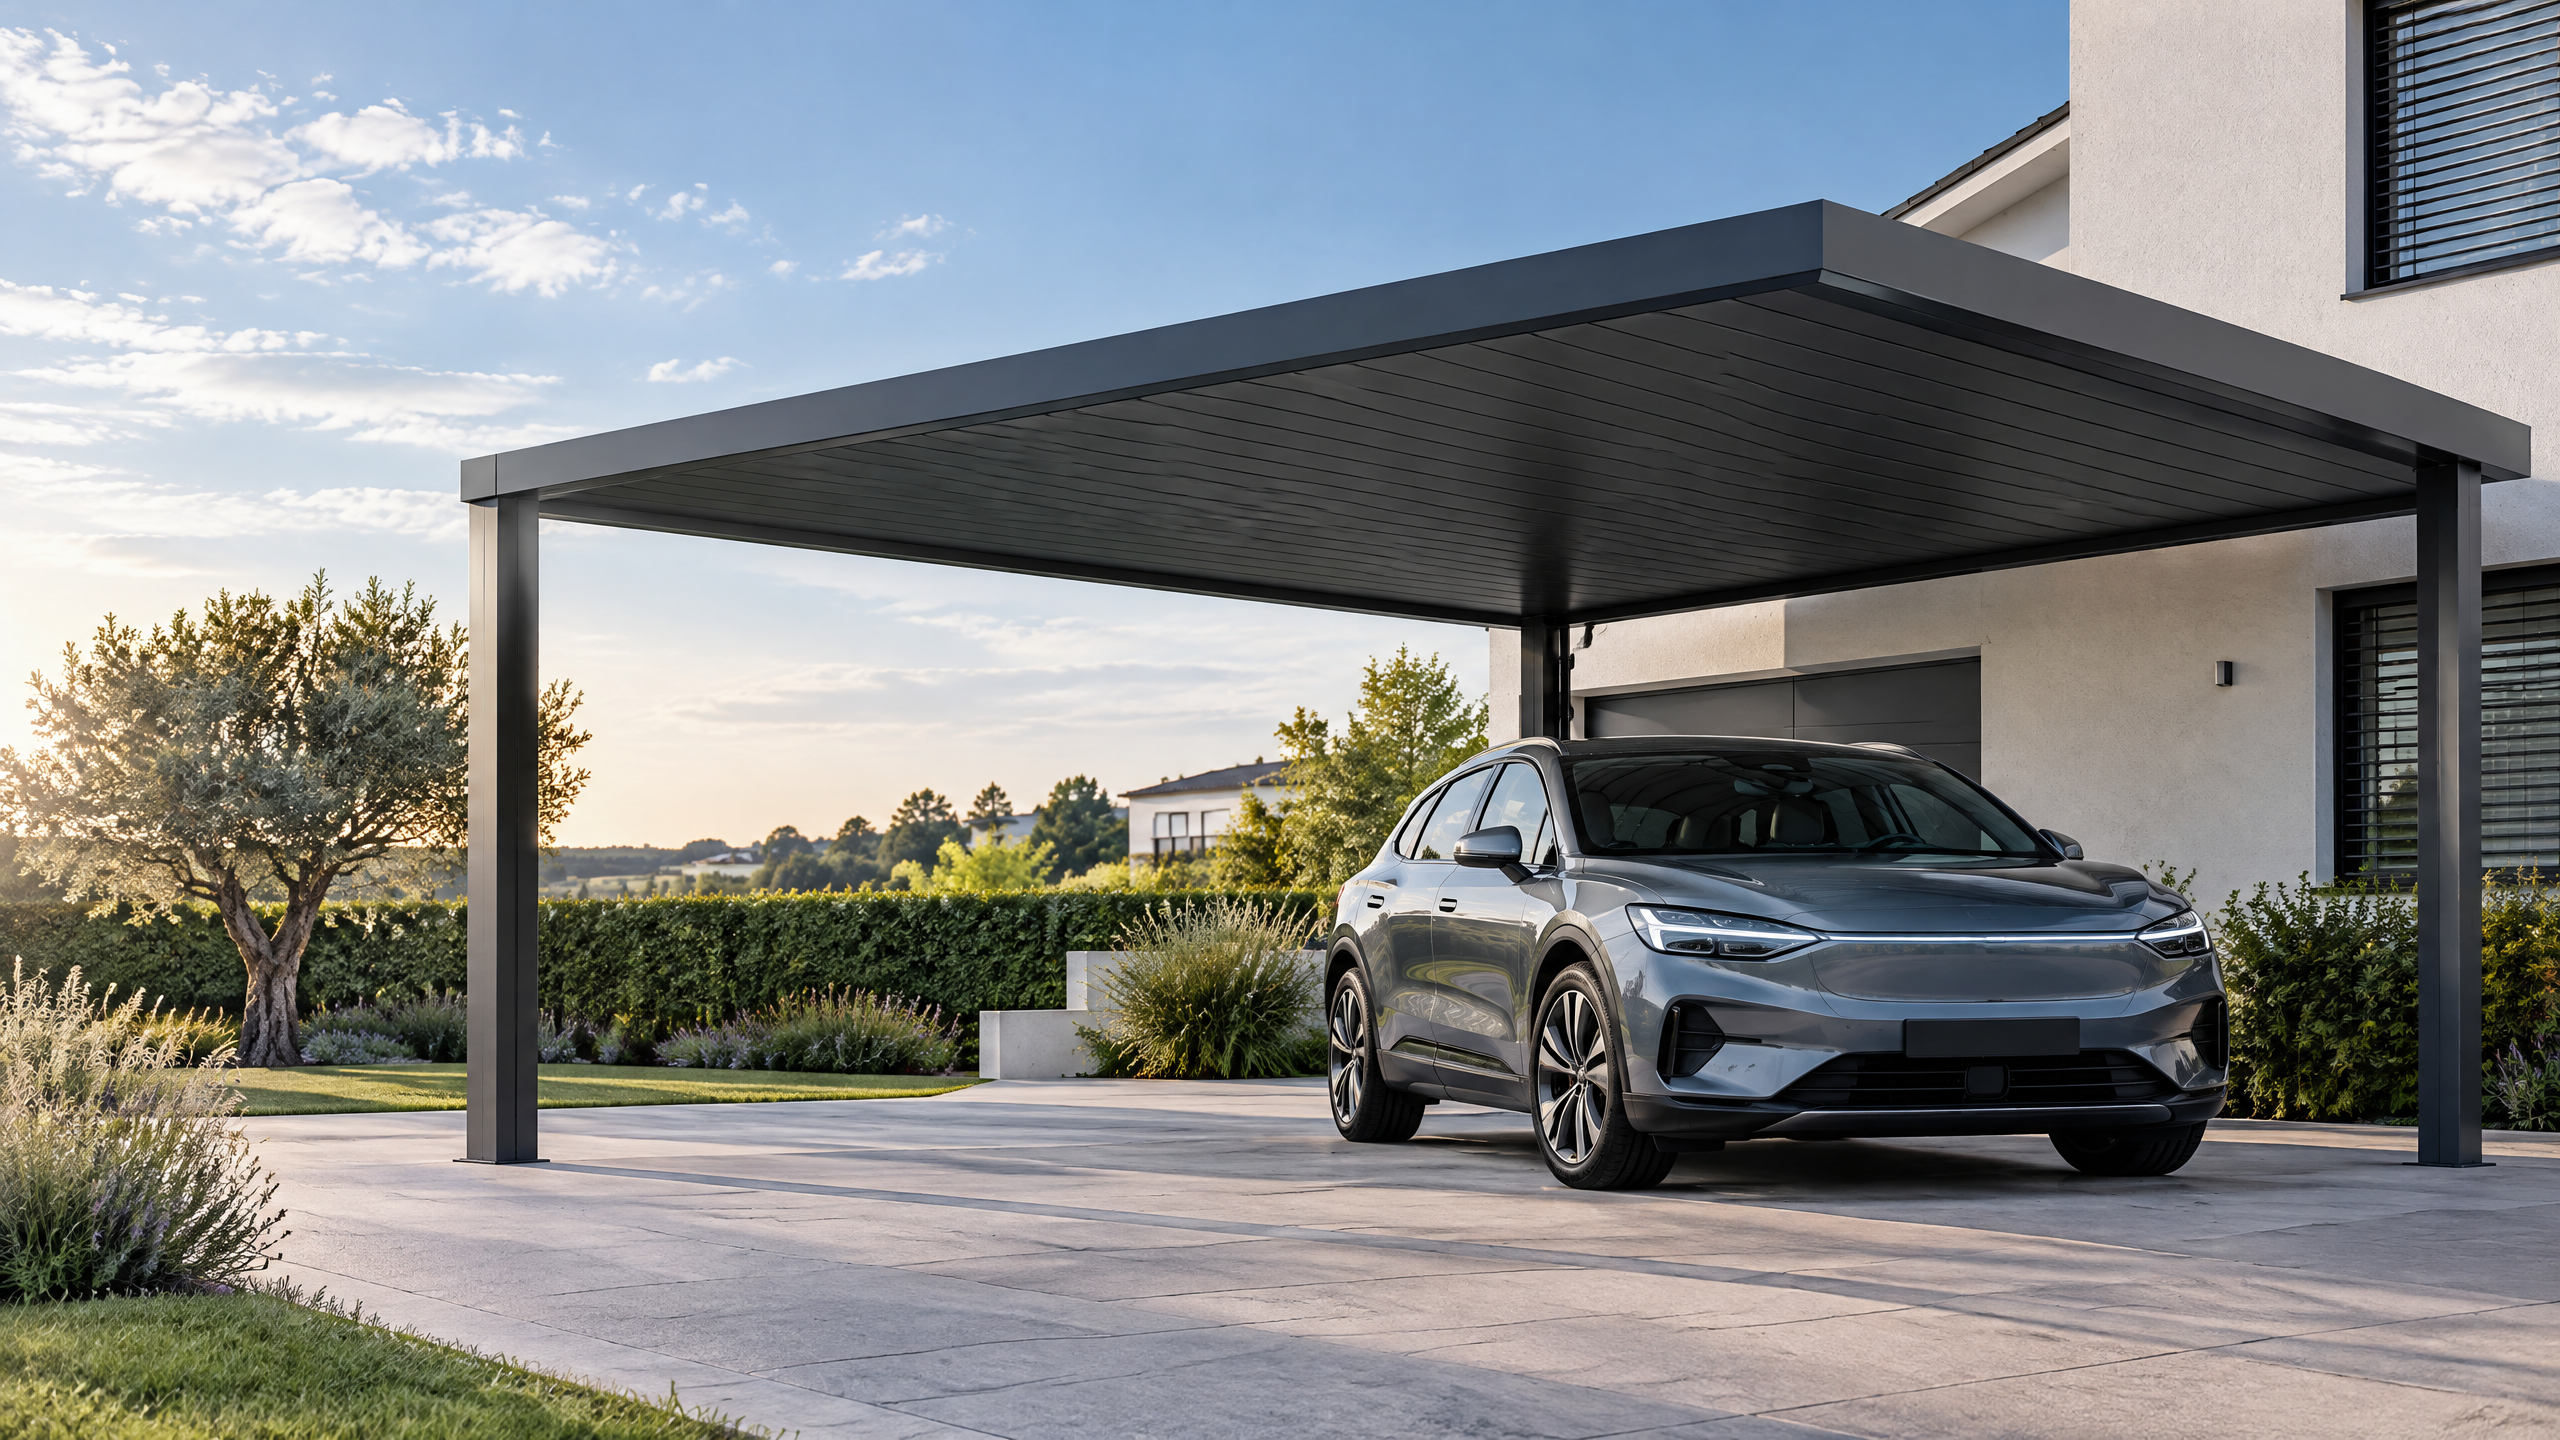
Answer — 120–180 words Specifying an aluminum carport system factory direct means procuring extruded aluminium structural assemblies and associated components directly from a manufacturer to control quality, lead time and configuration for a commercial project. Start by defining project scope (user type, loads, electrical/solar integration, site constraints) and required deliverables (shop drawings, factory test evidence, finish samples). Use structural design inputs referenced to local codes and international guidance (for example Eurocodes for wind and snow where relevant) [1]. Evaluate aluminium alloy and profile geometry against load cases and compatibility with coatings and fasteners (aluminium profile selection, finish and fastener compatibility). Require documented factory QA, material certificates and an explicit shop drawing review and installation readiness protocol before shipment. This approach reduces on-site modifications, improves schedule certainty and creates a clear handover path for installers, utilities and owners — provided the buyer validates foundations, permits, electrical design, energy yield, warranty terms and local approvals with qualified specialists.
Buyer context and scope boundary: who buys factory-direct and why
Commercial buyers for architectural aluminium systems — distributors, architects, contractors, developers, solar EPCs and fleet operators — choose factory-direct procurement when they need:
- Repeatable dimensional control for multi-bay modular carports.
- Integrated solutions (structural, canopy, roof drainage coordination, solar mounts) with single-source responsibility.
- Defined finish and fastener compatibility across large exposed surfaces.
- Certainty on lead times, production capacity and documented factory evidence for compliance and warranty negotiations.
Scope boundary: “factory direct” applies to the supply of aluminium extrusions, fabricated assemblies, engineered brackets, roof panels or PV mounts and factory-applied finishes. It does not, by itself, include site-specific items that require local specialists: structural capacity verification of the site, foundations, permits, electrical connection and solar grid interconnection, local approvals, lead time impacts, final price and warranty activation — all of which require a documented project basis and involvement of local qualified professionals, installers, utilities and authorities. State this boundary explicitly in procurement documents to avoid misaligned expectations.
Core decision principle: when factory-direct yields value
Decision principle: choose aluminum carport system factory direct when the incremental value of specification control, single-source responsibility and production repeatability exceeds the costs and logistics of direct procurement.
Key value drivers
- Complexity: integrated solar, custom curvatures or concealed fixings make factory control advantageous.
- Volume/repeatability: multiple identical bays lower unit costs and justify factory tooling and QA.
- Aesthetic control: tight finish tolerances and anodized or high-performance powder coat systems require factory application and verification.
- Risk allocation: assigning responsibility for dimensional coordination and interface points to the manufacturer reduces on-site change orders.
When project scale is small, or when local supply chains and fast-tracked delivery are paramount, hybrid procurement (local fabricator or distributor plus factory-supplied profiles) may be preferable. Use the commercial evaluation in the procurement section to quantify trade-offs.
Planning inputs — what you must supply before factory quotation
A factory needs a minimum documented project basis to produce an accurate factory-direct quotation and to commit to production. At minimum provide:
- Project brief and scope diagram
- Site plan, parking layout, elevation constraints, bay spans, number of bays.
- Design loads and code jurisdiction
- Applicable codes and basis of structural design (e.g., local code referencing Eurocodes where applicable) [1].
- Geotechnical/foundation data (or an instruction that the buyer will supply foundation design)
- Soil bearing capacity, groundwater, frost depth, pile design if any.
- Roof and drainage constraints
- Rainfall intensity, outlet locations, roof pitch and required roof drainage coordination.
- Adjacent interfaces
- Building interfaces, clearances, fire egress, lighting and CCTV mounting zones.
- Electrical and solar integration requirements
- Inverter locations, cable routing zones, DC string lengths, setback requirements from equipment and access for maintenance.
- Finish and specification expectations
- Colour, gloss, AAMA/ISO finish class if required, anti-graffiti or marine environment considerations [3][4].
- Programme constraints
- Critical dates, staged delivery requirements, storage capacity on site.
Providing these inputs reduces ambiguity, shortens lead time for final shop drawings and avoids costly change orders.
Technical specification and interfaces
This section outlines the technical content you should specify in procurement documents and what to confirm in factory documents.
Aluminium materials and alloys
- Specify alloy and temper for structural members (commonly 6061-T6 for structural sections and 6063-T6 for architectural extrusions, though requirements vary by project). Reference material traceability and mill test certificates from the mill via the manufacturer [2].
- Specify corrosion allowance for coastal or industrial atmospheres; indicate need for anodizing vs powder coat and any pre- or post-treatment.
Aluminium profile selection
- Provide span and loading envelopes, then match to profile modulus and section properties. Define interface points for bolted connections and ensure profiles accommodate fastener types.
- Consider extruded section wall thicknesses, webs, stiffeners, and tolerance banding. For critical load-bearing posts or rafter members, require section modulus data and calculation references.
Fasteners, seals and compatibility
- Define finish and fastener compatibility to avoid galvanic corrosion. Stainless steel passivated fasteners are often specified but require compatibility checks against aluminium alloy and surface finish (finish and fastener compatibility).
- Specify gasket materials for roof seals and their temperature/UV resistance.
Roofing, water management and roof drainage coordination
- Define roof panel type (metal, composite, PV+glass) and required attachment spacing. Clarify water shedding strategy: continuous gutters, internal drains or scuppers. Request the manufacturer provide a roof drainage coordination drawing showing slopes, outlet locations and overflow paths (roof drainage coordination).
- Make the buyer’s expectations explicit: no ponding, integrated overflow where applicable, access for maintenance.
Solar integration (if applicable)
- Define PV module frame types, clamp positions, electrical conduit paths and DC string limits. Identify inverter and combiner locations early to avoid rework.
- Require manufacturer to provide load paths for PV point loads and confirm capacity with structural calculations.
Thermal movement and expansion
- Specify expected ambient temperature range and design for expansion gaps, sliding connections or elongated bolt slots as appropriate.
Finish systems
- Specify finish performance class (e.g., AAMA 2604/2605 for powder coat longevity or equivalent), colour tolerance, gloss and sample signing procedure. Request test documentation where applicable (finish and fastener compatibility) [3].
Inspection and tolerances
- Define acceptable fabrication tolerances for extrusion length, end squareness, hole positions and flatness. Hold the manufacturer to a sign-off process during shop drawing review.
References and standards
- Reference applicable regional structural codes; for projects in Europe include Eurocodes for actions and verification [1]. For material and finish standards reference The Aluminum Association or AAMA where relevant [2][3]. For quality management and traceability reference ISO standards for document control and material traceability [4].
Procurement: what factory evidence to request and how to evaluate it
Factory-direct procurement shifts responsibility onto the manufacturer but demands documentary evidence. Request the following items explicitly in the contract and evaluate them before issuing purchase orders.
Essential factory evidence checklist (use as contract schedule)
- Manufacturer company profile and production capacity statement.
- Material certificates (mill test reports) for aluminium alloys.
- Welding procedure specification and welder qualifications (if welding is used).
- Surface treatment certificates and test reports for batch coatings (align to AAMA/ISO finish requirements) [3][4].
- Dimensional inspection reports or gauge control charts.
- Sample panels and finish mock-ups for colour and gloss approval.
- Assembly and shipping drawings, including lifting and protection details.
- Load calculations for main structural members, signed and stamped by a qualified engineer where local regulations require.
- Packing, handling and storage procedures.
- Non-conformance reporting, rectification and warranty procedures.
Decision table — Factory evidence prioritisation
| Evidence type | Purpose | Minimum acceptance |
|---|---|---|
| Mill test reports | Verify alloy and mechanical properties | Signed MTR referencing alloy designation |
| Finish certificate (AAMA/ISO) | Validate coating durability | Manufacturer’s certificate tied to batch or process |
| Dimensional inspection | Confirm tolerances | Inspection report with traceable measurement points |
| Load calculations | Ensure structural adequacy | Calculations from a qualified structural engineer |
| Sample mock-up | Visual/aesthetic approval | Approved physical sample before mass production |
When reviewing evidence, prioritize items that have direct impact on safety (load calculations and material certificates), durability (finish and fastener compatibility) and constructability (clear shop drawings).
Mid-article CTA If you want factory-direct procurement support, submit your project brief and planning inputs to our team for a preliminary feasibility conversation: /inquiry.
Shop drawing review and installation readiness
Shop drawing review is the single most important factory-stage control to ensure on-site success. A structured process reduces errors and aligns expectations.
Shop drawing review protocol
- Receive: Manufacturer submits full shop drawing set including part lists, connection details, foundation pack, roof drainage coordination drawings and PV interface drawings where needed.
- Technical check: Verify main member sizes, connection plates, bolt grades, drainage paths and any embedded items against the project scope.
- Coordination: Confirm alignment with MEP, civil and architectural teams. Use the drawings to coordinate electrical routes, inverter locations and lighting fixings before production.
- QA sign-off: Require signature from the buyer’s representative (engineer/architect) and the manufacturer indicating acceptance of drawings and acceptance of responsibility for discrepancies arising from shop drawings.
- Pre-production sample: For critical joints or finishes, require a first-off sample or witness inspection.
Installation readiness
- Pre-delivery checks: Ensure manufacturer provides lifting diagrams, as-built drawings, parts lists, and sequence-of-assembly instructions.
- Site acceptance: Confirm site access, crane capacity, storage protection, and installation crew competency are in place prior to delivery. Verify any pre-cast or pile foundations are completed to specification.
- Training and handover: Schedule on-site installation supervision or training if the system uses novel connections or concealed fasteners. Require a readiness certification from the installer prior to commissioning.
Include the exact phrase shop drawing review in the procurement schedule so it becomes a contractual milestone and trigger for payment and shipment.
Site installation and operations — practical coordination
Site installation for factory-supplied aluminium systems is a predictable activity only when upstream coordination is rigorous.
Foundations and interfaces
- Foundations must match anchor plate positions and tolerances from the approved shop drawings. Tight coupling between the structural drawings and the foundation contractor reduces rework.
- For modular multi-bay projects, require control points (survey markers) and a one-off leveling plan.
Handling, protection and lifting
- Aluminium extrusions, finished panels and anodized surfaces need protection from abrasion and contact with steel, concrete and corrosive substances. Specify packing that prevents moisture entrapment and contact damage.
Installation sequence and inspections
- Define erection sequence, torque values for bolted connections, and inspection hold points (e.g., after post erection, after beam installation, after roof installation).
- Use torque-controlled fastening and record completion certificates. For critical bolts and connections request checklists signed by installer.
Operations and maintenance
- Provide an operations manual including finish care, fastener checks, drainage maintenance and PV maintenance zones if applicable. Define inspection frequency and criteria for when remedial action is required.
State clearly in the tender that site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Decision table — On-site readiness checklist
| Readiness element | Responsible party | Evidence required |
|---|---|---|
| Foundations completed | Buyer/Primary contractor | As-built foundation drawing and survey |
| Crane and lifting plan | Contractor | Lift plan and crane certification |
| Installer competency | Installer / Contractor | CVs, trade certificates or factory training records |
| Site storage and protection | Contractor | Method statement and photos |
| Electrical connection approval | Utility / EPC | Permission to connect / grid acceptance |
Implementation risk, avoidance and contract language
Common implementation risks and mitigations
- Design mismatch: Risk — shop drawings do not align with architectural or MEP interfaces. Mitigation — enforce a shop drawing review sign-off process and cross-discipline coordination workshops before production.
- Foundation mismatch: Risk — anchor locations or embed depths differ from as-built foundations. Mitigation — require as-built foundation survey prior to arrival and include adjustable base plates or packing allowances in design.
- Finish failure or incompatibility: Risk — coatings or fasteners lead to premature degradation. Mitigation — specify compatible fastener materials, require finish certificates and pre-production samples; reference AAMA/ISO finish standards [3][4].
- Lead time and logistics delays: Risk — production or shipping delays affect the programme. Mitigation — include milestone-based release of production, contingency windows and clearly defined penalties or incentives in contract.
- Warranty and spare parts ambiguity: Risk — warranty terms do not cover certain defects. Mitigation — agree written warranty scope tied to factory evidence and specify spare parts kit and lead times.
- Solar electrical interface risk: Risk — PV layout causes structural overstress or electrical safety hazards. Mitigation — require combined structural and electrical review, confirm cable routing and string lengths pre-production.
Contract language recommendations
- Define scope split in the contract: what the factory supplies vs what the site contractor supplies.
- Require evidence and milestones (shop drawing approval, pre-production sign-off, final inspection) as payment triggers.
- Include a clause stating that the manufacturer’s responsibility extends to conformance with approved shop drawings and factory-applied finishes but not to site-installed foundations, utilities, or permits unless specifically contracted.
- Specify dispute resolution and hold points for non-conforming product deliveries.
Cite the relevant standards and local code references rather than prescriptive technical values. For structural load basis in Europe, reference Eurocodes for actions and verification [1]. For aluminum material traceability and guidance use The Aluminum Association [2]. For finish performance reference AAMA finish standards [3] and relevant ISO standards for QA processes [4].
Six-step buyer workflow (named)
"Carportiva Factory-Direct Decision Path" — six explicit steps for buyers
- Define Project Basis and Objectives
- Produce a document with site plan, number of bays, intended use, solar requirements, finish expectations and target programme. Identify the authority having jurisdiction for structural and electrical permits.
- Site Survey and Geotechnical Input
- Commission surveys and geotechnical report to define foundation strategy and site constraints. Provide these to manufacturers for foundation interface design.
- System Selection and Preliminary Quotation
- Use selection criteria (aesthetic, loads, solar integration, budget) to choose candidate systems. Request preliminary quotations and evidence of manufacturing capacity and references.
- Procurement and Factory Evidence Collection
- Issue RFQ specifying required factory evidence: MTRs, finish certificates, load calculations, production capacity and sample approvals. Use the procurement checklist in this guide.
- Shop Drawing Review and Approvals
- Execute formal shop drawing review workshops. Approve drawings with a signed checklist covering dimensional tolerances, drainage coordination, PV interfaces and lift points. This is the contractual production authorization.
- Installation Readiness, Delivery and Handover
- Confirm site readiness (foundations, access, storage). Accept delivery with an agreed inspection protocol. Conduct final commissioning, document handover and register warranty per contract terms.
Each step should produce a signed or recorded deliverable before moving to the next step. This reduces scope creep and protects programme certainty.
Related B2B sourcing terms
For the same project brief, buyers may also encounter these connected search terms: architectural carport specification. They must be interpreted against the actual project scope rather than treated as independent technical guarantees.
FAQ
Q: What is the difference between factory-direct and local fabrication? A: Factory-direct means primary fabrication, finishing and assembly are completed at the manufacturer’s facility and shipped to site as assemblies. Local fabrication can refer to finishing, minor fabrication or assembly done near site by local partners. Factory-direct controls tolerances and coating quality tightly; local fabrication may allow faster lead times and easier on-site adjustments.
Q: What aluminium alloys are typical for carport structures? A: Commonly used alloys in architectural applications include 6061 and 6063; 6061 provides higher strength for structural members, while 6063 is widely used for architectural extrusions. Specify mill test certificates to confirm alloy and temper [2].
Q: How should finish performance be specified? A: Specify finish class (e.g., AAMA 2604/2605 equivalent for powder coat) and require batch certificates and mock-ups. Include environmental exposure considerations (marine, industrial) in the procurement documents [3].
Q: Does the factory warranty cover on-site installation issues? A: Warranties vary. Factory warranty typically covers manufacturing defects and finishes if maintained per manufacturer instructions. Site issues—incorrect foundations, installation errors, or utility work—are normally excluded unless the factory explicitly contracted to perform those works. Always require clear written warranty scope.
Q: How is roof drainage coordinated across multiple bays? A: Define drainage strategy in the initial brief and require roof drainage coordination drawings in the shop drawing set. Clarify gutters, scuppers, outlets and overflow paths and identify maintenance access routes.
Q: Do I need a local structural engineer if I buy factory-direct? A: Yes. Site-specific structural capacity, foundations, permits and approvals must be validated by local qualified professionals. The factory supplies member capacities and shop drawings; the local engineer confirms foundation design and site compliance.
Q: What documentation should be provided at handover? A: As-built drawings, operation and maintenance manuals, material certificates, finish certificates, fastener schedules, and warranty paperwork. Also provide a spare parts list and suggested inspection intervals.
Short procurement templates and contract clauses
Suggested clause snippets (conceptual)
- “Manufacturer shall provide mill test reports for all aluminium supplied and a certificate of conformity to the specified alloy and temper.”
- “Shop drawings constitute the manufacturer’s construction documents. No production shall commence until the buyer’s authorized representative issues a signed shop drawing review acceptance.”
- “Factory shall provide protective packing sufficient to prevent abrasion and moisture entrapment during standard shipping and site storage.”
- “Warranty shall be issued in writing and specify coverage start date tied to the date of final acceptance on site.”
Use these as starting points, and have your legal or commercial teams adapt them to local procurement law.
Further resources and product links
For modular architectural aluminium systems, see our product family and technical data: NordArch architectural aluminium system. Explore all systems for comparative configurations and visit our sourcing guides for templates and checklists.
Conclusion
Specifying an aluminum carport system factory direct offers strong benefits in quality control, finish durability and pre-coordination of interfaces — particularly for commercial projects with integrated solar, large repeatable bays or high aesthetic requirements. Success depends on disciplined planning inputs, a documented procurement evidence process, rigorous shop drawing review and clear contract milestones tied to installation readiness. Remember: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and validation by relevant local qualified professionals, installers, utilities and authorities. If your project requires a factory-direct solution with clear deliverables and a coordinated handover, contact us to start the procurement conversation: info@carportiva.com.
Appendix — quick reference decision table
| Question | Factory-direct recommended? | Rationale |
|---|---|---|
| Multi-bay, repeat modular carport | Yes | Improved dimensional control, economy of scale |
| Single bespoke canopy with short programme | Possibly not | Local fabrication may be faster and more flexible |
| Integrated PV with specific electrical design | Yes | Simplifies PV interface and structural verification |
| Coastal/marine exposure | Yes (with explicit finish spec) | Factory-applied anodizing or high-spec powder coat can be controlled and verified |
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion