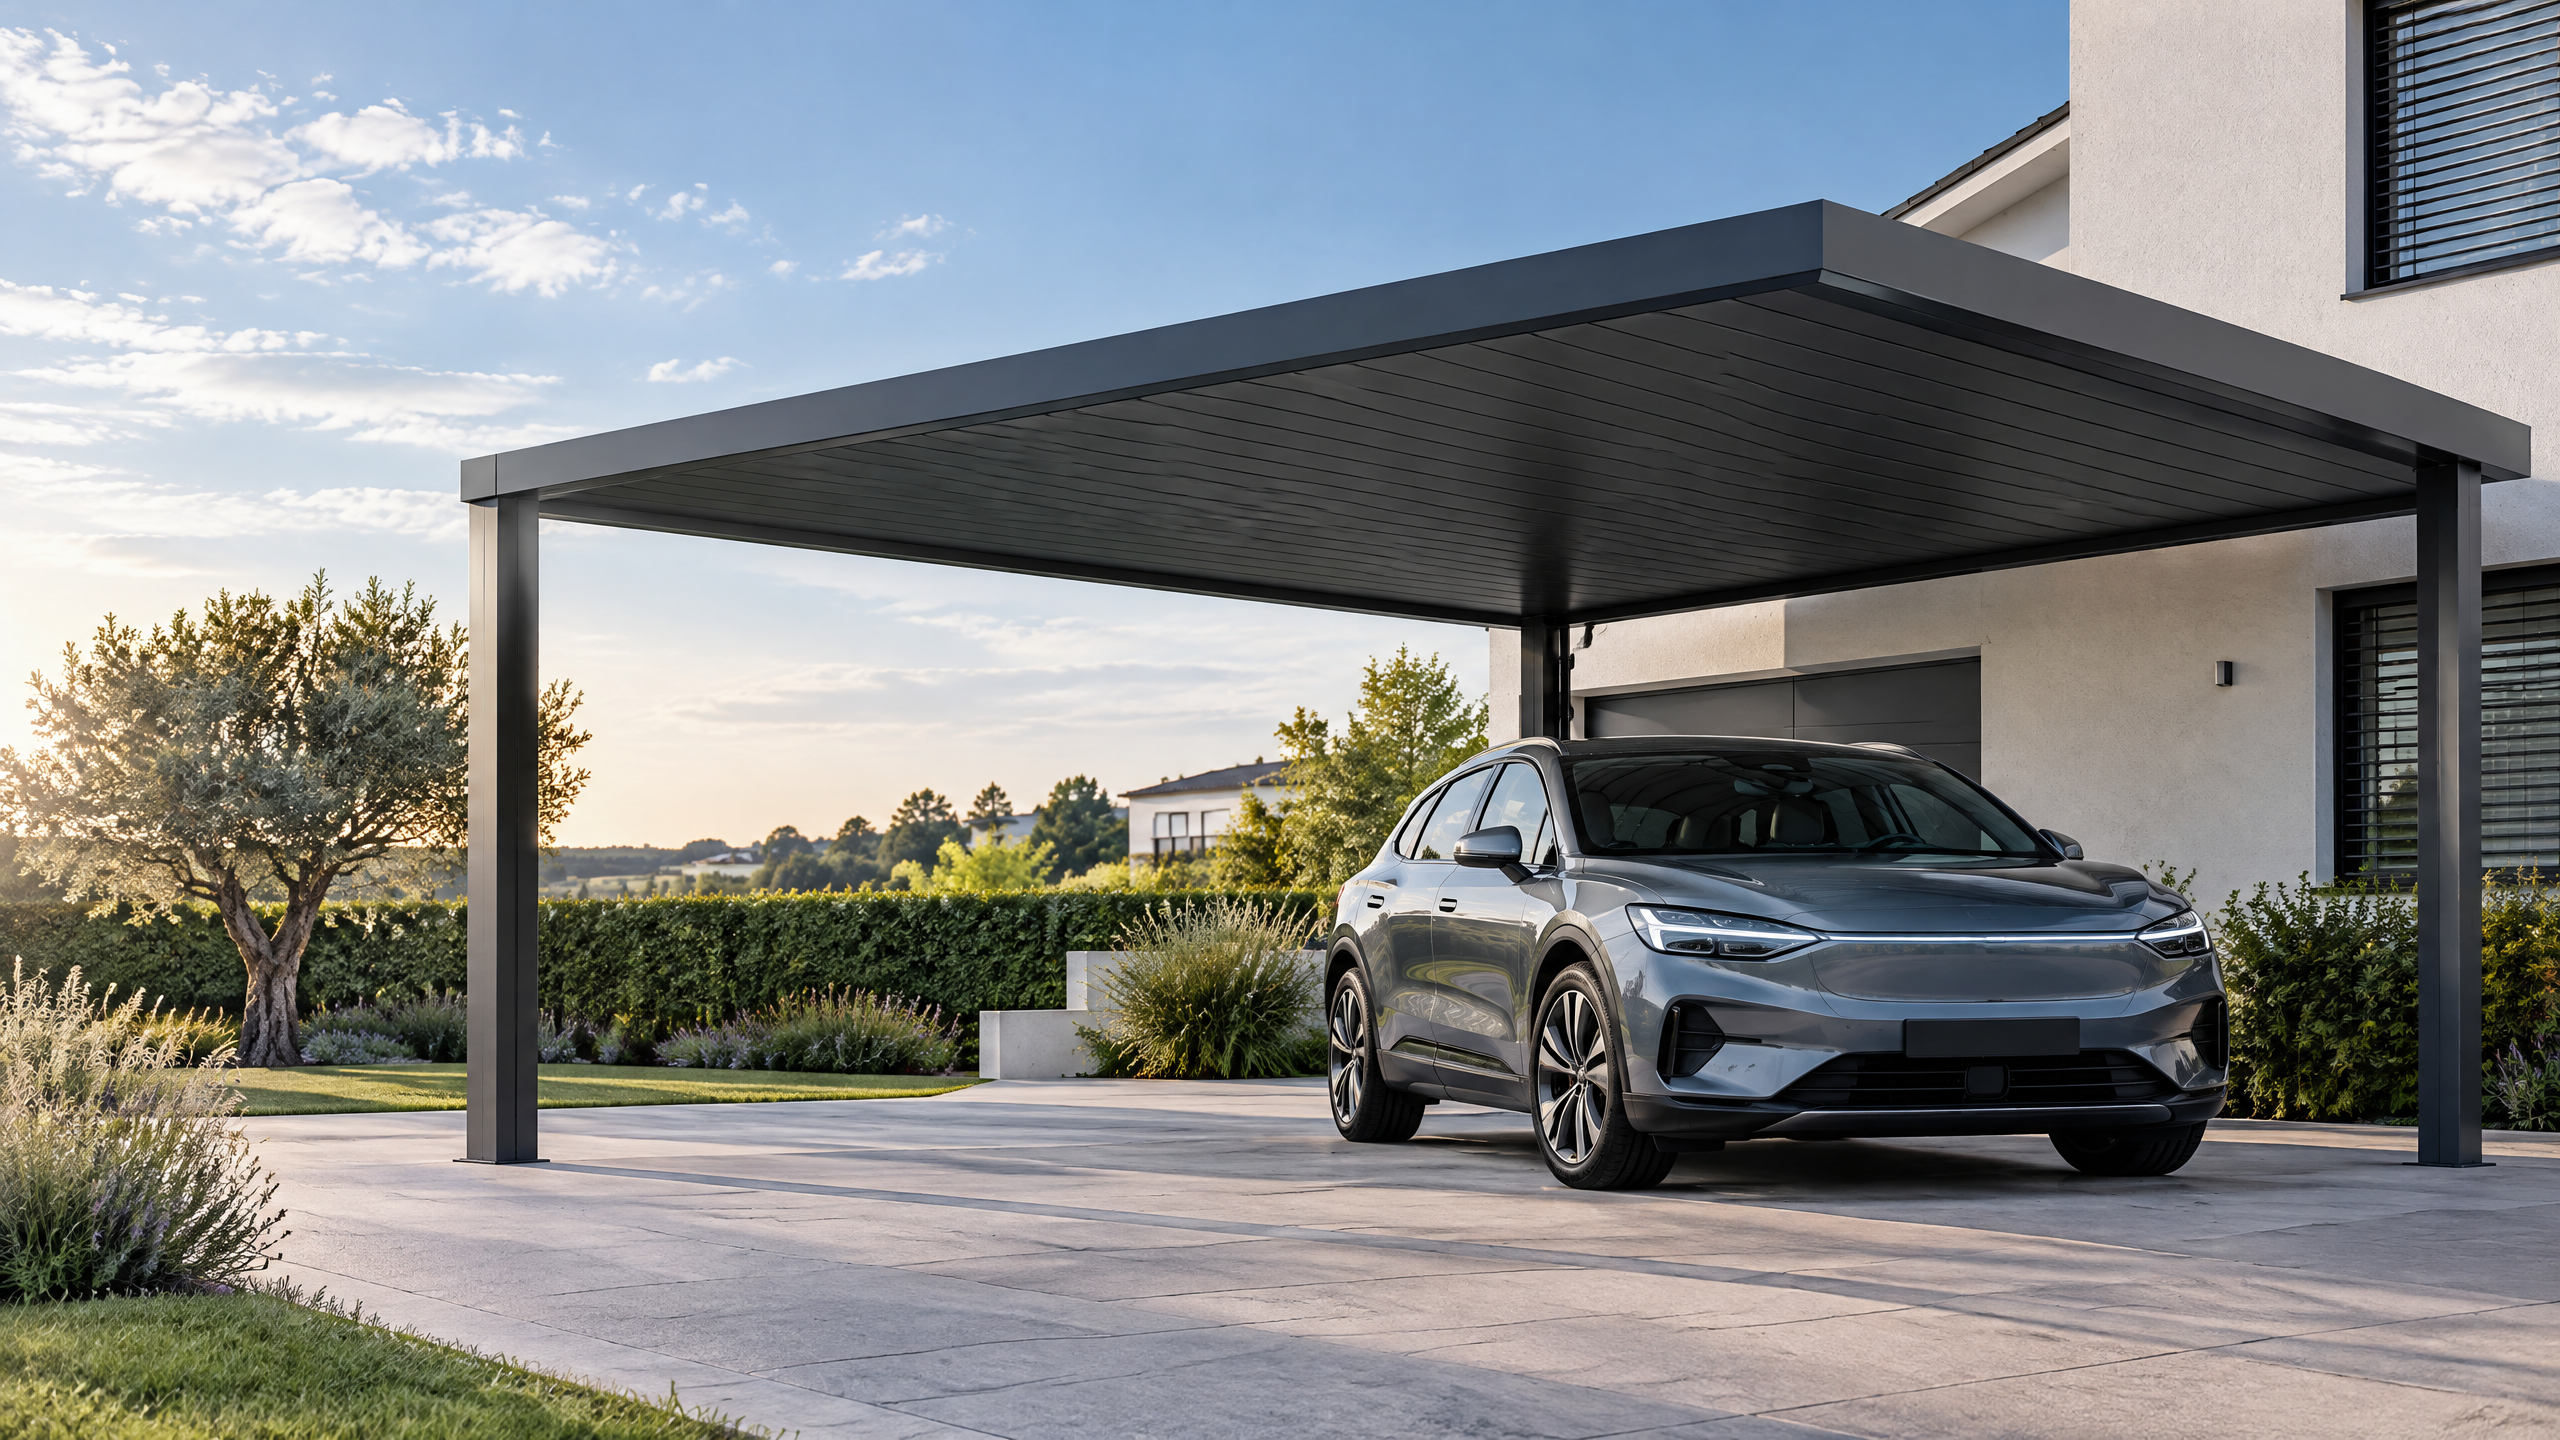
Answer (direct, 120–180 words) A project team commissioning a double bay aluminium carport manufacturer must confirm that the supplier can deliver a documented, engineered solution that matches the project’s scope, local loads and integration needs. At minimum verify: demonstrable capability in architectural aluminium systems; engineering documents and shop drawing review; tested material specifications and alloy traceability; aluminium profile selection and extrusion tolerances; finish and fastener compatibility for the environment; roof drainage coordination with downstream civil and MEP systems; manufacturing quality-control and factory acceptance evidence; and clear installation readiness including certified installers, foundation details and sequencing. Procurement should require verifiable samples, a staged approval process (prototype or pilot, shop drawings, pre‑shipment inspection) and contractual acceptance criteria for lead time, price milestones, warranty coverage and post‑installation maintenance. Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and verification by relevant local qualified professionals, installers, utilities and authorities.
Buyer context and scope boundary: defining the "double bay" requirement
Why focus on a double bay aluminium carport manufacturer?
- “Double bay” indicates two adjacent vehicle bays under a single continuous structure. Project teams must separate decisions around the manufacturer (provider of engineered aluminium components and assemblies) from site-specific design responsibilities (foundations, electrical interconnects, local permitting).
- Use scope boundary statements in procurement documents to allocate responsibilities: manufacturer (supply and factory assembly), specialist installer (on-site erection), civil contractor (foundations and site grading), electrical contractor (if PV or lighting), and authority stakeholders (permits and local approvals).
Scope checklist to include in tender documents:
- Precise bay dimensions (clear width, bay spacing, typical vehicle clearances)
- Intended functions: sheltered parking only, integrated photovoltaics, EV charging, or mixed-use
- Environmental exposure class (marine/industrial/urban) and local load cases (wind, snow, seismic)
- Finish expectations and maintenance access
- Connection and handover interfaces (drainage, electrical, civil)
Clarify commercial roles early to avoid later disputes: who supplies anchor bolts, who coordinates with utilities, and who signs off on installation readiness.
Core decision principle: evidence over claims
Primary selection criterion: verifiable engineering and manufacturing evidence
- Prioritize suppliers that produce project-specific engineering packages rather than generic brochures.
- Require a documented shop drawing review process and factory quality records as pre-conditions to contract award.
What “evidence” means in practice:
- Calculations tied to local code load cases (or Eurocodes where applicable) and signed by a qualified engineer.
- Material certificates and traceability for aluminium alloys and fastener materials.
- Non-proprietary test reports or third‑party inspection records for welds, connection performance and roof cladding attachment where relevant (do not accept unverified claims).
Standards and references
- Structural design references should be identified (e.g., Eurocodes where applicable) and the basis of calculation included in delivery documentation [1]. For finish systems and alloy guidelines, consult regional standards such as those from The Aluminum Association and AAMA [2][3]. Use ISO where clarified product or process standards are specified [4].
Decision rule example (simple):
- If the manufacturer cannot provide project-specific engineering, shop drawings, and traceable material certificates, exclude them from shortlist.
Planning inputs: data the manufacturer needs and the team must supply
Manufacturer inputs they should expect from the buyer:
- Site coordinates and relevant geotechnical/geographic data (ground conditions, frost depth)
- Project wind/snow/seismic design actions or local code designation
- Exact bay layout, vehicle turning and clearance diagrams, and any parapet or pedestrian interface requirements
- Intended finish class and environmental exposure rating
- Any electrical or PV scope: inverter location, DC/AC routing, cable trays, earthing strategy
Buyer responsibilities to prepare:
- A documented project brief that frames the scope (reference to architectural carport specification or client performance brief)
- Baseline programme with procurement milestones and allowed tolerances for lead time
- Permitting and approvals schedule; identify local authority variance or special access constraints
- Allocation of site work and foundation responsibility
Why these inputs matter
- Aluminium profile selection, anchor design, and roof drainage coordination depend on geotechnical and rainfall/runoff data; without this, the manufacturer cannot engineer reliable attachments or drainage interfaces.
Technical specification and interfaces: what to confirm in detail
This section lists the technical elements a project team must review and confirm with a double bay aluminium carport manufacturer.
- Structural design and load cases
- Confirm design load basis (wind, snow, seismic) and the design code used. If Eurocodes are the reference, ensure the manufacturer’s calculations explicitly state the parts used and partial safety factors [1].
- For seismic regions, confirm dynamic response assumptions and anchorage detailing.
- Aluminium alloys and procurement
- Request alloy specifications (e.g., 6000-series extrusions) with temper designations and certificate of conformity for each lot. The Aluminum Association provides industry guidance on alloy selection and handling [2].
- Ask for aluminium profile selection rationale—extrusion wall thicknesses, section modulus, and tolerance bands—and how they were checked against deflection/serviceability limits.
- Connections, fasteners and corrosion control
- Confirm finish and fastener compatibility: galvanic compatibility between aluminium and fasteners, use of isolation barriers, and coating specifications (powder coat or anodize) must be documented. For coating performance and testing protocols, reference AAMA and ISO guidance where applicable [3][4].
- Fasteners should be specified with material grades (e.g., stainless steel grade) and any sacrificial or isolation detailing noted.
- Roof cladding, sealing and drainage
- Confirm roof deck design, cladding attachment method, ponding allowance, and roof drainage coordination with site stormwater management. Include secondary drainage paths and overflow provisions.
- For photovoltaic installations, review combined loads and thermal expansion allowances.
- Thermal movement and tolerances
- Include expansion joint strategy when bays are long or when thermal gradients differ between supported materials.
- Confirm manufacturing and field tolerances, as aluminium extrusions and assembled frames require strict tolerances for glazing panels, cladding and PV mounting.
- Shop drawing deliverables
- Specify content and approval process. Expect full dimensional shop drawings, connection details, anchor bolt charts, BOM and assembly sequence.
- The buyer should mandate a shop drawing review milestone before manufacture begins (shop drawing review).
- Integration with other trades
- Define interface points for foundations, drainage, electrical conduits, and any lighting or security systems.
- Coordinate rooftop access for maintenance and PV servicing if included.
Procurement and factory evidence: what documentation to demand
Procurement documents should establish acceptance criteria, quality gates, and documentary deliverables. Below is a recommended procurement evidence checklist.
Decision table 1 — Procurement evidence checklist
| Evidence / Deliverable | Purpose | Accept or Reject threshold |
|---|---|---|
| Project-specific structural calculations signed by a qualified engineer | Verify capacity for local loads | Accept if signed and references design codes; reject if generic |
| Material mill/test certificates for aluminium extrusions and fasteners | Traceability and corrosion performance | Accept if batch traceable and matches specified alloy; reject if absent |
| Shop drawings with anchor bolt plan and tolerance chart | Install coordination and foundation interface | Accept if stamped and dimensioned; reject if incomplete |
| Coating and finish test data / manufacturer’s guarantees | Visual durability and environmental suitability | Accept with specified standard adherence (AAMA/ISO); reject if no test basis |
| Factory quality control plan and production inspection records | Assurance of consistent fabrication | Accept if QC plan submitted and available for audit; reject if none |
| Pre-shipment inspection report or witness testing availability | Final verification before delivery | Accept if available or permitted; reject if supplier refuses inspection |
| Packaging and handling method statements | Protect goods in transit and on-site | Accept if protective measures match component sensitivity; reject if inadequate |
| Installation readiness package (tools, templates, installer training) | Reduce site delays | Accept if defined; reject if no plan for installation readiness |
Contract terms to include in purchase order
- Clear acceptance milestones linked to deliverables above.
- Call-outs for non-conformance remediation and retention amounts if deliverables or shop drawing review are not completed.
- Warranty start date linked to practical completion, with definition of scope and exclusions.
Factory audit and QA
- If the project size or risk justifies it, plan for an in-factory audit or third‑party inspection to verify manufacturing tolerances, coating application and assembly jigs.
- Confirm manufacturer’s capacity for serial consistency, particularly for multi‑unit projects.
References to standards and testing
- For finish systems, require test standards or equivalence per AAMA and ISO expectations rather than proprietary claims [3][4].
- For structural calculations, require reference to the applicable national code or Eurocodes [1].
Site installation, sequencing and operations
Installation readiness is a critical acceptance criterion; confirm this with the manufacturer and the installer.
Installation readiness checklist (must-have items)
- Anchor bolt templates and precise coordinate lists for foundations (provided prior to concrete pour).
- Pre-fitted components and jigs to minimize on-site adjustments.
- On-site training or supervision by manufacturer representatives during critical lifts and connections.
- Detailed lift plan and crane access information when modules or long extrusions require mechanical handling.
- Packaging and temporary protection for finishes during installation.
Decision table 2 — Installation mode comparison
| Installation mode | Typical application | Pros | Cons |
|---|---|---|---|
| Fully factory-assembled modules | Large commercial sites with controlled lifts | Reduced field labor, consistent quality | Requires heavy lifting equipment and precise foundations |
| Semi-assembled frames with field bolting | Common for mid-size projects | Balance of transportability and field flexibility | More field time and potential for alignment issues |
| Kit-of-parts with on-site assembly | Remote or constrained sites | Lower transport cost, adaptable | Requires skilled site installers and more QA oversight |
Site commissioning and handover
- Coordinate final checks: fastener torque, sealant continuity, roof drainage performance under test flows, and PV electrical commissioning if applicable.
- Provide as‑built drawings, maintenance manuals, finish touch-up kits and spares list.
- Define responsibility for post-installation cleaning, touch-up, and warranty activation.
Operational considerations
- Establish maintenance intervals for finishes and drainage clearing.
- For solar carports, coordinate energy yield expectations with the electrical contractor; energy yield and related financial forecasts require a documented project basis and qualified electrical engineers and EPCs.
Important statement (compliance reminder) Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and verification by relevant local qualified professionals, installers, utilities and authorities.
Implementation risks and mitigation
Identify likely areas of dispute and how to control risk.
Risk: Incomplete shop drawing review leading to rework
- Mitigation: Make shop drawing review a contractual milestone with formal acceptance sign-off.
Risk: Finish and fastener incompatibility causing corrosion or staining
- Mitigation: Require finish and fastener compatibility verification, including specification of sacrificial anodes/isolation layers and material pairing plans.
Risk: Misaligned foundations due to inaccurate templates
- Mitigation: Provide survey-accurate anchor templates and require manufacturer-issued tolerance charts before concrete placement.
Risk: Roof drainage failure or ponding
- Mitigation: Include roof drainage coordination and overflow detailing in early design workshops; require a drainage test before handover.
Risk: Supplier lead-time variance impacting programme
- Mitigation: Lock in lead time with shipment milestones and include liquidated delay allowances or staged release schedules; require manufacturer's production schedule and advance notification of delays.
Risk: Warranty and post-installation support scope mismatch
- Mitigation: Define warranty triggers (practical completion acceptance, defects list process) and request clear exclusions for misuse or unauthorized alterations.
Risk: Inadequate installer competency
- Mitigation: Require certification of installer competence, or include manufacturer supervision period in scope. Define acceptance tests to prove installation readiness.
Risk: Integration with PV/Electrical systems
- Mitigation: Conduct cross-discipline coordination workshops early; require interface drawings showing conduit routes, inverter locations and earthing bonds.
Six-step buyer workflow (named and sequence-driven)
Follow this structured workflow to reduce procurement and delivery risk:
- Define and freeze the project brief (ScopeLock)
- Produce a single architectural carport specification for all bidders, including bay dimensions, environmental exposure class and integration demands.
- Pre-qualification and shortlist (QualifySelect)
- Evaluate manufacturers on evidence: past project types (not claims), manufacturing capacity, engineering capability and QA systems.
- Detailed enquiry and shop drawing review clause (DetailBid)
- Issue a Request for Proposal with explicit requirements for shop drawings, material certificates, finish and fastener compatibility statements and factory QA records.
- Prototype / sample approval and factory audit (SampleVerify)
- Approve finish samples, connection mock-ups and request a factory audit or witness testing for critical processes.
- Manufacture with staged inspections (ProdControl)
- Maintain production control points: material receipt check, mid‑fabrication inspection, pre-shipment inspection and packing verification.
- Installation, commissioning and formal handover (InstallComplete)
- Require manufacturer-provided installation readiness support and a formal handover with as-built documentation and maintenance manuals.
This six-step workflow aligns procurement with assurance actions and reduces the chance of late design changes, rework and disputes.
Practical procurement clauses and contract language examples
Suggested procurement clauses (short phrasing)
- “Supplier shall provide project-specific structural calculations signed by a licensed engineer for the project jurisdiction and referencing the applicable local design codes.”
- “Supplier to submit shop drawings for approval within X weeks of PO; manufacture will not commence until written approval is issued.”
- “All aluminium extrusions shall be accompanied by mill certificates indicating alloy, temper and heat number traceability.”
- “Finish systems shall comply with AAMA/ISO standard test performance for the specified exposure class; fastener materials and isolation measures shall be specified.”
- “Anchor bolt templates shall be issued with tolerances and coordinate lists before foundation works; buyer will verify prior to pour.”
- “Pre-shipment inspection by buyer or nominated third party shall be permitted and scheduling agreed in advance.”
Contractual acceptance criteria to include
- Acceptance is conditional upon receipt of approved shop drawings, factory inspection report and delivery of required maintenance and handover documents.
- Warranty start date and conditions (e.g., defects liability period begins at practical completion and acceptance testing).
FAQ (practical answers B2B buyers need)
Q: How do I verify a manufacturer’s structural calculations? A: Require signed calculations referencing the applicable design code (e.g., Eurocodes where used) and the engineer’s registration. Do not accept un‑referenced spreadsheets. For critical projects, commission an independent review.
Q: When should I involve geotechnical and civil contractors? A: Before issuing anchor templates. Foundations affect the entire manufacturing acceptance; geotechnical input must precede anchor bolt placement.
Q: What questions should I ask about corrosion protection? A: Ask for explicit finish and fastener compatibility statements, including whether anodize or powder coat is specified, the coating thickness, expected maintenance intervals and any isolation measures between dissimilar metals [3][4].
Q: Is it acceptable to start manufacturing before shop drawing approval? A: Only if contractually agreed and with formal waivers for off-setting risk. Best practice: approve shop drawings first. This reduces costly rework.
Q: What evidence should be supplied for PV-integrated carports? A: Electrical single-line diagrams, structural calculations incorporating PV loads, PV mounting details, earthing/ bonding plans, and coordination with the electrical contractor for DC/AC routing and inverter locations.
Q: What role does the buyer play in installation readiness? A: The buyer must confirm site access, foundations to tolerance, crane availability if required, and ensure that a qualified installer is engaged. The manufacturer should provide installation templates and supervision as required.
Q: Can I rely on supplier-supplied installers? A: Yes, but require verification of competency (e.g., installer CVs, past project references) and include manufacturer supervision days in the contract where installation complexity is high.
Q: How should lead time risk be managed? A: Break delivery into milestones, require production schedules, and include reasonable contractual remedies or re-sequencing provisions. Validate supplier capacity during pre-qualification.
Mid-article CTA
If you need help turning these requirements into a tailored procurement package, request a conversation and project checklist: /inquiry. For product-level options, see the NordArch architectural aluminium system, our overview of all systems and related sourcing guides.
Due diligence and third-party verification
When to engage third parties
- Large or high-risk programmes: engage independent engineers for structural verification.
- Where local competency is limited: commission third-party factory inspection agencies.
- When finishes have long-term exposure: ask for independent laboratory test reports or accreditation statements.
What to expect from a factory inspection
- Verification of extrusion tolerances, weld practices, coating application and assembly procedures.
- Cross-check of BOM against packing list and random component dimensions.
- Photographic or signed reports that can be attached to the contract acceptance record.
Using standards as procurement anchors
- Reference Eurocodes or local equivalents as the calculation framework for structural design to provide a common basis [1].
- Use AAMA expectations for coating systems and seek ISO references for process control and material identification where applicable [3][4].
Operational readiness and lifecycle considerations
Maintenance planning
- Establish routine inspection intervals for seals, fasteners and drainage clearance.
- Factor in access for cleaning and for PV maintenance if present.
Lifecycle cost considerations
- Compare initial capital cost against total cost of ownership: expected finish refresh cycles, fastener replacement and potential corrosion mitigation.
- Confirm availability of spare parts and long-term production plans with the manufacturer for multi-phase deployments.
Spares and spare-part planning
- Request a spare parts list with lead times and part numbers. For extruded sections, include length tolerances and finish re‑order codes.
Warranty expectations
- Clarify warranty coverage for structural components, finishes and workmanship. Define what triggers warranty remediation and the process and lead times for claims.
- Warranty specifics (duration, exclusions) must be set by documented project basis and verified with local legal and technical advisors.
Conclusion and final checklist
Final procurement checklist (condensed)
- Project brief and scope freeze (ScopeLock)
- Manufacturer pre-qualification (QualifySelect)
- Mandatory shop drawing review milestone (DetailBid)
- Material certificates and finish/fastener compatibility confirmation
- Factory audit or pre-shipment inspection agreement
- Anchor templates issued before foundations pour
- Installer competency verification and installation readiness plan
- Defined acceptance criteria, warranty terms and maintenance obligations
Remember: selecting a double bay aluminium carport manufacturer is a systems-level procurement decision within the architectural aluminium systems cluster. Insist on documented engineering, traceable material evidence, clear shop drawing review, finish and fastener compatibility, coordinated roof drainage and concrete foundations, and a defined installation readiness plan. For product details and system options, see NordArch architectural aluminium system and review our all systems and sourcing guides for template clauses and checklists.
Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and verification by relevant local qualified professionals, installers, utilities and authorities.
For project consultancy, proposals or to request our procurement checklist, contact us: /inquiry or email info@carportiva.com.
References
- Eurocodes and design rules for structural design [1]
- Guidance on aluminium materials and industry practices [2]
- Architectural finish/coating standards and expectations [3]
- ISO product and process standards for materials and testing [4]
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion