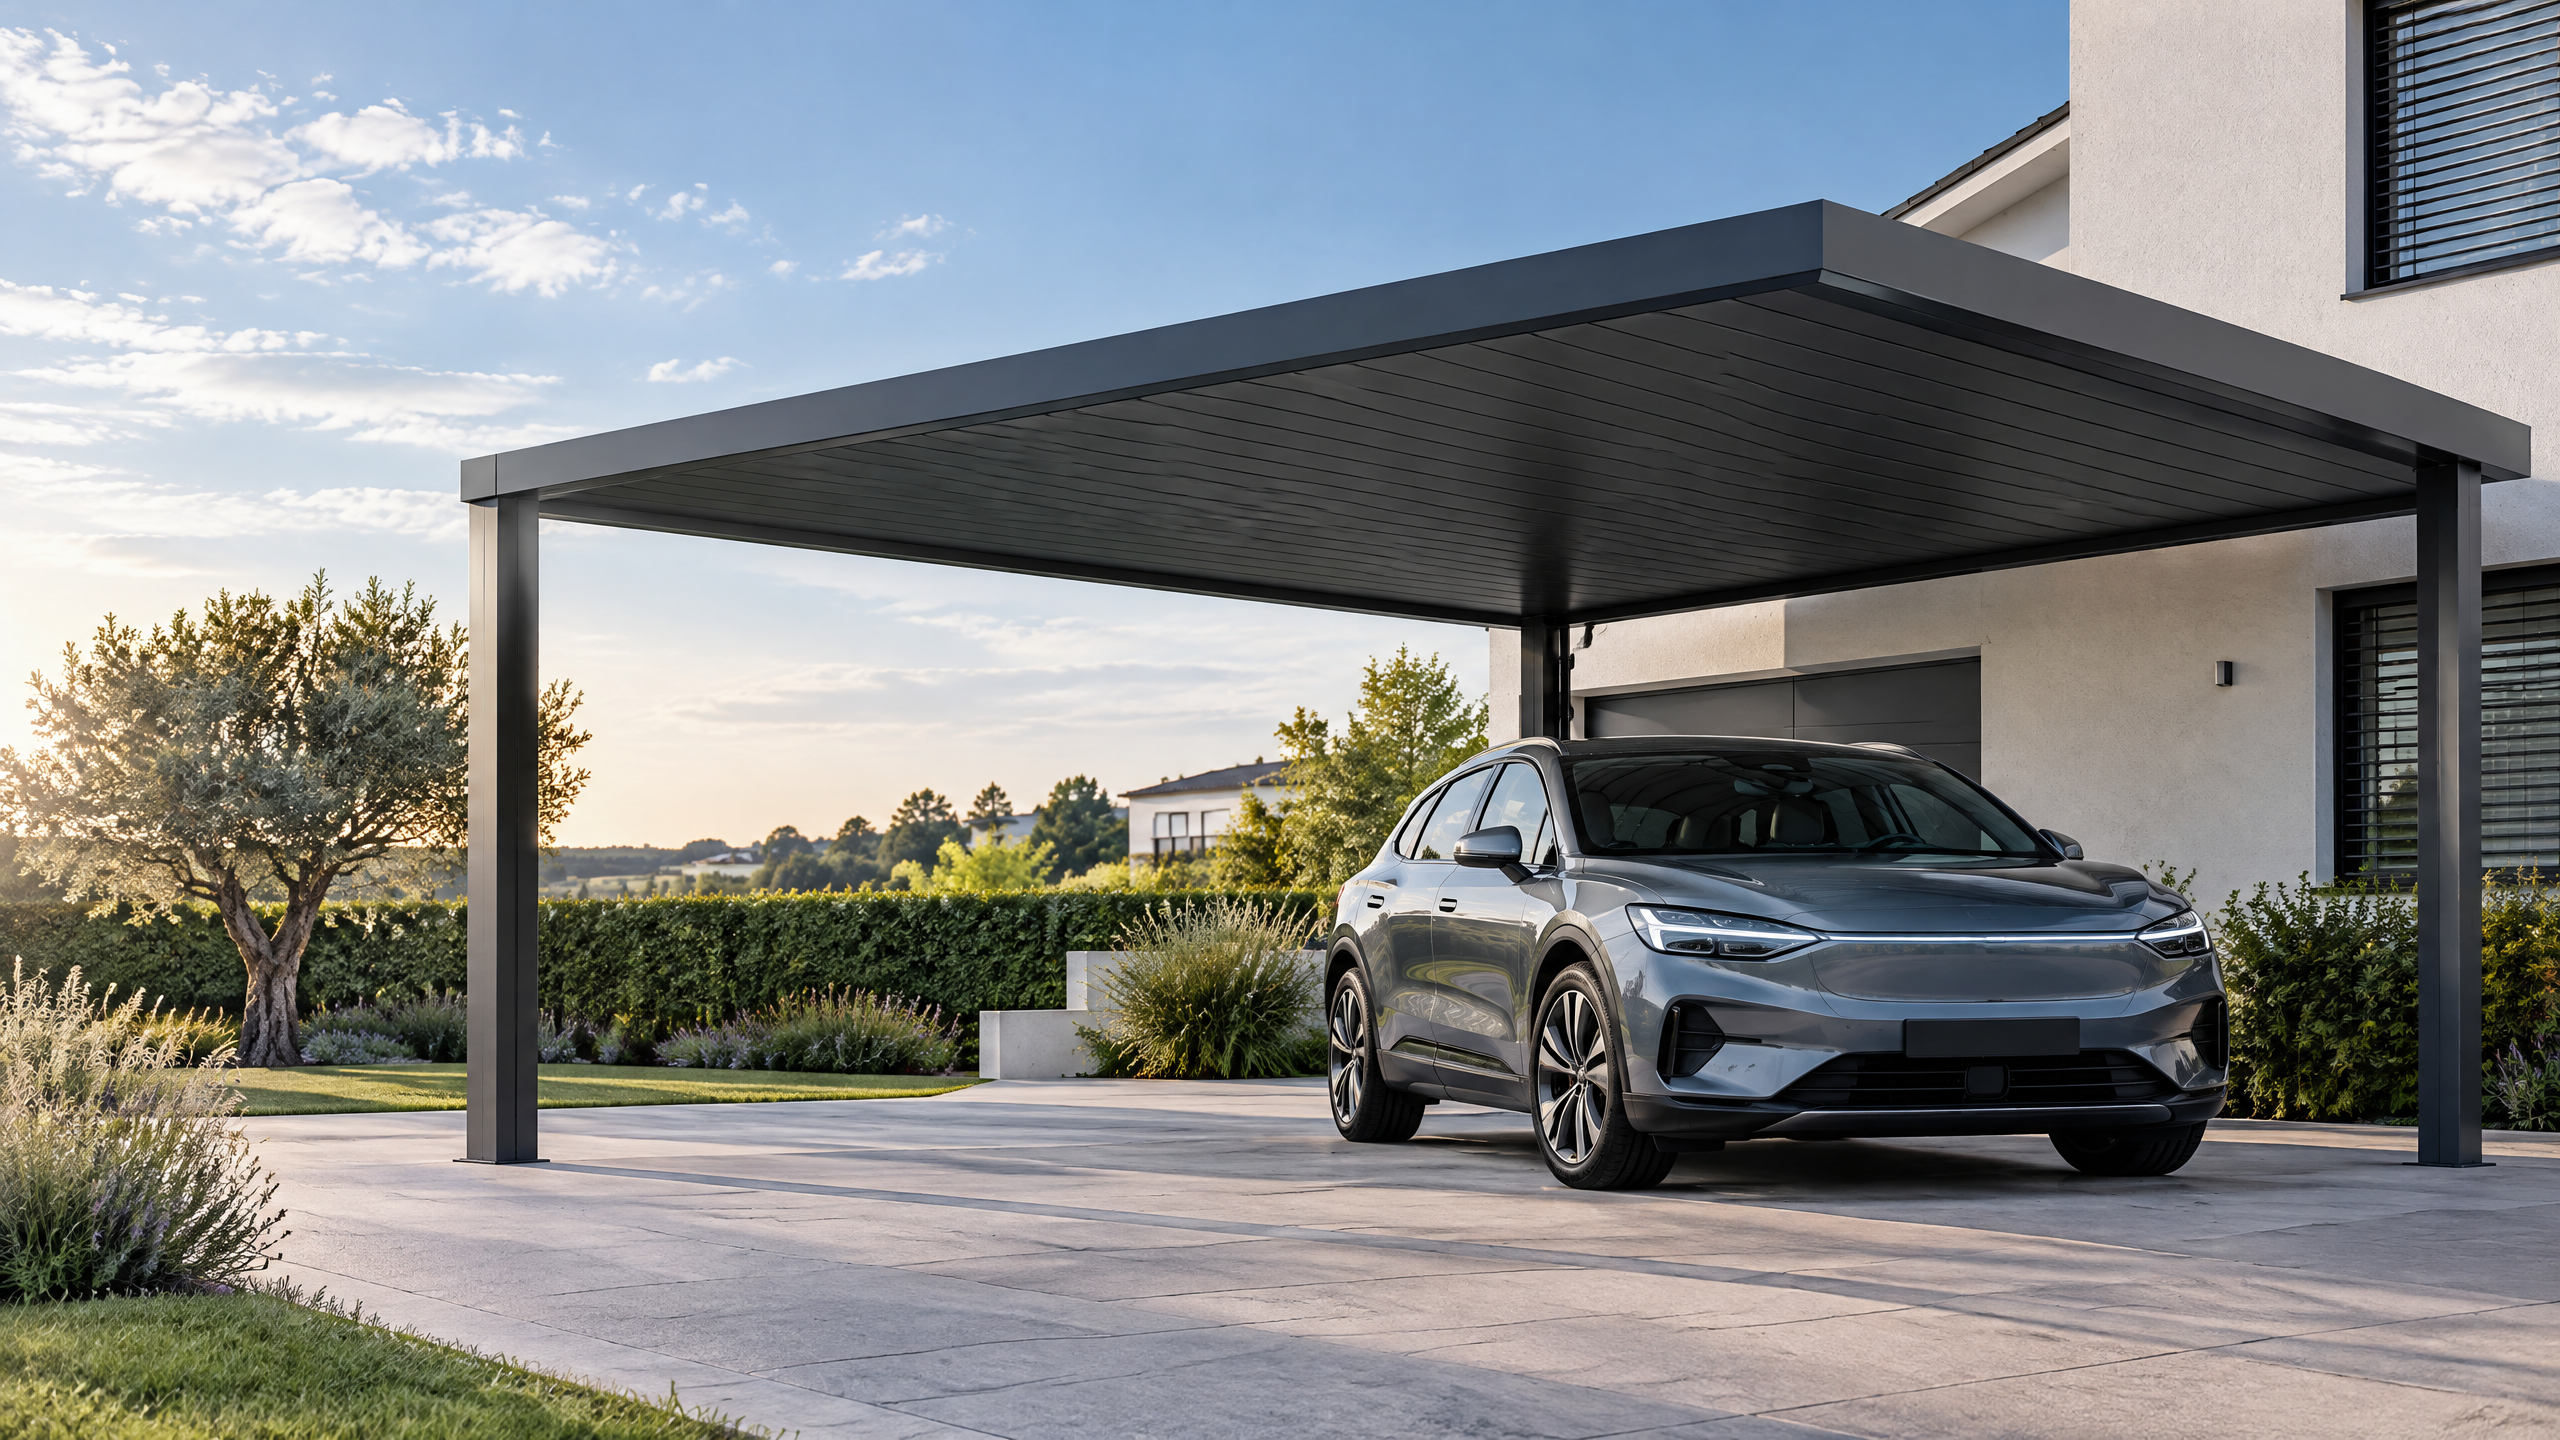
Direct answer (140–170 words) Double bay aluminium carport project supply becomes a decisive procurement factor when the supplier’s scope, documentation and factory evidence materially affect project outcomes: structural compatibility, finish durability, drainage and roof integration, supplier-led shop drawings, and coordinated installation readiness. For B2B buyers—distributors, architects, contractors, developers, solar EPCs and fleet operators—the supply decision is not only about price or delivery; it defines who is responsible for aluminium profile selection, anchor/foundation interface, roof drainage coordination, electrical routing (for canopies with PV), and warranty backstops. Early alignment of procurement scope prevents costly rework during installation and commissioning. To evaluate suppliers, demand documented proofs: material certificates, sectional and connection details, factory QA records, controlled shop drawing review cycles, clear change-order processes and a documented installation readiness checklist. Where local structural capacity, permits, electrical design, approvals, lead time, price, energy yield and warranty matter, these must be defined on a documented project basis and validated by local qualified professionals, installers, utilities and authorities.
Buyer context and scope boundary: who must care and why
Who cares
- Distributors: manage inventory, logistics, and resale terms.
- Architects: specify architectural carport specification and interfaces with buildings and site drainage.
- Contractors and installers: need clarity on installation readiness and supplier scope.
- Developers and owners: require performance, lifecycle cost and warranty clarity.
- Solar EPCs and fleet operators: require roof and electrical coordination for PV and fleet charging.
Why supply matters in this scope
- A double bay aluminium carport is typically a paired-span canopy with shared or adjacently mounted posts and a continuous roof plane. The procurement of the entire carport system (project supply) determines responsibility boundaries for foundations, anchorage details, rainwater management, flashings and PV support. If those boundaries are ambiguous, contractors may encounter gaps between "supply" and "install" responsibilities that drive scope disputes, delays and cost overruns.
Recommended contractual boundary checklist (to include in RFP/SOW)
- Delivered scope: catalogue items, shop drawings, factory acceptance tests.
- Installed scope: groundworks, anchor bolts, electrical interconnection, drainage tie-ins.
- Change control: lead times and responsibilities for design revisions.
- Acceptance criteria: inspection points, installation readiness sign-offs, warranty start triggers.
Note: Site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Core decision principle: when supply selection changes project outcomes
Principal rule Choose the supply option (full supply, kit supply, or parts-only) that minimizes project risk where the supplier’s controllable inputs have the largest impact on safety, schedule and lifecycle cost.
How this applies to double bay aluminium carport project supply
- Structural integrity: If the supplier controls the aluminium frame and connections, they should provide complete connection details and structural calculations or coordinate with the project’s engineer.
- Interface control: If the supplier supplies integrated gutters, flashings and PV rails, they should be responsible for roof drainage coordination and sealing details.
- Finish system: When the supplier provides anodizing or powder coating, confirm finish and fastener compatibility to avoid dissimilar-metal corrosion issues.
- Quality traceability: Factory evidence and shop drawing review cycles reduce on-site variation and rework.
Decision triggers that push toward broader supplier responsibility
- Complex roof drainage or concealed gutters across the double bay junctions.
- Integrated PV with roof-level electrical conduits and combiner boxes.
- Long lead extrusions or bespoke profiles requiring tooling.
- High wind/snow load locations requiring bespoke connections per Eurocodes [1] or equivalent local standards.
Planning inputs: data and documents needed before procurement
Minimum planning package to issue to suppliers
- Site survey and geotechnical baseline: soil bearing, frost depth, existing utilities.
- Architectural plan: location, adjacent structures, walkways and intended finishes.
- Wind/snow loads and local design criteria (reference national codes and Eurocodes where applicable) [1].
- Drainage and stormwater plan: existing system capacity and tie-in points.
- Electrical brief (if PV or EV charging): inverter location, AC/DC routing, earthing strategy.
- Project timeline and milestone constraints: on-site windows, phased builds.
- Warranty expectations: duration and coverage, defined start date.
- Acceptance and test regime: factory inspection, shop drawing review, installation readiness checklists.
Why each item matters
- Geotechnical and load data define foundation design and anchor sizing; the profile and connection detail depend on this data.
- Drainage and stormwater plans influence gutter sizing and fall direction across a double bay.
- Electrical briefs change the location and size of penetrations and routing allowances through members.
Planning deliverables to require from shortlisted suppliers
- Preliminary concept drawings with connection typologies.
- Aluminium material spec with temper and alloy (and mill certificates).
- Indicative lead times for bespoke extrusions, finishes and fasteners.
- A factory quality assurance summary and production capacity statement.
Technical specification and interfaces: what to check in detail
Key technical topics to include in the specification
- Architectural carport specification: dimension tolerances, module grid, column spacing, bracing, clear height, parapet or integrated gutter details.
- Aluminium profile selection: alloy grade, temper, wall thicknesses, and section modulus for sections used in beams, posts and rails.
- Connection design: bolted vs welded joints, splice plates, required corrosion protection, and galvanic separation where dissimilar metals meet.
- Roof systems and load paths: cladding type, panel spans, thermal movement joints and integration with PV modules if specified.
- Roof drainage coordination: gutter capacity, downpipe locations, roof falls, and overflow provisions.
- Finish and fastener compatibility: coating system and fastener metallurgy to prevent staining and corrosion.
- Shop drawing review process: review timelines, drawing levels (PID, SFD, fabrication drawings), and approval stamps.
- Installation readiness: packaging, on-site protection, lift plans, anchorage templates and as-built submission.
Aluminium profile selection: practical checks
- Confirm alloy and temper for structural use (for example EN AW-6061-T6 equivalents), and request mill/test certificates.
- Check extrusion tolerances and whether custom tooling is required — tooling changes increase lead time and cost.
- Evaluate section geometry for ease of on-site bolting and gasket placement to maintain weather seal.
Roof drainage coordination: common errors to avoid
- Neglecting fall direction across a multi-bay canopy; small misalignments at the double bay junction cause pooling.
- Ionic corrosion risk when aluminium gutters are tied to cast iron or untreated steel without dielectric separation.
- Failure to route overflow outlets away from pedestrian routes or equipment.
Finish and fastener compatibility: specification highlights
- Specify coating system (powder coat system class, film thickness) and compliance with relevant standards; consider AAMA specifications for coatings [3].
- Define fastener metallurgy and coatings: stainless fasteners may be required for coastal environments; confirm compatibility with aluminium to avoid galvanic corrosion (use isolating washers or coatings where necessary).
- Include inspection and adhesion test requirements at factory and on-site.
Shop drawing review: required content and process
- Shop drawings must include section cuts, connection details, splice plates with bolt sizes and torques, anchor bolt templates, and welding symbols where applicable.
- Define a two-stage review: 1) structural approval by a licensed engineer, 2) architectural review for interfaces, flashings and drainage.
- Allow time for one revision cycle in the procurement schedule; late changes should carry documented lead-time and cost impacts.
Installation readiness: on-site deliverables to expect
- Pre-assembled modules vs. site assembly instructions and weight/handling data.
- Anchor bolt templates (cast-in or drilled-in) and location tolerances.
- Lifting points and rigging instructions for safe hoisting.
- Packaging and storage guidance to avoid damage to finished aluminium surfaces and ingress to profiles.
Caveat: Structural design and detailed anchor/foundation design must align with local codes (Eurocodes or national equivalents) and be verified by a licensed structural engineer [1]. Site-specific capacities and approvals must be validated by local licensed professionals.
Procurement and factory evidence: what to ask suppliers for
Documents and evidence that materially reduce risk
- Material certificates (chemical composition and mechanical properties) and traceability for major structural members.
- Factory quality control plan: inspection points, dimensional checks, coating adhesion and thickness tests.
- Sample reports: powder coat color and thickness test, anodizing passivation reports (if anodized).
- Evidence of extrusion control: process capability for critical cross-section tolerances.
- Welding procedure specification (WPS) and welder qualifications for any welded components.
- Fastener certificate: grade, batch and plating details.
- Shop drawing review log and revision history.
Factory acceptance and verification
- Factory Acceptance Test (FAT) scope: dimensional checks, trial assembly if applicable, coating inspection, and packaging checks.
- Witness and third-party inspection options: define the right to inspect and the cost-sharing terms.
- Packing lists and palletization detail to ensure on-site handling matches installation equipment capacities.
Two decision tables to help buyers compare supplier offers
Table 1 — Supply scope comparison (choose which allocation reduces your project risk most)
| Supply Model | Supplier provides structural frame | Supplier provides gutters & flashings | Supplier provides PV rails/electrical interfaces | Buyer responsibilities |
|---|---|---|---|---|
| Full project supply | Yes | Yes | Yes (if specified) | Foundations, permits, final M&E connections |
| Fabrication-only supply | Yes | Partial | No | Flashings, PV rails, final connections, site coordination |
| Component/kit supply | Parts only | No | No | Full assembly, drainage coordination, PV mounting |
Table 2 — Evidence and QA acceptance matrix (minimum acceptable)
| Evidence / QA item | Minimal acceptable proof | Preferred proof |
|---|---|---|
| Aluminium material | Mill certificates (traceable) | Mill certificates + third-party chemical tests |
| Coating system | Supplier declaration + samples | AAMA-compliant tests or independent coating lab report [3] |
| Shop drawings | Full set with basic dimensions | Full set with approval stamps from structural engineer + revision log |
| Factory QA | QA plan summary | Factory FAT with witness and signed checklist |
Procurement clauses to reduce ambiguity
- Specify lead times for bespoke extrusions and finishes and the consequences for late delivery in the contract.
- Include a definitive shop drawing review schedule with maximum turn-around times.
- Require the supplier to hold an installation readiness meeting two weeks prior to mobilization.
- Define warranty start: upon practical completion or after final sign-off, with conditions documented.
Note: For finish testing and coating standards reference AAMA documents where relevant [3]. For material characteristics and aluminium industry best-practice, refer to The Aluminum Association [2]. Use ISO or national equivalents to define specific test methods where needed [4].
Site installation and operations: practical handovers and checks
Pre-mobilization checks (installation readiness)
- Confirm anchor locations with “as-built” utilities to avoid clashes.
- Receive and review the supplier’s installation method statement, lifting plan and risk assessment.
- Validate that anchor bolt templates match the approved shop drawings and that foundation strength matches required embedment and torque values.
- Confirm site storage provisions to protect finished surfaces (e.g., dry, ventilated cover, off-ground pallets).
On-site coordination points
- Roof drainage coordination: verify fall direction on site and that overflow/drain positions match supplier drawings. Ensure tie-in to local stormwater system is permitted and available.
- Electrical and PV: ensure conduit runs and insertion points through columns/rails are protected from weather and only made where shown on approved drawings.
- Fasteners and finish compatibility: ensure the correct fastener packs and sleeve washers are used as supplied; replacements must be approved by the supplier.
Acceptance and commissioning
- Use a documented installation checklist that includes dimensional verification, torque checks for bolted connections, sealant thickness and weathering checks, and initial water test for drainage systems when safe to do so.
- Supplier should provide as-built drawings and a package of certificates: mill certs, coating certificates, fastener batches, and FAT reports.
Operations and maintenance handover
- Require the supplier to provide an O&M manual that includes cleaning regimes for powder coated or anodized surfaces, fastener inspections, and sealant renewal intervals.
- Establish a warranty claim pathway: who to contact, response times, and inspection process.
Safety and lifting
- Large pre-fabricated modules for double bay carports can be heavy and have high wind exposure during handling. Ensure a qualified rigger and lift plan are mandatory under the contract.
Reminder: Installation specifics, including anchor design and on-site conditions, must be validated by local qualified professionals, installers, utilities and authorities.
Implementation risks and how procurement allocation mitigates them
Common implementation risks
- Mismatched connection dimensions between factory-fabricated members and site-cast anchors.
- Pooling at bay junctions due to inadequate roof drainage coordination.
- Corrosion from incompatible fastener and finish choices, especially in coastal or industrial atmospheres.
- Delays from bespoke extrusion tooling or long finish queues at external coaters.
- Warranty disputes due to unclear warranty commencement or excluded items.
Risk mitigation via procurement choices
- Transfer responsibility for complex interfaces (roof drainage, PV rails) to supplier under full supply to reduce on-site variation.
- Require supplier-supplied anchor templates and pre-approved foundation drawings referenced to working points.
- Include finish and fastener compatibility clause requiring supplier to submit a fastener schedule with metallurgy and protective treatments for approval.
- Insist on a shop drawing review with at least one iterative revision built into the commercial timeline to manage change without schedule slippage.
- Build milestone-based payments tied to delivery of evidence (mill certs, FAT reports, approved shop drawings) to align incentives.
Risk allocation table — who should own which risk?
| Risk | Best ownership (to reduce project cost & delay) | Rationale |
|---|---|---|
| Anchor mismatch | Supplier if anchor templates supplied; otherwise Contractor/Engineer | Supplier-supplied templates reduce drilling errors |
| Roof pooling | Supplier if gutters & flashings supplied | Supplier can manage continuous falls and joint detailing |
| Corrosion at fasteners | Supplier for fastener supply or Engineer if owner-supplied | Supplier control reduces galvanic mismatch |
| Lead time on extrusions | Supplier | Supplier control of tooling and extruder relationships |
| PV electrical interface | Solar EPC if integrator; supplier if they supply PV rails | Clear coordination prevents penetrations errors |
Named six-step buyer workflow for double bay aluminium carport project supply
A practical prescriptive workflow buyers can adopt.
Step 1 — Define project basis and responsibilities (2–4 weeks)
- Produce a Project Basis Document: site data, loads, finishes, electrical brief, timeline and acceptance criteria.
- Identify who will be responsible for foundations, drainage tie-ins and final electrical connections.
- Engage structural and geotechnical consultants to set design parameters.
Step 2 — Issue a focused RFP with mandatory evidence list (2–6 weeks for procurement)
- Include a mandatory list of documents: mill certs, factory QA, sample finishes, preliminary shop drawings and FAT rights.
- Define procurement models sought (full supply, fabrication-only, kit).
Step 3 — Evaluate technical offers and shortlist (2–4 weeks)
- Score offers against technical evidence, lead times for custom extrusions, finish options, and factory capacity.
- Use the decision tables to rank supply models by risk transfer and cost impact.
Step 4 — Approve shop drawings and finalize contract (4–8 weeks)
- Ensure one revision cycle is included. Confirm shop drawing review includes structural engineer sign-off and architectural interface approval.
- Lock in lead times, completion milestones, and FAT schedule.
Step 5 — Factory acceptance and pre-shipment verification (1–3 weeks)
- Conduct or witness FAT: dimensional checks, trial assembly where feasible, coating inspection and packaging verification.
- Resolve non-conformities before shipment.
Step 6 — Installation, commissioning and handover (2–6 weeks depending on project size)
- Use an installation readiness checklist and require as-built documentation and O&M manuals.
- Conduct final inspections and confirm warranty start criteria.
Notes on timelines: these are indicative and depend on project complexity, availability of local approvals, bespoke extrusion tooling and finish availability.
Frequently asked questions (FAQ)
Q: How does double bay aluminium carport project supply differ from single-bay procurement? A: Double bay carports have contiguous roof planes, shared or closely adjacent structural elements and more complex guttering and junction detailing. Supply scope must address junction continuity, roof drainage coordination and any increased wind load effects across the wider span.
Q: What evidence should I insist on to prove material quality? A: Mill certificates for alloy and temper, third-party chemical/mechanical testing where risk is high, and batch traceability for all major members. For coatings, AAMA or equivalent test reports are preferred [3].
Q: Can I source raw extrusions locally and have the supplier fabricate? A: Yes. But ensure the supplier is approved to fabricate with the nominated extrusions and that the extrusions meet the specified tolerances and alloy grades. A signed interface document specifying acceptance criteria is advisable.
Q: How is roof drainage coordination best handled? A: Include gutters and flashings in the supplier scope where possible. If the buyer retains drainage, require clear interface points, fall direction confirmation and overflow provisions in the shop drawings.
Q: What is shop drawing review and why is it important? A: Shop drawing review is the process by which supplier-prepared fabrication and assembly drawings are checked and approved by the project design team (structural and architectural). It prevents field conflicts and defines the exact fabrication geometry.
Q: Who is responsible for installation readiness? A: Responsibility should be contractually defined. Good practice is a combined responsibility: supplier provides anchor templates, lifting instructions and as-built drawings; contractor ensures site foundations and access match those inputs.
Q: How do finish and fastener compatibility issues present on-site? A: Issues can show as staining, accelerated corrosion or failed coatings near fastener interfaces. Avoid by specifying compatible materials, using isolators, and confirming fastener coatings or inherently corrosion-resistant materials (e.g., stainless steel).
Q: Are there global standards I should reference for design? A: Use applicable national structural standards or the Eurocodes for locations that follow them [1]. For material properties and best practice for aluminium, consult The Aluminum Association [2] and for finishing and performance testing, consult standards such as those referenced by AAMA [3]. Use ISO for specific test methods where relevant [4].
Conclusion
Double bay aluminium carport project supply matters most where the supplier’s deliverables control the highest-risk interfaces: structural connections, roof drainage, finishes and PV/electrical integration. Procurement choices determine who handles those risks. B2B buyers should adopt a documented, evidence-led approach: define the project basis, require mill and coating certificates, mandate a shop drawing review process, insist on factory acceptance testing, and set clear installation readiness and warranty start conditions. Transfer responsibility for complex, high-impact items (for example gutters that cross bay junctions or PV rails integrated into the frame) to the party best able to control them; this typically reduces on-site rework and contractual disputes.
For product-level exploration, see NordArch architectural aluminium system and our all systems overview. For procurement templates and deeper sourcing checklists consult our sourcing guides.
Mid-article call to action If you would like to discuss how double bay aluminium carport project supply should be scoped on your project, contact our team at /inquiry or email info@carportiva.com.
Final reminder: site-specific structural capacity, foundations, permits, electrical design, approvals, lead time, price, energy yield and warranty require a documented project basis and relevant local qualified professionals, installers, utilities and authorities.
Closing CTA For a project discussion or to request our procurement checklist and evidence template, please contact /inquiry or email info@carportiva.com.
References (select)
- Eurocodes and structural design guidance for design loads and verification where applicable [1].
- Aluminium material properties and industry guidance [2].
- Finishing performance and coating testing references such as AAMA documents for powder coat and other exterior finishes [3].
- ISO for specific test method references where required [4].
References
- European Commission Eurocodes: https://eurocodes.jrc.ec.europa.eu/
- The Aluminum Association: https://www.aluminum.org/
- American Architectural Manufacturers Association: https://aamanet.org/
- ISO Online Browsing Platform: https://www.iso.org/obp/ui/
Keep the project brief connected.
Bring the actual project brief to the engineering table.
Share your location, layout, target application and available technical inputs. Carportiva can help identify the relevant product-interface information before a project-specific commercial discussion.
Request a project discussion